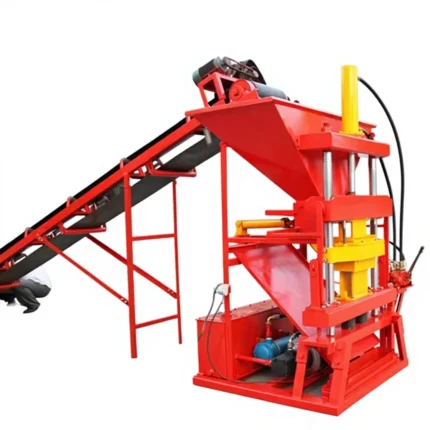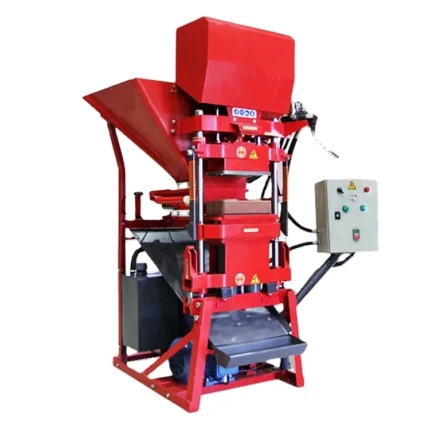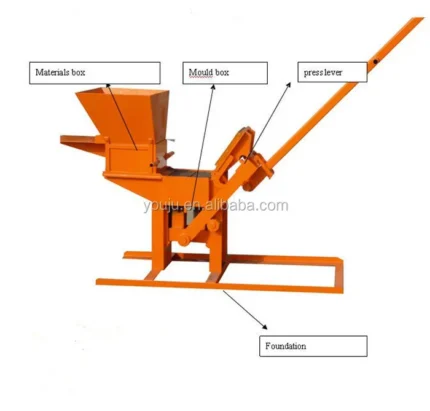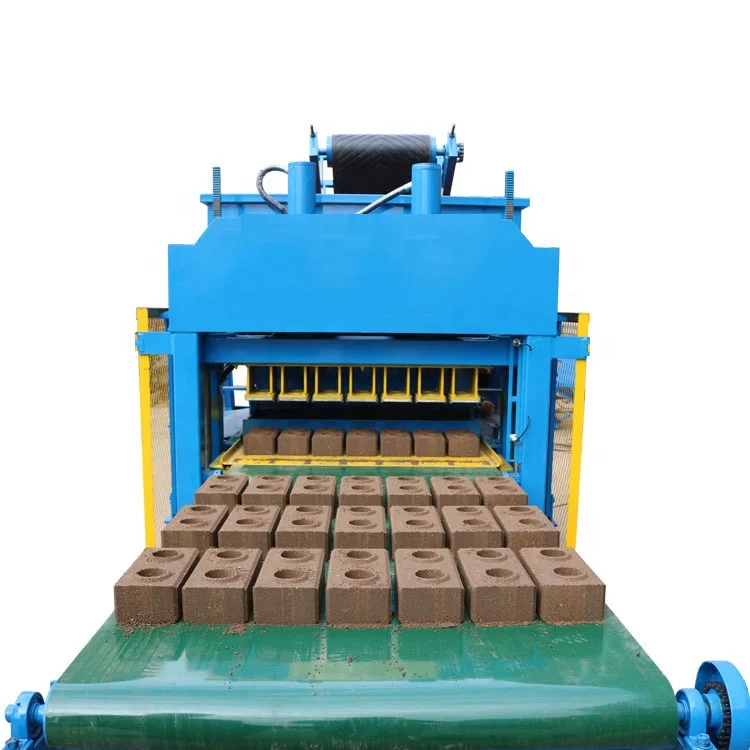
Description
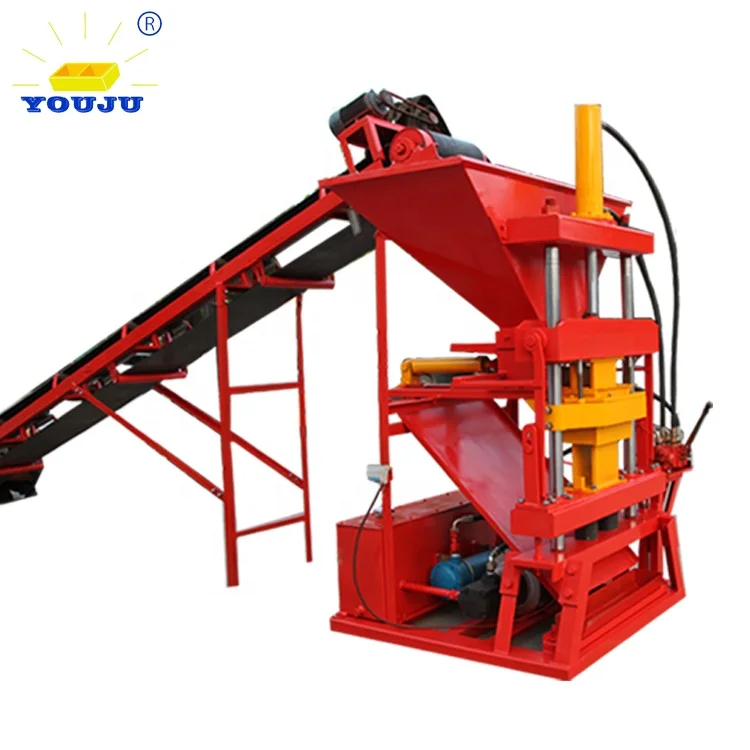
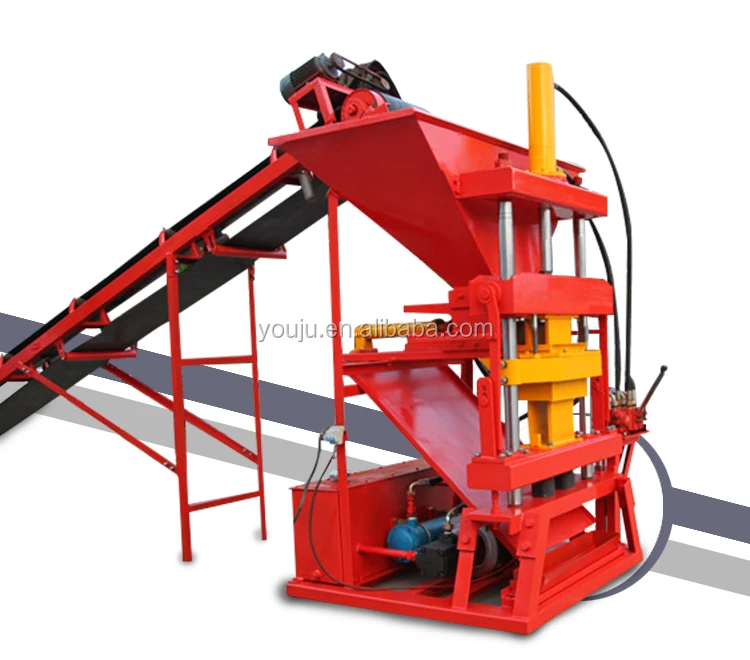
Precision control configuration — the ECO2700 hydraulic circuit and PLC display language are locked to your local voltage and operator language before the machine leaves the factory, so the 16 MPa pressing force actually delivers repeatable clay interlocking brick quality on day one.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | ECO2700 |
| Product Type | Hydraulic Clay Interlocking Brick Making Machine |
| Overall Dimensions (L×W×H) | 1000 × 1000 × 1800 mm |
| Shaping Cycle | 15–20 seconds (basis not stated in source — confirm block format) |
| Hydraulic Pressure | 16 MPa |
| Rated Power | 5.5 kW |
| Voltage & Frequency | 380V, 3-phase, 50Hz (customizable to local supply) |
| Total Weight | 1000 KGS |
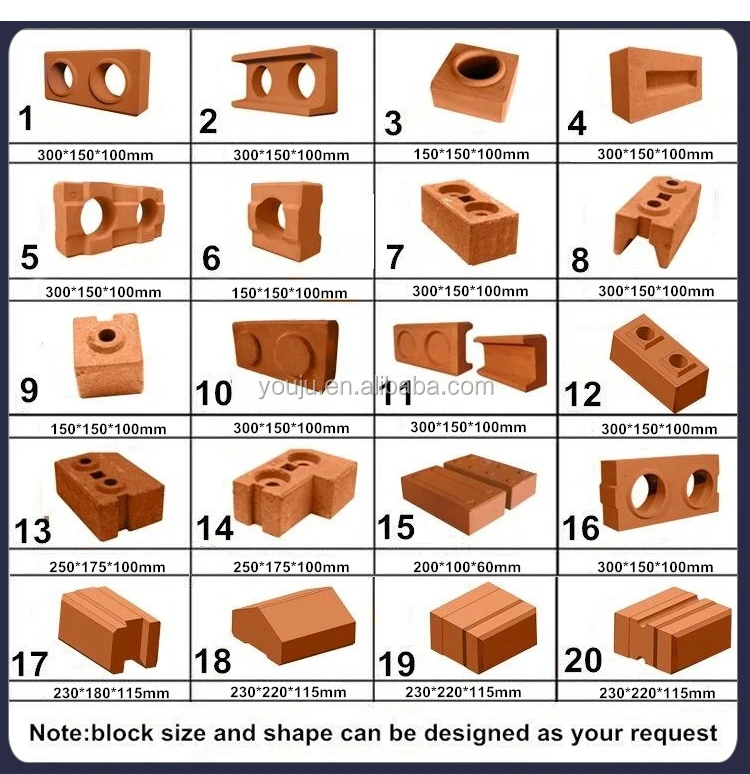
| Mould Format | Interlocking clay brick (dimensions to confirm per buyer drawing) |
| Control System | To be confirmed (PLC or manual — verify at inquiry stage) |
| Automation Level | Semi-automatic with manual pallet handling |
| Stacking Method | Manual |
| Certification | CE |
| Warranty | 1 year |
Application Suitability
| Application | Material or Output |
|---|---|
| Small workshop clay interlocking brick production | Local clay, mud, and soil blends |
| On-site housing project brick forming | Excavated site soil mixed with stabilizer |
| Low-investment community block yard | Clay with sand or laterite filler |
| Rural construction contractor brick supply | Raw clay with cement or lime binder |
Why the PLC Language Question Beats the Capacity Question Every Time
An automatic clay interlocking brick machine PLC controlled in a language your operator cannot read is a semi-automatic machine with an expensive screen.
I spent two weeks in a brick plant outside Ho Chi Minh City watching exactly this happen. The press cycle was solid, the hydraulic pressure held within tolerance, but the operator could not navigate the alarm screens. Every fault meant a phone call, a translation delay, and twenty minutes of lost production. The automatic stacking station sat idle because nobody trusted the auto mode [NEED_CITE: PLC display language and operator comprehension in Southeast Asian block plants]. That plant owner paid for automation and received a very heavy manual press.
What Control Intelligence Actually Removes from the Operator
A consistent shaping cycle depends on more than a timer. The hydraulic valve must open and close at the same point every stroke, and the pressure must reach 16 MPa before the mould releases. When an automatic clay interlocking brick machine PLC controlled system manages these sequences, the variation between the first brick of the morning and the five-hundredth brick of the afternoon shrinks to a level that manual valve operation simply cannot match.
Where the Upgrade Path Matters for Growing Plants
Most buyers start with manual pallet feeding and stacking because the capital outlay fits their first-year cash flow. The question that rarely gets asked early enough is whether the control architecture supports adding automatic pallet feeders and stackers later without replacing the main PLC. Confirming this at the inquiry stage prevents a situation where the only way to automate is to buy a different machine entirely [NEED_CITE: PLC module compatibility for staged automation upgrades in hydraulic brick presses].
Reading the Specs That Actually Shape Your Daily Output
The 15–20 second shaping cycle sounds fast until you account for manual pallet placement, clay feeding into the hopper, and hand-stacking at the output end. With a single operator handling all auxiliary tasks, the realistic cycle stretches considerably beyond the press stroke alone. The 5.5 kW rated power keeps energy draw manageable for sites with limited transformer capacity, which is common on housing project sites running temporary power. The 16 MPa hydraulic pressure must be matched against your specific clay mix design — a high-sand blend compresses differently from a pure laterite soil, and the pressure setting that produces strong bricks from one mix will leave another under-compacted.
What Misconfigured Controls Cost After Arrival
Voltage confirmed wrong at the container door means weeks of downtime while a transformer is sourced locally. A PLC display in English for a Vietnamese, Burmese, or Bahasa-speaking crew means errors get ignored until something breaks. Hydraulic pressure set to a default rather than your clay mix means bricks crumble at the curing rack or crack during transport — and the blame lands on the raw material supplier instead of the machine setup [NEED_CITE: hydraulic pressure calibration against local clay aggregate in brick production].
Why Procurement Through This Channel Works for Control-Focused Buyers
Block machinery is the single focus here, which means the PLC program, hydraulic circuit, and mould tooling are specified as one matched system rather than pulled from separate catalogues. The control language and voltage are confirmed before production starts, not discovered during commissioning. Mould designs are built to the interlocking brick format your market actually buys, including custom drawings when standard formats do not fit. The automation level is selectable — start semi-automatic now and add pallet feeding or stacking modules when volume justifies the investment. Every machine ships with a factory test record run on parameters matching your configuration.
Documentation & Verification
- Machine specification sheet listing confirmed voltage, frequency, and PLC language
- Hydraulic and electrical schematic for the exact ECO2700 configuration ordered
- Factory test record showing shaping cycle and pressure on your clay mix parameters
- Mould drawing and interlocking brick format dimensions before production begins
- Operation and maintenance manual with control system section in operator language
- CE declaration covering the press and hydraulic system scope
Installation, Commissioning & Support
- 1000 × 1000 mm footprint fits standard workshop floors without special foundations
- 5.5 kW draw requires a dedicated 3-phase circuit matched to confirmed voltage and frequency
- Machine arrives at 1000 KGS — plan forklift or gantry access for unloading
- First-day commissioning includes hydraulic pressure calibration against your clay sample
- Operator training covers PLC navigation, alarm response, and mould change procedure
- Wear parts list identifies hydraulic seals, solenoid valves, and sensor replacements
What to Prepare Before Requesting a Quotation
Share the specific interlocking brick dimensions your market sells, the clay or soil type available locally, and any stabilizer you plan to add. Confirm your site voltage and frequency — the 380V 50Hz baseline is adjustable, but only if the target is stated upfront. Specify the PLC display language your operators need, and whether your plan includes adding automatic pallet handling at a later stage.
Frequently Asked Questions
Q: How is the 15–20 second shaping cycle verified, and for which interlocking brick format does it apply?
A: The shaping cycle is measured during the factory test using the specific mould and clay mix parameters you confirm at the order stage. The 15–20 second figure represents the hydraulic press stroke only and does not include manual feeding, pallet placement, or stacking time. Your quotation includes a capacity calculation tied to the exact brick format you specify.
Q: What automation level does the ECO2700 ship with, and what is the upgrade path?
A: The standard configuration is semi-automatic with manual pallet handling and stacking. The PLC architecture can be specified to support future addition of automatic pallet feeders and stacking stations. Confirming this upgrade path at the inquiry stage ensures the control modules and wiring harness are pre-configured to accept auxiliary equipment without a full PLC replacement.
Q: How are voltage, frequency, and PLC display language confirmed before shipment?
A: These parameters are locked during the quotation stage and documented on the machine specification sheet. The factory test is run at the confirmed voltage and frequency, and the PLC display is set to the agreed language before the machine is packed. Any mismatch caught at this stage costs days, not weeks.
Q: How is hydraulic pressure matched to local clay mix design?
A: The 16 MPa system pressure is adjustable, and the correct working pressure depends on your clay composition, moisture content, and stabilizer ratio. During commissioning, test bricks are pressed at several pressure settings and broken to verify compressive strength. The optimal setting is then recorded in your operation manual for repeatable production.
Q: What control-side spare parts are included, and what is the replacement lead time?
A: The spare parts list covers hydraulic seals, solenoid valves, proximity sensors, and PLC relay modules specific to your ECO2700 configuration. Replacement lead times depend on part type and destination. Confirming critical spares at the order stage means they ship in the same container, avoiding production stops while waiting for a single sensor.