Description
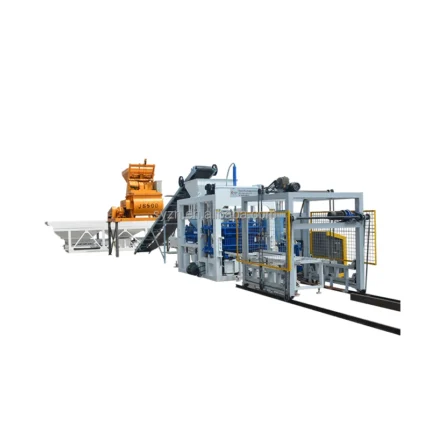
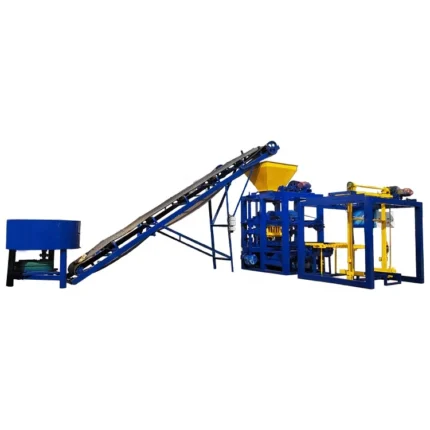
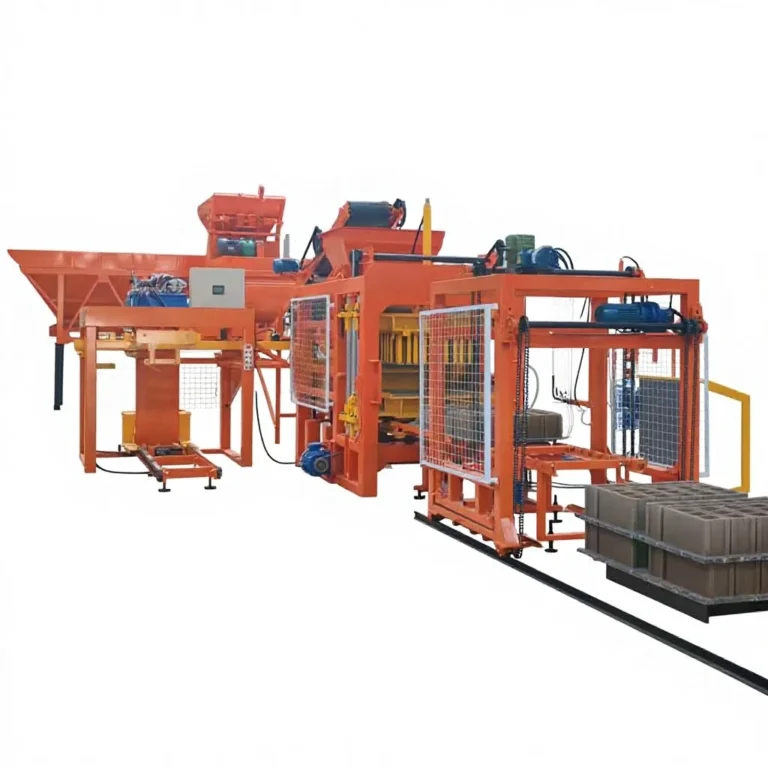
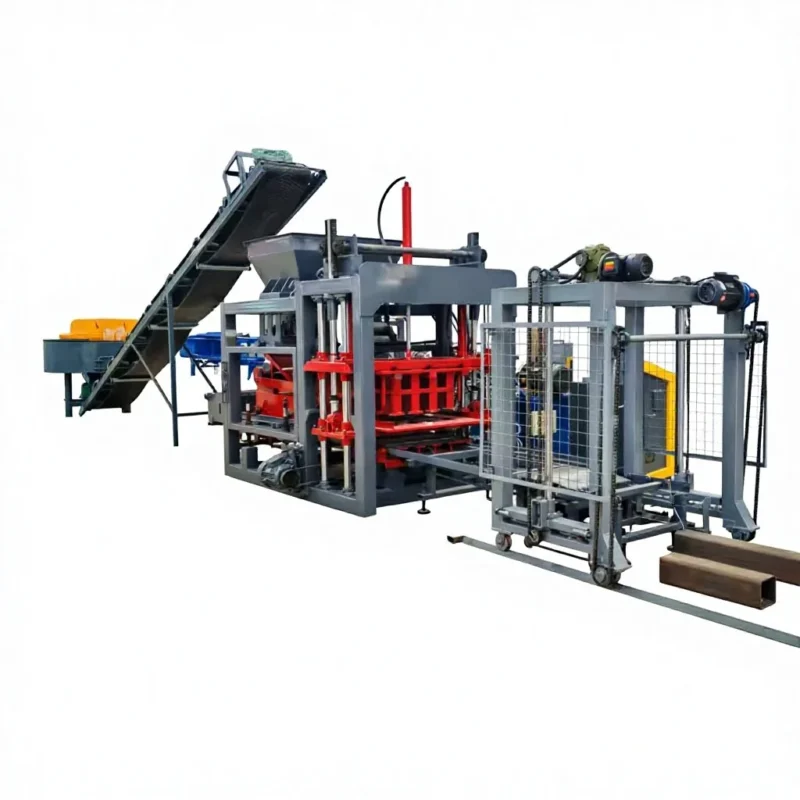
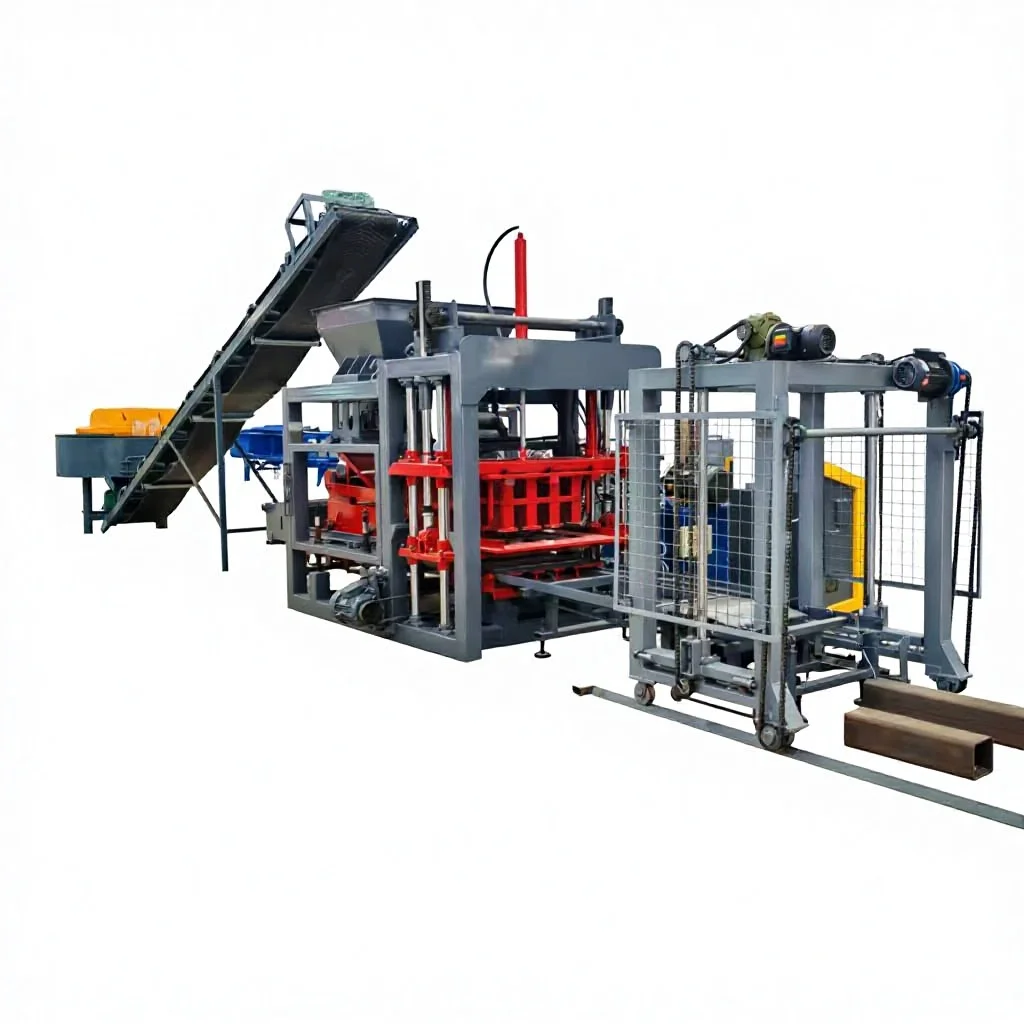
Matched system configuration — The QT4-15A fully automatic block press, pallet handling and control logic are specified as one integrated line rather than assembled from disconnected suppliers, so cycle times align from mixer to stacker.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-15A |
| Product Type | Fully Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 4100×1600×2600 mm |
| Rated Hydraulic Pressure | 16–21 MPa |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency | 4200 r/min |
| Vibration Force | 55 kN |
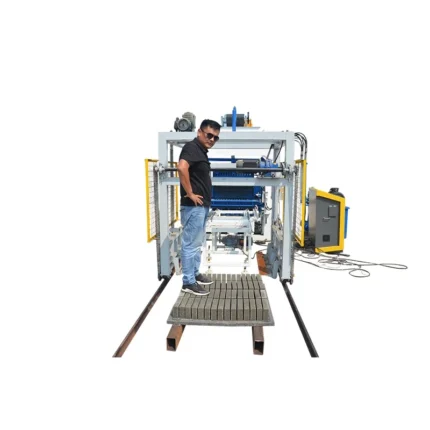
| Pallet Size | 880×550 mm |
| Molding Cycle | 25–30 s (basis not stated in source — confirm block format / material / thickness) |
| Overall Power | 18.45 kW |
| Total Mass | 4 T |
| Demolding Method | Hydraulic |
| Factory Area Required | 300 m² |
| Control System | PLC |
| Automation Level | Fully Automatic |
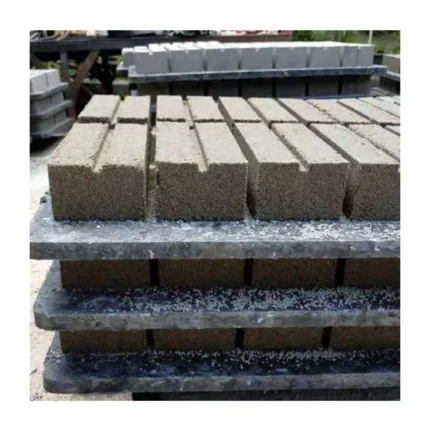
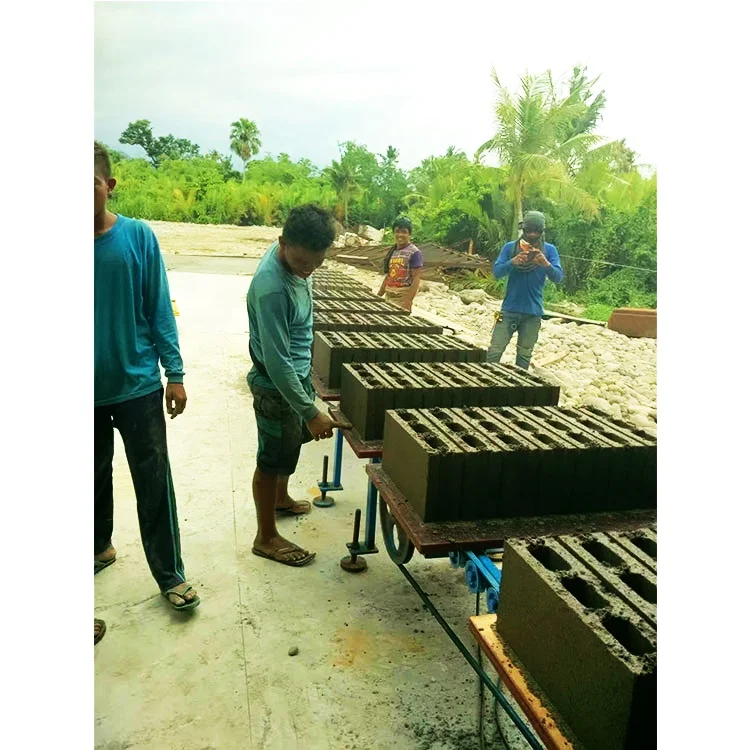
| Applied Products | Concrete blocks, hollow/solid blocks, pavers, interlocking blocks, curbstone, colored pavers |
| Raw Materials | Crushed stone, sand, cement, dust, fly ash, gravel, slag |
| Warranty | 1 year (whole machine, excluding spare parts) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow and solid block production for load-bearing walls | Crushed stone, sand, cement, fly ash blends |
| Interlocking paver manufacturing for driveways and walkways | Fine aggregate with cement and pigment additives |
| Curbstone and kerb production for municipal infrastructure | Coarse gravel and cement mixes requiring high hydraulic pressure |
| On-site block production for housing development projects | Locally sourced sand, dust and slag adjusted to available aggregate |
| Concrete product plants expanding format range | Multiple mould formats on a single 880×550 mm pallet platform |
Why "25–30 Seconds per Cycle" Needs a Format Attached
Cycle time means nothing until you know which block format and mix design it was measured on.
Every block machine quotation I have reviewed from拉美 brick plants includes a cycle time figure, but buyers repeatedly discover that the number quoted assumed a thin paver while they need hollow blocks that take noticeably longer to compact and demold. The automatic QT4-15A block machine PLC controlled system records actual cycle data per format, so you can see where time goes rather than trusting a single headline number. When a plant owner in Colombia told me his previous machine "never hit quoted output," the issue was not the press — it was that the pallet return and stacking stations were undersized for the press speed, leaving the machine idle between cycles [NEED_CITE: common causes of output shortfall in block production lines].
How PLC Control Removes Operator Variability from the Block Line
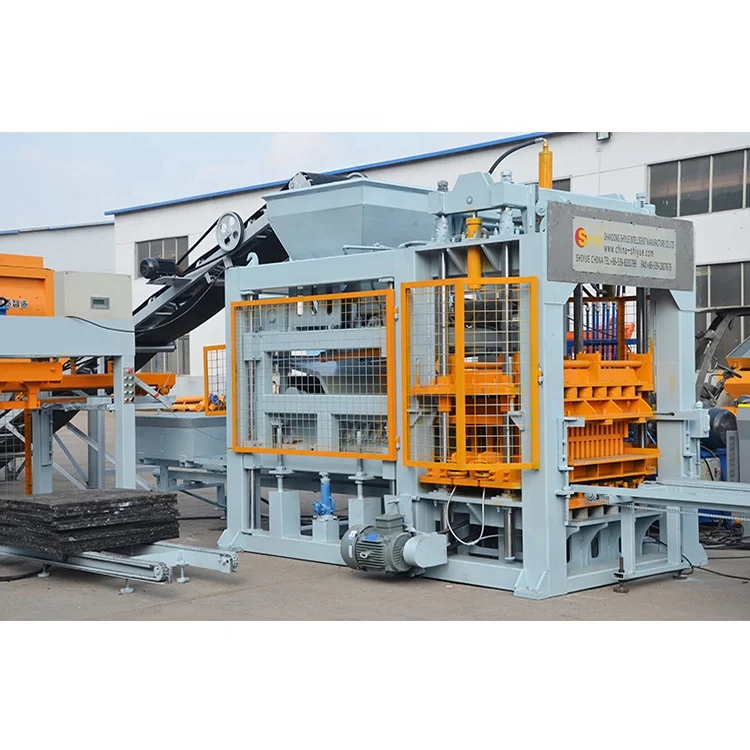
A manual or semi-automatic press relies on the operator to judge when vibration is sufficient and when to release hydraulic pressure. The automatic QT4-15A block machine PLC controlled logic standardizes these decisions: vibration duration, pressure ramp, and demolding sequence are stored per mould format and recalled automatically. This means the third shift produces blocks with the same density as the first, regardless of who is at the panel.
Where Automation Actually Reduces Labour on the Block Line
The intelligent side of this machine is not just the PLC screen — it is what the control system removes from the operator’s hands. Automatic pallet feeding means no one is lifting wooden or bamboo pallets into position every 25 to 30 seconds. When the line includes automatic stacking, cured blocks are cubed for forklift transport without manual handling. The operator’s role shifts from physical labour to monitoring batch consistency and managing mould changes [NEED_CITE: labour allocation in fully automatic versus semi-automatic block plants].
What the Pressure and Vibration Numbers Mean for Block Density
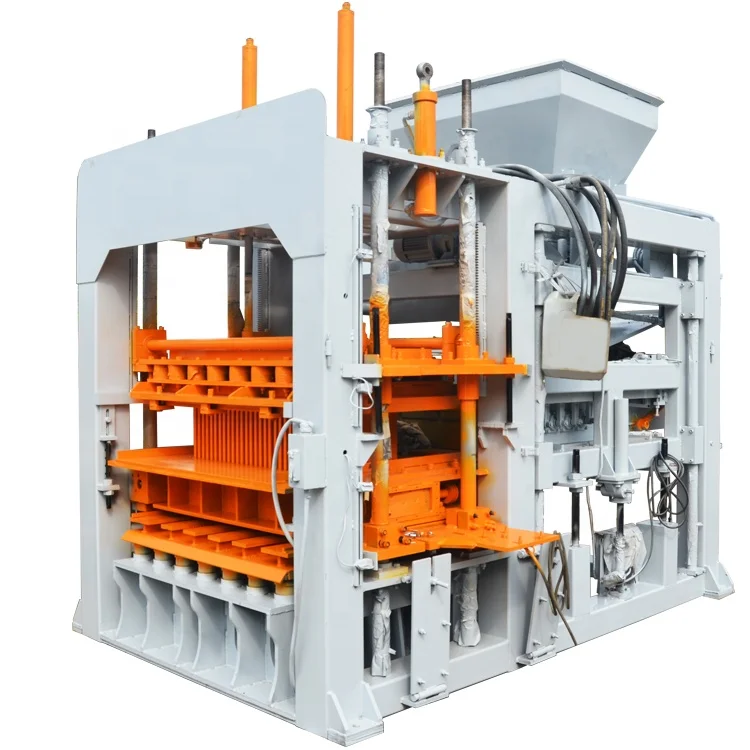
The 16–21 MPa hydraulic pressure and 55 kN vibration force on the QT4-15A are not independent specifications — they work together during compaction. Platform vibration at 4200 r/min settles the mix into the mould cavity, while hydraulic pressure applied from above compresses the material to eliminate voids. If vibration force is too low for a given mix, blocks emerge with weak corners. If pressure is too high for a fine-aggregate paver mix, the material is squeezed out of the mould before it sets. The 880×550 mm pallet size determines how many blocks fit per cycle, and that pallet must match the curing rack spacing and forklift tine width already in your yard.
The Cost of Skipping Voltage and Language Confirmation Before Shipment
I once arrived at a plant in Peru where a block machine sat idle for ten days because the PLC display was in Chinese and the local electrician could not navigate the menus. The motor was also wired for 380V/50Hz while the site supply was 220V/60Hz. With the QT4-15A, voltage, frequency and PLC display language are confirmed before production begins — not after the container arrives. Skipping this step does not just delay commissioning; it risks motor burnout on first start [NEED_CITE: electrical mismatch failures in exported industrial machinery].
Why Buyers Source the QT4-15A Through This Channel
Block machinery is the single focus here, so the press, moulds, pallets and handling equipment are specified as one matched system. Configuration is set against your actual mix design and local aggregate, not a catalogue default. Mould design covers the formats your market actually sells, including custom drawings when standard options do not fit. Automation level is selectable — you can start with the fully automatic QT4-15A and add stacking or cubing modules as demand grows. Installation support includes operator training so your team runs the line independently from day one.
Documentation & Verification
- Line layout with capacity calculation stating the block format assumed for the 25–30 s cycle
- Machine specification sheet confirming hydraulic pressure, vibration force and pallet dimensions
- Mould drawing and format list for every block type included in your order
- Hydraulic and electrical schematic for on-site troubleshooting and maintenance
- Voltage, frequency and PLC display language confirmation recorded before production
- Factory test record on your target block format and mix before dispatch
Installation, Commissioning & Support
- Foundation must support 4 T total mass with level tolerances for the 4100×1600 mm footprint
- Dedicated power circuit sized for 18.45 kW overall draw at confirmed voltage and frequency
- Machine ships partially assembled; hydraulic and electrical connections completed on-site
- First-run commissioning includes cycle tuning on your specific mould format and mix design
- Operator training covers PLC navigation, mould change procedure and daily maintenance checklist
- Wear parts and spare mould list provided with recommended replacement intervals
What to Share Before Requesting a Quotation
To size the QT4-15A correctly, provide your target block formats with dimensions, the daily output you need per format, and the raw materials available locally including aggregate grading. Share your site voltage and frequency, preferred PLC display language, and whether your existing curing area uses racks or floor curing. If you already operate a block line, note the pallet size and forklift capacity so the new equipment integrates without requiring changes downstream.
Frequently Asked Questions
Q: How is daily output calculated per block format on the QT4-15A?
A: Daily output depends on the specific block format, mould cavity count, and confirmed cycle time for that format. The 25–30 second cycle figure must be validated against your target block dimensions and mix design. We provide a capacity calculation sheet that states exactly which format was assumed, so the number you plan against reflects your actual product, not a generic estimate.
Q: What PLC brand and display language options are available?
A: The PLC brand and display language are confirmed during the order process based on your operator team’s requirements and local service availability. Common languages include English, Spanish and others upon request. Confirming this before production avoids the situation where a machine arrives with a display your team cannot read, delaying commissioning.
Q: How does the automation level affect labour requirements on the block line?
A: The fully automatic configuration with PLC control reduces manual pallet handling and stacking tasks, shifting the operator role toward monitoring and mould changes. Actual labour count depends on whether automatic stacking and cubing are included in your line layout. A semi-automatic starting point remains available if your volume does not yet justify full automation.
Q: What is the mould change procedure and expected time per format?
A: Mould change time depends on the format and whether quick-release fixtures are included in your configuration. The procedure involves releasing the current mould from the press, mounting the new mould, and recalling the matching PLC program for vibration and pressure settings. We provide a format list and change procedure document so your team can plan production scheduling around realistic changeover durations.
Q: Can the QT4-15A be upgraded with automatic stacking and cubing later?
A: The automation level is designed to be selectable and expandable. If you start with manual pallet handling and stacking, the PLC platform supports adding automatic stacking and cubing modules as your output volume grows. The upgrade path is discussed during initial configuration so the base machine wiring and pallet conveyor are prepared for future additions.