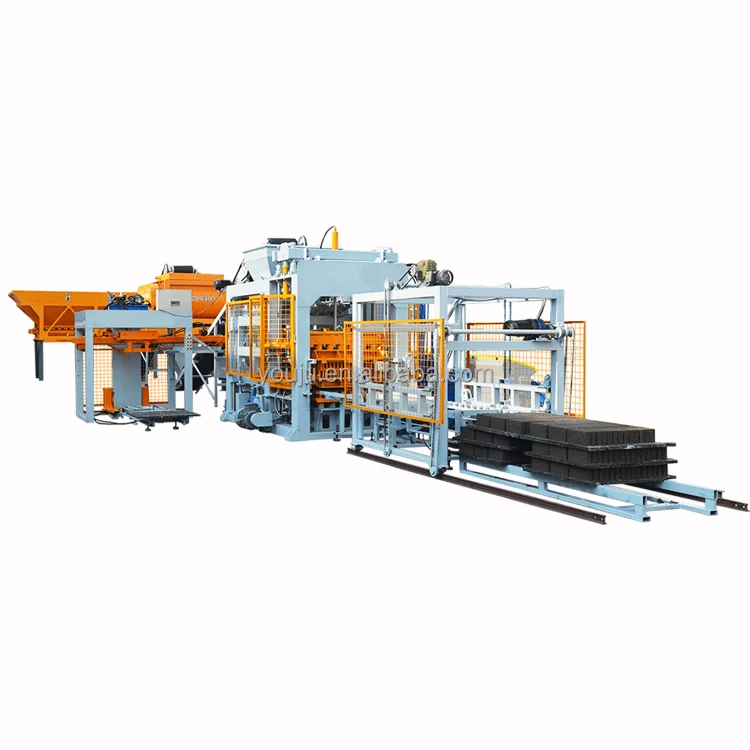

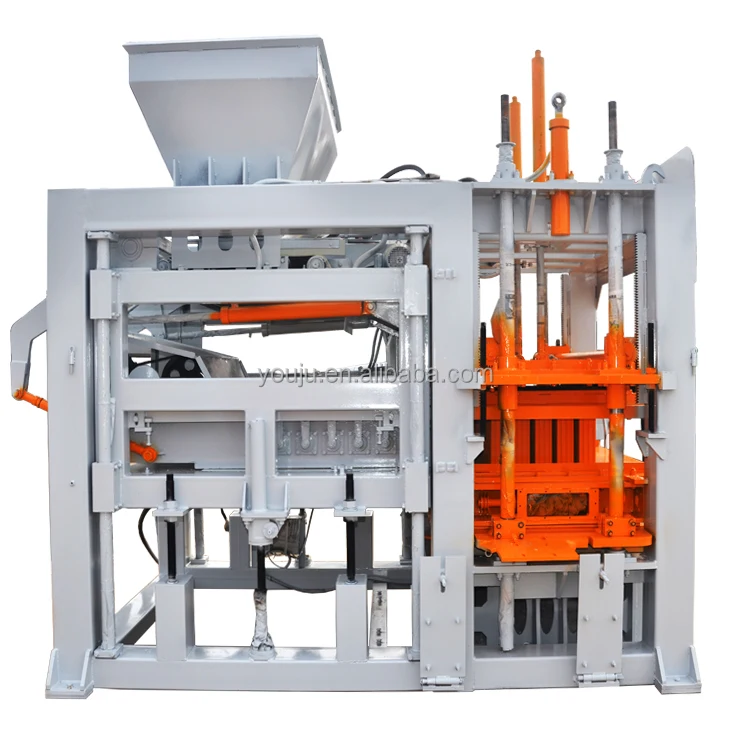
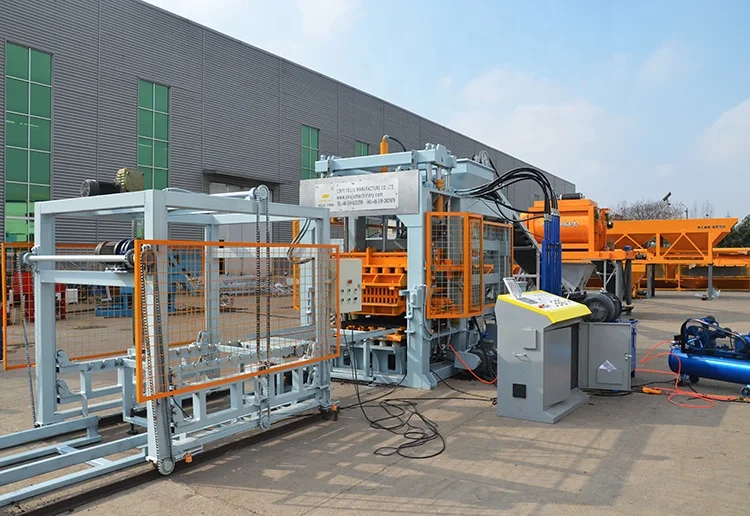

Description
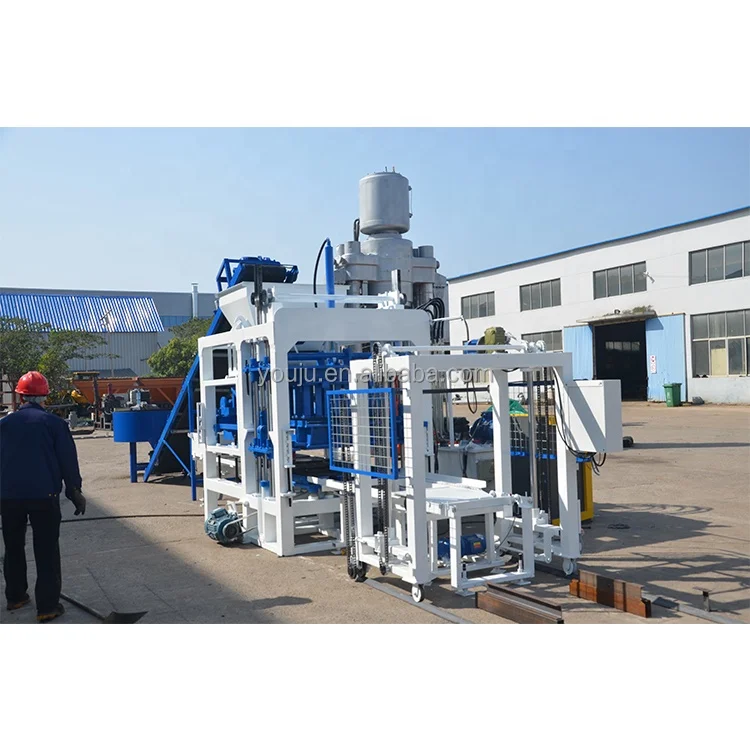
Matched PLC Configuration — Every QT 8-15 automatic block making machine PLC controlled system is verified for voltage, frequency, and operator language before production begins, preventing commissioning stalls that arise when assumptions replace confirmation.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT 8-15 |
| Product Type | Fully Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 8300 x 1860 x 3000 mm |
| Rated Power | 37 kW |
| Control System | PLC (Programmable Controller) with touch screen interface |
| Vibration Form | Platform Vibration |
| Vibration Frequency | 2800–4500 RPM |
| Pallet Size | 950 x 900 mm |
| Molding Cycle | 15–25 s (basis not stated in source — confirm block format / material / thickness); with color feeding 20–25 s |
| Brick Height Range | 50–200 mm |
| Output Capacity | 1912 pcs/h (based on 400×200×200 mm hollow block, 8 pcs/mold); 2875 pcs/h (based on 400×150×200 mm, 12 pcs/mold); 4320 pcs/h (based on 240×115×90 mm, 18 pcs/mold); 9360 pcs/h (based on 240×115×53 mm, 39 pcs/mold); 3000 pcs/h (based on 225×112.5×60 mm, 18 pcs/mold); 4625 pcs/h (based on 200×100×60 mm, 28 pcs/mold) |
| Daily Output (8 hours) | 15,300 pcs (400×200×200 mm); 23,000 pcs (400×150×200 mm); 34,560 pcs (240×115×90 mm); 74,880 pcs (240×115×53 mm); 24,000 pcs (225×112.5×60 mm); 37,000 pcs (200×100×60 mm) |
| Block Compressive Strength | up to 15 MPa (source value — verify against manufacturer catalog) |
| Raw Materials | Fly ash, slag, gangue, industrial waste, river sand, gravel, cement |
| Color Capability | Optional color feeding machine for colored paving blocks |
| Hydraulic System | Independent integrated hydraulic station, isolated from dust and main machine vibration |
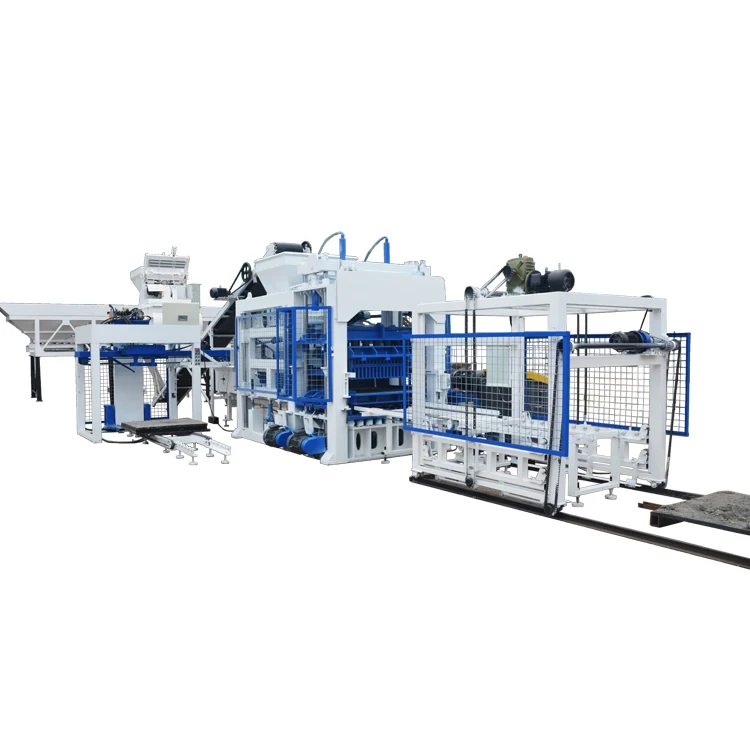
| Line Equipment (simple configuration) | Cement silo, host block machine, mixer, batching machine, stacker, forklift |
| Key Features | Fully automatic with PLC control, intelligent electronic control, touch screen HMI, pallet feed machine, storage hopper, conveyor |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow Block Production | 400×200×200 mm or 400×150×200 mm hollow blocks using crushed stone, river sand, and cement |
| Paving Block Manufacturing | 225×112.5×60 mm or 200×100×60 mm interlocking pavers from fine aggregates with optional color feeding |
| Porous Block and Kerbstone | Standard and kerbstone formats using fly ash, slag, or gangue blended with cement |
| Slope and Landscape Blocks | Grass blocks, slope-protecting blocks, and ring-tree blocks using gravel and cement mixes |
| High-Volume Solid Block | 240×115×90 mm or 240×115×53 mm solid bricks for large-scale masonry supply |
Why the Control Language Question Stops Production Before It Starts
When an automatic block making machine PLC controlled unit arrives with the touch screen displaying a language the local operators cannot read, the entire commissioning process freezes. The PLC interface must be confirmed in the buyer’s required language before production, not after delivery.
I once sourced a mid-size press for a factory in the Middle East. The machine arrived with every menu and alarm in English, while the floor crew only read Arabic. The supplier had never asked. [NEED_CITE: language configuration requirements for PLC in export markets] That plant sat idle while the control panel was reflashed and translated — weeks of lost output over a single unchecked box on the order form. This page exists to make sure the automation layer of the QT 8-15 is specified against your actual operating environment, not a catalogue default.
Removing the Operator from the Press Cycle
The QT 8-15 wraps its entire pressing sequence — pallet indexing, material feed, vibration, hydraulic pressure, and block ejection — inside a PLC with a touch screen HMI. Process data can be stored and recalled, so a shift change does not mean resetting parameters from memory. For a plant owner upgrading from manual or semi-automatic operation, this is the point where the automatic block making machine PLC controlled system stops depending on one experienced operator and starts running the same cycle every time.
Consistency Across Shifts and Formats
When you switch from hollow blocks to paving blocks, the vibration frequency, pressure dwell, and feed timing all shift. The PLC stores each format profile, so the change is a menu selection rather than a manual calibration. Batch-to-batch density stays within a narrow band because the control loop does not drift. [NEED_CITE: PLC stored recipe benefits in multi-format block production] The independent hydraulic station sits away from dust and press vibration, keeping valve response stable over long shifts.
Reading the Numbers That Matter
Platform vibration at 2800–4500 RPM means the frequency can be tuned to your specific mix design; a lighter fly ash blend needs a different resonance point than a dense crushed-stone mix. The 950 x 900 mm pallet size dictates both your curing rack spacing and the forklift tine width you already have on site — change it after delivery and you rebuild the curing area. Molding cycle figures of 15–25 seconds carry a format dependency: a thin solid brick completes faster than a 200 mm hollow block, so daily output must be read against the format column in the table above. The optional color feeding unit extends cycle to 20–25 seconds and requires its own hopper space in the line layout. Rated power at 37 kW determines the transformer capacity you must confirm before the machine ships.
The Commissioning Gap Nobody Budgets For
Arriving with the wrong voltage or frequency means the main motor either burns out or runs at reduced torque. I have seen plants delay opening by a month while waiting for a step-down transformer to clear customs. [NEED_CITE: voltage and frequency standards by export market] When the PLC display language does not match the crew, operator training becomes impossible and mistakes cascade into the hydraulic settings. These are not warranty issues — they are specification oversights that turn a fully automatic line into an expensive static asset.
Why Source the QT 8-15 Through This Channel
Block machinery is the single product focus here, so the QT 8-15 is specified as a matched system — press, mould, pallet, and handling — rather than assembled from unrelated suppliers. Automation level is selectable; a buyer can start with the base automatic configuration and add stacker or cubing later without replacing the press. Configuration is set against your actual mix design, local aggregate, and target block format instead of a catalogue default. [NEED_CITE: aggregate and mix design influence on block machine vibration settings] Mould design covers the formats your market actually sells, including custom drawings when standard formats do not match. Voltage, frequency, and PLC display language are confirmed in writing before production begins.
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed for each output figure
- Machine specification sheet with PLC language, voltage, and frequency confirmed
- Mould drawing and format list for every mould included in the order
- Hydraulic and electrical schematic matching the as-built configuration
- Factory test record on your target block format before dispatch
- Operation and maintenance manual in the confirmed PLC display language
Installation, Commissioning & Support
- Foundation plan sized to the 8300 x 1860 x 3000 mm footprint and dynamic vibration load
- Dedicated power circuit rated for the 37 kW motor with confirmed voltage and frequency
- Machine shipped dismantled per container loading plan with reassembly sequence documented
- PLC parameters set on-site against your confirmed block format and mix design
- Operator training conducted in the confirmed touch screen language
- Wear parts and mould list provided with clear replacement intervals
What to Include in Your Inquiry
To configure the QT 8-15 correctly, provide your target block formats, daily volume requirement, and the raw materials available locally. State the voltage and frequency at your plant, the language your operators read, and the pallet size your existing curing racks and forklifts can accommodate. If you already have a mixer, batching plant, or stacker on site, list those so the line layout accounts for them.
Frequently Asked Questions
Q: How is the output capacity verified, and which block format does each figure assume?
A: Every capacity figure for the QT 8-15 is listed alongside the specific block dimension and mould cavity count that produced it. A 400×200×200 mm hollow block yields a different hourly rate than a 200×100×60 mm paver because the cycle time, pallet coverage, and material volume per press all change. Always compare the output line that matches your target format.
Q: What PLC language options and voltage configurations are available for my target market?
A: The touch screen HMI can be set to the operator language you specify before production. Voltage and frequency are confirmed to match your local grid standard. Both parameters are locked in writing at the order stage so the machine arrives ready for immediate commissioning without transformer or software delays.
Q: How does the automation level compare to semi-automatic — what tasks are removed from the operator?
A: The QT 8-15 automates pallet indexing, material feeding, vibration timing, hydraulic pressing, and block ejection through the PLC. The operator monitors the touch screen and intervenes only for format changes or fault alarms. Manual pallet handling and manual feed timing are eliminated, reducing shift-to-shift variation in block density.
Q: What is the mould change procedure and how long does a format switch take?
A: Mould change on the QT 8-15 involves releasing the clamping bolts, lifting the current mould with an overhead crane, and lowering the new mould into position before re-securing and loading the corresponding PLC recipe. The exact time depends on crane availability and operator familiarity. Confirm the procedure during commissioning training.
Q: How does the machine’s vibration and hydraulic pressure match my local aggregate and mix design?
A: Platform vibration is adjustable between 2800 and 4500 RPM, and hydraulic pressure is set during commissioning based on your specific mix. A fly ash blend requires a different vibration profile than a crushed-stone mix to achieve target compressive strength. Provide your material test data so the configuration is matched before the machine ships.