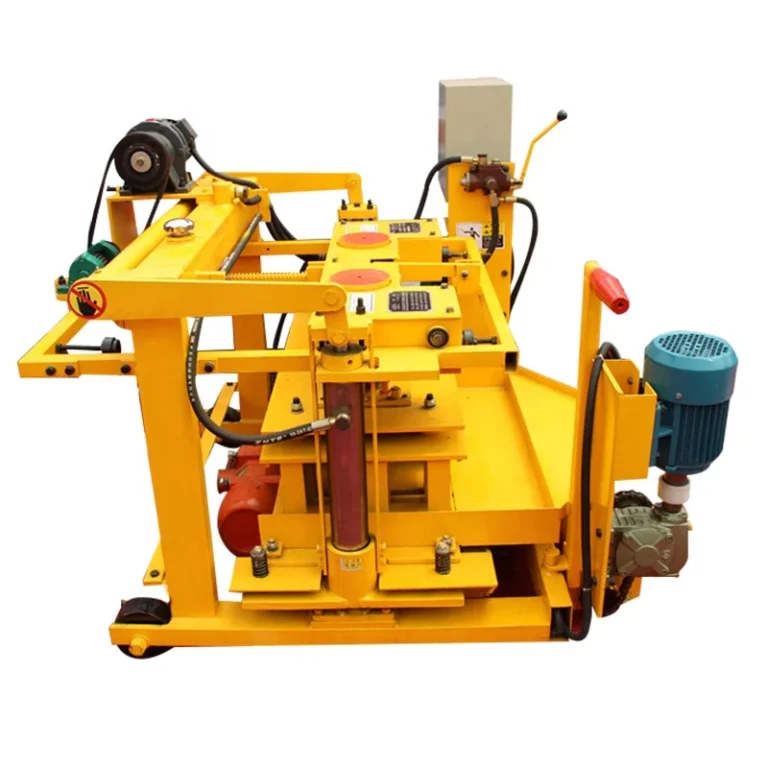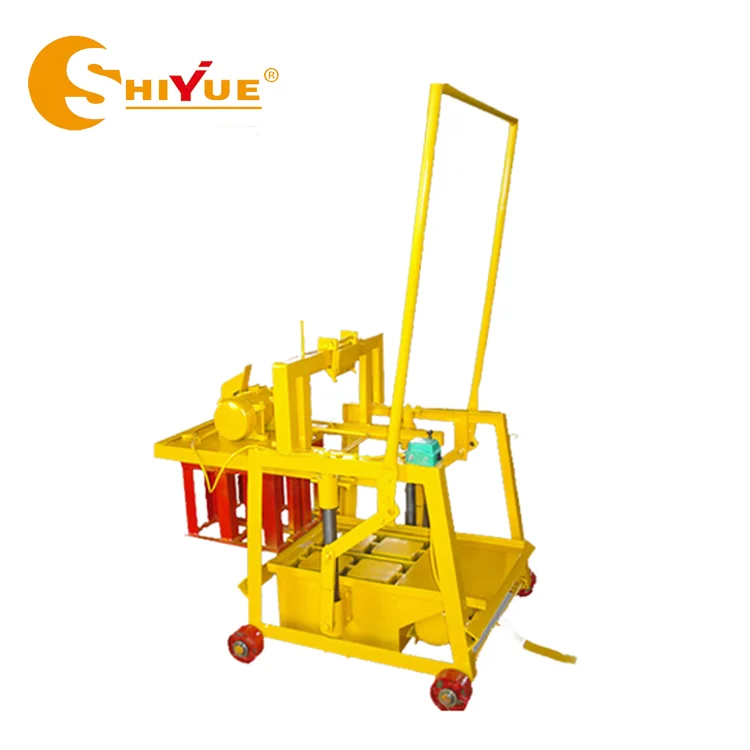
Description
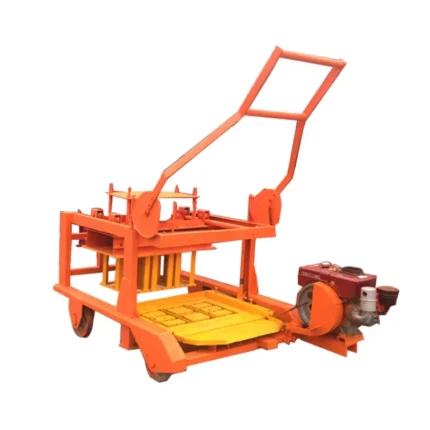
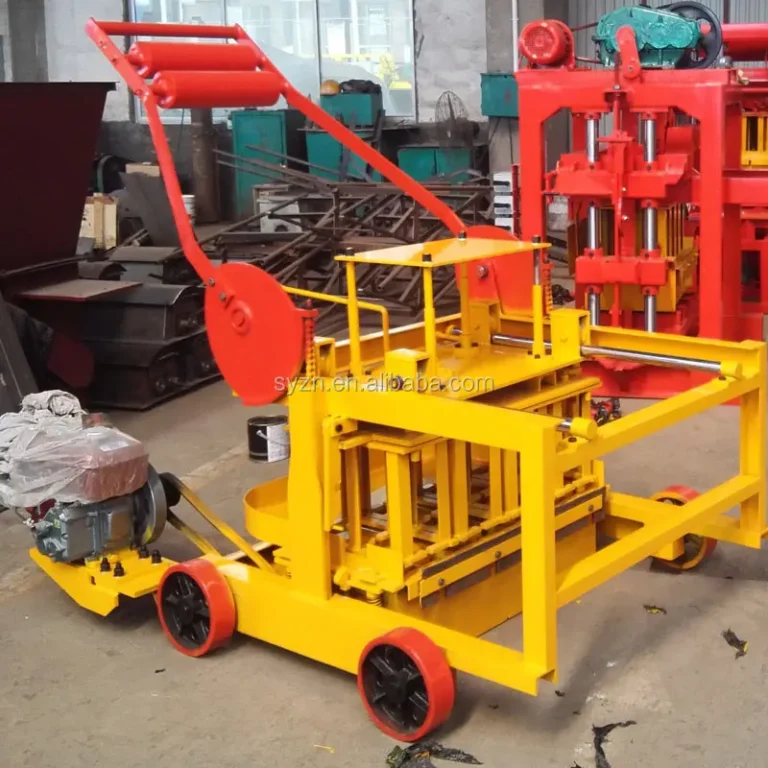
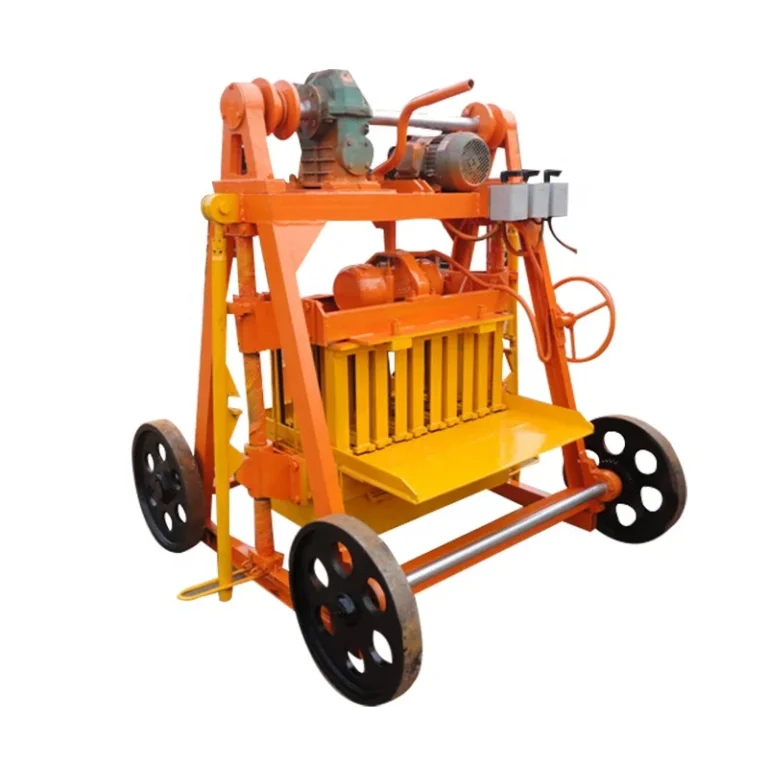
Upgrade-Ready Manual Block Press — the QMJ2-45 ships as a pallet-free egg-laying machine and connects directly into a future semi-automatic or PLC-controlled line without replacing the core press.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QMJ2-45 |
| Product Type | Mobile Mini Portable Cement Block Making Machine |
| Operation Mode | Manual, egg-laying type (pallet-free) |
| Mould Format: 400×200×200mm | 2 pcs/mould, 25-30s cycle, 160 pcs/hour, 1280 pcs/8hr |
| Mould Format: 400×150×200mm | 3 pcs/mould, 25-30s cycle, 240 pcs/hour (basis not stated in source) |
| Mould Format: 400×100×200mm | 4 pcs/mould, 25-30s cycle, 320 pcs/hour, 2560 pcs/8hr |
| Mould Change | Interchangeable moulds for listed hollow brick formats |
| Labor Requirement | 1 to 3 workers |
| Mobility | Free-moving on flat ground, no fixed plant required |
| Pallet Requirement | None |
| Automation Level | Manual (upgrade path to semi-automatic or automatic available) |
| Control System | Manual operation |
| Voltage & Frequency | Configurable to target market (to be confirmed at order) |
| Power Source | Electric motor (rated power to be confirmed at order) |
Application Suitability
| Application | Material or Output |
|---|---|
| On-site hollow block production | Cement, sand, crushed stone or local aggregate mixes |
| Small-scale block plants in limited space | Hollow bricks produced directly on ground without pallets |
| Housing project contractors | 400×200, 400×150, 400×100mm hollow formats on building sites |
| First plant entrepreneurs | Low-volume start with upgrade path to higher automation |
What "Cycles Per Hour" Leaves Out About Mobile Block Output
The QMJ2-45 cycle time of 25-30 seconds holds only when the mix design and aggregate match the mould geometry — and that is rarely the case on arrival.
I spent weeks in West Africa watching contractors run mobile block machines on local red laterite blended with whatever sand was available at the site. The cycle time printed on the nameplate assumed a standard graded aggregate that simply did not exist within two hundred kilometers of the project. The vibration parameters had to be reworked from scratch, and the first week of output fell well below the rated figure. This is the gap that causes most disputes between buyer and supplier after the machine lands on site [NEED_CITE: mix design and local aggregate variability in block production].
From Manual Egg-Laying to PLC-Controlled Operation
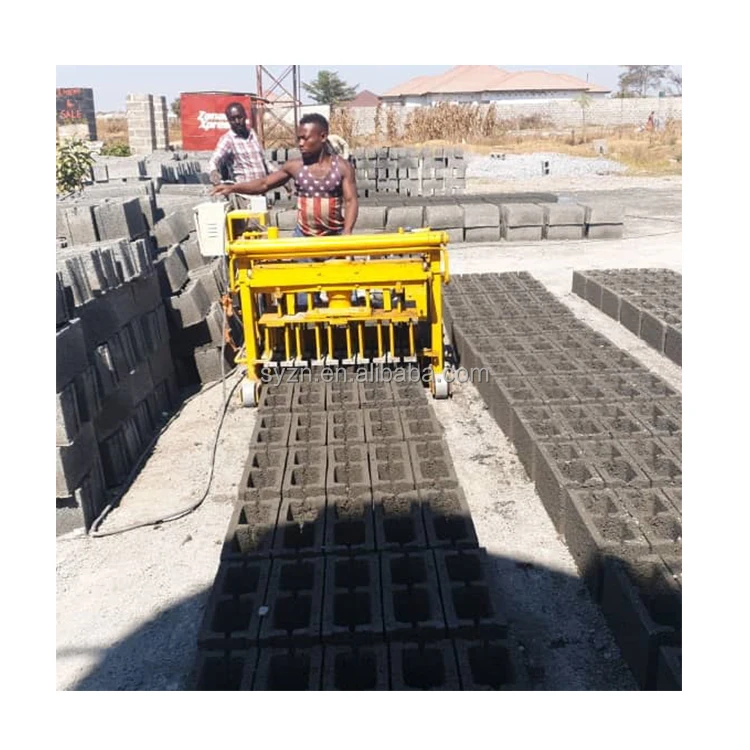
The QMJ2-45 starts as a manually operated, pallet-free press. Blocks are laid directly on the ground and cured in place, which removes pallet cost and pallet handling labor from day one. When production volume grows, the same machine platform can be integrated into a semi-automatic line with powered material feeding and later into a fully automatic mobile block machine configuration with PLC control, automatic stacking, and cubing.
The Automation Upgrade Path Defined Step by Step
Moving from manual to semi-automatic operation typically adds a mixer with controlled feed and a pallet return system if the buyer later switches to stationary production. The next step introduces PLC-controlled batching for consistent mix proportioning and an automatic stacker that removes the need for manual block handling after curing. Each stage can be implemented independently, so a buyer does not have to commit to a full automatic line at the initial purchase [NEED_CITE: staged automation investment in concrete block plants].
Why Mould Cycle Time Matters More Than Headline Capacity
The QMJ2-45 moulds cycle in 25-30 seconds across all three hollow brick formats listed. However, the actual daily output depends on which format is being produced: a 400×200×200mm block yields 2 pieces per mould for a rated 1280 pieces per 8-hour shift, while a 400×100×200mm block yields 4 pieces per mould for 2560 pieces per 8-hour shift. Any capacity discussion must state the block format assumed, or the number is meaningless for production planning. The vibration force and the hydraulic pressure applied during each cycle must also match the buyer’s specific mix — a drier mix with coarser aggregate will need different settings than a wetter, finer blend to achieve consistent block density.
What Happens When Automation Is Skipped Too Long
Buyers who stay on manual operation past the point where their volume justifies an upgrade face compounding problems. Block strength varies between shifts because manual batching cannot hold proportions within a tight band. Labour costs rise as more workers are added to move, stack, and cure output by hand. Mould changeovers take longer without assisted systems, eating into the format flexibility the interchangeable moulds were meant to provide. These issues accumulate quietly until a competitor with a PLC-controlled line begins delivering more consistent product at a lower unit cost [NEED_CITE: labor cost escalation in manual block production].
Why Source This Machine Through a Block-Line Specialist
Shiyue focuses exclusively on block making machinery, which means the QMJ2-45 is specified as part of a matched system — moulds, pallets (if the buyer later adds stationary production), and handling equipment are designed together rather than assembled from unrelated suppliers. The configuration is set against the buyer’s actual mix design and local aggregate, not pulled from a catalogue default. Mould design covers the hollow brick formats the buyer’s market actually sells, and custom mould drawings are available when standard formats do not match local demand. The automation upgrade path is documented at the point of sale so the buyer knows exactly which PLC, stacker, and cubing components can be added and when. Installation support includes operator training on both the manual baseline and the planned upgrade stages.
Documentation & Verification
- Line layout and capacity calculation stating the hollow block format assumed
- Machine specification sheet with confirmed voltage and frequency for target market
- Mould drawing and format list for all interchangeable hollow brick sizes
- Factory test record run on buyer-specified mix before dispatch
- Operation and maintenance manual with mould change procedures
Installation, Commissioning & Support
- Flat, compacted ground surface required; no fixed foundation or plant structure needed
- Electrical supply connection to be confirmed for local voltage and frequency before motor wiring
- Machine delivered assembled; mould mounting and initial cycle parameter setting on site
- Operator training covers manual mould change, mix loading sequence, and egg-laying technique
- Wear parts list and mould replacement schedule provided at commissioning
- Upgrade component compatibility verified during initial installation for future automation stages
Before You Request a Quotation
To size the QMJ2-45 correctly, we need the hollow block formats your market sells, the target daily output per format, and a description of the aggregate and cement available locally. Please also confirm your site voltage, frequency, and the control display language your operators require. If you plan to add automatic stacking or PLC batching later, let us know the timeline so the base machine can be configured to accept those modules without modification.
Frequently Asked Questions
Q: How is daily output verified for each hollow block format on the QMJ2-45?
A: Output is calculated per format using the 25-30 second cycle time and the number of cavities in each mould. The 400×200×200mm format yields 2 pieces per cycle for 1280 pieces per 8-hour shift. Verification assumes a mix design and aggregate gradation confirmed during factory testing. If local materials differ, cycle parameters are adjusted during commissioning and the output figure is recalculated accordingly.
Q: Can the QMJ2-45 be upgraded to semi-automatic or PLC-controlled operation later?
A: Yes. The machine platform supports staged upgrades starting with powered material feeding and controlled batching, then advancing to PLC control with automatic stacking and cubing. Each upgrade stage uses components designed to interface with the existing press without structural modification. The upgrade path is documented at initial purchase so buyers can plan investment and timing.
Q: What voltage, frequency, and control language options are available?
A: The electric motor and any control components are configured to the buyer’s confirmed site voltage and frequency before production. PLC display language is set to the operator’s preferred language when the automation upgrade is installed. Both electrical and language specifications are confirmed during the order process to avoid commissioning delays on arrival.
Q: How long does a mould change take, and what is required?
A: Mould change on the QMJ2-45 involves releasing the existing mould, lifting it clear, and seating the replacement format. The process requires basic hand tools and can be completed by trained operators within a single shift once familiarity is established. Mould change procedures are covered in the operation manual and during on-site operator training at commissioning.
Q: What automation components can be added, and at what production stage?
A: Initial additions include a powered mixer with controlled feed and a pallet system if stationary production is introduced. The next stage adds PLC-controlled batching for mix consistency, followed by an automatic stacker and cubing unit for finished block handling. Each component is matched to the press capacity so no station creates a bottleneck for the others.