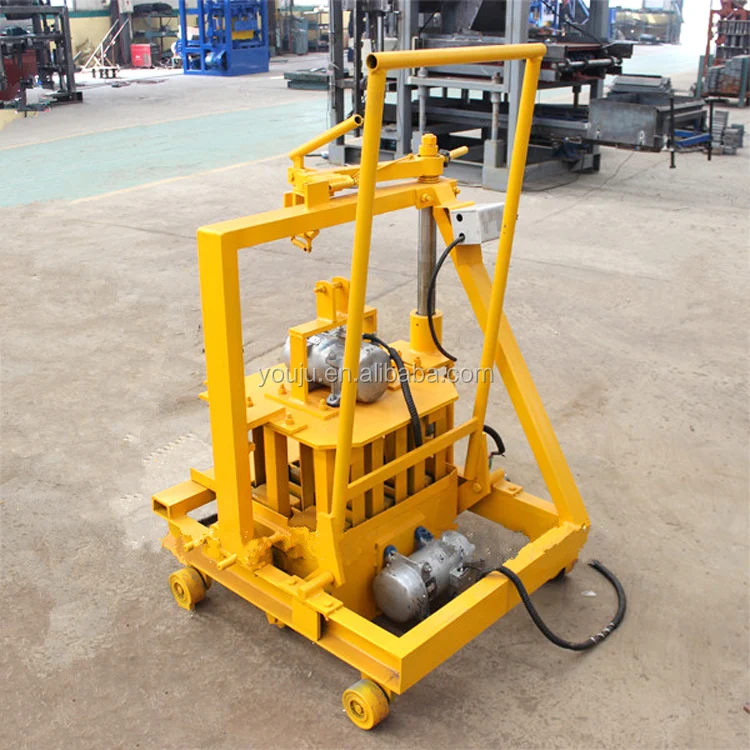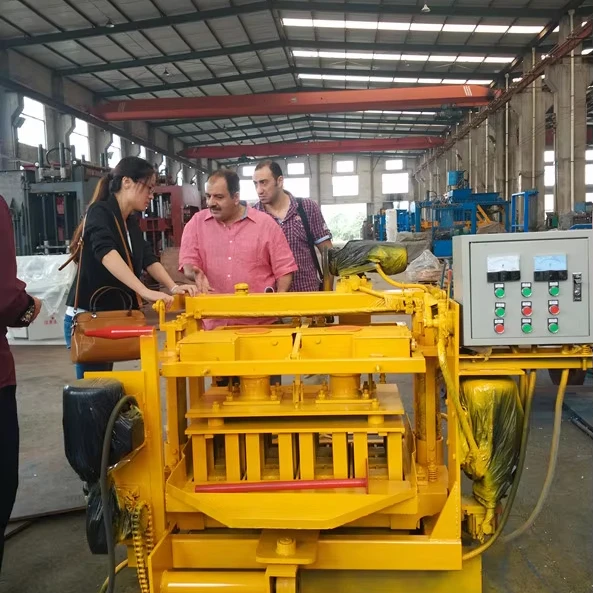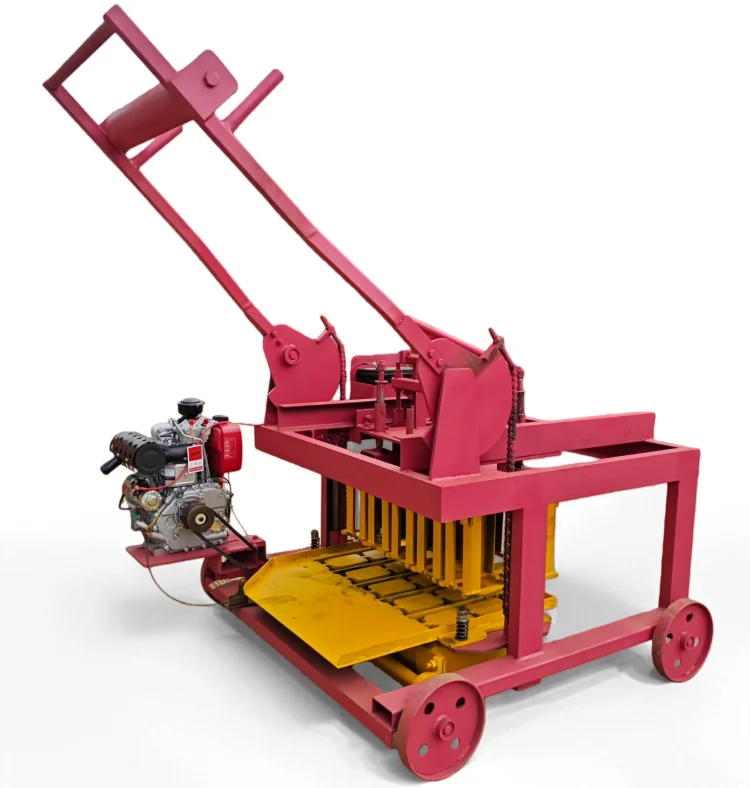
Description
Automation-first configuration — Every QMR4-45 mobile block machine ships with control logic matched to your site conditions, not a catalogue default.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QMR4-45 |
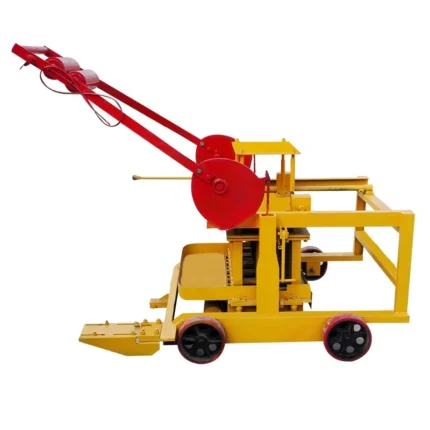
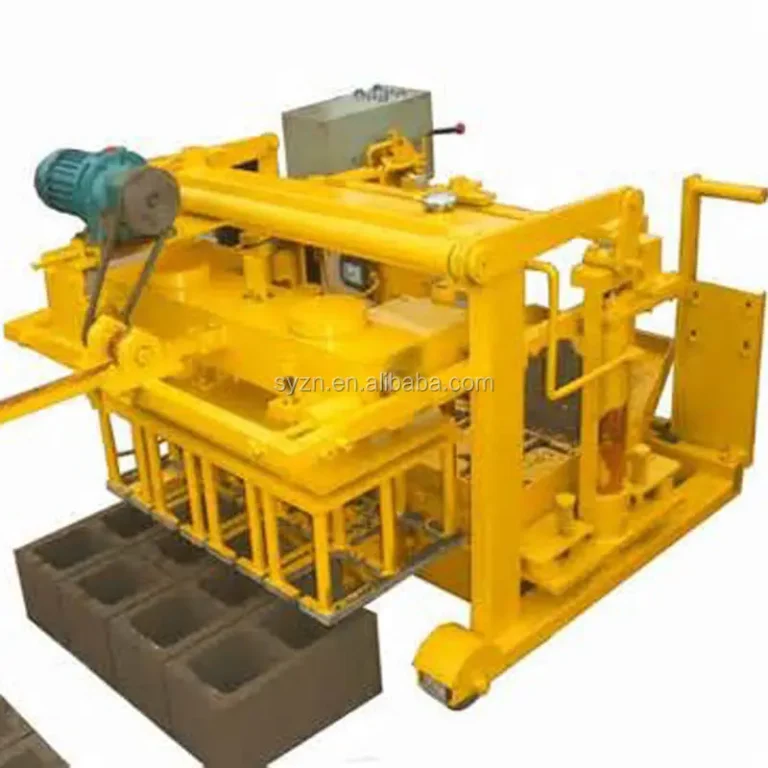
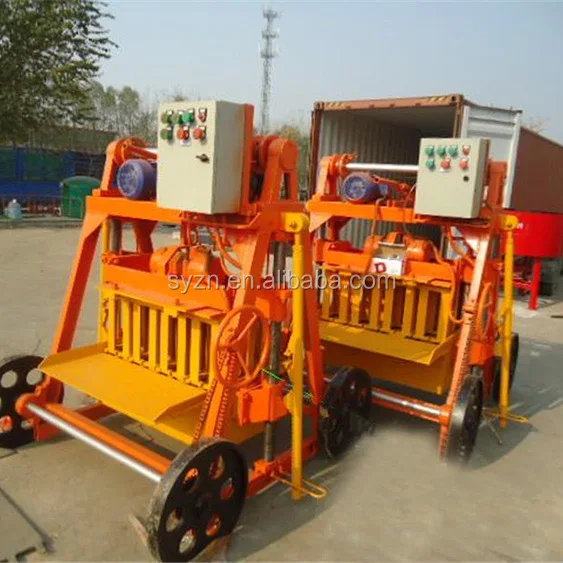
| Product Type | Mobile Diesel Block Making Machine |
| Molding Cycle | 45 s (basis not stated in source — confirm block format) |
| Power Source | Diesel engine |
| Rated Power | 8 hp |
| Molding Form | Vibration and pressure |
| Vibration Force | 60 kN |
| Total Weight | 800 kg |
| Overall Dimensions | 2420 × 1320 × 1650 mm |
| Automation Level | Manual operation with mechanical vibration; PLC control available as upgrade |
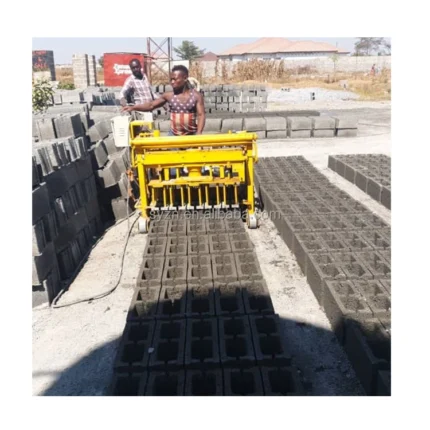
| Pallet Requirement | Pallet-free (egg-laying type) |
| Block Formats | Paver brick, hollow block, concrete block, solid brick, fly ash brick |
| Basic Equipment Included | JZC350 or JQ350 diesel concrete mixer, trolley |
| Voltage & Frequency | Configurable based on site (basis to be confirmed) |
| Control System | Mechanical vibration standard; PLC upgrade available (basis to be confirmed) |
| Output Capacity | Depends on block format and material (basis to be confirmed) |
Application Suitability
| Application | Material or Output |
|---|---|
| On-site housing project block production | Hollow and solid concrete blocks using locally sourced crushed stone and sand |
| Remote construction without grid electricity | Paver and kerbstone bricks from cement and aggregate mixes |
| Small-scale entrepreneur block plant | Fly ash bricks incorporating local industrial by-products |
| Supplementary mobile line for peak demand | Concrete blocks and pavers in parallel with a stationary plant |
| Rural infrastructure and community projects | Solid and interlocking bricks from available regional aggregates |
Why the Voltage Question Must Precede the Price on a Mobile Block Machine
Mismatched electrical supply is the most preventable cause of commissioning failure on site.
I once supported a QMR4-45 automatic mobile block machine installation where the generating unit arrived configured for a frequency the local grid does not use. The motor overheated within the first production run, and the crew spent weeks sourcing replacement windings while the site stood idle. This happens more often than buyers expect — and the fix always costs more than a ten-minute confirmation before shipment [NEED_CITE: voltage and frequency standards by export market]. When you evaluate a PLC controlled mobile brick machine, the control panel language, voltage rating, and phase specification must be locked to your actual site conditions, not assumed from a quotation template.
What Automation Actually Removes from the Operator
On a standard QMR4-45, the operator controls mixing ratios by eye, triggers vibration manually, and judges cycle completion from experience. That works for a skilled crew, but consistency drops when shifts change or when the local aggregate moisture content varies after rain. Adding PLC-controlled batching and cycle timing to this automatic mobile block machine removes those judgement calls from the workflow — the system meters material by weight and holds vibration duration constant regardless of who is running the shift.
Where Control Upgrades Matter Most for Egg-Laying Machines
Egg-laying machines produce blocks directly on the ground, which means each block cures in place without pallet support. Batch-to-batch consistency in mix moisture and compaction becomes critical because there is no pallet to absorb variation. A PLC controlled mobile brick machine with integrated moisture feedback adjusts water dosing per batch, keeping block density uniform across an entire production day. This is where automation pays for itself — not in speed, but in reducing the number of blocks that crack or crumble before they reach curing age [NEED_CITE: concrete block curing strength development factors].
How Vibration Force and Diesel Power Shape Block Density
The 60 kN vibration force on the QMR4-45 works together with mechanical pressure to compact the mix inside the mould cavity. On mobile machines, this compaction must happen quickly because the machine moves forward after each cycle. The 8 hp diesel engine drives both the vibration motor and the mixer, which means engine load fluctuates with every mould fill. If the engine is undersized for the actual mix stiffness, vibration amplitude drops and block walls come out less dense. Confirming your local aggregate gradation and cement ratio against the vibration force rating is essential before the machine leaves the factory. The 45-second molding cycle applies to a specific block format under controlled conditions — different formats and mix designs will shift this timing, and realistic daily output should be calculated against the exact block you intend to sell.
The Cost of Skipping Configuration Verification
When a mobile block machine arrives on site with a control language the crew cannot read, operators default to manual overrides — defeating the purpose of the automation investment. Commissioning delays compound: electricians rewire panels, new components ship internationally, and the project timeline slips by weeks [NEED_CITE: CE machinery directive requirements for industrial equipment]. On egg-laying machines specifically, running an unverified mix design against a fixed vibration setting produces blocks that pass visual inspection but fail compressive strength tests at 28 days. The rework cost of tearing out and replacing substandard blockwork far exceeds the time spent confirming parameters before production begins.
Why Buyers Source This Machine Through Our Configuration Process
Block machinery is our sole focus, so the QMR4-45 is specified as a matched system — machine, mixer, and trolley together rather than assembled from separate suppliers. We configure the diesel engine, vibration settings, and any control upgrades against your actual mix design and local aggregate, not a catalogue default. If you plan to start with manual operation and add PLC batching later, the electrical architecture supports that upgrade path without a full panel replacement. Mould options cover the formats your market actually buys, and custom mould drawings are available when standard formats do not match local building codes. Every machine undergoes a factory test on the target block format before crating, so you see cycle behaviour and block output before the machine ships.
Documentation & Verification
- Factory test record on your specified block format before dispatch
- Machine specification sheet confirming diesel engine rating and vibration force
- Voltage, frequency, and control language confirmation document
- Mould drawing and block format list matched to your market
- Operation and maintenance manual in your preferred language
- Packing photographs and customs documentation support
Installation, Commissioning & Support
- Ground surface must be level and firm to support the 800 kg machine during egg-laying operation
- Diesel fuel supply and spare filter schedule confirmed before first production run
- Mixer and trolley arrive assembled; machine requires only mould installation on site
- Vibration force calibrated against your local aggregate during commissioning
- Operator training covers mould change procedure and daily maintenance checkpoints
- Wear parts list with reorder codes provided at handover
What We Need to Configure Your QMR4-45 Correctly
Before we finalise a quotation, we need to know the exact block formats your market requires, the daily output you are targeting per format, and the aggregate materials available within economical transport distance of your site. Please also confirm your local voltage and frequency if you are considering an electric-start or PLC control upgrade, along with your preferred control panel display language.
Frequently Asked Questions
Q: What automation upgrades are available for the QMR4-45 — can PLC control be added later?
A: The standard QMR4-45 runs with mechanical vibration and manual batching. PLC-controlled batching, cycle timing, and automatic water dosing can be specified at order or retrofitted later because the electrical architecture is designed to accommodate control upgrades without replacing the main panel. We confirm the upgrade path during initial configuration so future additions remain compatible.
Q: How does the 45-second molding cycle translate to realistic daily output?
A: The 45-second cycle applies to one specific block format under controlled conditions. Hollow blocks, solid bricks, and pavers each have different compaction requirements, so actual cycle time varies by format. We provide a capacity calculation that states the assumed block dimensions and mix design so you can plan daily output against your real product mix, not a single headline number.
Q: What voltage and control language options are supported with an electric generating unit?
A: When the JQ350 electric generating unit replaces the standard diesel mixer, voltage and frequency must match your site supply. The PLC display language is confirmed before production. We document all electrical specifications in a pre-shipment confirmation to prevent commissioning delays caused by mismatched supply standards.
Q: How is vibration force calibrated to the buyer’s local aggregate?
A: The 60 kN vibration force is adjustable. During commissioning, we test the machine with your actual aggregate sample and cement ratio, then set the vibration duration and amplitude to achieve consistent block density. This calibration is recorded in the factory test documentation so settings can be restored after any maintenance.
Q: What is the upgrade path from this mobile machine to a stationary line?
A: The QMR4-45 serves as a production starting point or a supplementary unit. When volume demands exceed mobile capacity, buyers transition to a semi-automatic or fully automatic stationary line where pallet-based handling, automatic stacking, and higher output tiers are available. The mould formats and mix knowledge gained on the mobile machine carry forward into the stationary line specification.