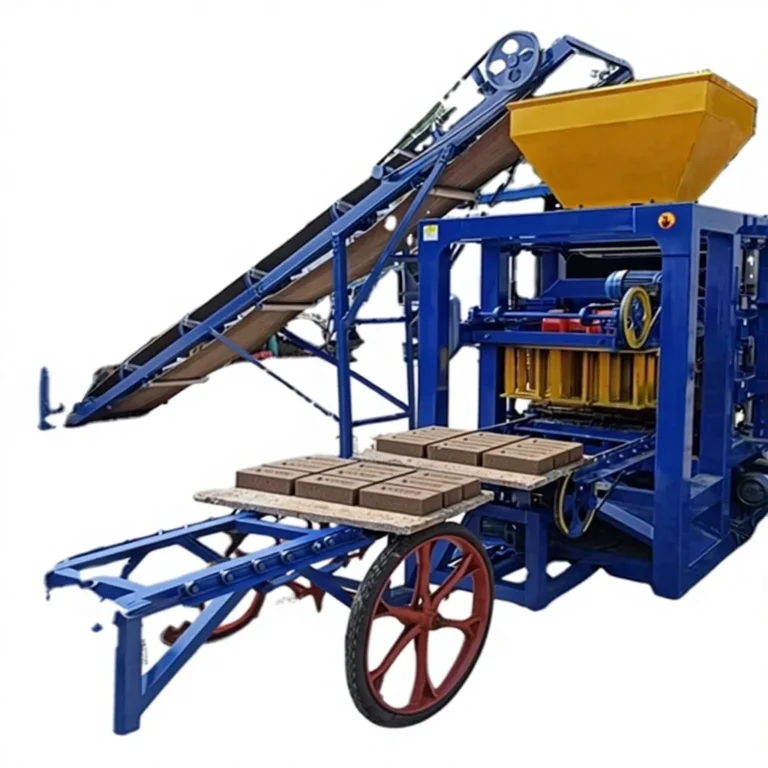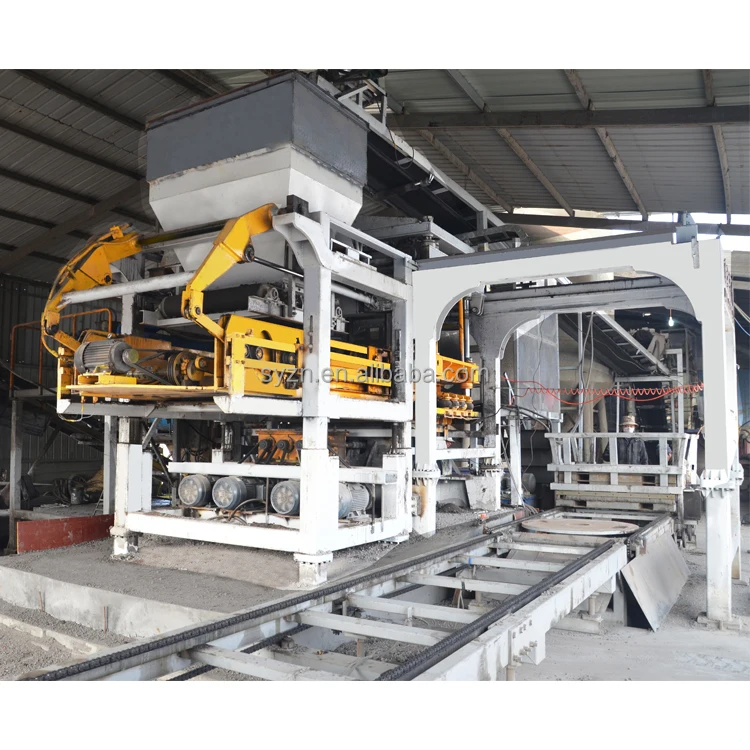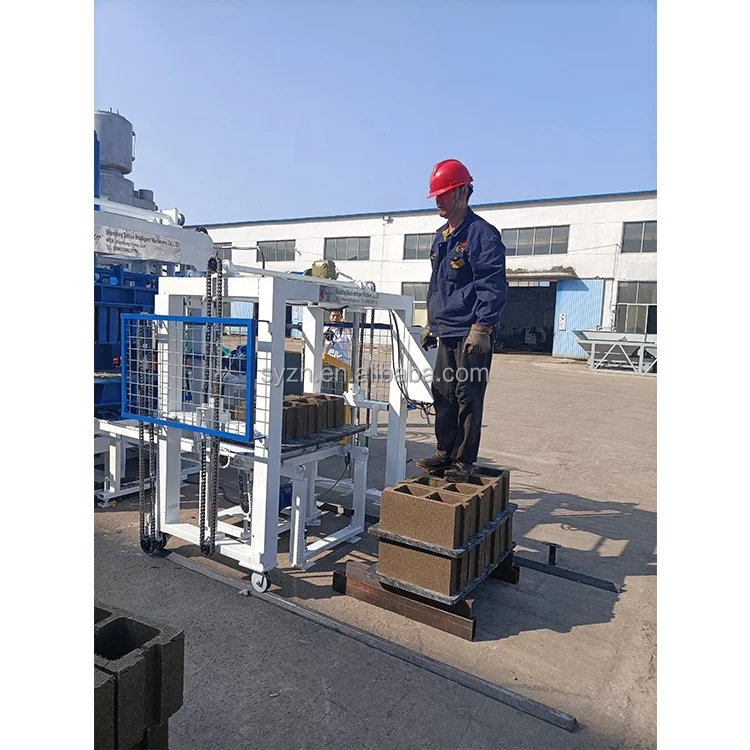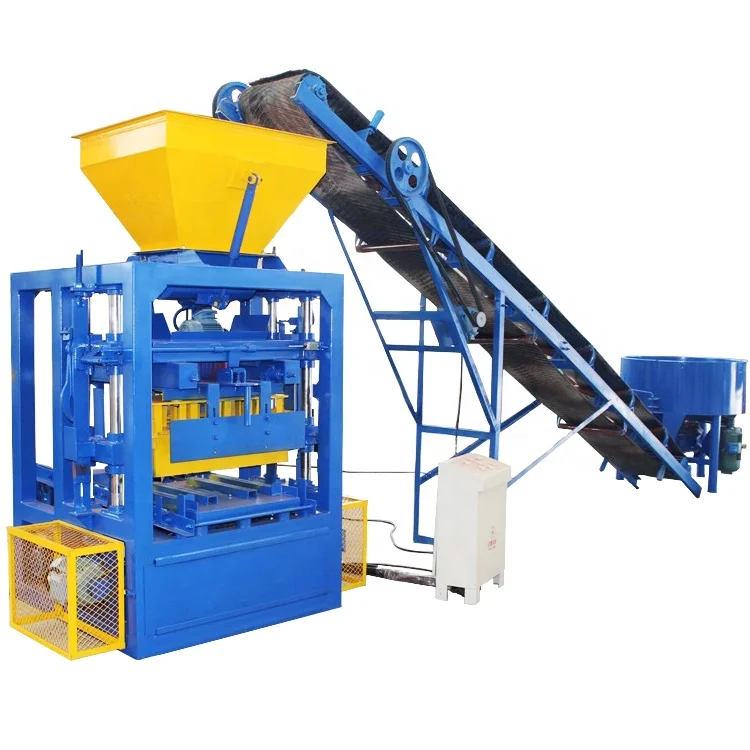
Description
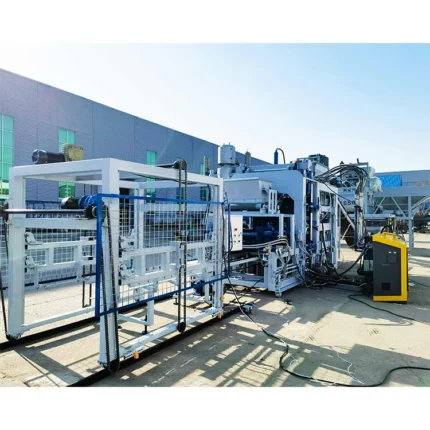
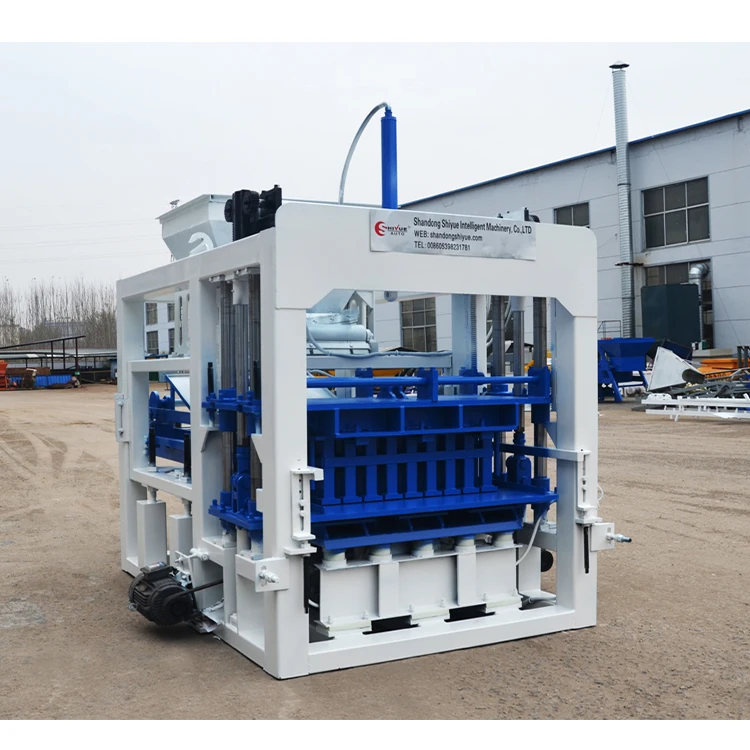
Automation That Grows With You — The QTJ4-24 starts as a semi-automatic press with manual pallet handling, but its control architecture supports field installation of PLC batching, auto stacking, and remote diagnostics when your output targets demand it.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-24 |
| Product Type | Semi-Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 3600mm × 1700mm × 2560mm (working state) |
| Total Mass | 1750 kgs |
| Molding Type | Platform Vibration |
| Pallet Size | 850mm × 450mm |
| Overall Power | 14.25 kW |
| Mould Format Options | 390×190×190mm (4 pcs/mold); 240×115×53mm (21 pcs/mold) |
| Vibration System | Lower platform (2 × 3 kW) + Upper (1.5 kW) |
| Elevating System | Cone-shape motor, JZQ250 speed reducer, V-belt drive |
| Delivery Device | Cycloidal pin wheel reducer, chain and V-belt drive |
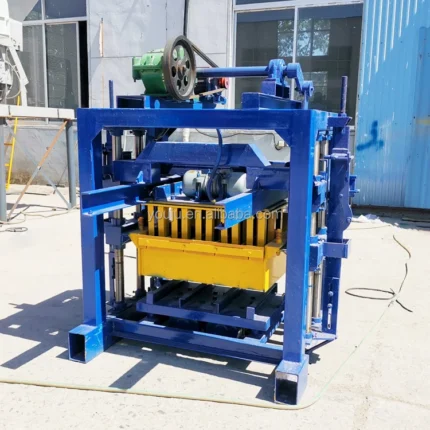
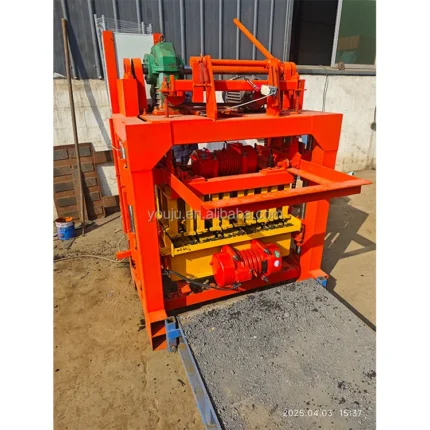
| Machine Frame | Dragon gate steel construction, four wear-resisting vertical shafts |
| Control System | Mechanical and electronic combination (PLC availability to be confirmed) |
| Automation Level | Semi-automatic (auto stacker optional) |
| Mixer (Included) | JQ350 pan mixer |
| Conveyor (Included) | 6m belt conveyor |
| Cycle Time | (basis to be confirmed — depends on block format and material) |
| Output Capacity | (basis to be confirmed — depends on block format and material) |
| Voltage & Frequency | Configurable to target market requirements |
| Hydraulic Pressure | Not applicable (mechanical vibration system) |
| Key Features | Trolley included, optional auto stacker (3–6 layers), semi-automatic baseline |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production | Crushed stone, cement, sand, and water for 390×190×190mm units |
| Solid brick production | Fine aggregate and cement mixes for 240×115×53mm bricks |
| Small-scale block plant startup | First-line production for entrepreneurs entering the block market |
| On-site construction block making | Contractor-produced hollow blocks using locally sourced aggregate |
| Format expansion for existing plants | Adding hollow or solid brick formats without full-line reinvestment |
Why Your PLC Display Language Matters Before Commissioning Day
A PLC controlled semi-automatic block machine only automates what the operator can read and navigate.
I spent years on assembly floors and commissioning sites across the Yangtze Delta region, and the single most frustrating failure mode I have witnessed is a machine arriving overseas with its touch screen locked in a language the local crew cannot parse. The hardware runs fine. The automation logic executes perfectly. But the operator stares at a panel of unfamiliar characters and cannot acknowledge an alarm, adjust a cycle timer, or initiate a mould change sequence. One shipment I supported sat idle for an entire week while I flew out to reconfigure the HMI language and retrain the team from scratch [NEED_CITE: control interface language requirements for export machinery]. That delay cost the buyer production time they had already committed to a construction schedule. Voltage mismatches produce similar outcomes — a 440V motor on a 380V supply burns out within shifts, and a 50Hz machine running on 60Hz mains vibrates at unintended frequencies, throwing block density off specification.
Building Automation in Stages, Not All at Once
The QTJ4-24 ships as a semi-automatic press, which means pallet feeding and block removal start as manual operations. Buyers who are transitioning from egg-laying machines or fully manual setups can learn the press rhythm without managing a full PLC controlled semi-automatic block machine from day one. The optional auto stacker handles 3 to 6 layers depending on block height, reducing the labour required at the output end while the crew builds confidence with the vibration and cycle parameters.
The Upgrade Path from Relay Logic to Intelligent Control
When daily volumes grow or consistency demands tighten, the machine accepts field-installed upgrades to PLC-controlled batching, automatic pallet feeding, and remote diagnostics. The dragon gate frame and four vertical guide shafts remain constant — only the control layer and material handling stations change. This means a buyer’s initial capital outlay is not stranded when production scales up. The JQ350 pan mixer and 6m belt conveyor can similarly be integrated into an automatic block machine upgrade with PLC-governed dosing, replacing manual batch measurement with programmable recipes tied to specific block formats [NEED_CITE: PLC batching integration for stationary block presses].
How Vibration Force, Frame Rigidity, and Pallet Size Shape Block Quality
Platform vibration on the QTJ4-24 comes from two 3 kW lower motors and a 1.5 kW upper device, which together consolidate the concrete mix into the mould cavity. The lower motors compact from below while the upper unit settles the surface — this dual action is what determines whether a hollow block emerges with uniform wall density or shows weak zones that crack during curing. The dragon gate steel frame with four wear-resisting vertical shafts resists deflection under vibration load, so the mould stays square across thousands of cycles. Pallet size at 850mm × 450mm dictates the curing rack dimensions and the forklift tine spacing the buyer must have ready before the machine arrives. If the buyer’s existing curing yard uses a different pallet standard, every pallet becomes a manual handling problem rather than a mechanized flow. Total connected power at 14.25 kW means the buyer must verify the site electrical supply can sustain continuous draw, not just peak start-up current.
The Hidden Cost of Skipping Configuration Confirmation
When a buyer accepts a quotation without specifying which block format the cycle time assumes, the machine arrives and produces far fewer blocks per shift than the pro-forma invoice implied. The mismatch is not a defect — it is an unasked question. Similarly, when mould changeover procedure is not documented with the specific tooling and sequence for this press, a format swap that should take thirty minutes stretches into most of a shift, cancelling the flexibility the buyer paid for [NEED_CITE: mould changeover time benchmarks for semi-automatic block machines]. Voltage and frequency left unconfirmed can delay commissioning by days or damage motors before the first production run completes.
Why Buyers Source This Machine Through Our Configuration Process
Every QTJ4-24 proposal begins with the buyer’s target block format, local aggregate, and site electrical conditions — not a catalogue default. Machine, mould, pallet, and handling equipment are specified as one matched system, so the mixer output rate aligns with the press cycle time and the pallet dimensions match the curing area the buyer already operates. Mould design covers the formats the buyer’s local market actually sells, with custom drawings available for non-standard brick dimensions. Automation level is selectable at order and upgradable in the field, so a buyer starting semi-automatic can add PLC batching and stacking as demand justifies the investment. Factory testing runs the specific block format and mix design the buyer will produce, generating a verified cycle time and output figure before the machine ships.
Documentation & Verification
- Line layout and capacity calculation stating the exact block format assumed for each output figure
- Mould drawing and format list covering both 390×190×190 hollow and 240×115×53 solid configurations
- Voltage, frequency, and control display language confirmation sheet signed before production begins
- Factory test record showing vibration force and cycle time measured against your specified mix design
- Hydraulic and electrical schematic with part-numbered wear parts and mould replacement list
Installation, Commissioning & Support
- Foundation pad must be level and rated for the 1750 kg operating mass plus dynamic vibration load
- Electrical supply confirmed for 14.25 kW continuous draw with dedicated circuit breaker and correct voltage
- Machine ships in working-state dimensions (3600×1700×2560mm); on-site assembly covers conveyor and mixer positioning
- First commissioning run verifies cycle time against the buyer’s block format and adjusts vibration duration accordingly
- Operator training covers mould change sequence for both hollow and solid formats using included tooling
- Wear parts list with part numbers supplied so replacement shafts and vibration motor mounts are orderable immediately
What to Include in Your Inquiry
Send us your target block format and dimensions, the daily output you need to meet contract obligations, and the aggregate materials available at your site. We also need your local voltage and frequency standard, preferred control panel language, and whether your existing curing yard uses standard or custom pallet sizes so we can match the 850×450mm pallet specification to your handling equipment.
Frequently Asked Questions
Q: How is the realistic daily output calculated per block format, and what cycle time does each format require?
A: Output depends on whether you are running the 390×190×190mm hollow mould (4 pieces per cycle) or the 240×115×53mm solid mould (21 pieces per cycle). Cycle time varies with mix design, material moisture, and compaction requirements. We provide a format-by-format capacity sheet with your quotation, stating the exact block type each figure assumes so there are no surprises at commissioning.
Q: Can the QTJ4-24 be upgraded to full PLC control with automatic pallet feeding and stacking after initial installation?
A: Yes. The machine frame, vibration system, and guide shafts remain unchanged. The control layer accepts field-installed PLC modules for batching accuracy, automatic pallet feeding, and stacking. This automatic block machine upgrade path lets you start semi-automatic and add intelligent control stations as your production volume and consistency requirements grow.
Q: What voltage, frequency, and PLC display language options are available for my target market?
A: Voltage and frequency are configured to your site supply before production begins. The PLC controlled semi-automatic block machine interface language is confirmed in writing during the order process — we have seen machines delayed by a full week because the touch screen shipped in a language the operator could not read. Both details go on a signed confirmation sheet.
Q: How do I match the vibration force to my local aggregate and mix design for consistent block strength?
A: The dual 3 kW lower motors and 1.5 kW upper vibration unit produce a fixed vibration profile. We match this to your specific aggregate gradation and cement ratio during factory testing, adjusting cycle parameters to achieve consistent compaction. The factory test record documents the settings that produced acceptable block strength with your submitted mix sample.
Q: What automation add-ons are available and how do they change labour requirements?
A: The optional auto stacker handles 3 to 6 layers depending on block height, removing the need for manual stacking at the press output. Upstream, PLC-controlled batching replaces manual material measurement. These additions reduce the crew size at the press station and shift the operator’s role from manual handling to monitoring and quality checks on the PLC controlled semi-automatic block machine output.