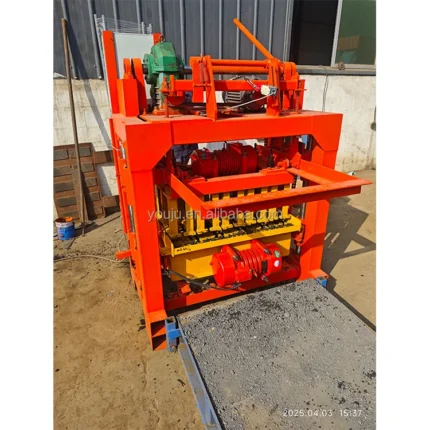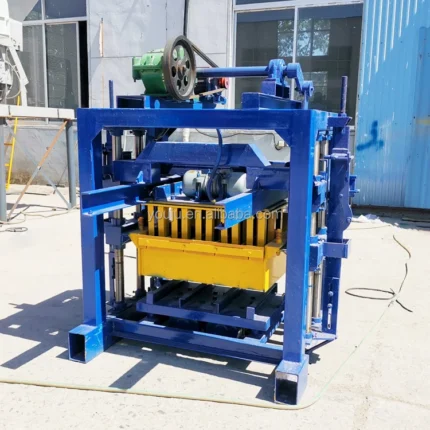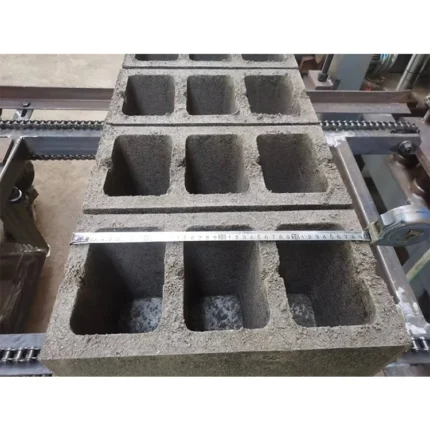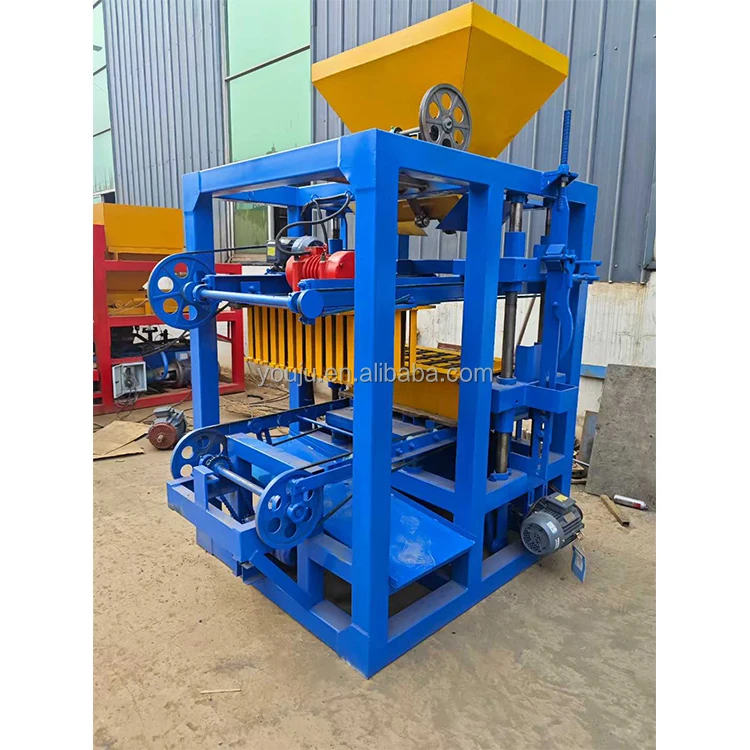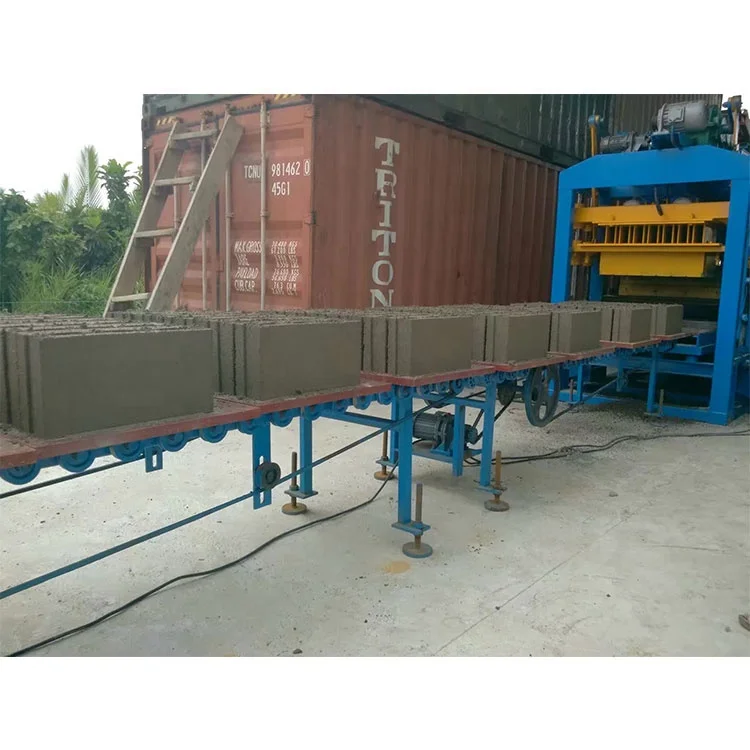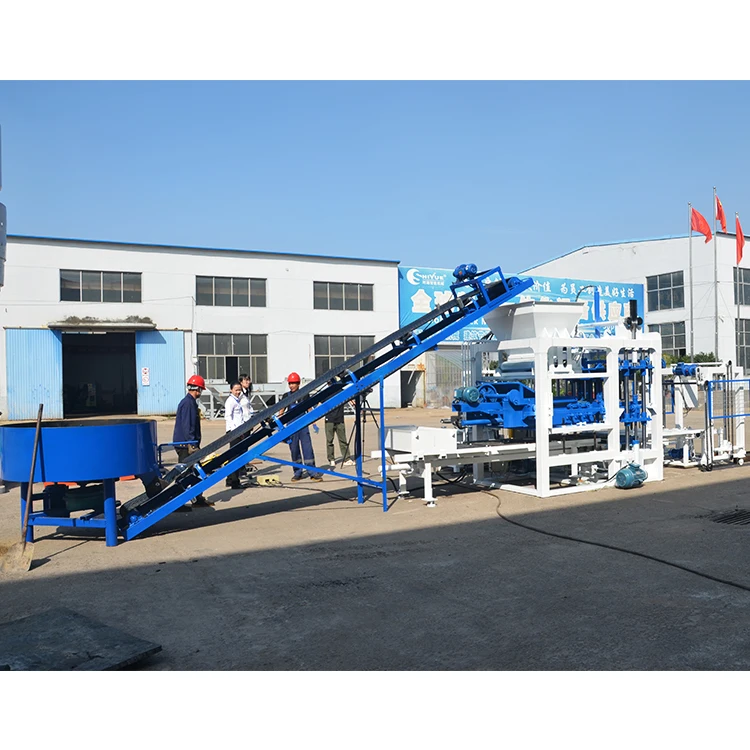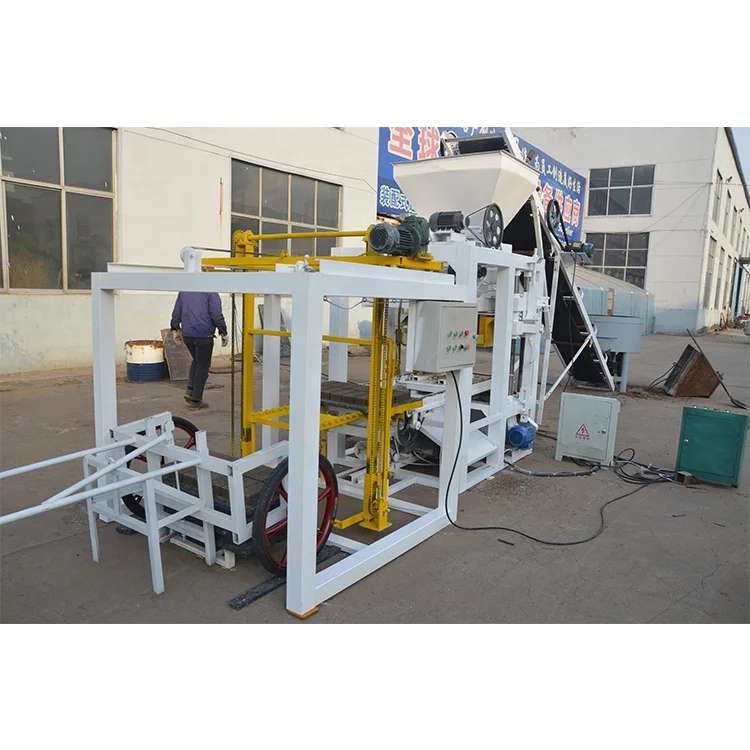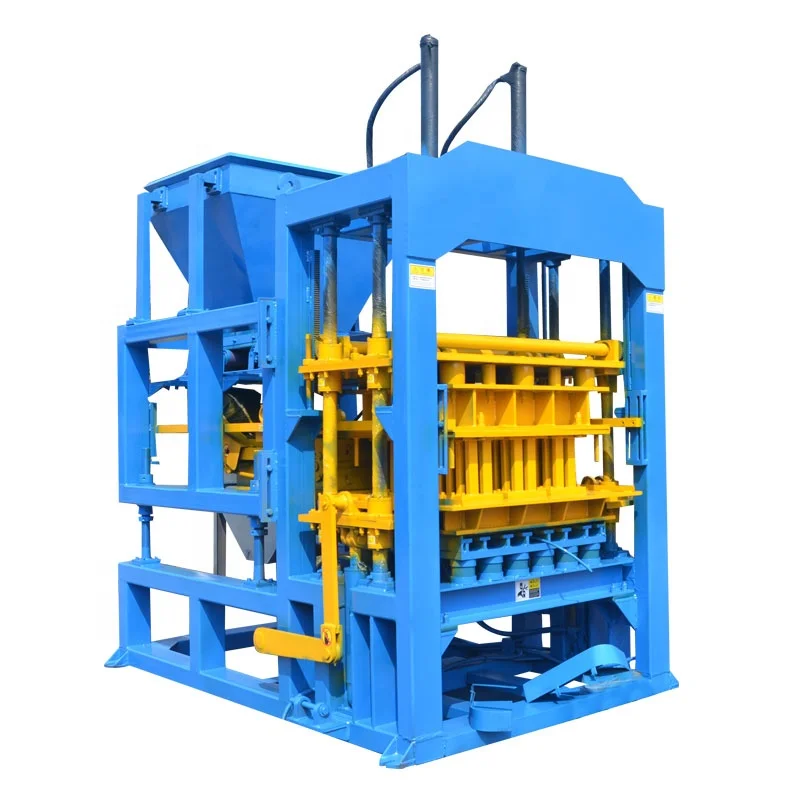
Description
Intelligent fault diagnosis — every PLC alarm on the QT5-15 points the operator directly to the faulty sensor or valve, cutting shift-ending guesswork down to a traceable fix.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT5-15 |
| Product Type | Automatic Hydraulic Block Making Machine |
| Control System | PLC with fault diagnosis and long-distance controlling capability |
| Vibration System | Synchronization vibration with variable frequency (low frequency feeding, high frequency compaction) |
| Material Feeding | Particular storage and description material system for feeding accuracy |
| Automation Level | Automatic |
| Output Capacity | 900–1,200 pcs/h based on 400×200×200 mm hollow block, 5 pcs/mould |
| Output Capacity | 1,080–1,440 pcs/h based on 400×150×200 mm hollow block, 6 pcs/mould |
| Output Capacity | 5,760–7,680 pcs/h based on 240×115×53 mm solid brick, 32 pcs/mould |
| Output Capacity | 3,600–4,500 pcs/h based on 200×100×60 mm rectangular paver, 25 pcs/mould |
| Output Capacity | 2,304–2,880 pcs/h based on 225×112.5×60 mm zigzag paver, 16 pcs/mould |
| Daily Output (8 hr) | 7,200–9,600 pcs based on 400×200×200 mm hollow block |
| Daily Output (8 hr) | 46,080–61,440 pcs based on 240×115×53 mm solid brick |
| Cycle Time | 15–20 s (basis not stated in source — confirm block format and mix) |
| Cycle Time (Pavers) | 20–25 s (basis not stated in source — confirm block format and mix) |
| Hydraulic Pressure | Value to be confirmed against manufacturer catalog |
| Vibration Force | Value to be confirmed against manufacturer catalog |
| Pallet Size | Value to be confirmed against manufacturer catalog |
| Rated Power | Value to be confirmed against manufacturer catalog |
| Voltage & Frequency | Configurable — to be confirmed before production |
| Overall Dimensions | Value to be confirmed against manufacturer catalog |
| Net Weight | Value to be confirmed against manufacturer catalog |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production | Crushed stone, sand, cement, fly ash aggregates in 400×200×200 mm and 400×150×200 mm formats |
| Solid brick production | Dense aggregate and cement mixes in 240×115×53 mm format |
| Rectangular paving brick | Fine aggregate and cement with high compaction in 200×100×60 mm format |
| Zigzag interlocking paver | Interlocking profile moulds with variable-frequency compaction in 225×112.5×60 mm format |
| Multi-format plant operation | Mould change across hollow block, solid brick, and paver formats within a single production shift |
What "Automatic" Really Means When the PLC Screen Speaks a Language Your Crew Cannot Read
An automatic PLC controlled block making machine is only automatic if every alarm label, parameter menu, and diagnostic prompt is readable by the people standing in front of it.
I spent most of a night in Lagos on a video call with a plant owner whose crew had powered up a newly arrived block machine and frozen it within the first hour — not because the hardware failed, but because the PLC interface was still in Chinese and the operator tapped the wrong sequence trying to clear a pallet jam. The machine sat idle until we could talk through each screen together. That kind of delay has nothing to do with engineering quality and everything to do with a single unchecked configuration setting before the crate left the factory [NEED_CITE: commissioning delays caused by incorrect PLC language settings on export machinery]. When a buyer invests in an automatic PLC controlled block making machine, the automation layer must be confirmed in writing — language, voltage, frequency, alarm logic — the same way the mould cavity count is confirmed.
Remote Diagnostics That Actually Shorten the Service Call
The PLC on the QT5-15 carries built-in fault diagnosis, meaning the controller does not simply flash a generic error code when something goes wrong. It identifies the specific sensor, solenoid, or limit switch that triggered the fault and displays it on screen. For a plant owner running multiple block lines or managing a site from a different city, the long-distance controlling capability allows production status and alarm history to be accessed off-site. This removes the need for a technician to physically stand in front of the cabinet before any meaningful troubleshooting begins.
How Variable-Frequency Vibration Changes What the Operator Controls
Conventional block presses run a single vibration frequency throughout the entire cycle. The QT5-15 uses synchronization vibration with variable frequency — low frequency during material feed so the mix flows evenly into the mould cavity, then high frequency during compaction to densify the block. The operator does not manually switch between these stages; the PLC sequences the transition as part of the automatic cycle. This is what keeps block density consistent from the first pallet of the shift to the last, regardless of how fatigued the crew is [NEED_CITE: effects of variable-frequency vibration on concrete block compressive strength consistency].
Reading the Specs That Decide Your Daily Output
The capacity figures for the QT5-15 are stated per block format because a single headline number tells a buyer almost nothing about what the machine will actually produce on a given day. Producing 400×200×200 mm hollow blocks at five cavities per mould yields a different hourly throughput than running 240×115×53 mm solid bricks at thirty-two cavities per mould, even though the press itself is the same machine. The particular storage and description material feeding system supports this range by maintaining feeding accuracy across different mix consistencies — a hollow block mix with coarse aggregate behaves differently in the hopper than a fine paver mix. The vibration force and hydraulic pressure must both be matched to the buyer’s local aggregate and target block strength, which is why these values should be confirmed during configuration rather than accepted as catalog defaults.
The Cost of Skipping Configuration Confirmation Before Shipment
When voltage, frequency, or PLC language are treated as afterthoughts, the machine arrives on site and cannot be commissioned until an electrician rewires the panel or a translator rewrites the HMI screens. Production schedules slip, concrete mix sits in the batcher, and the crew loses the first week of output they had planned around. On machines where the hydraulic schematic and electrical diagram are not provided in a format the local maintenance team can follow, even a minor fault becomes a multi-day event because nobody on site can trace the circuit [NEED_CITE: hydraulic and electrical schematic documentation standards for export machinery]. These are not machine defects — they are configuration gaps that were entirely preventable before the container was sealed.
Why Buyers Specifying Automation Choose This Configuration
Block machinery is the single focus here, so the QT5-15 is specified as a matched system — press, mould, pallet, and handling — rather than assembled from separate suppliers who each ship their own manual. The configuration is set against the buyer’s actual mix design and target format, not a catalog default, which means the vibration and hydraulic settings arrive tuned for the aggregate the buyer can actually source. Mould design covers the formats the buyer’s market sells, including custom drawings when the local demand calls for a non-standard profile. The automation level is selectable, so a buyer currently running semi-automatic equipment can plan a migration path without replacing the entire line at once. Installation and commissioning support includes operator training so the crew understands the PLC fault diagnosis screens before the first production run.
Documentation & Verification
- Line layout and capacity calculation stating the block format and mould cavity count assumed for each output figure
- Machine specification sheet confirming voltage, frequency, and PLC display language before production
- Mould drawing and format list covering every block profile the buyer intends to produce
- Hydraulic and electrical schematic in a format the local maintenance team can trace independently
- Factory test record on the buyer’s target block format before dispatch
- Operation and maintenance manual with wear parts and mould list included at packing
Installation, Commissioning & Support
- Foundation plan matched to the QT5-15 vibration load and overall dimensions confirmed at order stage
- Dedicated electrical circuit sized to the machine’s rated power with voltage and frequency verified before production
- PLC display language, alarm labels, and HMI menus confirmed in writing before the control cabinet is sealed
- First-run commissioning on the buyer’s target block format with cycle time and vibration frequency adjusted to local mix
- Operator training covering PLC fault diagnosis screens, mould change procedure, and daily maintenance checkpoints
- Wear parts list and mould inventory recommendation based on the buyer’s planned production volume and format rotation
What to Share Before Requesting a Quotation
To configure the QT5-15 accurately, the starting point is the specific block formats your market demands along with the target daily output for each format. Share your local aggregate type and cement source so the mix design can be factored into the vibration and hydraulic settings. Confirm the voltage, frequency, and PLC language your crew needs, and describe your existing pallet size and curing area layout so the handling equipment can be matched accordingly.
Frequently Asked Questions
Q: How is the QT5-15 capacity verified per block format, and what cycle time applies to each?
A: Every output figure is tied to a specific block dimension, mould cavity count, and cycle range. For example, 400×200×200 mm hollow blocks at five cavities per mould run a 15–20 second cycle, yielding 900–1,200 pieces per hour. Paver formats carry a separate 20–25 second cycle range. The capacity calculation document provided with each quotation states these assumptions per format so daily production planning is based on confirmed numbers, not a single headline figure.
Q: What PLC language options and voltage configurations are confirmed before shipment?
A: The PLC display language, alarm text, and HMI menu labels are confirmed in writing during the order stage — typically English, French, or the buyer’s specified language. Voltage and frequency are set to match the buyer’s local grid, and the electrical schematic reflects that configuration. This written confirmation prevents commissioning delays caused by language or voltage mismatches when the machine arrives on site.
Q: How does the remote diagnostics system work, and what data can be monitored off-site?
A: The long-distance controlling capability in the QT5-15 PLC allows authorized users to view production status, alarm history, and cycle parameters from a remote connection. When a fault occurs, the built-in diagnosis identifies the specific component at fault, so a multi-plant operator or off-site technician can guide on-site crew through resolution without traveling to the factory floor first.
Q: What is the upgrade path from semi-automatic to this fully automatic configuration?
A: The automation level is selectable, meaning a buyer currently running semi-automatic equipment can specify the QT5-15 with the same mould and pallet format while adding automatic pallet feeding, stacking, and PLC-controlled cycle sequencing. This lets the plant migrate from manual pallet handling to full automation without changing the block format or replacing the mould inventory already on hand.
Q: How are vibration frequency and hydraulic pressure matched to my local aggregate and mix design?
A: The variable-frequency synchronization vibration system on the QT5-15 is configured against the buyer’s actual aggregate source and target block strength rather than a single catalog default. During the proposal stage, the mix design is reviewed so the low-frequency feed and high-frequency compaction settings, along with hydraulic pressure, are calibrated for the material the buyer will actually run on site.