Description
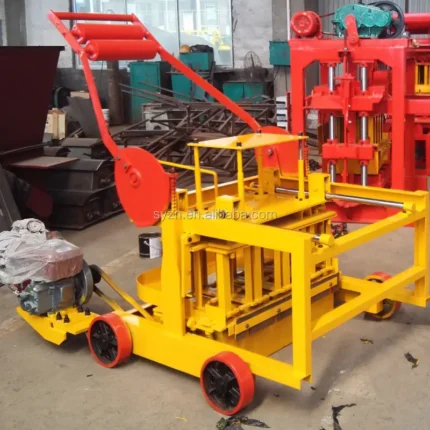
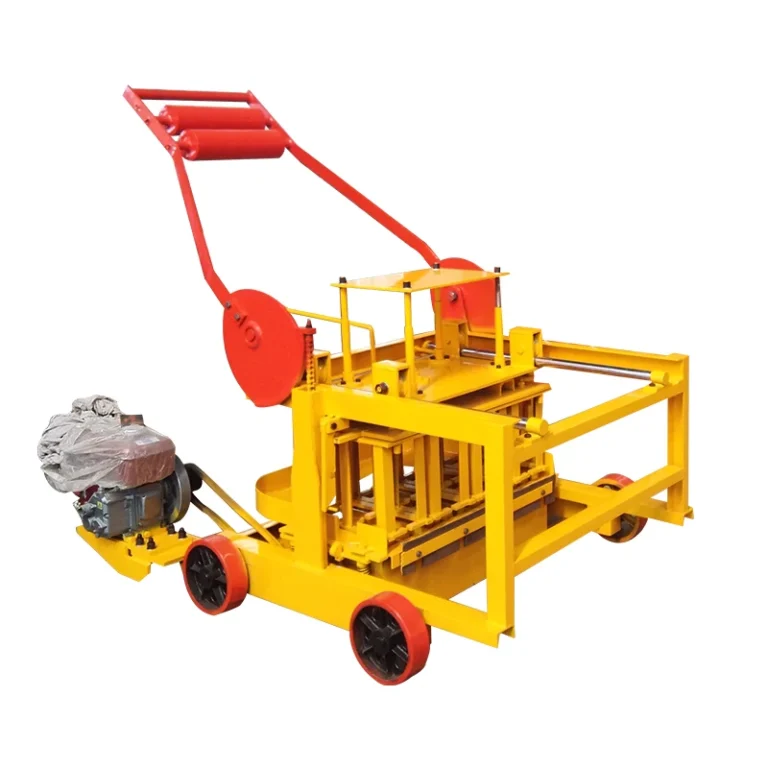
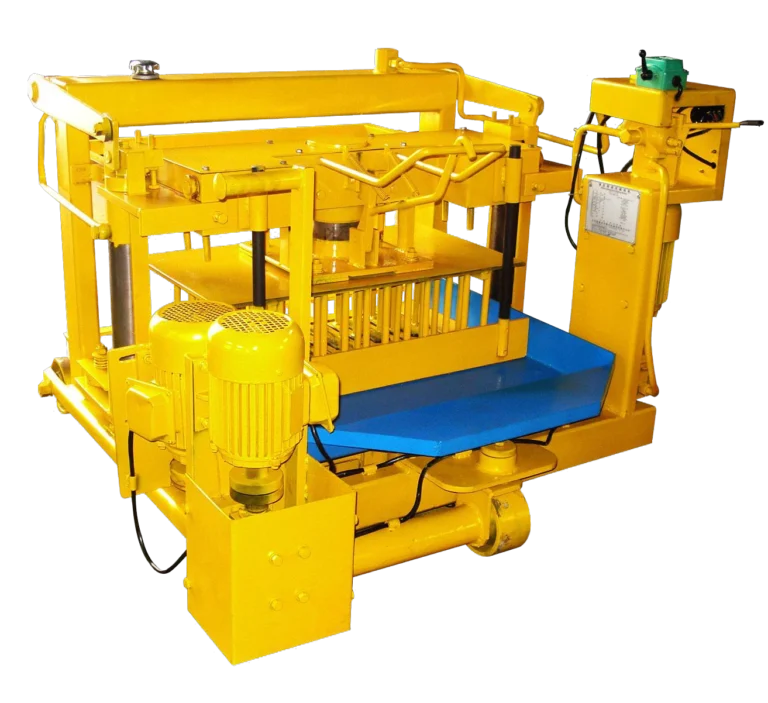
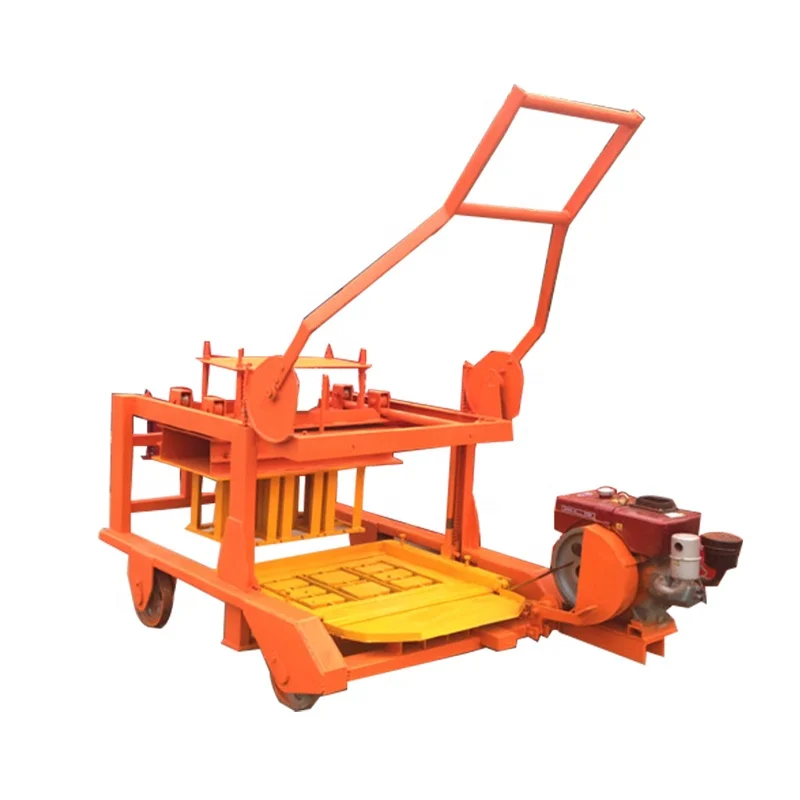
Integrated System Matching — the QMR4-45 diesel mobile block machine is specified as a matched unit where vibration force, hydraulic pressure, and mould design are set against the buyer’s actual mix and target block format, not a catalogue default.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QMR4-45 |
| Product Type | Diesel Engine Mobile Concrete Block Making Machine |
| Power Source | Diesel engine (rated kW subject to engine model confirmation) |
| Hydraulic Method | Mold Vibration |
| Exciting Power | 28.6 kN |
| Excitation Frequency | 4500 r/min |
| Molding Cycle | 30 s |
| Output Capacity | 3000 pcs/day (8 hours) (basis not stated in source — confirm block format) |
| Overall Dimensions (L×W×H) | 1300 × 1500 × 1000 mm |
| Net Weight | 950–1000 kg |
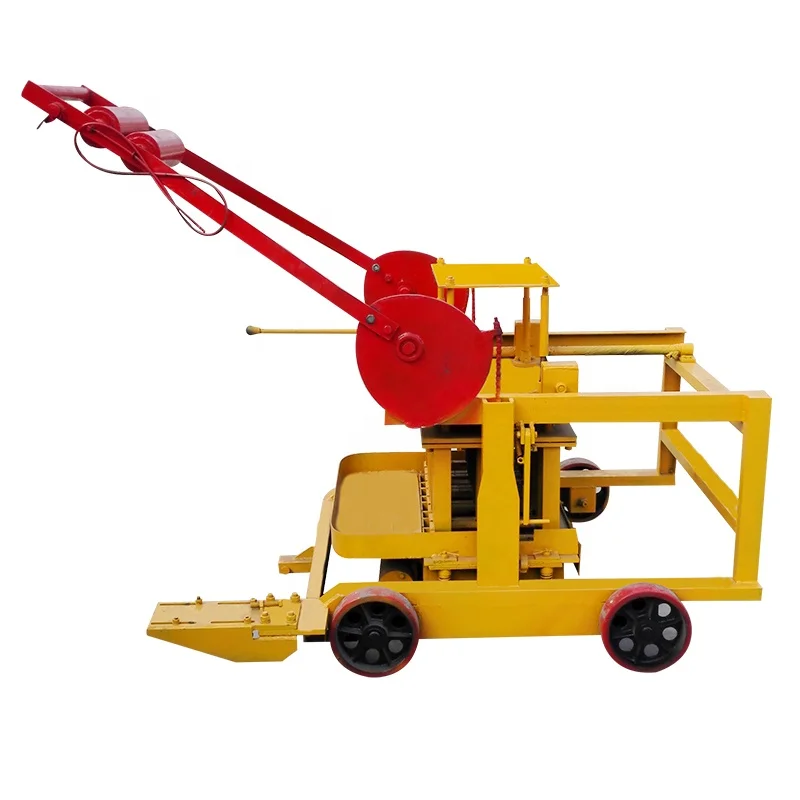
| Control System | Manual handle operation with vibratory motor and hydraulic pump |
| Automation Level | Manual / diesel-powered mobile unit |
| Raw Material Compatibility | Concrete, sand, cement, fly ash, lime, gypsum, stone dust, slag, mine tailings, river sand, construction waste, coal gangue |
| Operating Environment | Mountainous, hilly, mine industrial, suburban, desert, coastal areas |
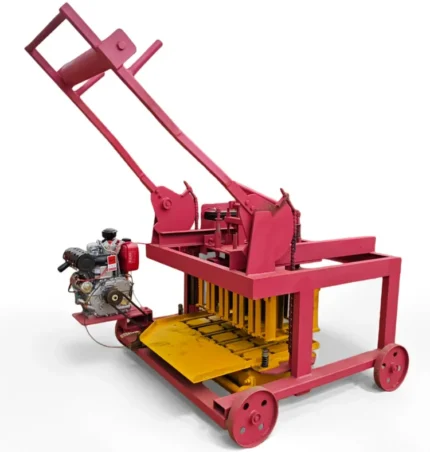
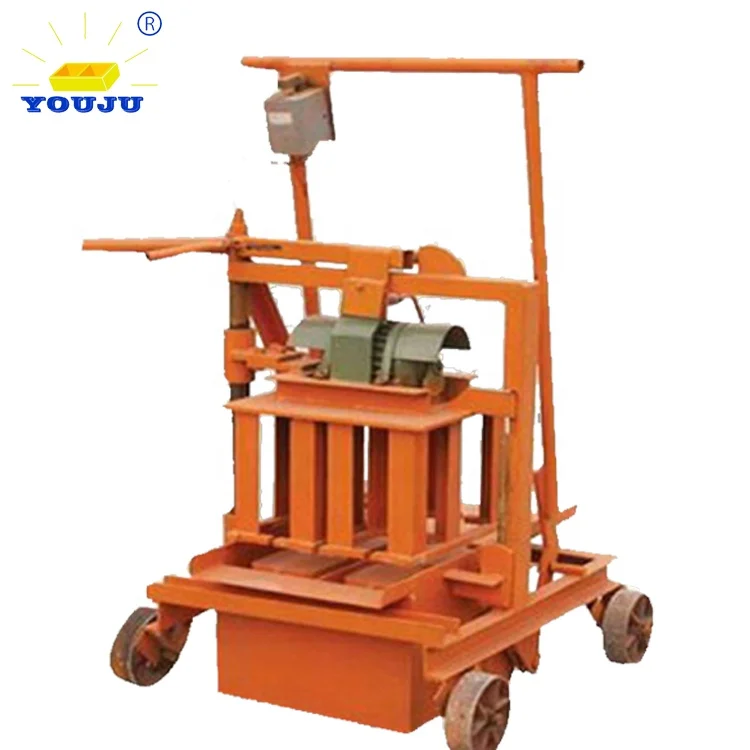
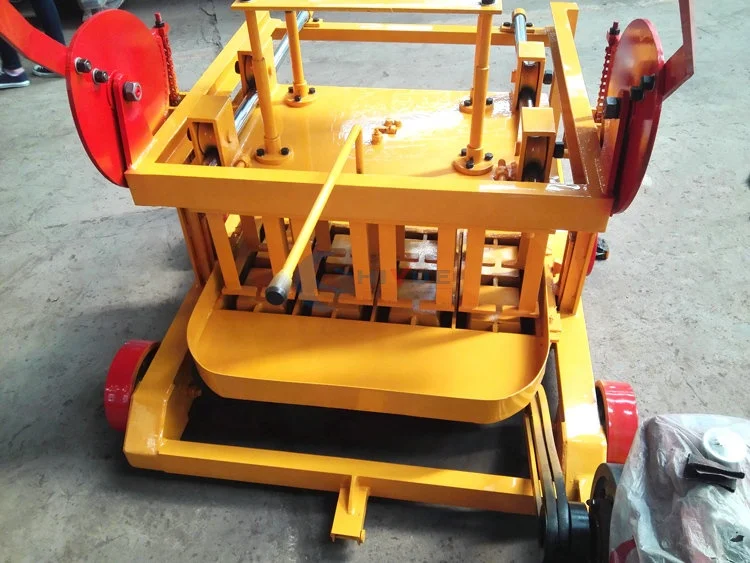
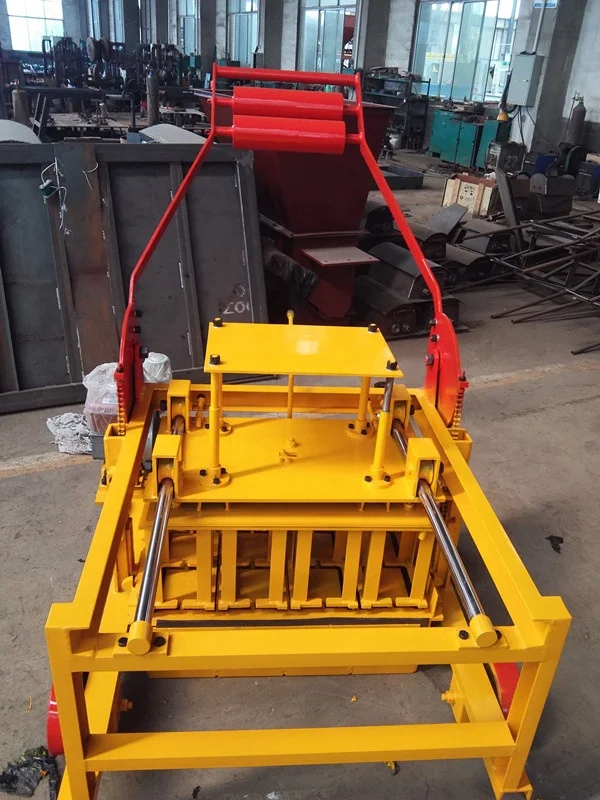
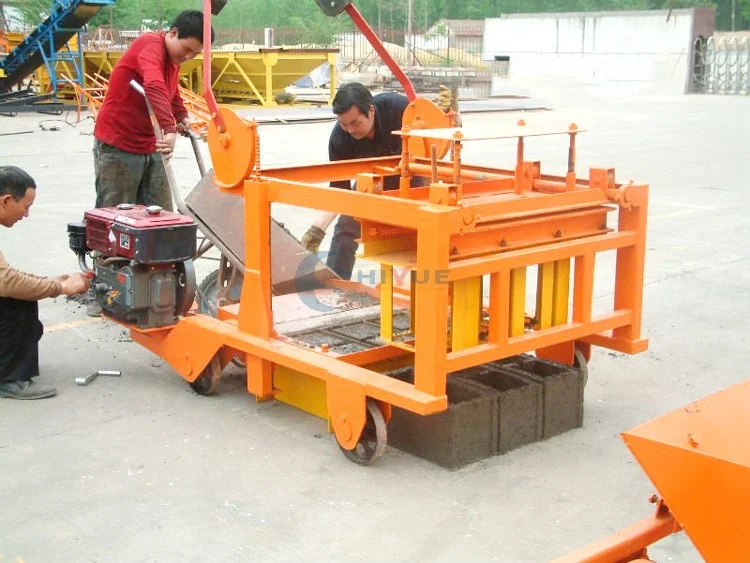
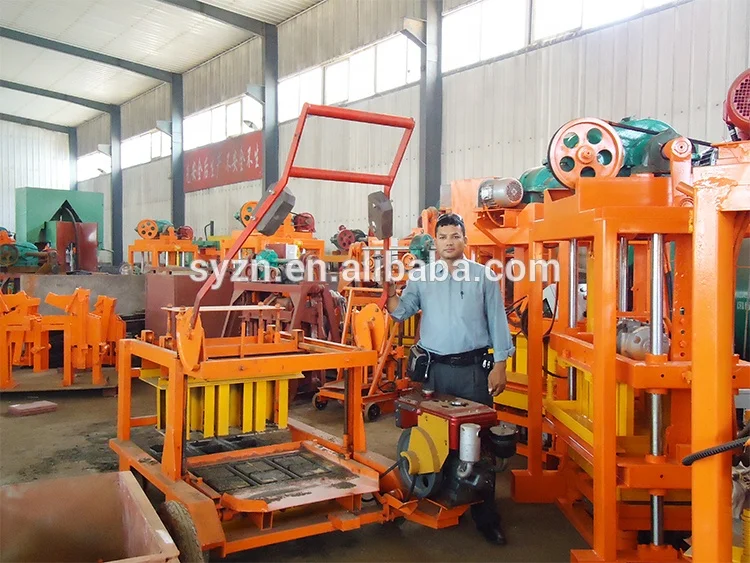
| Assembly State | Integrated mobile frame with hopper, mould box, vibratory motor, hydraulic pump |
Application Suitability
| Application | Material or Output |
|---|---|
| Remote construction site production | Crushed stone, river sand, and cement mixed on-site without grid power |
| Housing project block supply | Fly ash, slag, or construction waste blended with local aggregate |
| Entrepreneur first block plant | Standard concrete hollow blocks and solid blocks in small batch runs |
| Off-grid paver and kerbstone work | Stone dust and sand mixes in desert or coastal terrain conditions |
| Mine-adjacent building material output | Mine tailings and coal gangue as partial aggregate replacement |
What "3000 Pieces Per Day" Actually Means for Your Site
The stated daily figure only becomes real once a specific block format, wall thickness, and local mix design are locked in.
I once flew to a site in West Africa where a mobile unit was producing barely a fraction of the expected output. The operator was using red clay soil with a high moisture content, and the vibration frequency could not compact the mix properly. Every block that came off the mould was under-density and crumbled within hours. The 3000-piece number on the brochure assumed a standard concrete hollow block in a dry aggregate mix — conditions that simply did not exist at that location [NEED_CITE: impact of local aggregate moisture on block compaction density].
This is the gap between a catalogue figure and a production commitment. Before that number means anything, you need to know which mould is installed, what thickness the walls are, and whether your local sand, stone dust, or fly ash can actually achieve the compaction the vibration system delivers.
Where Manual Operation Sets the Ceiling
The QMR4-45 runs entirely on manual handle operation. The operator controls the vibratory motor start and stop, the hydraulic pump engagement, and the mould release by hand. This keeps the machine simple and field-serviceable — there is no PLC to diagnose when something goes wrong on a remote site. But it also means that cycle consistency depends entirely on the operator’s rhythm and attention.
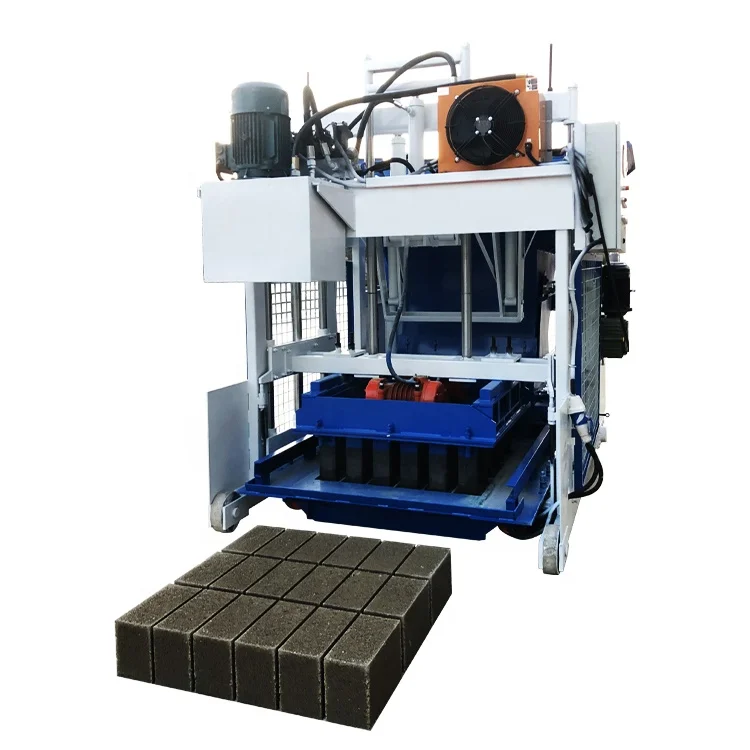
An experienced operator can hold a steady 30-second cycle. A fatigued or distracted one cannot. Batch-to-batch block density will vary across a shift, especially in hot climates where operator fatigue sets in quickly. This is the baseline that defines what the automatic mobile block machine PLC controlled configuration is designed to remove.
What a PLC Upgrade Changes in Mobile Production
Moving from manual handle control to a PLC-governed cycle means the machine controls vibration duration, hydraulic pressure application, and mould release timing automatically. The operator’s role shifts from executing every step to monitoring the sequence and feeding raw material. For mobile producers planning to scale, the question is whether the frame and hydraulic architecture of this unit accept a future PLC retrofit — or whether the path to automatic mobile block machine PLC controlled operation requires stepping up to a different machine tier entirely [NEED_CITE: PLC retrofit compatibility with manual mobile block press frames].
Vibration Force and Cycle Timing Against Your Mix
The 28.6 kN exciting power at 4500 r/min defines what this machine can compact. Vibration force and frequency together determine how densely the aggregate particles pack inside the mould. A coarse, angular crushed stone mix responds well to high-frequency vibration because the particles rearrange under rapid oscillation. A fine, high-clay mix absorbs vibration energy differently and may require longer cycle times or higher amplitude to achieve the same density.
The 30-second moulding cycle is the mechanical baseline. Whether that cycle produces a structurally sound block depends on whether your cement-to-aggregate ratio, water content, and particle size distribution align with what 28.6 kN can consolidate in that window. A factory test run using your actual raw material — not a standard lab mix — is the only way to confirm this before the machine ships.
The Cost of Skipping the Mix-to-Vibration Match
When vibration force and hydraulic pressure are not evaluated against the buyer’s specific aggregate, the consequences show up in the curing yard. Blocks crack during handling. Wall density is uneven from top to bottom. Reject rates climb, and the operator compensates by adding more cement — the most expensive ingredient in the mix. The machine is not broken; it is simply configured for a material it is not processing. I have seen entire production runs scrapped because the vibration frequency was set for river sand while the site was running quarry dust [NEED_CITE: block rejection rates from unmatched vibration settings].
Why Sourcing This Unit Through a Matched-System Supplier
Block machinery is our single focus, which means the QMR4-45 is evaluated as a system where the diesel engine, vibration motor, hydraulic pump, and mould are specified together — not assembled from separate vendor catalogues. Every configuration is checked against your local aggregate type, target block format, and site conditions before production begins. Mould design covers the formats your market actually sells, and custom mould drawings are supported from the start. The automation level is selectable, so you can begin with manual diesel operation and plan a clear path toward semi-automatic or PLC-controlled production as demand grows. Installation support includes operator training so that cycle timing and mix handling are established from the first day on site.
Documentation & Verification
- Capacity calculation document stating the specific block format and wall thickness assumed
- Factory test record showing vibration force and cycle time measured against your submitted mix sample
- Mould drawing and format list covering every block type included in your order
- Hydraulic and electrical schematic with voltage and frequency confirmation for your market
- Operation and maintenance manual in your operator’s language
- Wear parts and mould list with recommended replacement intervals
Installation, Commissioning & Support
- Level compacted ground required; integrated mobile frame eliminates fixed foundation work for the 1300 × 1500 mm footprint
- Diesel engine fuel specification and lubricant schedule confirmed before first startup on the QMR4-45
- Mould box alignment and vibration motor connection checked during on-site commissioning
- Operator training covers manual handle cycle rhythm, mix loading sequence, and block release technique
- Mould change procedure trained on-site so format switching does not consume a full shift
- Spare vibration motor brushes and hydraulic seals included for the first operational months
Before You Request a Quote
To give you a meaningful configuration, we need to know the block format and wall thickness you plan to produce, the daily output you are targeting, and the raw materials available at your site — including the type of sand or aggregate and your cement supply. If you are planning a future move to PLC-controlled automation, tell us your local voltage standard and preferred control language so the upgrade path is built into the initial specification.
Frequently Asked Questions
Q: How do I verify what 3000 pieces per day actually means for my block format?
A: The capacity figure requires a stated mould size, block wall thickness, and mix composition to be meaningful. Request a capacity calculation document that names the exact block format used for the calculation. Without this, the number is a catalogue reference, not a production commitment against your actual product.
Q: Can this manual diesel unit be upgraded to PLC-controlled operation later?
A: The QMR4-45 is built as a manual handle machine. Whether the frame accepts a future PLC retrofit, automatic pallet feeding, or stacking module depends on the hydraulic and electrical architecture. Ask for a written upgrade path assessment before committing, so you know the options and their cost.
Q: How do I confirm the electrical standard if the machine runs on diesel?
A: The vibratory motor and any future PLC control module still require an electrical specification. Confirm your local voltage and frequency, and your preferred control panel language, before production begins. This avoids costly rewiring or control replacement if you later add automation components.
Q: How is the vibration force matched to my local aggregate and mix design?
A: The 28.6 kN exciting power and 4500 r/min frequency must be evaluated against your specific material. Submit a sample of your aggregate and your planned cement ratio. A factory test using your material — not a standard reference mix — confirms whether block density meets your structural requirement before the machine ships.
Q: What does PLC control add compared to the manual handle on this diesel unit?
A: A PLC-controlled system governs vibration duration, hydraulic pressure timing, and mould release automatically. This removes cycle-to-cycle variation caused by operator fatigue and delivers consistent block density across an entire shift. For the QMR4-45, the key question is whether your growth plan justifies starting manual and upgrading, or selecting a PLC-native mobile line from the outset.