
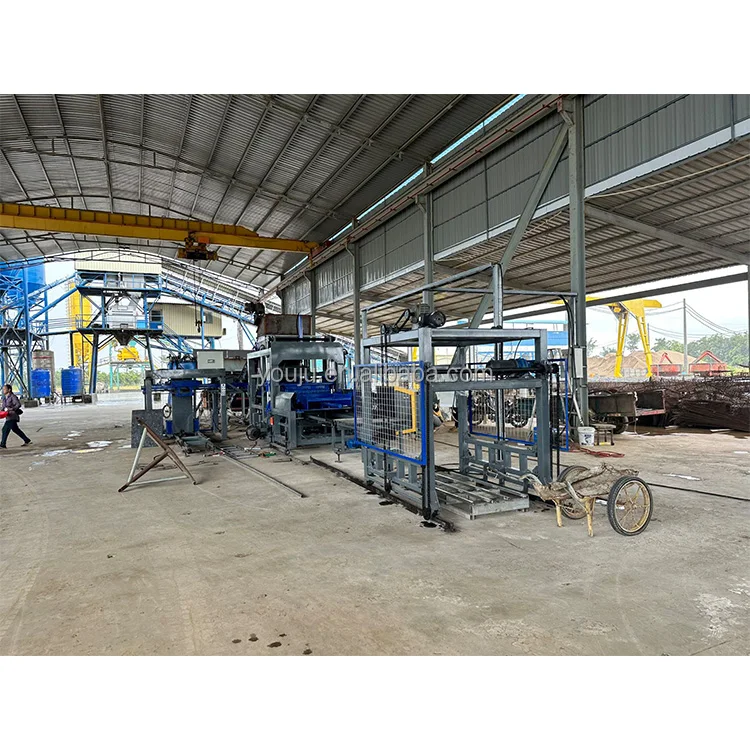
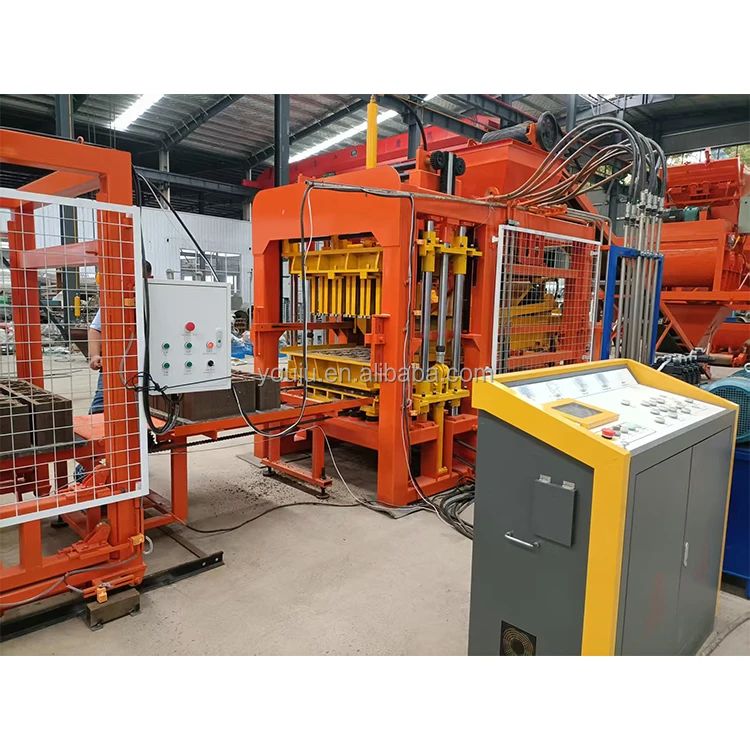


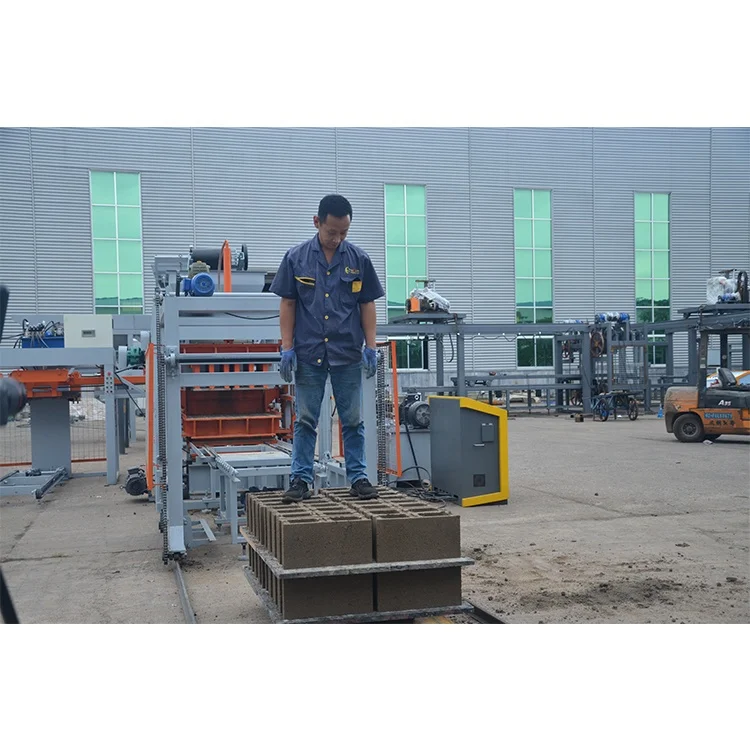
Description
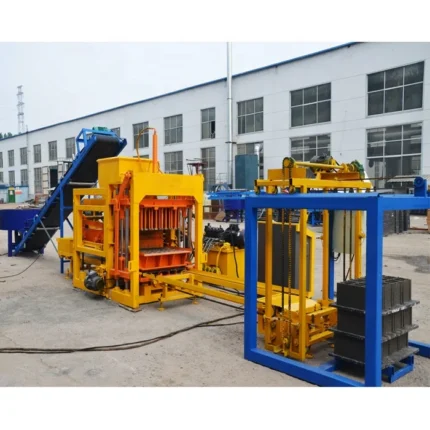
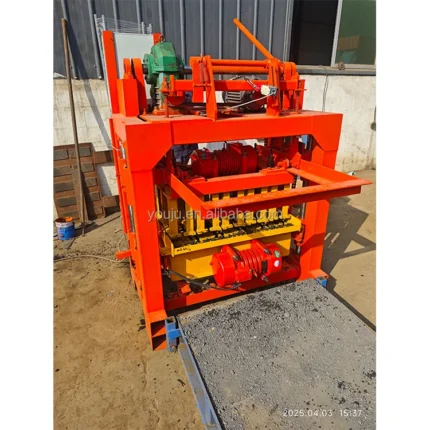
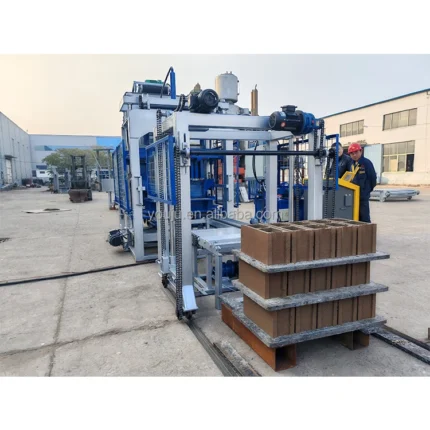
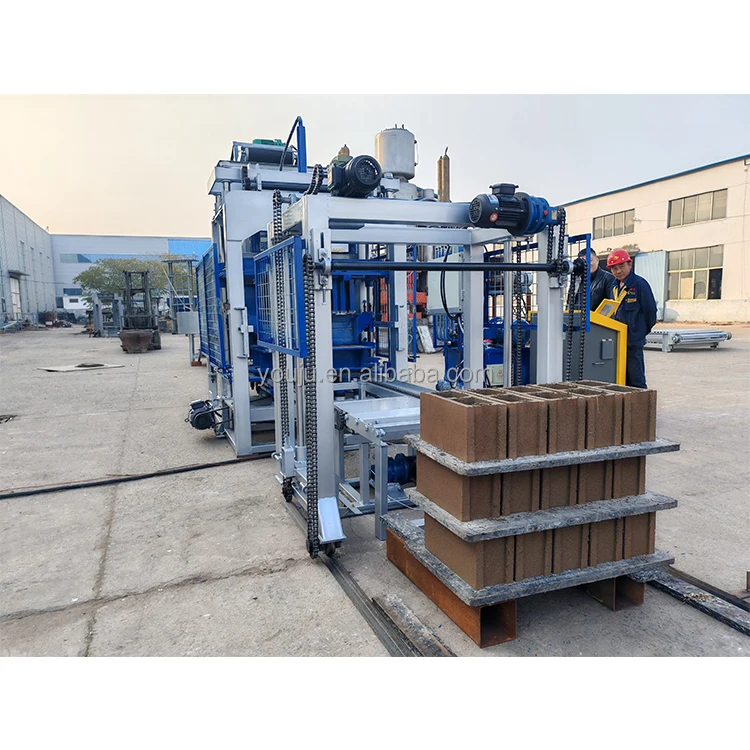
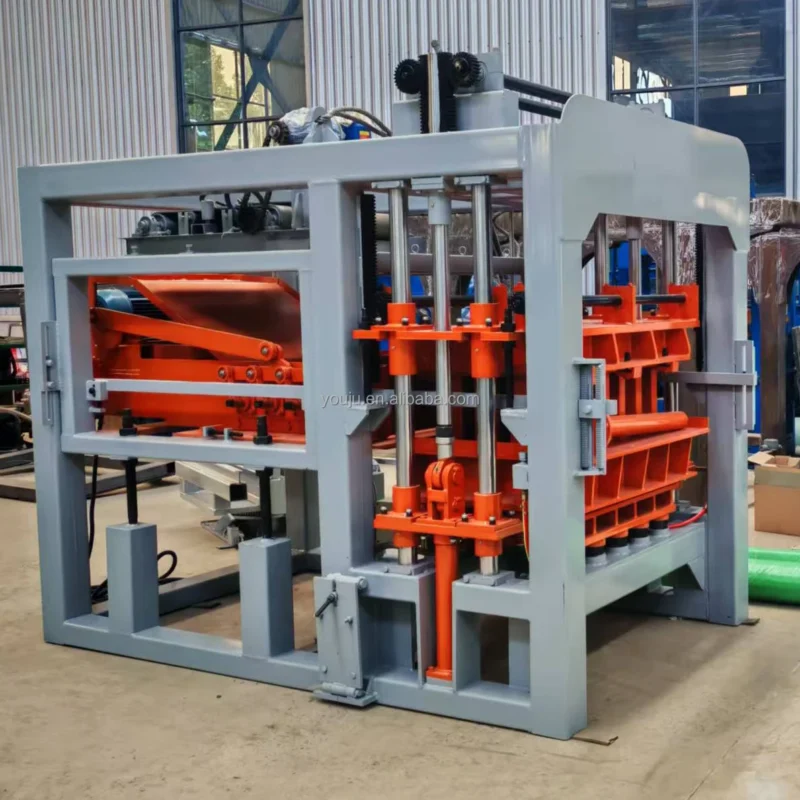
Intelligent Control Integration — the QT6-15 automatic QT6-15 block making machine replaces manual judgment with PLC-managed cycle parameters, ensuring every pallet leaves the press at the same density regardless of operator experience.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT6-15 |
| Product Type | Stationary Hydraulic Block Making Machine |
| Overall Dimensions (L×W×H) | 7100×1500×3000 mm |
| Rated Pressure | 21 MPa |
| Main Vibration Form | Platform vibration |
| Vibration Frequency | 4500–5100 r/min |
| Pallet Size | 880×850 mm |
| Moulding Cycle | 15–25 s |
| Overall Power | 31.25 kW |
| Net Weight | 8700 kg |
| Control System | PLC intelligence control |
| Automation Level | Fully automatic |
| Hydraulic Drive | Yes |
| Raw Material Ratio (example) | Cement 8–10%, Sand 30–40%, Stone 50–60% |
| Water Consumption | 3–5% of raw material weight |
Application Suitability
| Application | Material or Output |
|---|---|
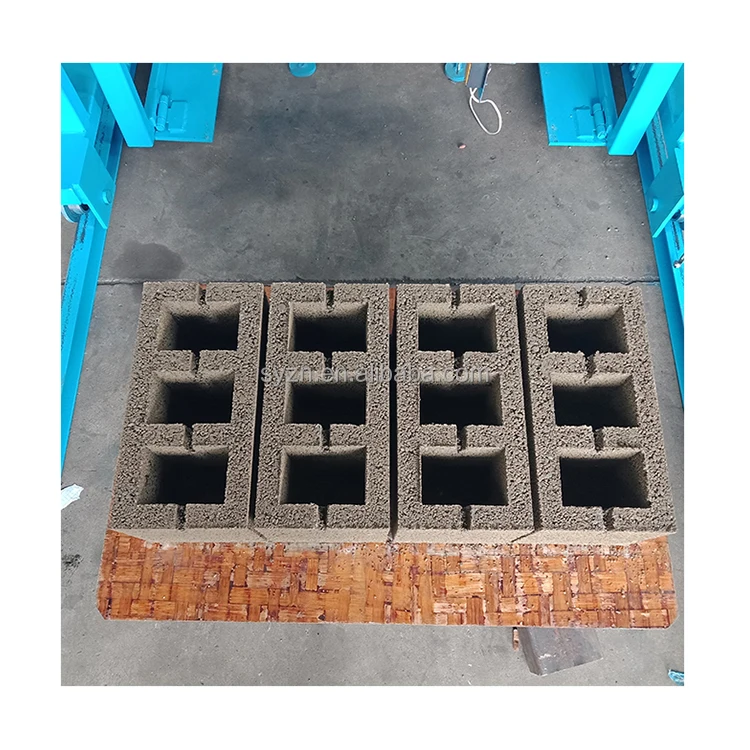
| Hollow block production plants | Crushed stone, sand and cement blends targeting 8–10 MPa compressive strength |
| Solid brick manufacturing | Dense aggregate mixes for load-bearing walls, 10–20 MPa range |
| Paver and interlocking brick lines | Fine aggregate and pigment combinations for architectural finishes |
| On-site contractor production | Locally sourced gravel and cement for housing and infrastructure projects |
Why the PLC Language Setting Matters Before the Crate Is Nailed Shut
A fully automatic press becomes a very expensive manual press when the operator cannot read the screen.
I once spent four hours on a video call at three in the morning, walking a Spanish-speaking crew through an auto-stacking sequence that would not start because the HMI defaulted to English. The hardware was perfect. The software spoke the wrong language. Commissioning delays like this are more common than mechanical faults, and they are entirely preventable if the PLC controlled hydraulic block machine display language, voltage and frequency are locked down before the machine leaves the factory floor. Buyers often focus on cycle speed and pallet size, yet the control interface is where the operator lives every shift [NEED_CITE: common commissioning delay causes in exported industrial machinery].
What the PLC Actually Takes Over From the Operator
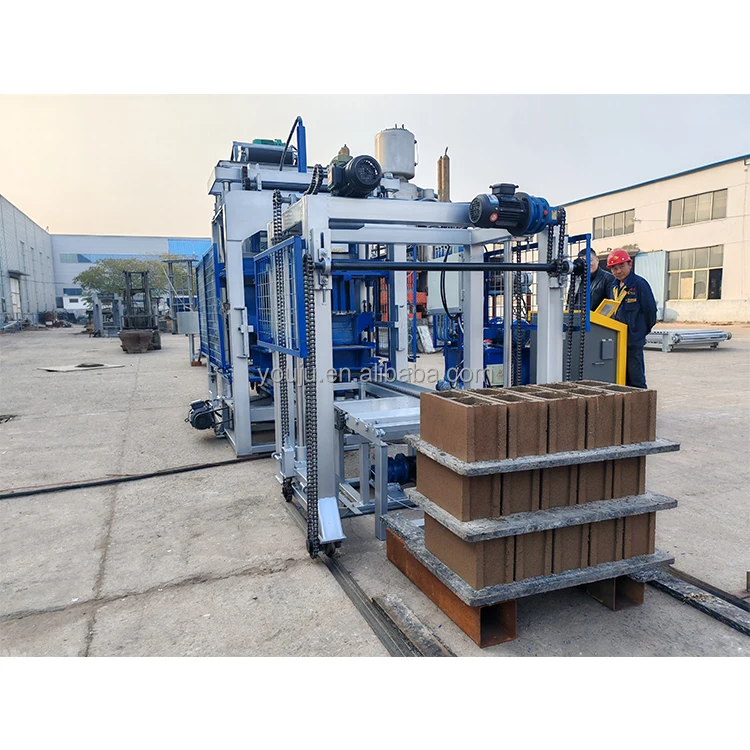
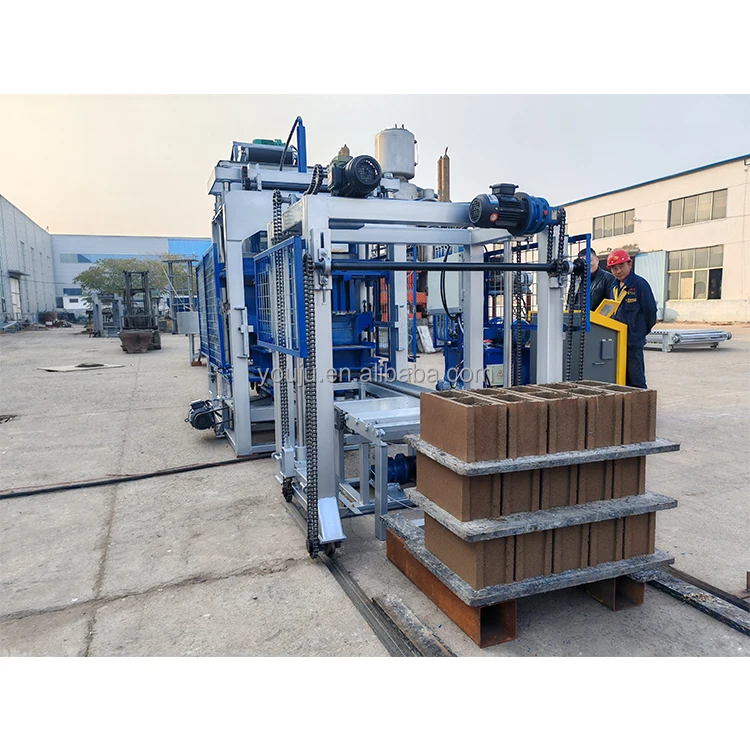
On a manual or semi-automatic press, the operator decides when to feed, when to vibrate, how long to hold pressure, and when to release. Every decision introduces variation. The automatic QT6-15 block making machine sequences these steps through programmable logic — raw material feed, vibration onset, hydraulic compression and pallet advance all run on stored recipes. Once a recipe is validated for a given block format and mix, the press repeats it within tight tolerances across hundreds of cycles. The operator’s role shifts from real-time decision-making to monitoring and exception handling.
From Semi-Automatic to Full Line Control
Many plants start with a semi-automatic press and add pallet handling later. The PLC architecture here supports that path: automatic pallet feeding, stacking and curing-rack handling can be integrated as separate stations that communicate with the main press controller. The critical constraint is cycle synchronization — if the stacker cannot clear a pallet within the press cycle window, the press waits and output drops. Matching station speeds during the line design phase prevents bottlenecks that no amount of PLC tuning can fix afterward [NEED_CITE: PLC synchronization principles in concrete block production lines].
Reading the Numbers That Actually Matter
The rated pressure of 21 MPa and vibration frequency of 4500–5100 r/min work together to compact the mix. Pressure alone flattens the block; vibration alone rearranges particles without full densification. Combined, they produce consistent internal density across the pallet — which is what determines whether a hollow block hits 8 MPa or falls short. The 880×850 mm pallet size defines how many blocks fit per cycle, and the 15–25 second moulding cycle range tells you that denser formats or thicker pavers sit at the upper end. The 31.25 kW overall power budget covers the hydraulic pump, vibration motors and conveyor drives simultaneously, so verify that your site electrical supply can sustain this draw continuously rather than just at peak startup [NEED_CITE: electrical load planning for stationary block making equipment].
The Cost of Skipping the Configuration Conversation
When voltage and frequency are assumed rather than confirmed, a machine wired for 380V/50Hz arrives at a site running 440V/60Hz and the hydraulic pump motor burns out within the first week. When the pallet size is chosen without checking the buyer’s existing curing racks and forklift tines, pallets stack unevenly or cannot be moved at all. When moulds are ordered without specifying the exact block dimensions the local market demands, the first format change reveals that the mould adapter plate was never machined for the second mould. These are not warranty issues — they are configuration oversights that delay revenue by weeks [NEED_CITE: export machinery installation failure patterns].
Why Procurement Here Reduces Integration Risk
Block machinery is the sole product focus, which means the press, moulds, pallets and handling equipment are specified as one matched system rather than sourced from separate vendors and forced to communicate afterward. Machine configuration is set against the buyer’s actual mix design and local aggregate, not pulled from a catalogue default — the cement-to-aggregate ratio matters because it changes how the 21 MPa pressure and vibration interact with the mix. Mould design covers the formats the buyer’s market actually sells, with custom drawings available when standard moulds do not match. Automation level is selectable so a buyer can commission the QT6-15 in semi-automatic mode and expand to full PLC-controlled operation as volume justifies the investment. Installation support includes on-site commissioning with operator training that covers recipe setup and fault-code reading in the confirmed language.
Documentation & Verification
- Line layout with capacity calculation stated per target block format
- Hydraulic and electrical schematic matching confirmed voltage and frequency
- Factory test record on buyer’s specified mould and pallet combination
- PLC program backup with recipe parameters for each ordered block format
- Wear parts and mould list with part numbers for first replacement cycle
- Operation and maintenance manual in confirmed display language
Installation, Commissioning & Support
- Foundation pad sized for 7100×1500 mm footprint with vibration isolation trenches
- Dedicated circuit rated for 31.25 kW continuous draw at confirmed voltage and frequency
- Machine shipped in modular sections for container loading and reassembled on site
- First-run commissioning includes recipe tuning for local aggregate and cement source
- Operator training covers PLC fault codes, mould changeover and daily maintenance checks
- Spare hydraulic seals and vibration motor brushes stocked for initial operating period
Before You Request a Quote
Send the exact block dimensions and compressive strength your market requires, the local aggregate type and cement grade available, and your site voltage and frequency. Include your existing pallet size if you plan to reuse curing racks and forklifts. Specify the PLC display language your operators read.
Frequently Asked Questions
Q: How is daily output capacity calculated for a specific block format?
A: The moulding cycle ranges from 15 to 25 seconds depending on block thickness and density target. Daily output is calculated by multiplying cycles per hour by blocks per pallet, then adjusting for actual shift length and mould change downtime. We state the capacity per block format in the proposal so you can compare it against your sales volume, not against a generic cycles-per-hour figure that assumes a format you may never produce.
Q: What is the upgrade path from semi-automatic to fully automatic operation?
A: The PLC architecture supports staged integration of pallet feeding, automatic stacking and curing-rack handling as separate stations. Each station communicates with the main press controller, and cycle synchronization is verified during commissioning. A plant running semi-automatic today can add automation modules as volume grows without replacing the press itself.
Q: How does the PLC maintain consistency across production batches?
A: Stored recipes control feed volume, vibration duration, hydraulic pressure hold time and pallet advance speed. Once a recipe is validated for a specific mix and block format, the press repeats these parameters within tight tolerances. The operator monitors the process rather than adjusting it in real time, which removes the batch-to-batch variation that manual operation introduces.
Q: What electrical and language details must be confirmed before shipment?
A: Site voltage, frequency and phase configuration must match the motor and pump ratings. The PLC display language must match what your operators read — an English interface in a Spanish-speaking plant creates commissioning delays. These three items are confirmed in writing before the machine enters final assembly.
Q: How long does a typical mould change take on this press?
A: Changeover time depends on whether the mould uses a quick-release clamp system or bolt-on mounting, and whether the new mould is pre-staged beside the press. The proposal includes the mould change procedure and estimated time for each format you order, so you can plan shift scheduling around format rotation rather than discovering the delay on the first day you switch.