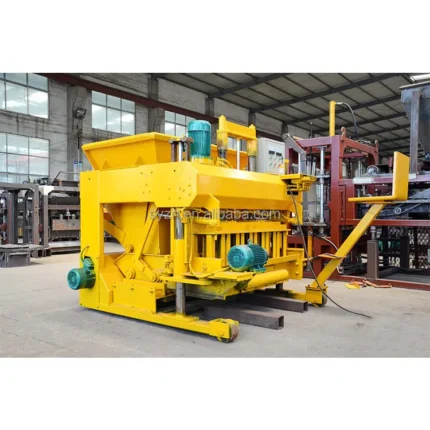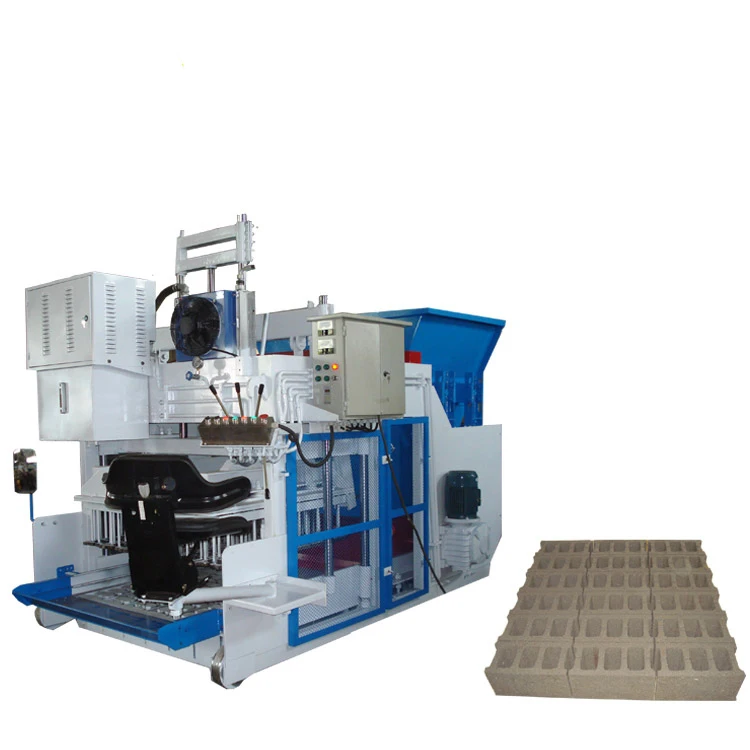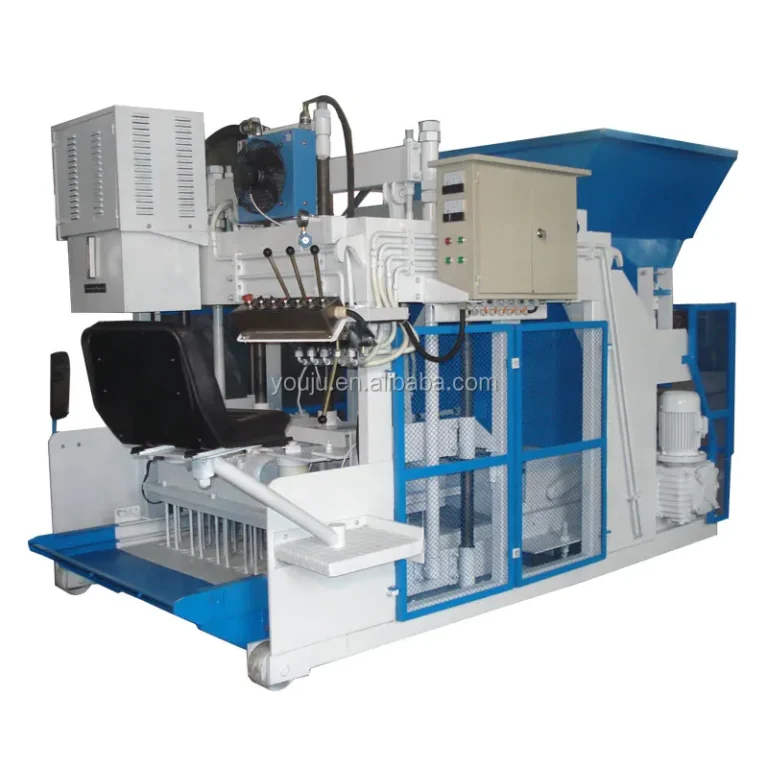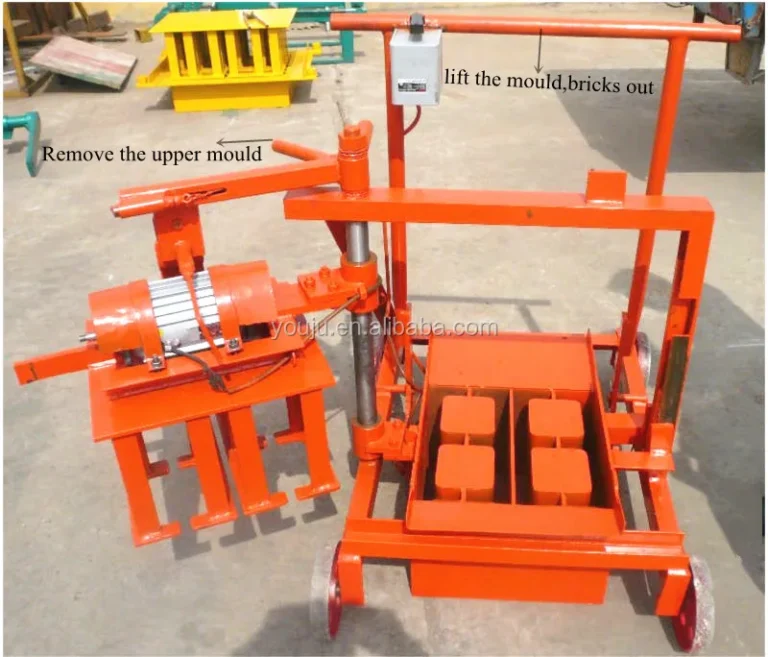
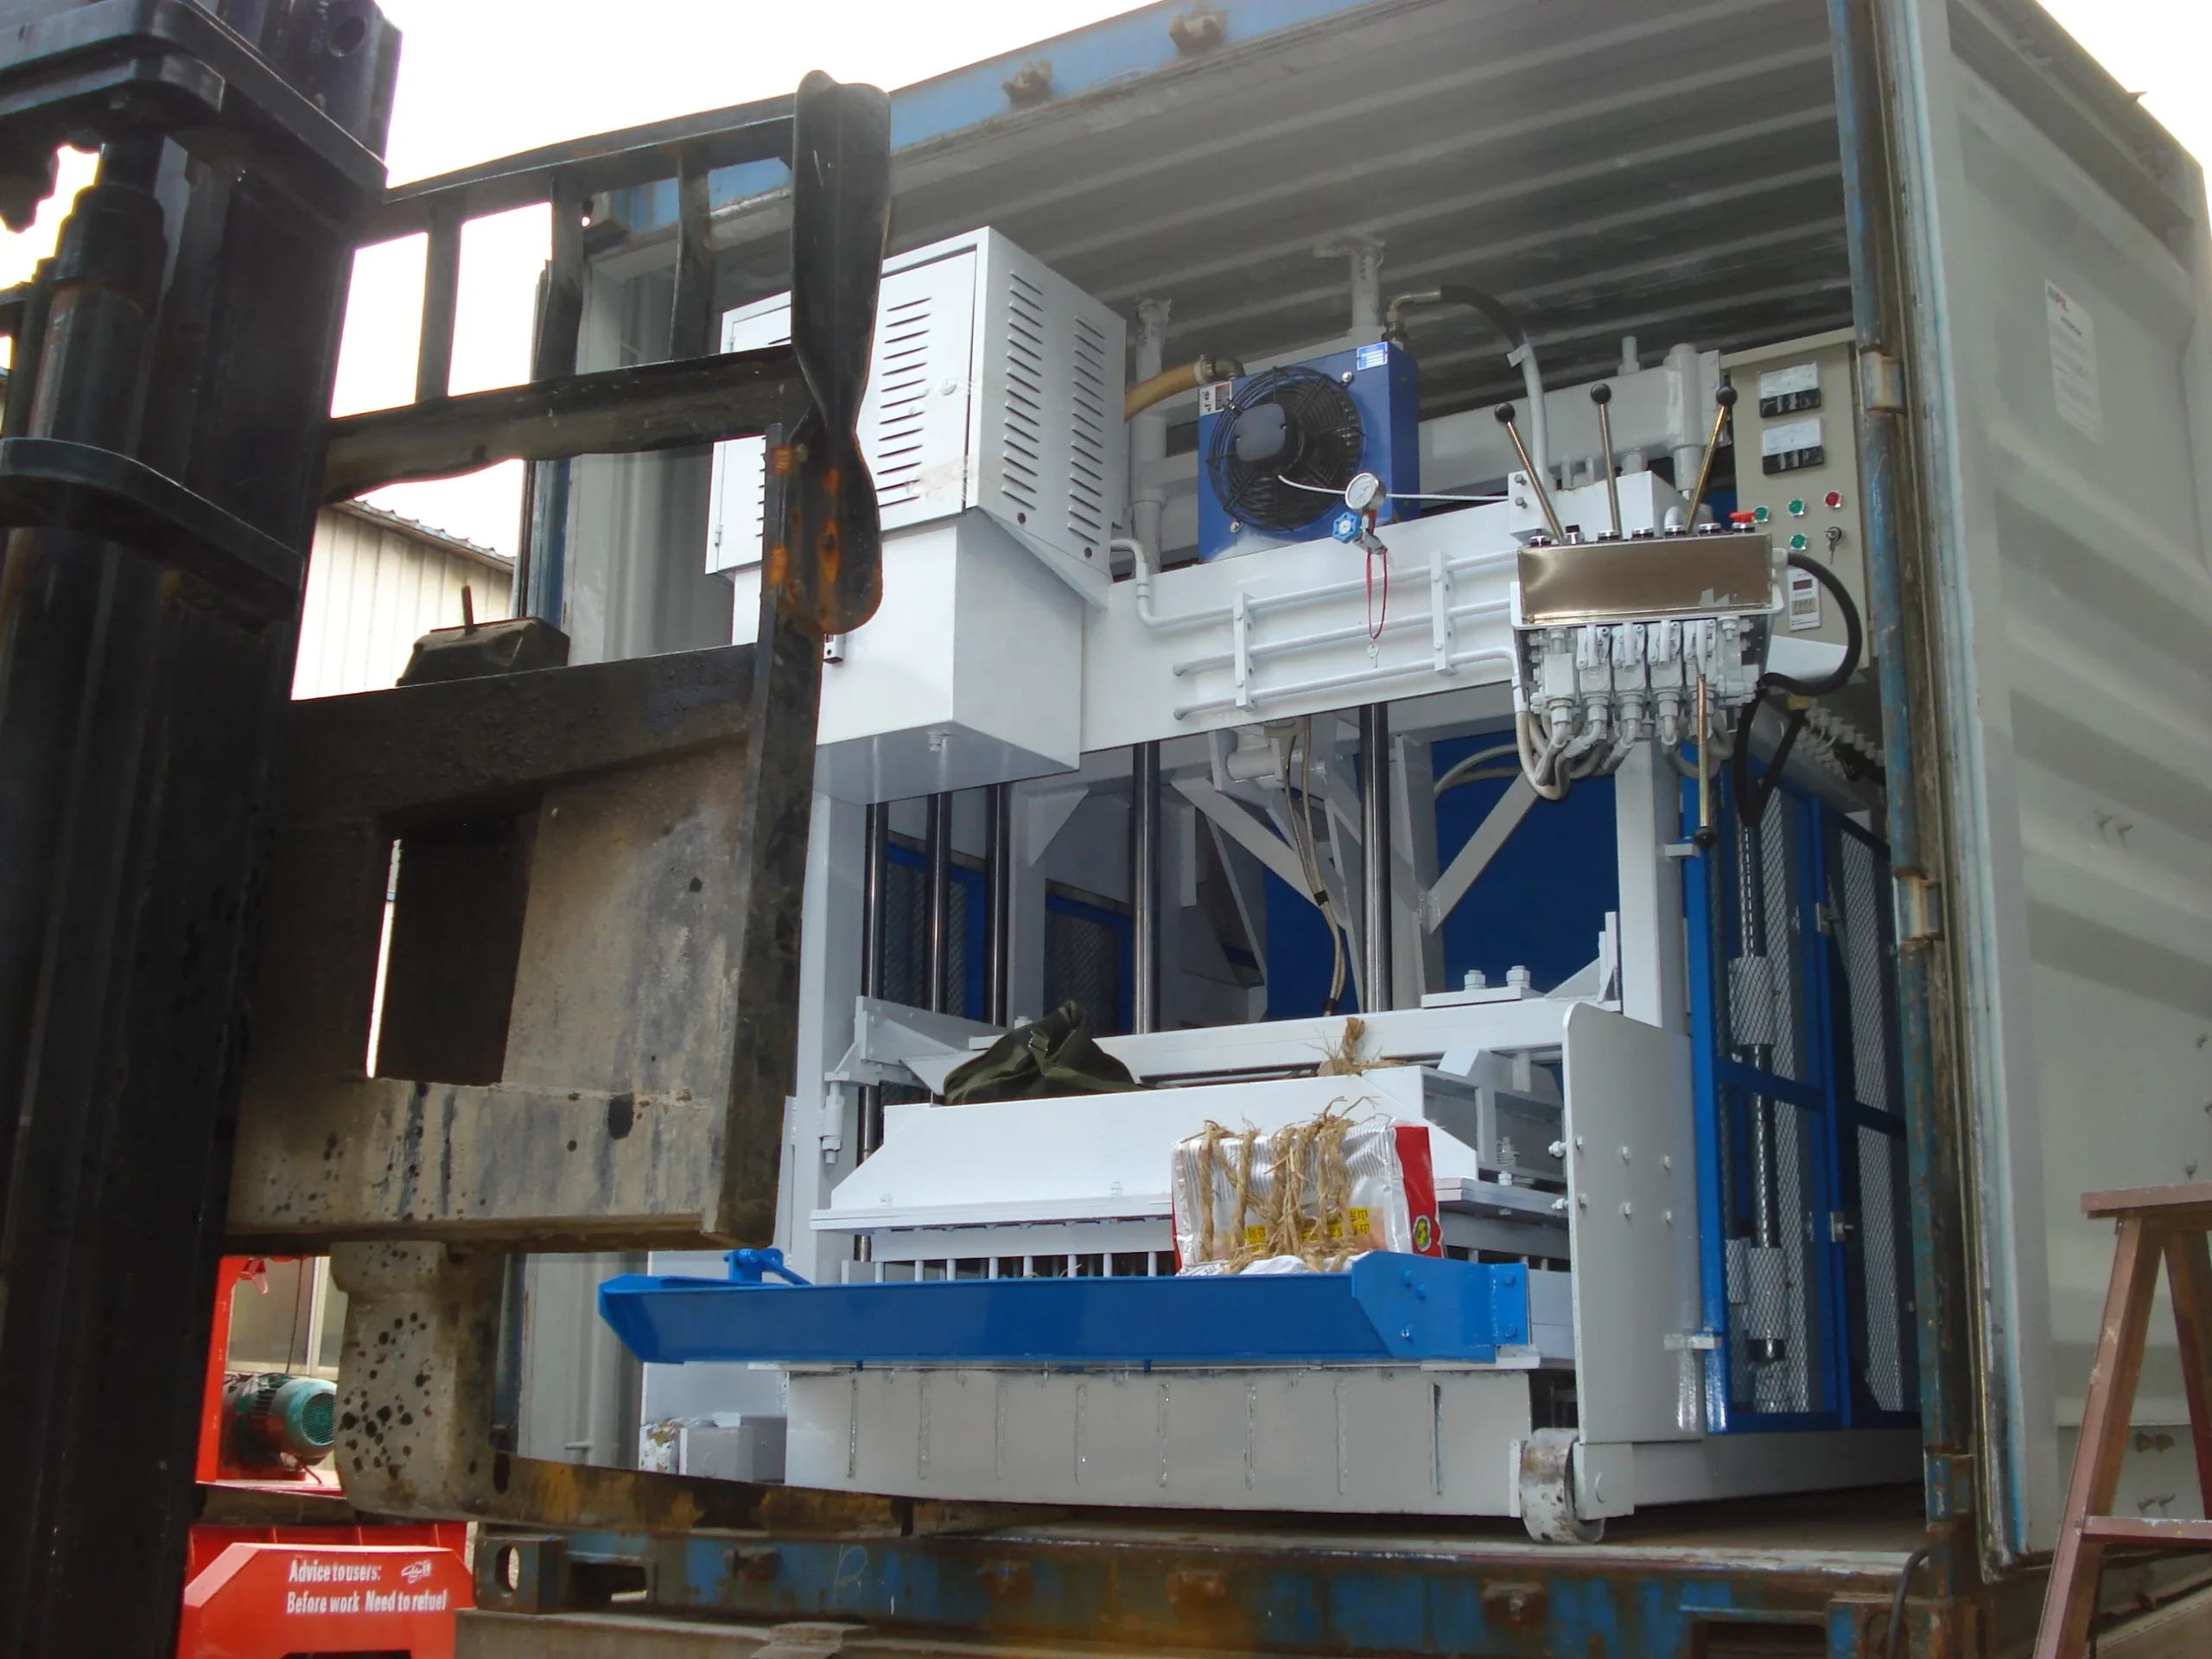
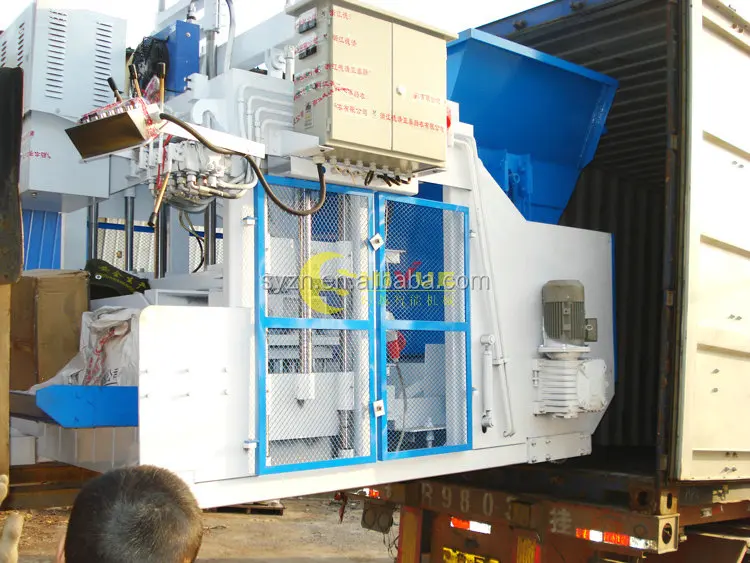
Description
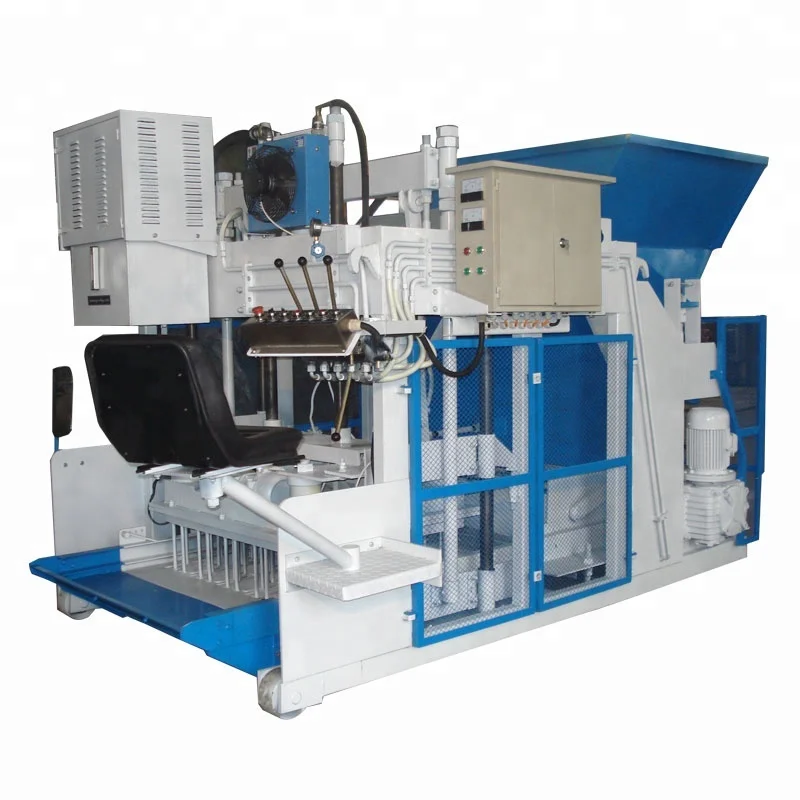
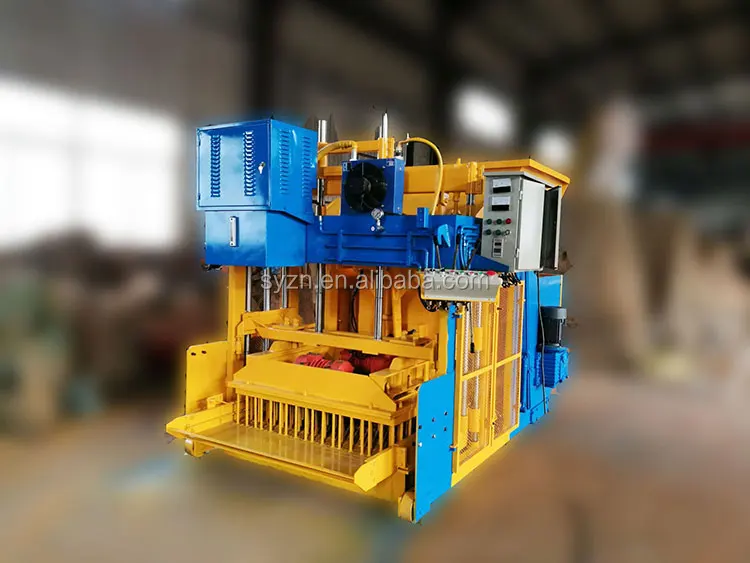
Single-Focus Engineering — Every QMY12-15 parameter, from its 16–20 MPa hydraulic system to its PLC logic, is tuned around one outcome: repeatable block density on the egg-laying path.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Mobile Egg Laying Block Making Machine |
| Model | QMY12-15 |
| Overall Dimensions (L×W×H) | 3250 × 2100 × 2300 mm |
| Net Weight | 4200 kg |
| Total Installed Power | 16 kW |
| Hydraulic System Pressure | 16–20 MPa |
| Vibration Mode | Three-dimensional mold vibration |
| Excitation Frequency | 3200 Hz |
| Molding Cycle | 10–15 s (basis not stated in source — confirm block format / material / thickness) |
| Demold & Turning Method | Hydraulic |
| Moving & Steering | Automatic movement with hydraulic steering |
| Mould Format Reference | 12 pcs/mould based on 400×200×200 mm hollow block |
| Output Capacity (400×200×200 mm hollow block) | 2880 pcs/h at 15–20 s cycle |
| Output Capacity (400×150×200 mm hollow block) | 3360 pcs/h at 15–20 s cycle |
| Output Capacity (400×100×200 mm hollow block) | 5280 pcs/h at 15–20 s cycle |
| Block Compressive Strength | ≥ 15 MPa |
| Control System | PLC computer automatic control (brand and display language to be confirmed) |
| Voltage & Frequency | To be confirmed against target site supply |
| Supported Raw Materials | Fly ash, cinder, coal gangue, river sand, gravel, cement, and other industrial residues |
| Mould Change Formats | Hollow block, porous brick, road kerb, road brick, grassing brick |
| Automation Level | Semi-automatic (automatic movement and hydraulic steering; pallet and stacking scope to confirm) |
| Paint Finish | Custom color available |
| Warranty | 1 year on whole machine, excluding spare parts |
Application Suitability
| Application | Material or Output |
|---|---|
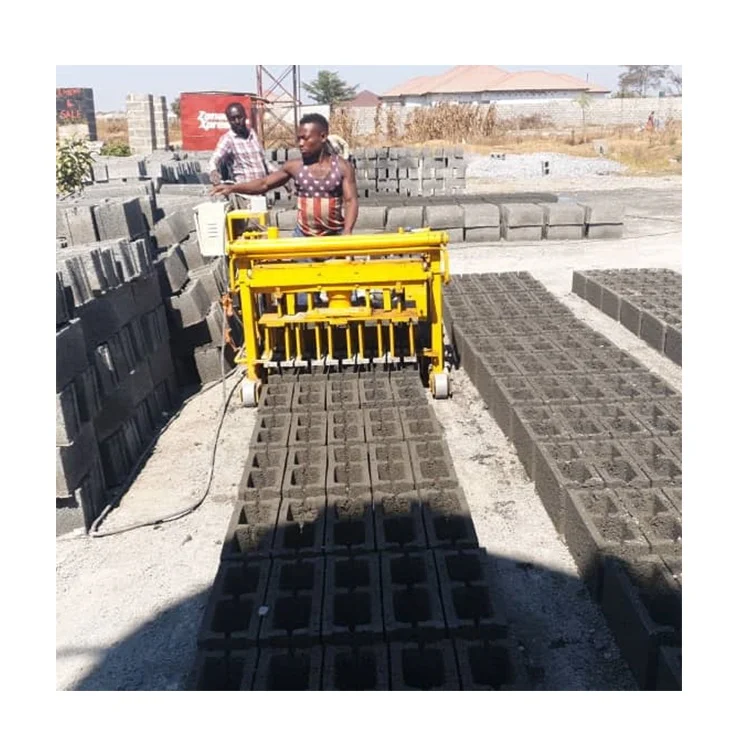
| On-site hollow block production without a fixed plant | River sand, gravel, and cement mixes laid directly on cured concrete floors |
| Porous brick manufacturing for permeable paving | Fly ash and coal gangue blends with controlled moisture |
| Road kerb and kerbstone forming at project sites | Crushed aggregate with high cement content for ≥ 15 MPa strength |
| Grassing brick for landscaping and drainage | Cinder and sand mixes with open-cell mould geometry |
| Small-plant paver and road brick runs | Industrial waste residues blended with cement binder |
What "2880 Pieces per Hour" Leaves Out About an automatic mobile block machine PLC controlled Setup
Quoted hourly output is meaningless unless tied to a specific block format, cycle time, and mix design.
I have watched buyers sign off on a mobile egg-laying machine because the brochure said "nearly 3000 pieces an hour," only to arrive at their site and discover that figure assumed a thin 100 mm hollow block on a perfect standard-sand mix. Switch to the 200 mm block their market actually buys, feed the machine river sand with high clay content, and the same machine drops to a fraction of that number while producing blocks that crack during curing. An automatic mobile block machine PLC controlled system can only hold consistent density if the vibration curve and hydraulic pressure are matched to the real aggregate sitting in your yard — [NEED_CITE: aggregate grading and moisture impact on concrete block compaction].
How the PLC Governs Every Egg-Laying Cycle
The QMY12-15 uses a PLC to sequence vibration, hydraulic pressure, and demold timing across each molding cycle. Rather than relying on an operator to judge when the block is ready, the controller follows a programmed profile, which means the 3200 Hz three-dimensional mold vibration is applied for the same duration on the first block of the shift and the last. For an automatic mobile block machine PLC controlled configuration, this repeatability is the difference between blocks that consistently meet the ≥ 15 MPa target and batches that fail a crush test at random.
Where Hydraulic Steering Intersects With Automation Logic
Automatic movement and hydraulic steering take the physical effort out of traversing the curing floor, but they also create a timing dependency the PLC must manage. The machine cannot start a new mold vibration cycle until it has reached the next lay position and settled. On uneven ground or a freshly poured floor with residual moisture, the travel speed fluctuates, and the controller must adjust dwell time before the next press to avoid misaligned rows — [NEED_CITE: floor flatness tolerance for egg-laying block machines].
Reading the Specification Sheet Without Getting Misled
The hydraulic system operates between 16 and 20 MPa, which is the force range that, combined with three-dimensional vibration, compacts the mix into a ≥ 15 MPa block. However, that pressure rating only delivers the promised strength if the mix moisture sits within a narrow window; too wet and the hydraulic squeeze pushes cement paste out of the cavity, too dry and the block crumbles on demold. The 16 kW total power figure covers vibration motors, hydraulic pump, and travel drive simultaneously, so running an undersized generator on-site will cause voltage sag during peak draw and leave the PLC faulting mid-cycle. Mould format determines output: 12 cavities per mould for a 400×200×200 mm hollow block yields 2880 pcs/h at a 15–20 s cycle, while switching to a 400×100×200 mm format with the same mould plate raises the figure to 5280 pcs/h — a different product entirely. Buyers comparing machines on hourly numbers alone are comparing a structural hollow block against a thin partition block.
The Cost of Ignoring PLC Language and Voltage Before Shipment
A control panel labeled in a language your operators cannot read turns every parameter adjustment into guesswork, and guesswork with 20 MPa hydraulic pressure produces cracked blocks and damaged moulds. Equally, a machine wired for a voltage and frequency that does not match your site supply will either refuse to start or, worse, run with degraded vibration amplitude, silently producing under-compacted blocks that fail weeks later in a wall — [NEED_CITE: voltage and frequency mismatch effects on electric motor performance].
Why Sourcing the QMY12-15 Through a Block-Line Specialist Matters
Block machinery is our only product category, so the QMY12-15 is never treated as a standalone press — its pallet handling, curing-rack workflow, and mould inventory are specified as one system. Machine configuration starts from your actual mix design and local aggregate, not from a catalogue default, which is why we ask for raw material samples before locking PLC parameters. Mould design covers the formats your market sells, and custom drawings are available when standard cavities do not match. Automation level is selectable: a buyer can begin with the semi-automatic QMY12-15 and plan a path toward fully automatic stacking later. Installation includes on-site commissioning and operator training so your crew understands the PLC interface before the first production shift.
Documentation & Verification
- Capacity calculation sheet stating block format, cycle time, and mould cavity count for every quoted output figure
- Hydraulic and electrical schematic matching the QMY12-15 as-built configuration
- Voltage, frequency, and PLC display language confirmation signed before dispatch
- Factory test record run on your specified raw material blend
- Mould drawing and format list for every cavity supplied
- Packing photographs and customs documentation support
Installation, Commissioning & Support
- Verify curing-floor flatness and load-bearing capacity for the 4200 kg machine weight and 3250 mm length
- Confirm site supply matches the agreed voltage and frequency before the 16 kW total load is energized
- PLC parameter set loaded and cycle timing verified against your mix during on-site commissioning
- Operator training covers mould change procedure, hydraulic steering operation, and PLC fault diagnosis
- Wear-part list and mould inventory reviewed so first replacements are on hand before production ramp-up
Before You Request a Quotation
Send us the exact block formats your market demands, the daily volume you need per format, and a sample of your local aggregate so we can confirm the QMY12-15 configuration against real material. Tell us your site voltage, frequency, and preferred PLC display language, along with whether your curing area uses pallets or direct floor laying, so the automation scope is defined before the quotation is issued.
Frequently Asked Questions
Q: How is the stated hourly output verified, and which block format is each figure based on?
A: Every capacity figure for the QMY12-15 is tied to a specific block dimension and cycle range. The 2880 pcs/h value assumes a 400×200×200 mm hollow block at a 15–20 s cycle; switching to a 400×100×200 mm partition block raises the number to 5280 pcs/h. We provide a written capacity sheet so buyers know which format drives which figure.
Q: What PLC brand and display language are installed, and can the HMI be configured locally?
A: The PLC brand and HMI language are confirmed during the pre-production review. Buyers specify their preferred interface language and we document it in the voltage and control confirmation sheet before dispatch, preventing commissioning delays caused by unreadable menus on site.
Q: What is the voltage and frequency configuration, and is it checked against our supply?
A: Voltage and frequency are agreed before production starts and recorded in the signed confirmation document. The QMY12-15 draws 16 kW total, so we also verify that the site transformer and cable sizing can sustain peak draw without voltage sag that would disrupt PLC logic.
Q: What automation is included versus what remains manual on the QMY12-15?
A: The QMY12-15 automates movement, hydraulic steering, vibration sequencing, and demold through the PLC. Pallet handling, stacking, and curing-rack transfer may remain manual at this tier. We map exactly which stations are automated and which are not so buyers can plan labor or a future upgrade path.