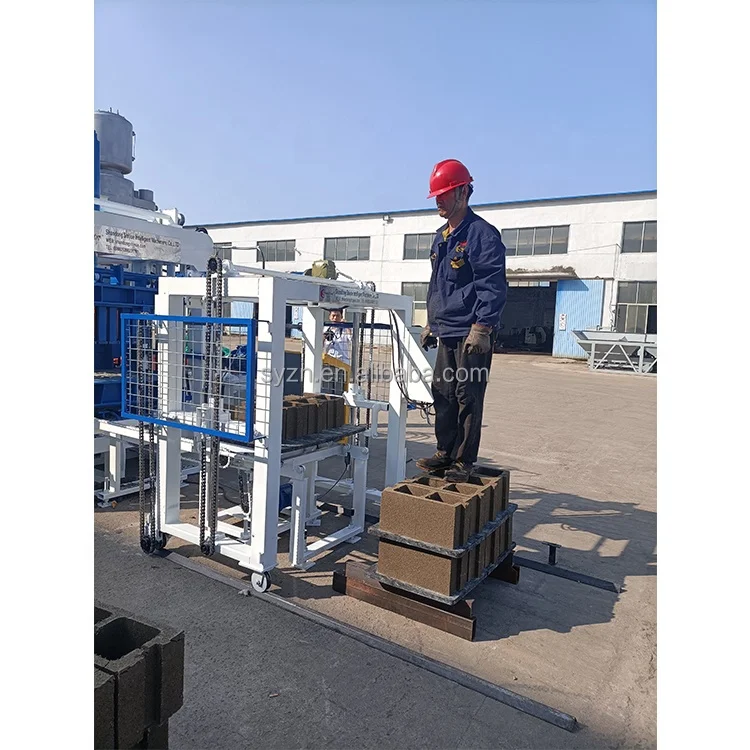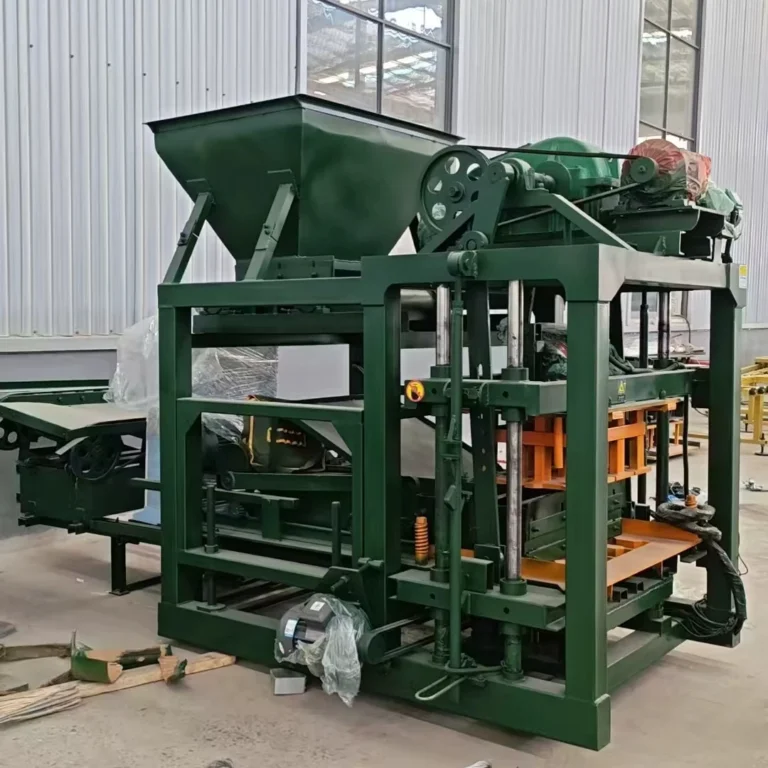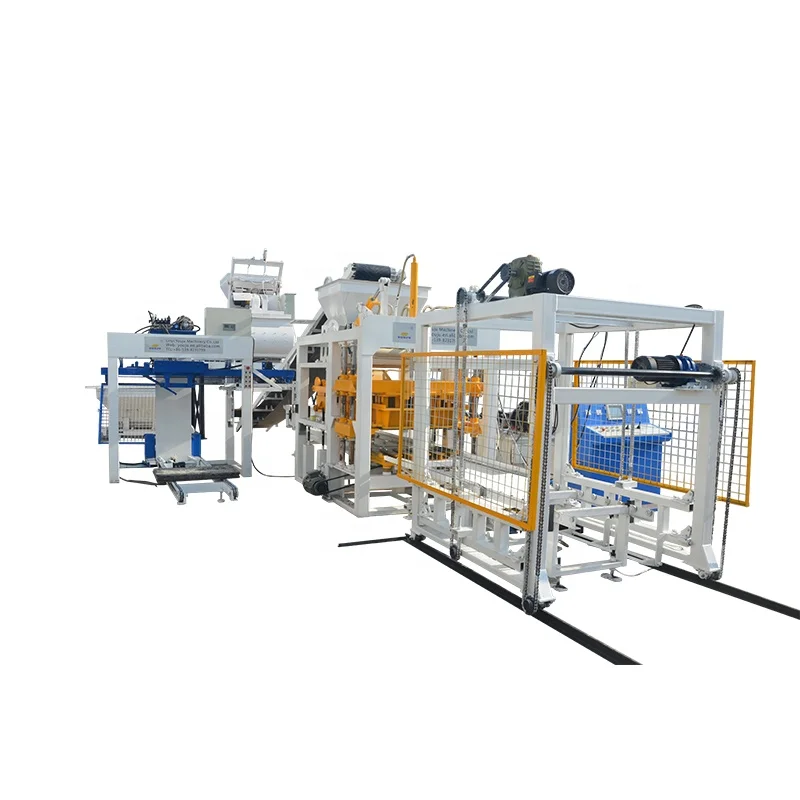
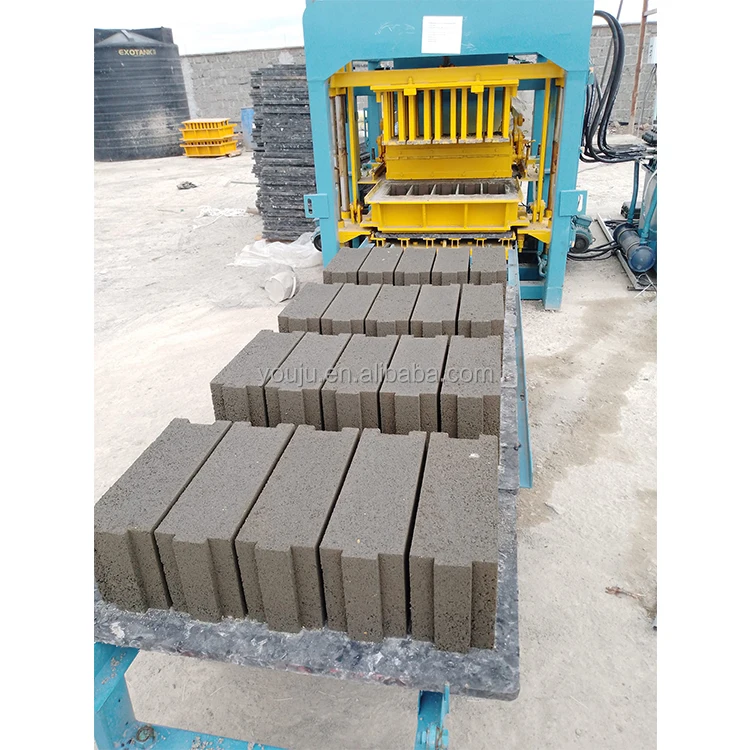

Description
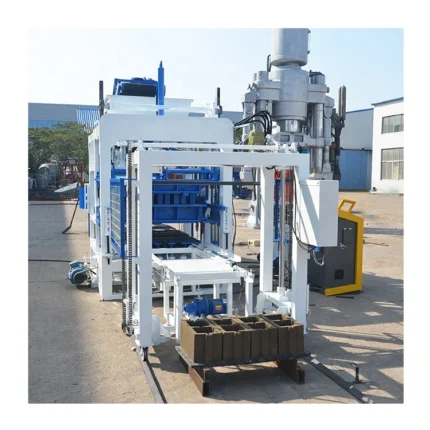
Computer-Controlled Vibration Management — The QT4-15 replaces manual timing guesswork with photoelectric hopper control and frequency-directed vibration, keeping block density consistent across every press cycle.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-15 |
| Product Type | Stationary Concrete Block Making Machine |
| Rated Power | 27.5 kW |
| Voltage & Frequency | 380V (frequency configurable to target market standard) |
| Control System | Computer controlled directional vibration with photoelectric material control |
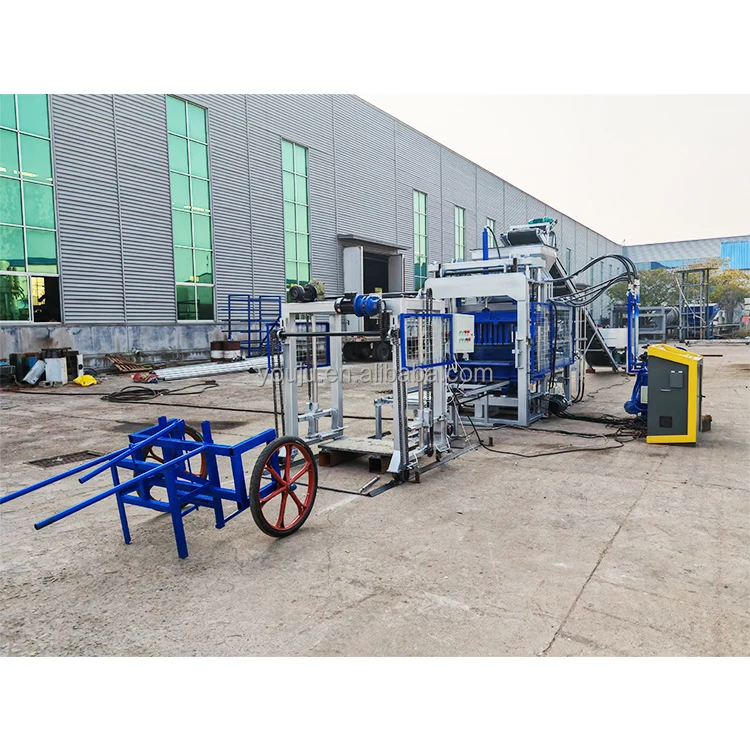
| Overall Dimensions (L×W×H) | 7100 × 1600 × 2610 mm |
| Net Weight | 5 T |
| Vibration Force | 40 kN |
| Pallet Size | 1020 × 570 mm |
| Moulding Cycle | 15 s |
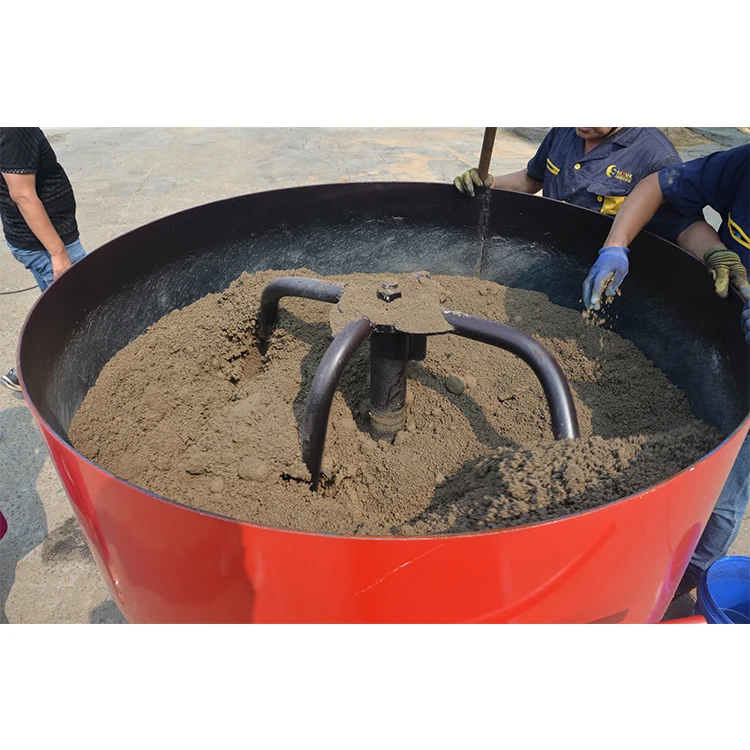
| Mixer Model | JS500 |
| General Water Consumption | 4 T/day |
| Workers Required | 3–4 |
| Workshop Area | 150 m² |
| Host Motor | Siemens Motor |
| Feeding System | Hopper with swing-type cutting device |
| Vibration Method | Table and mould vibrating together, low-frequency feeding / high-frequency vibrating |
| Automation Level | Semi-automatic with defined upgrade path available |
| Output Capacity | Basis to be confirmed per block format |
Application Suitability
| Application | Material or Output |
|---|---|
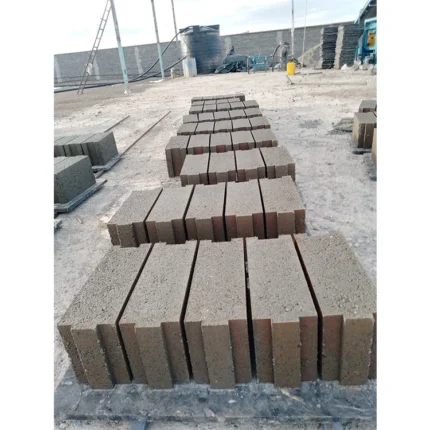
| Hollow block production | Crushed stone, sand, cement, and water mix |
| Solid block manufacturing | Dense aggregate blend for load-bearing masonry |
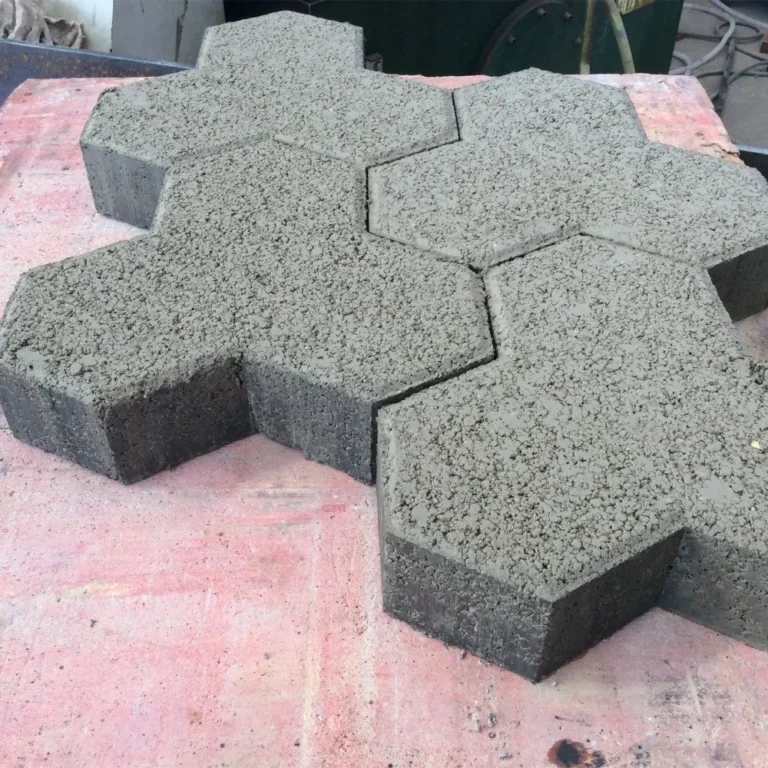
| Paving block production | Fine aggregate with pigment for interlocking or rectangular formats |
| On-site contractor production | Local aggregate sourced near the construction project |
Why the PLC Language Question Matters More Than the Price Tag
A control panel the operator cannot read turns an automatic QT4-15 block machine into a very expensive manual press.
I once spent two full days on a job site in West Africa because the PLC display defaulted to English while the local crew only read French. Every parameter adjustment required a translator standing by the HMI. The machine itself ran fine — the bottleneck was the language barrier between the operator and the computer controlling vibration frequency and hopper timing. When sourcing a PLC controlled stationary block machine, confirming the display language and voltage standard before production begins eliminates a problem that is entirely preventable yet surprisingly common [NEED_CITE: voltage and frequency standards by export market].
What the Computer Actually Controls on This Press
The QT4-15 uses photoelectric sensors to govern the hopper swing cycle. The cutting device inside the feed hopper meters material into the mould cavity based on detected fill level rather than a fixed timer. This matters because aggregate moisture and gradation shift from batch to batch — a timer-fed system overfills or underfills as conditions change, while photoelectric control adjusts the cut point to the actual material behaviour. The result is uniform layer weight across the pallet, which directly affects block height tolerance.
How Directional Vibration Removes Residual Energy
Standard table vibration sends shockwaves in all axes, and when the motor stops, residual energy continues to settle the mix unevenly. The computer-controlled directional vibration on this automatic QT4-15 block machine applies force along a single axis and engages a brake cancellation routine at cycle end. The brake stops the eccentric mass instantly rather than letting it coast down. This eliminates the micro-slump that occurs during spin-down, so the block leaves the mould at its pressed dimension rather than settling further before the pallet moves to the curing area [NEED_CITE: CE machinery directive requirements for industrial equipment].
Reading the Specs That Actually Shape Your Daily Output
The 40 kN vibration force paired with a 15-second moulding cycle means the concrete mix must liquefy and de-air within that window. If your local aggregate is angular crushed stone rather than rounded river gravel, the mix needs sufficient fines content to flow under vibration — otherwise the 40 kN force is wasted on friction between particles. The Siemens motor on the host drive delivers consistent torque through continuous start-stop cycling, which matters because a motor that loses torque under thermal load will shorten the effective vibration amplitude mid-shift. The 1020 × 570 mm pallet size defines your curing rack geometry; if your existing forklift and rack spacing were designed around a different pallet dimension, the mismatch compounds through every handling step downstream. The JS500 mixer capacity pairs with the press cycle to keep material flowing without the hopper running dry between batches.
The Hidden Cost of Unmatched Automation Components
A buyer once specified a semi-automatic press with a manual pallet return, assuming the labour savings on the stacking end would offset the slower cycle. What actually happened was the press completed its 15-second cycle, then sat idle while a worker hand-carried the finished pallet to the curing rack and returned an empty one. The computer-controlled vibration and photoelectric feeding delivered perfect consistency, but the line throughput dropped to whatever pace the slowest manual link allowed. When the automation level of individual stations is not specified as a matched sequence, the press capability becomes theoretical rather than actual [NEED_CITE: block plant automation mismatch case studies].
Why Sourcing Through This Channel Works for Automation Buyers
The machine, mould, pallet, and handling equipment are specified as a single system rather than assembled from independent suppliers, which means the PLC logic already accounts for the pallet feed timing and stacking sequence you will eventually add. Configuration is set against your actual mix design and local aggregate, not a catalogue default, so the vibration parameters loaded into the controller match the material you will actually press. Mould design covers the formats your market sells, and custom drawings are accepted when standard moulds do not fit your product range. The automation level is selectable at order and upgradable later — you can commission the QT4-15 as a semi-automatic press now and add automatic pallet feeding and stacking when volume justifies the investment. Installation support includes operator training on the specific PLC interface and control language confirmed at order.
Documentation & Verification
- Line layout showing station sequence and pallet flow path for your workshop dimensions
- Machine specification sheet with confirmed voltage, frequency, and PLC display language
- Mould drawing and format list covering the block types in your product catalogue
- Hydraulic and electrical schematic for independent local servicing
- Factory test record run on your specified block format before dispatch
- Packing photographs and customs documentation support for your import port
Installation, Commissioning & Support
- Foundation pad leveled to accommodate the 7100 × 1600 mm footprint with anchor bolt provisions
- Dedicated 27.5 kW circuit with voltage and frequency confirmed to your local grid standard before wiring
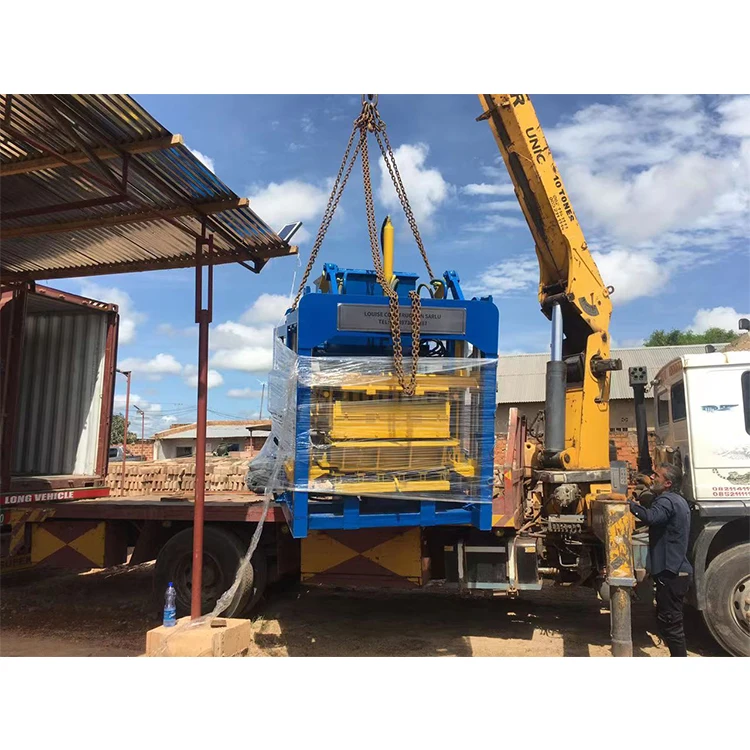
- Machine shipped dismantled with reassembly sequence documented in the operation manual
- First-run parameter tuning on your local aggregate mix with vibration frequency and feed timing adjusted on site
- Operator training covering PLC navigation, mould change procedure, and fault code interpretation in your confirmed language
- Wear parts list with hydraulic seal and vibration motor bearing part numbers for local sourcing
What to Prepare Before Requesting a Quotation
Provide the specific block formats you intend to produce, including dimensions and target compressive strength, so the mould configuration and vibration parameters can be matched to your product range. Share your local voltage and frequency standard along with the preferred PLC display language for your operators. Include your workshop dimensions and any existing curing rack or forklift specifications so the pallet handling layout integrates with equipment you already have on site.
Frequently Asked Questions
Q: How is the output capacity of the QT4-15 verified, and which block format is the calculation based on?
A: Capacity must be stated per specific block format with the moulding cycle assumption made explicit. A generic pieces-per-hour figure without naming the block dimensions and wall thickness is not a verifiable claim. We provide a capacity calculation sheet that names the exact mould, the cycle time applied, and the daily output based on your operating hours, so you can compare it against your production target before committing.
Q: What PLC brand and control language options are available, and can the HMI be set to the operator’s local language?
A: The PLC brand and HMI language are confirmed in writing before production begins. The interface can be set to your operator’s preferred language so that parameter adjustments and fault diagnostics do not require a translator on the shop floor. This confirmation step is built into the order process specifically because language mismatch is one of the most common commissioning delays we encounter in the field.
Q: Can the automation level be upgraded later from semi-automatic to include automatic pallet feeding and stacking?
A: Yes. The QT4-15 is designed with a defined upgrade path from semi-automatic computer-controlled pressing through to automatic pallet feeding, stacking, and cubing. The PLC architecture supports additional I/O modules, and the compatible component list for each upgrade stage is documented at the time of initial order so that future expansion does not require replacing the base controller.
Q: How does the computer-controlled vibration system adapt to different mix designs and local aggregates?
A: The vibration frequency and duration parameters in the PLC are adjustable to match your specific aggregate gradation and cement ratio. Angular crushed stone requires different de-airing time than rounded gravel, and the controller allows your technician to tune the low-frequency feed and high-frequency press stages independently. We recommend running a test batch with your actual material during commissioning to lock in the optimal settings.
Q: What voltage and frequency configurations are supported, and is this confirmed before shipment?
A: The standard configuration is 380V, and frequency is set to match your local grid standard. Both values are confirmed in writing during the order stage, along with the PLC display language, so that the machine arrives ready to connect to your existing electrical infrastructure without requiring a transformer or facing a language barrier at the control panel.