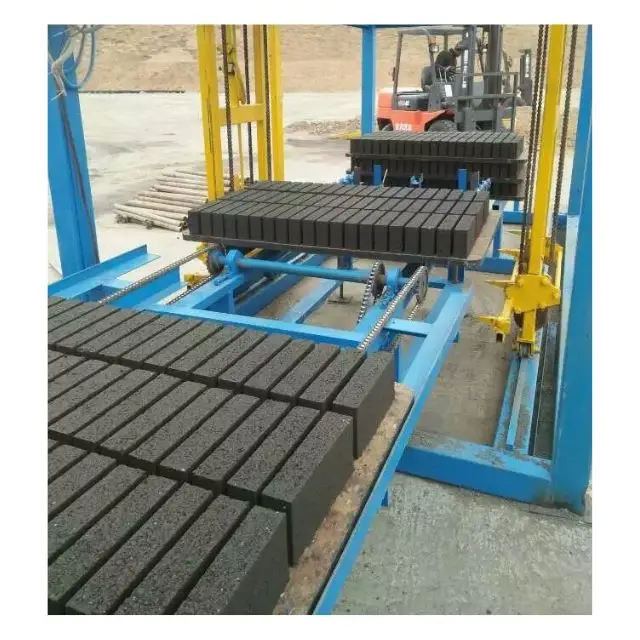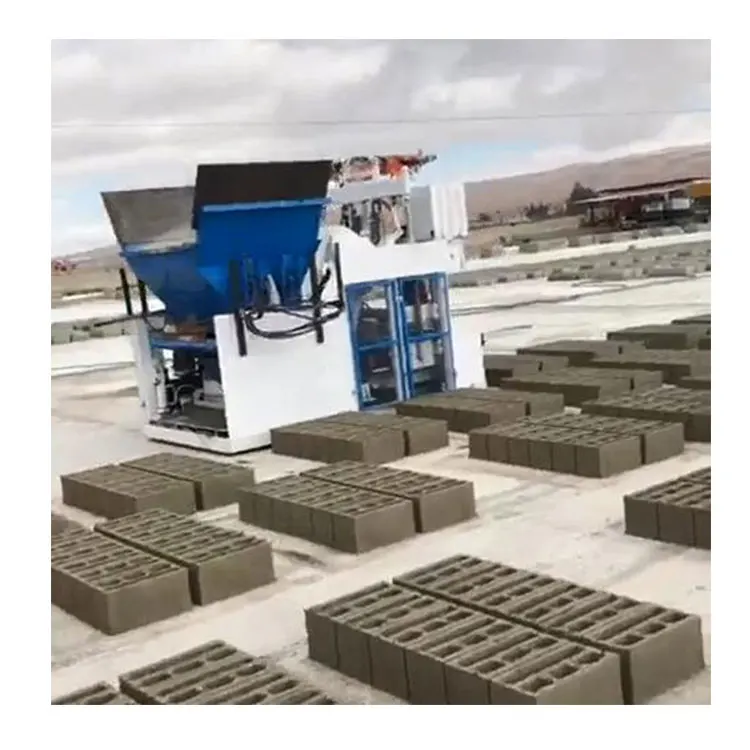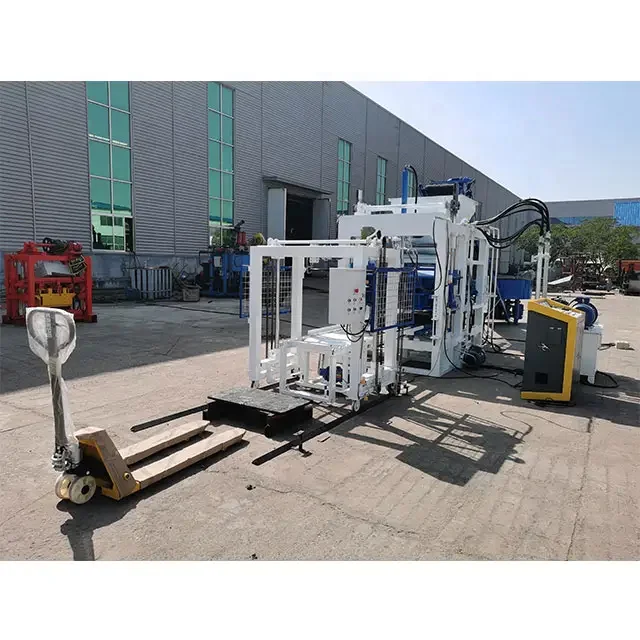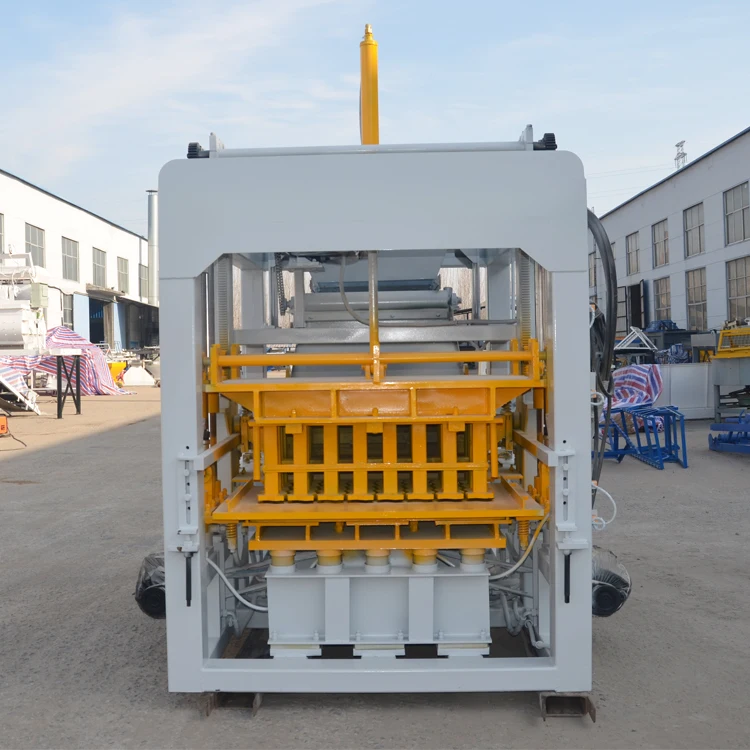


Description
PLC-Controlled Line Synchronisation — the QT5-15 is configured as one matched system where batching, pressing, pallet feeding and stacking operate on the same control logic rather than being assembled from separate suppliers.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT5-15 |
| Product Type | Automatic Concrete Block Making Machine |
| Dimension of Host Machine | 5870 × 2220 × 2850 mm |
| Weight of Host Machine | 5.5 Tons |
| Molding Area | 1050 × 500 mm |
| Workshop Area Required | 200 m² |
| Host Machine Power | 31.5 kW |
| Vibration Force | 55 kN |
| Vibration Frequency | 2800–4500 Times/Minute |
| Vibration Method | Hydraulic + Platform Vibration |
| Molding Period | 15 Seconds (basis to be confirmed per block format) |
| Pallet Size | 1100 × 550 × 25 mm |
| Voltage | 220/380/415/440V (Customized) |
| Control System | Original Siemens PLC with independently developed control program |
| Travel Switch | France Schneider and Japan Omron |
| Motor | Germany SIEMENS or CE standard brand |
| Mould Treatment | Heat treatment and carburizing, hardness 54–58 HRC, lifespan >100,000 cycles |
| Welding | Carbon dioxide protection welding |
| Batching Machine (PLD1200) | 1200L weigh-batching hopper, 4×2.5 m³ storage, ±2% ingredient precision, 56 m³/h theoretical productivity |
| Concrete Mixer (JS500) | 500L discharging volume, 25 m³/h production capacity, 18.5 kW mixing motor, max aggregate 60 mm |
| Stacker (SY-4) | 3 kW, mobile pallet stack, suitable for hollow block and pavers |
| Assembly State | Grouped equipment line (batching + mixing + press + stacker) |
| Standards | CE (materials and spare parts selected per international CE standards) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for residential and commercial walls | Crushed stone, sand, cement, and fly ash aggregates |
| Interlocking brick production for paving and landscaping | Fine aggregate with cement binder, dry-mix consistency |
| Solid block manufacturing for load-bearing structures | Coarse and fine aggregate blends, standard cement ratios |
| Paving brick production for driveways and walkways | High-density mix with colour oxide additives where required |
| On-site block production for housing and development projects | Locally sourced aggregate matched to regional supply |
What the 15-Second Moulding Period Actually Means for Your Daily Output
Cycle time is meaningless without the block format attached to it.
Many quotations list a single cycles-per-hour figure that assumes an ideal mould, a standard hollow block, and perfect material flow. In practice, a 15-second moulding period on the QT5-15 automatic concrete block making machine PLC controlled system applies to a specific format under specific conditions. Switch to a taller interlocking paver or a porous brick with a more complex cavity pattern, and the vibration dwell alone extends the cycle. I once spent three days on site adjusting parameters because the buyer’s aggregate had a higher clay content than the lab sample we tested against, and the actual output settled well below the catalogue figure. [NEED_CITE: effect of aggregate clay content on concrete block cycle time]
How PLC Synchronisation Eliminates Press Idle Time
The independently developed control program running on the Siemens PLC coordinates the batching hopper discharge, mixer cycle, pallet feed, and press operation as one sequence. When the mixer finishes a batch, the PLC already knows whether the press is ready or still completing a vibration cycle, and it holds or releases material accordingly. This is where an automatic concrete block making machine PLC controlled architecture shows its value — not in faster individual stations, but in fewer moments where the press sits empty waiting for concrete or pallets.
Vibration and Hydraulic Pressure Working as One System
The QT5-15 delivers 55 kN of vibration force through a combined hydraulic and platform vibration method, operating between 2800 and 4500 cycles per minute. The hydraulic pressure compresses the mix while the platform vibration settles fine particles into voids. If your local aggregate is angular crushed stone rather than rounded river gravel, the vibration frequency needs to sit at the higher end of the range to achieve proper consolidation. [NEED_CITE: vibration frequency selection for different aggregate shapes in block production] Getting this wrong produces blocks with inconsistent density across a single pallet.
Reading the Specifications That Actually Matter
The 1100 × 550 × 25 mm pallet size determines how many blocks are pressed per cycle and must match the curing rack spacing and forklift tine width the buyer already uses on site. The ±2% ingredient precision from the PLD1200 batching machine ensures that cement content stays consistent across batches, which directly affects block compressive strength. The mould carburising treatment to 54–58 HRC hardness means the mould surface resists abrasion from angular aggregate far longer than untreated steel, and the rated lifespan exceeds 100,000 press cycles before replacement is needed. A 200 m² workshop area covers the host machine, pallet circulation, and a basic curing zone but does not include raw material stockpiling.
The Cost of Skipping Voltage and Language Confirmation
Buyers who do not confirm voltage, frequency, and PLC display language before production starts face delays the moment the machine arrives. A 380V/50Hz machine shipped to a 440V/60Hz market will not run correctly on the installed transformer, and the PLC menu in a language the operator cannot read turns commissioning into a guessing exercise. [NEED_CITE: voltage and frequency standards by export market] These issues are entirely avoidable but appear on site with regular frequency.
Why Sourcing the Full Line From One Supplier Changes the Outcome
Block machinery as a single focus means the QT5-15 press, PLD1200 batching machine, JS500 mixer, and SY-4 stacker are specified together against your actual mix design and target block format, not pulled from separate catalogues. The mould is designed and supplied for the formats your market sells, including custom drawings if your buyers need a cavity pattern or interlocking profile that is not standard. Automation level is selectable, so a buyer can start with semi-automatic pallet handling and add the full stacking and cubing system later without replacing the press. Configuration is set against your local aggregate and target strength, not a default that assumes materials you cannot source. Installation and commissioning include operator training on the specific PLC program loaded into your machine.
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed for the QT5-15 cycle time
- Mould drawing and format list matching your target interlocking, hollow, paving, or solid brick profiles
- Hydraulic and electrical schematic with confirmed voltage and PLC display language
- Factory test record on your specified mix design before dispatch
- Pallet specification confirming dimensions and material against your curing rack and forklift
- Wear parts and mould list with first replacement cycle clearly documented
Installation, Commissioning & Support
- 200 m² workshop floor must be level and cured to support the 5.5-ton host machine and vibration loads
- Dedicated electrical circuit sized for 31.5 kW host plus 18.5 kW mixer, voltage confirmed before wiring
- Equipment arrives as grouped line; batching, mixer, press, and stacker assembled and aligned on site
- First-run parameter tuning matches vibration frequency and hydraulic pressure to your local aggregate
- Operator training covers the Siemens PLC program, mould change procedure, and daily maintenance checkpoints
- Mould wear parts list provided with recommended first replacement interval at 100,000 cycles
What to Prepare Before Requesting a Quotation
Provide your target block format with dimensions, the daily output you need for that specific format, and a sample or analysis of your local aggregate including moisture and clay content. Confirm your site voltage, frequency, and preferred PLC display language so the electrical and control package is correct before production begins.
Frequently Asked Questions
Q: How is realistic daily output calculated per block format, and what does the 15-second cycle time assume?
A: The 15-second moulding period applies to a specific block format under defined material conditions. Realistic daily output is calculated by multiplying the cycle rate for your exact mould, subtracting pallet exchange and mould repositioning time, and factoring in mixer batch intervals. We provide a written capacity calculation per format with the quotation, not a single headline figure.
Q: What PLC control language and voltage configurations are confirmed before shipment?
A: The Siemens PLC display language, voltage, and frequency are confirmed during the quotation stage and documented before production. The control program can be localised to the operator’s language, and all electrical components including travel switches and motors are selected to match the confirmed supply specification.
Q: How does the automation level scale from semi-automatic to full stacking and cubing?
A: The QT5-15 line can start with manual pallet handling after pressing and add the SY-4 automatic stacker at any point without modifying the press or PLC. Further upgrades to full cubing and curing rack handling are configurable. The PLC program is written to accept additional station inputs when automation stages are added later.
Q: How are batching accuracy and vibration parameters matched to the buyer’s local aggregate?
A: The PLD1200 batching machine delivers ±2% ingredient precision, and vibration frequency is adjustable between 2800 and 4500 cycles per minute. We request your aggregate analysis — including particle size distribution, clay content, and moisture — and set the vibration and hydraulic pressure parameters to match. Factory testing runs your specified mix before dispatch.
Q: What installation, operator training, and remote diagnostics support is provided after commissioning?
A: On-site installation covers machine alignment, electrical connection to your confirmed voltage, and first-run parameter tuning. Operator training addresses the PLC interface, mould change procedure, and daily maintenance. The Siemens PLC platform supports remote diagnostics where site connectivity allows, and a documented wear parts list guides the first replacement cycle.