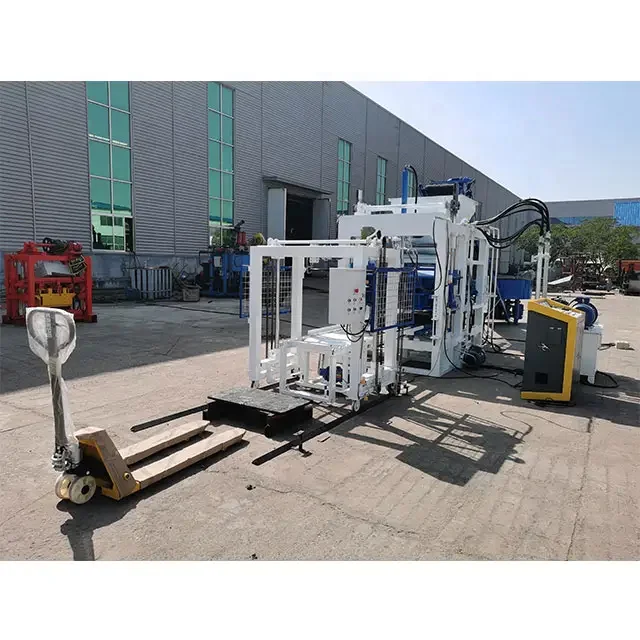
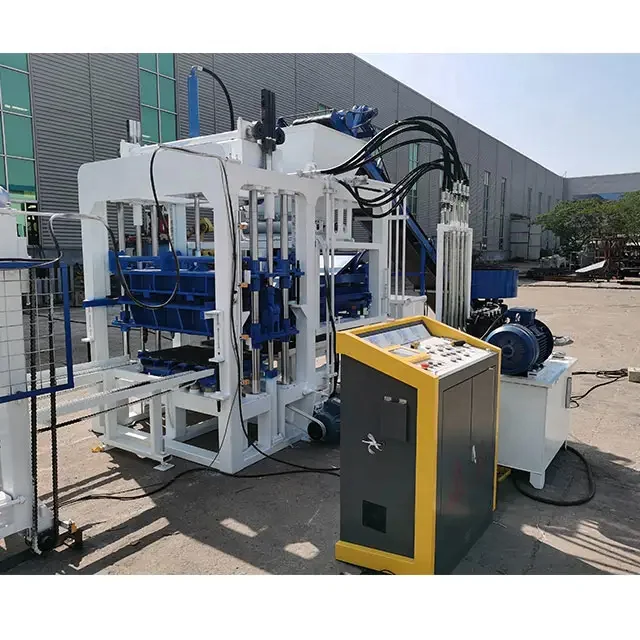


Description
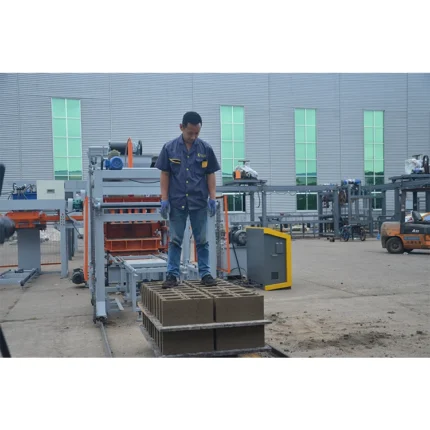
Integrated Line Control — PLC logic, pallet handling, and press cycle are configured as one matched system so the automation removes real operator tasks instead of creating gaps you still fill by hand.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-18 |
| Product Type | Automatic Concrete Block Making Machine |
| Overall Dimensions | 2500×1750×2200 mm |
| Rated Pressure | 16 MPa |
| Vibration Form | Platform Vibration |
| Pallet Size | 950×550 mm |
| Molding Cycle | 18–25 s (basis not stated in source — confirm block format / material / thickness) |
| Overall Power | 27.5 kW |
| Control System | PLC with frequency converter, machine-to-person interface |
| Electrical Components | Schneider (international brand) |
| Mold Lifting Mechanism | Double-sided synchronous gears |
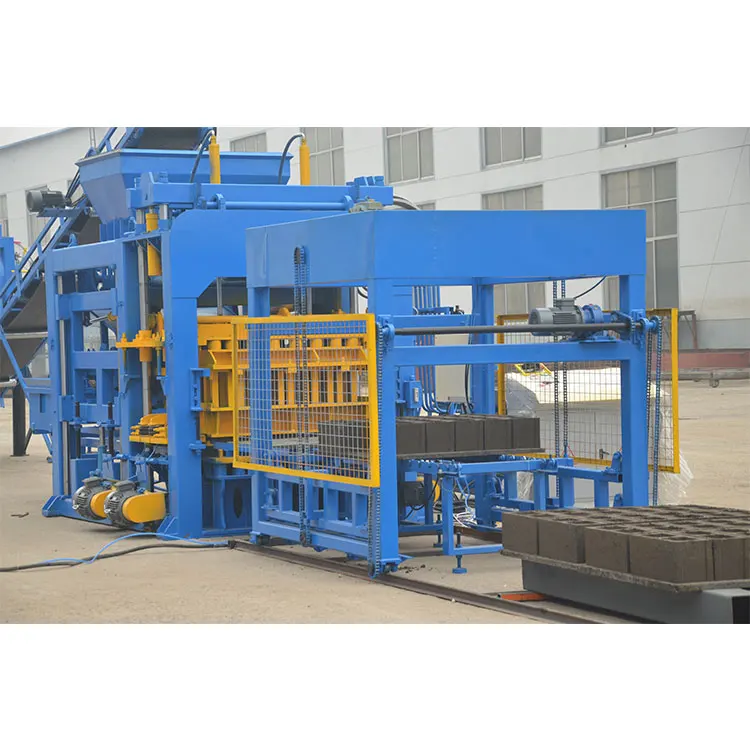
| Material Feeder System | Hopper, feeding box, feeding platform, conveyor system |
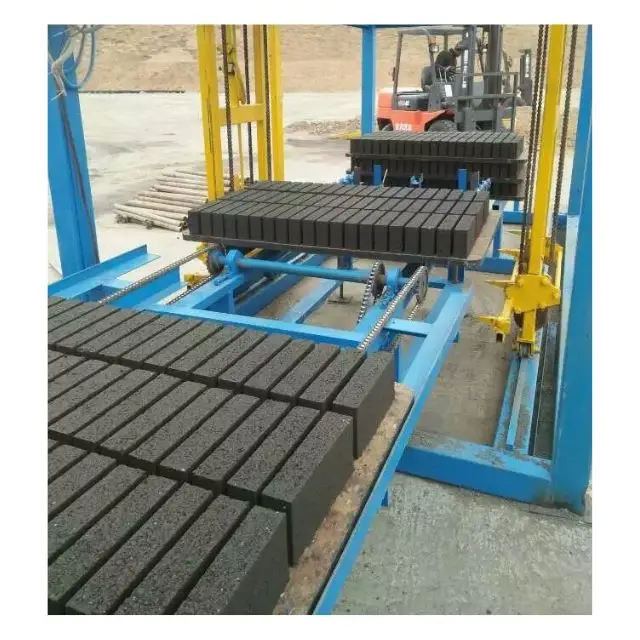
| Block Receiver | Frame, conveyor system, idler wheels, motor and reducer with triangle belt |
| Automation Level | Automatic (pallet feeder driven by hydro-cylinder, automatic demould and pallet cycling) |
Application Suitability
| Application | Material or Output |
|---|---|
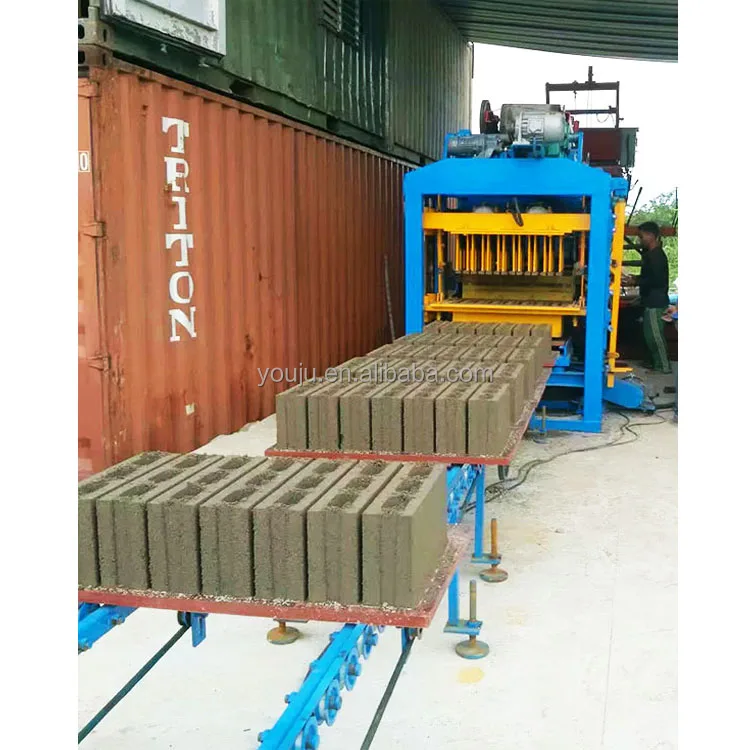
| Hollow block production | Crushed stone, cement, sand, and water mix with standard aggregate grading |
| Solid block manufacturing | Dense concrete mix for load-bearing masonry units |
| Paving block and kerbstone | High-strength concrete with fine aggregate and pigment addition |
| Interlocking and porous brick | Specialized mix designs requiring precise moisture control and vibration |
What "PLC Controlled" Actually Means on the Shop Floor
An automatic concrete block making machine PLC controlled system only reduces labour when the pallet feeder, press cycle, and conveyor logic are written to talk to each other.
Too often, the PLC on a block machine simply sequences the press while pallets are still loaded by hand and finished blocks are stacked manually at the end of the line. The operator ends up watching a screen that tells them the machine is running, yet they are still doing the heaviest work. [NEED_CITE: automation gaps in semi-automatic block lines] The QT4-18 ties the hydro-cylinder pallet feeder directly to the demould cycle, so the press is never left idle waiting for the next board. That is the difference between a machine that has a PLC and a line that actually runs on one.
How the Control Logic Removes the Operator from Repetitive Tasks
The frequency converter in the QT4-18 control cabinet smooths motor starts and stops, which means the pallet feeder does not jerk the board into position and the press does not shock-load the hydraulic circuit. Each movement is ramped, timed, and interlocked through the PLC. When the automatic concrete block making machine PLC controlled sequence is set correctly, the operator’s job shifts from feeding and pulling pallets to monitoring mix consistency and checking block dimensions at the conveyor exit.
Where Automation Ends and the Operator Still Steps In
The QT4-18 automates pallet feeding, press cycling, and demould, but the upstream mixer, belt conveyor loading, and downstream stacking still require decisions. [NEED_CITE: labour allocation in block production lines] If the mixer batch is too dry, the PLC cannot compensate — it will press a weak block at the same cycle time. The operator must watch the mix, adjust water at the pan mixer, and decide when a worn mold needs rotation. Automation handles rhythm; material judgment stays human.
Pressure, Vibration, and What They Decide Together
The 16 MPa rated pressure works with platform vibration to compact the concrete mix inside the mold cavity. Pressure alone would leave air pockets; vibration alone would not consolidate the surface. The double-sided synchronous gear mold lifting mechanism ensures the mold box drops and lifts square every cycle, which directly affects block dimensional repeatability across a shift. With 27.5 kW total power, the vibration motors and hydraulic pump run without competing for current, provided the supply circuit is sized correctly. The 950×550 mm pallet size defines the maximum block arrangement per cycle — and that pallet must match the curing racks and forklift tines already on your site.
The Cost of Skipping the Voltage Conversation Before Shipment
We once shipped a PLC-controlled line where the HMI language defaulted to Chinese and the voltage was set for 380V/50Hz while the site ran 415V/60Hz. The commissioning technician arrived, powered up, and the screen went black. Three weeks of waiting for a reflash and a step-down transformer before the first block was pressed. [NEED_CITE: commissioning delays from unconfirmed voltage and PLC language] Confirming the local supply standard, the operator’s language, and the frequency converter settings before the cabinet is wired avoids a problem that no amount of on-site troubleshooting can fix quickly.
Why Buyers Source This Press Through Shiyue
Block machinery is the single focus here, so the QT4-18 press, mold, pallet, and handling equipment are specified as one matched set rather than assembled from unrelated suppliers. Configuration is set against your actual mix design, local aggregate, and target block format, not pulled from a catalogue default. Molds are designed and built for the formats your market sells, with custom drawings when standard formats do not cover your needs. The automation level is selectable — start with the automatic pallet feeder and add stacking or cubing modules later as volume grows. Installation support includes operator training so the PLC interface and mold change procedure are understood before the first production shift.
Documentation & Verification
- Line layout drawing with capacity calculation stated per block format and cycle time
- Machine specification sheet confirming pallet size, pressure rating, and power draw
- Hydraulic and electrical schematic for your local electrician and maintenance team
- Voltage, frequency, and PLC display language confirmation signed before production
- Factory test record showing press cycle and pallet feeder timing on your chosen mold
- Operation and maintenance manual with wear parts list and mold change procedure
Installation, Commissioning & Support
- Poured cement foundation per installation drawing before the QT4-18 arrives on site
- Dedicated electrical circuit matching confirmed voltage and frequency for the 27.5 kW load
- Press shipped partially dismantled for container loading, reassembled on foundation
- PLC language and HMI interface verified at power-up during commissioning visit
- Operator training covers mold change, pallet feeder adjustment, and daily lubrication points
- Wear parts and spare mold list provided for first replacement ordering
What to Send with Your Inquiry
Provide your target block format and dimensions, the daily output you need to hit, and the local aggregate and cement you will source. Confirm the site voltage, frequency, and the language your operator reads. Let us know if you already have a mixer, curing racks, or a forklift so the pallet size and conveyor length can be matched to what is already there.
Frequently Asked Questions
Q: How do I verify the actual output of the QT4-18 for my block format?
A: The 18–25 second molding cycle is a range, not a fixed number. Actual cycle time depends on your block dimensions, wall thickness, and concrete mix stiffness. Ask for a capacity calculation that names the specific block format used as its basis, so the daily output figure matches what your market actually buys rather than the fastest possible press cycle.
Q: Can I run the QT4-18 on a 60 Hz power supply?
A: The machine can be configured for different voltage and frequency standards, but this must be confirmed before the electrical cabinet is built. A 60 Hz supply changes motor speeds and vibration frequency, which affects both the PLC timing parameters and the hydraulic pump output. Lock in your site electrical spec during the quotation stage, not after dispatch.
Q: What does the automatic concrete block making machine PLC controlled system actually handle?
A: On the QT4-18, the PLC manages pallet feeding via hydro-cylinder, press cycle timing, vibration duration, mold lifting through the synchronous gears, and demould sequencing. Upstream mixing, raw material batching, and downstream stacking are separate decisions. The automation removes the operator from the press rhythm but not from material judgment or end-of-line handling.
Q: How long does a mold change take on this press?
A: Mold change time depends on the mechanism and how familiar your operator is with the procedure. The double-sided synchronous gear system on the QT4-18 keeps the mold box aligned during lifting, which reduces adjustment after a swap. Plan for a first shift dedicated to training your team on the change sequence so production changeovers stay predictable.
Q: What happens if the PLC screen language does not match my operator?
A: The HMI displays all machine parameters, fault codes, and cycle settings. If the language is wrong, your operator cannot read alarms or adjust timing, which stalls production until the system is reflashed. Specify the required display language during the order confirmation so the PLC is programmed correctly before the machine leaves the factory.