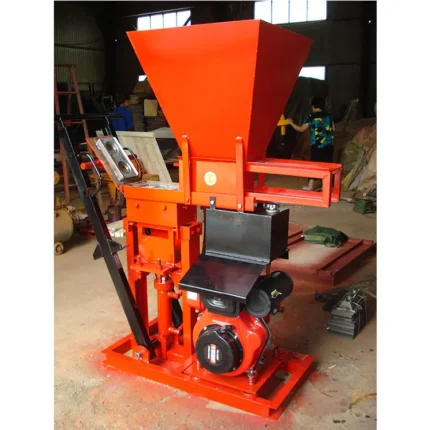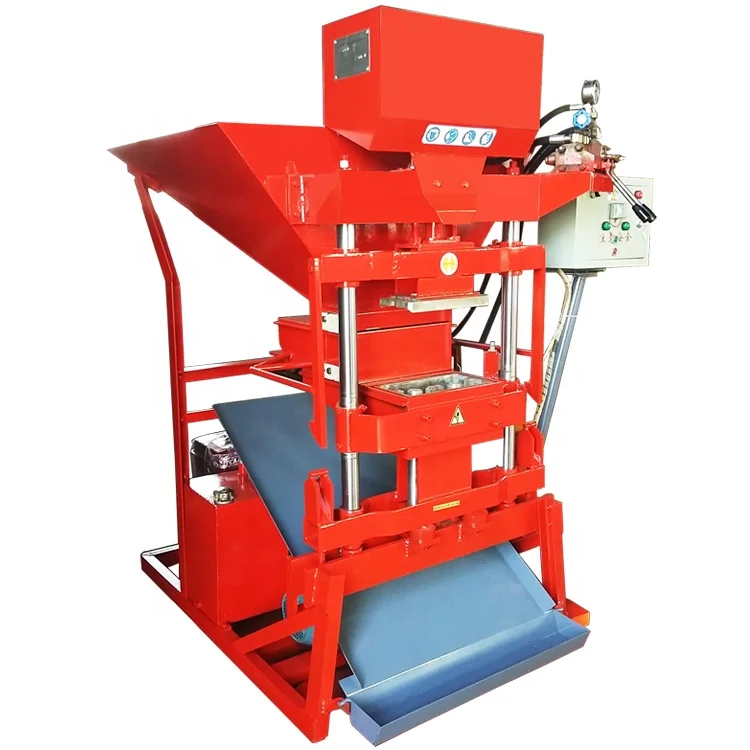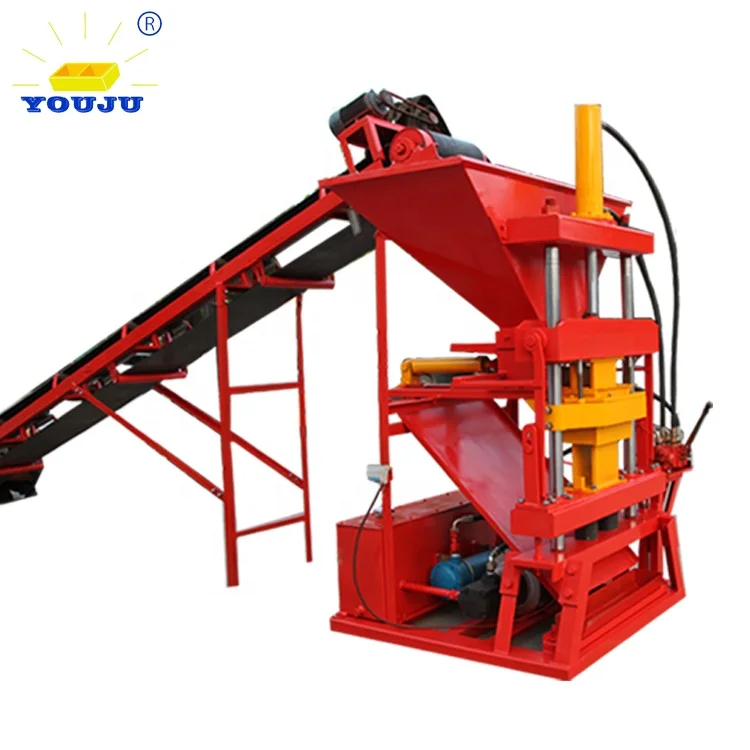
Description
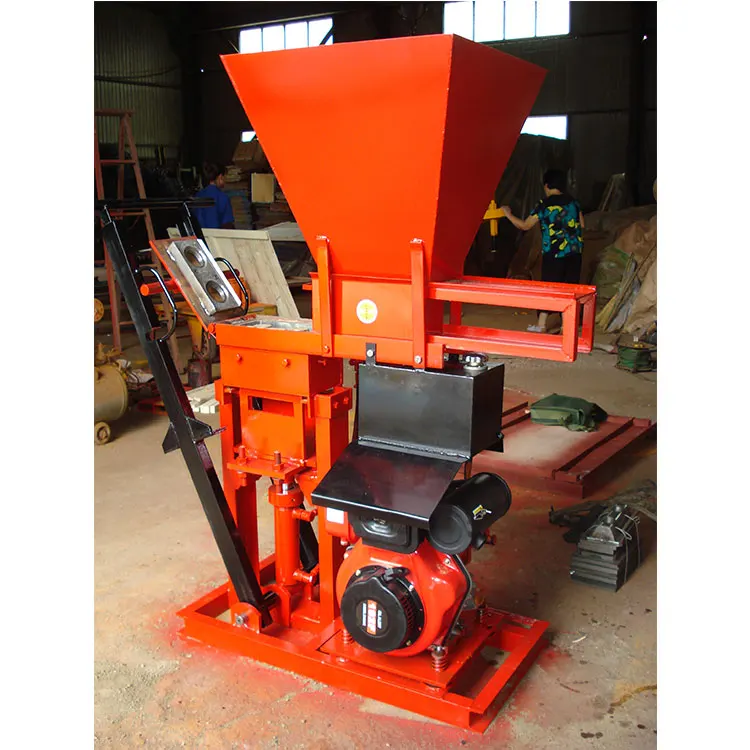
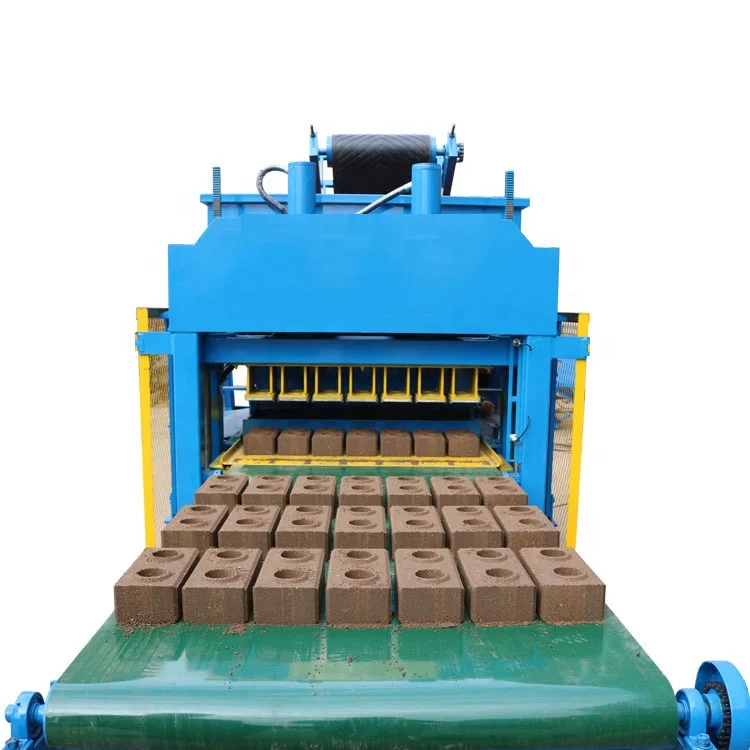
Integrated System Matching — Every LY7-10 dispatch pairs the clay interlocking brick press with the mould, pallet and control language confirmed against your actual site conditions, not a catalogue default.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | LY7-10 |
| Product Type | Automatic Clay Brick Making Machine |
| Machine Power | 18.5 kW |
| Hydraulic Pressure Range | 25 – 32.5 MPa |
| Molding Cycle | 10 – 15 seconds |
| Output Capacity | 2,520 pcs/hour (based on 300×150×100 mm interlocking brick, 7 pcs/mould) |
| Daily Capacity | 20,160 pcs/day (based on 300×150×100 mm interlocking brick, 7 pcs/mould) |
| Raw Materials | Laterite, yellow or red soil, sand, cement, water |
| Automation Level | Automatic (material feeding, mould pressing, mould lifting) |
| Worker Requirement | 1 – 2 operators |
| Overall Dimensions | 2,260 × 1,500 × 2,380 mm |
| Machine Weight | 1,600 kg |
| Control System | PLC-based automatic operation (brand and language to be confirmed) |
| Voltage & Frequency | Configurable to site supply (to be confirmed) |
| Pallet Size | To be confirmed based on curing area and handling setup |
Application Suitability
| Application | Material or Output |
|---|---|
| Interlocking brick production for load-bearing walls | Laterite and red soil blended with cement |
| Stabilized soil block manufacturing | Yellow soil, sand and cement mixes |
| On-site brick production for housing projects | Locally sourced laterite with cement stabilization |
| Clay paver and format brick runs | Red soil and sand blends for decorative masonry |
Why the Control Panel Language Must Be Decided Before Crating
A PLC screen in the wrong language turns commissioning day into a standstill.
I have stood on a job site where an automatic clay interlocking brick machine PLC controlled sat idle because the operator could not read the alarm codes on the HMI. The machine was mechanically sound. The problem was a language mismatch that nobody checked before the crate left the factory floor. That delay cost the contractor days of lost production and required a specialist to reflash the system on site. [NEED_CITE: PLC display language and localization requirements for export machinery]
Every control parameter — from hydraulic pressure set-points to mould cycle timing — is accessed through that screen. When the text is unreadable, the automatic material feeding, mould pressing and mould lifting sequences cannot be adjusted or troubleshooted by local staff. Confirming the PLC display language and HMI layout against the operator’s working language is a ten-minute conversation that prevents a multi-week delay.
How Automation Removes Cycle-to-Cycle Variation
The LY7-10 handles material feeding, mould pressing and mould lifting as one coordinated sequence. Each cycle follows the same timing, pressure application and release pattern regardless of operator fatigue or shift changes. This is where batch-to-batch consistency originates — not from a single component, but from removing manual intervention at every step of the press cycle. The 10–15 second molding cycle holds steady across a full production shift.
What PLC Coordination Means for Brick Density
Hydraulic pressure between 25 and 32.5 MPa is applied with consistent timing against the clay-soil-cement mix. The PLC coordinates the pressure build-up, hold time and release in relation to the mould position, so each interlocking brick receives the same compaction force. When pressure and cycle are manually controlled, density drifts as operators compensate for material variations by feel. The automatic sequence eliminates that drift, giving you bricks that stack true and meet the strength specification your market demands. [NEED_CITE: hydraulic pressure and cycle consistency effects on soil-cement block compressive strength]
Reading the Specification Sheet Against Your Mix Design
The hydraulic pressure range of 25–32.5 MPa must be matched to the laterite, red soil or yellow soil you actually source. A higher clay content requires different pressure than a sand-heavy mix to achieve the same interlocking brick density without surface cracking. The 18.5 kW power rating drives the hydraulic pump and vibration system simultaneously; if your mix demands sustained high pressure, the duty cycle of the motor must be verified against continuous shift operation. Molding cycles of 10–15 seconds define throughput only when paired with a specific mould — the 300×150×100 mm format at 7 pieces per mould gives the stated 2,520 pieces per hour, but switching to a larger interlocking format changes that number. Pallet size is not a minor detail: it determines how many bricks cure per rack and must align with the forklift and curing space you already operate.
The Cost of Skipping the Voltage and Frequency Check
Buyers who confirm voltage only after the machine arrives face a choice between running step-down transformers permanently or rewinding the main motor. The 18.5 kW drive on the LY7-10 is configured for a specific voltage and frequency combination — typically 380V/50Hz or 440V/60Hz for export markets. A mismatch does not simply reduce performance; it causes the motor to overheat, the PLC to fault, and the hydraulic pump to deliver inconsistent pressure. [NEED_CITE: voltage and frequency standards by export market] The electrical schematic must document the exact configuration so your electrician can prepare the supply circuit and dedicated breaker before the machine is uncrated.
Why This Machine Is Specified as a System
The LY7-10 is configured against the buyer’s actual mix design, local aggregate and target brick format rather than shipped as a catalogue default. Machine, mould, pallet and handling are specified as one matched set, so the press is not waiting on a mismatched pallet feeder or an undersized mixer. Mould design covers the interlocking formats your market sells, including custom profiles drawn to your specifications. Automation level is selectable — a buyer can start with the automatic press sequence and add stacking or cubing automation as production volume grows. Installation support includes operator training on the PLC, hydraulic adjustments and mould change procedure.
Documentation & Verification
- Line layout showing LY7-10 placement within the clay brick production workflow
- Capacity calculation sheet stating the 300×150×100 mm interlocking brick format assumed
- Machine specification sheet with confirmed voltage, frequency and PLC language
- Mould drawing and format list for each interlocking profile included in the order
- Hydraulic and electrical schematic matching the as-built LY7-10 configuration
- Factory test record on your laterite or red soil mix before dispatch
Installation, Commissioning & Support
- Foundation plan sized to the 2,260 × 1,500 mm footprint and 1,600 kg weight of the LY7-10
- Dedicated 18.5 kW circuit with voltage and frequency verified against your local supply
- Machine arrives as a single unit; hydraulic connections and PLC are pre-wired for faster hook-up
- On-site commissioning includes hydraulic pressure calibration against your actual soil-cement mix
- Operator training covers PLC navigation, alarm response and mould change procedure
- Wear parts list with recommended stock levels for hydraulic seals and mould components
What We Need to Configure Your LY7-10 Correctly
Send us the interlocking brick dimensions and profile your market requires, along with a sample or lab analysis of your locally sourced laterite or red soil. We need your site voltage and frequency, the preferred PLC display language, and the curing area dimensions so we can match pallet size to your existing handling equipment. If you are integrating the LY7-10 into an existing line, share the upstream mixer output rate and downstream stacking method so the cycle timing aligns.
Frequently Asked Questions
Q: How is the 2,520 pieces per hour capacity verified and which block format does it assume?
A: That figure is based on the 300×150×100 mm interlocking brick with 7 pieces per mould and a 10–15 second molding cycle. Any change in brick dimensions or mould cavity count alters the hourly output. We provide a capacity calculation sheet that states the exact format assumed, so there is no gap between quoted and achievable throughput on your chosen brick profile.
Q: What PLC brand and display language are installed, and can they be changed before shipment?
A: The PLC brand and HMI language are confirmed with you during the quotation stage and set before the machine leaves the factory. We document the selected brand and language on the electrical schematic. Changing either after arrival requires a specialist visit and system reflashing, so we lock these details down early in the sales process.
Q: How do I confirm voltage, frequency and control panel layout for my country?
A: We confirm your site supply voltage and frequency — typically 380V/50Hz or 440V/60Hz for export — and match the LY7-10 motor winding and PLC power supply accordingly. The control panel layout and button labeling are documented in the electrical schematic sent for your approval before production begins.
Q: What is the mould change procedure and can I run multiple interlocking formats?
A: The LY7-10 can run multiple interlocking formats by changing the mould. We provide the mould drawing and change procedure for each profile ordered. Change time depends on the mould size and fastener arrangement; we confirm this for your specific configuration so you know the format flexibility before committing.
Q: How is hydraulic pressure matched to my local laterite or red soil mix for target brick strength?
A: The 25–32.5 MPa hydraulic range is set during commissioning based on a test run with your actual soil-cement mix. We adjust pressure and hold time until the bricks meet the compressive strength and dimensional tolerance your market requires, then lock those values in the PLC so every subsequent cycle repeats them.