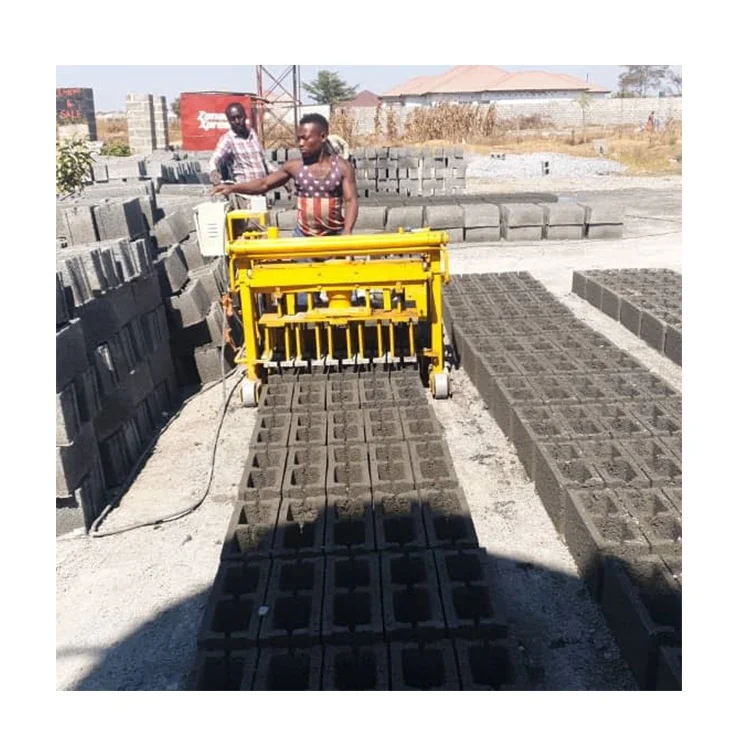
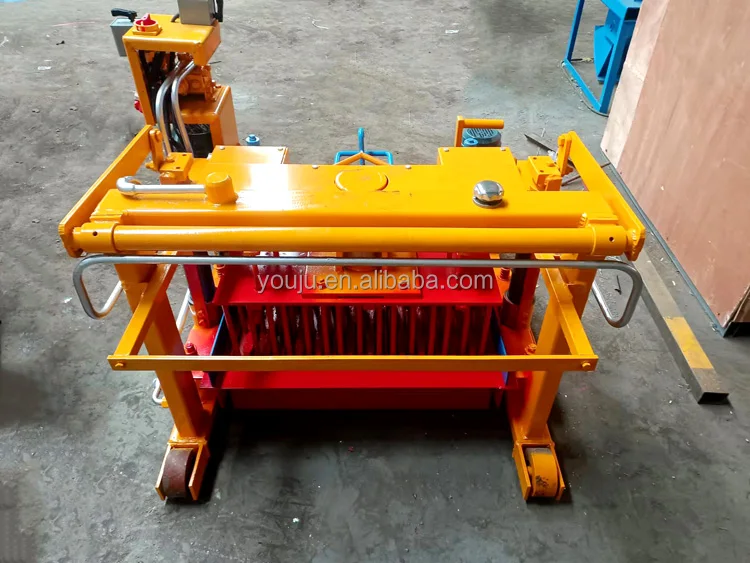
Description
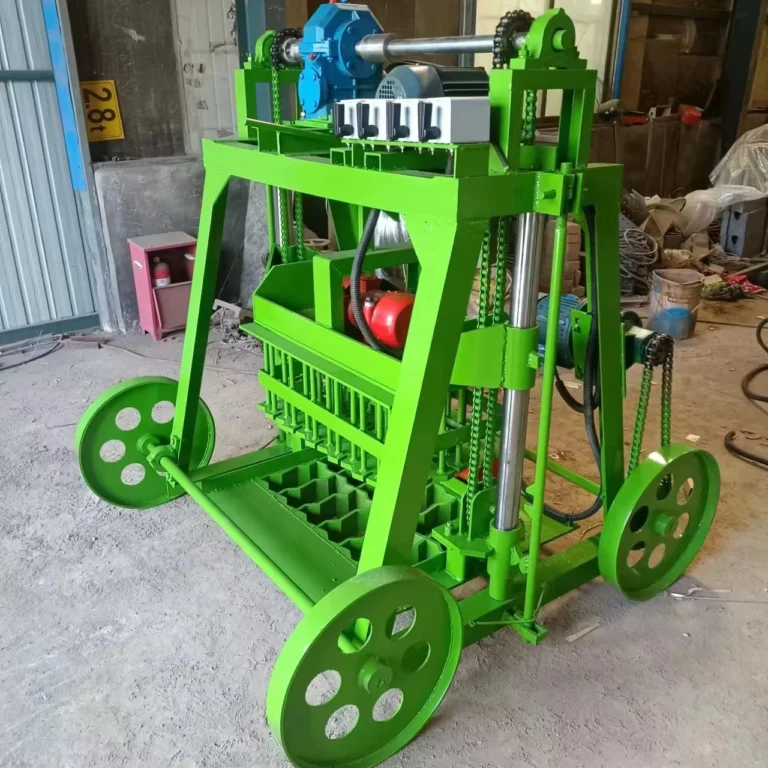
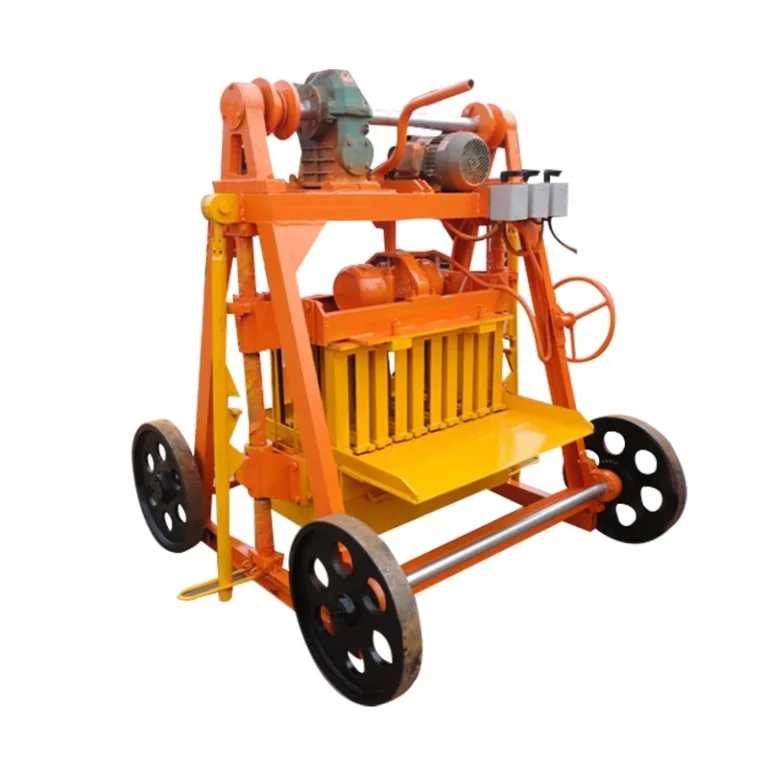
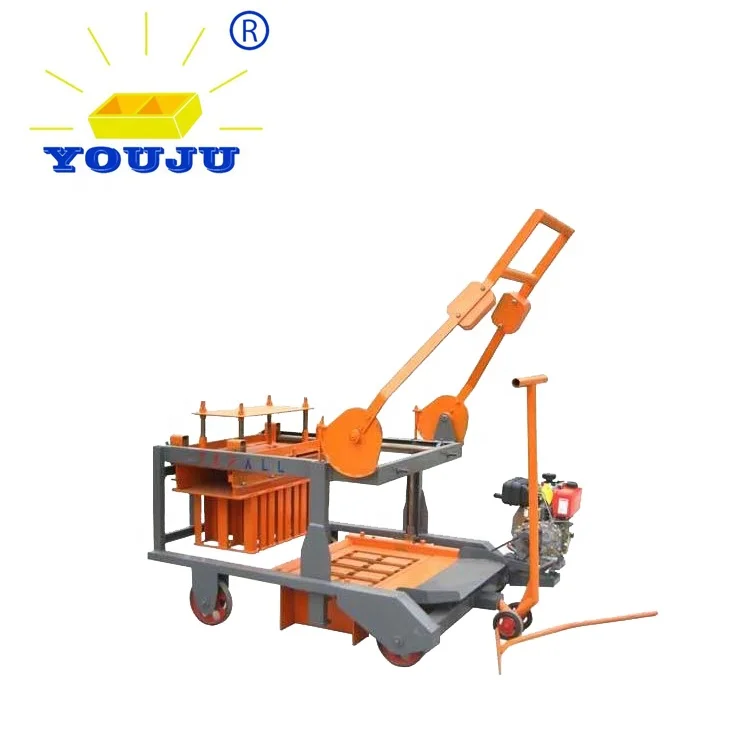
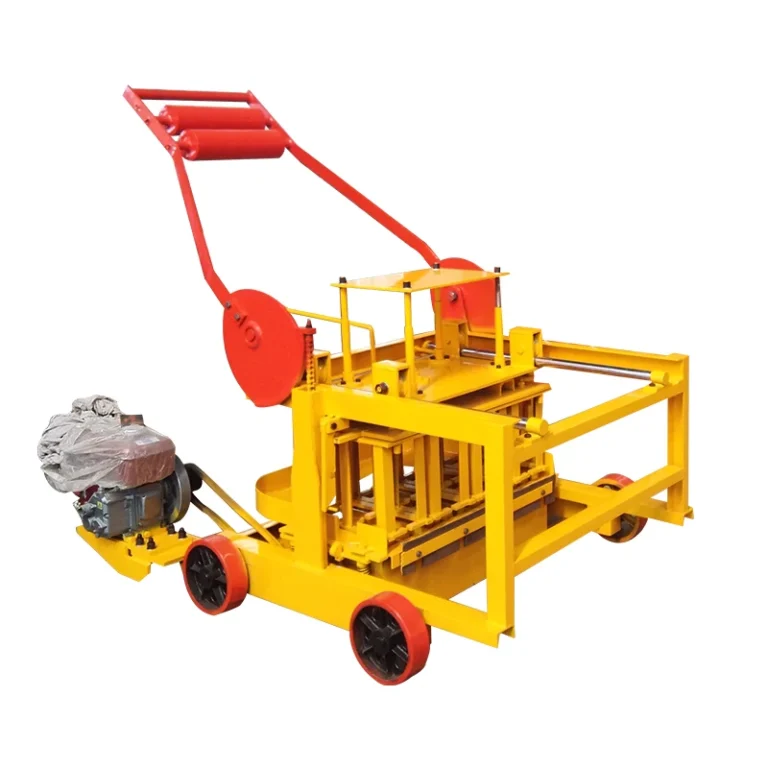
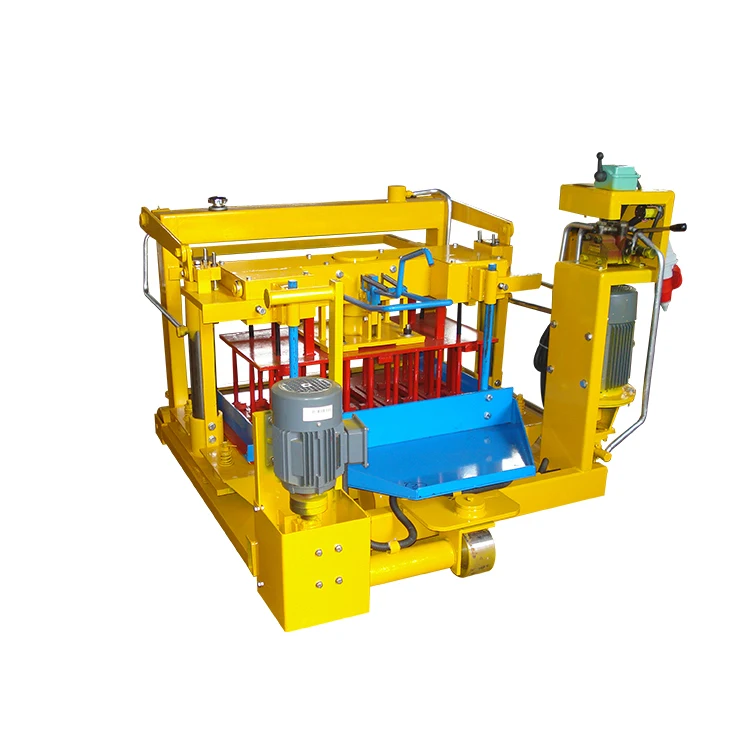
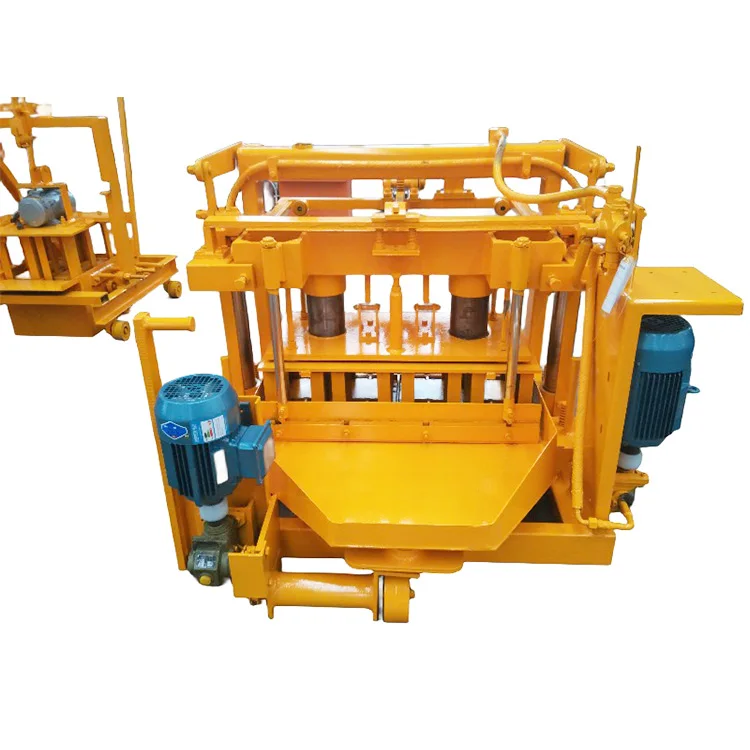
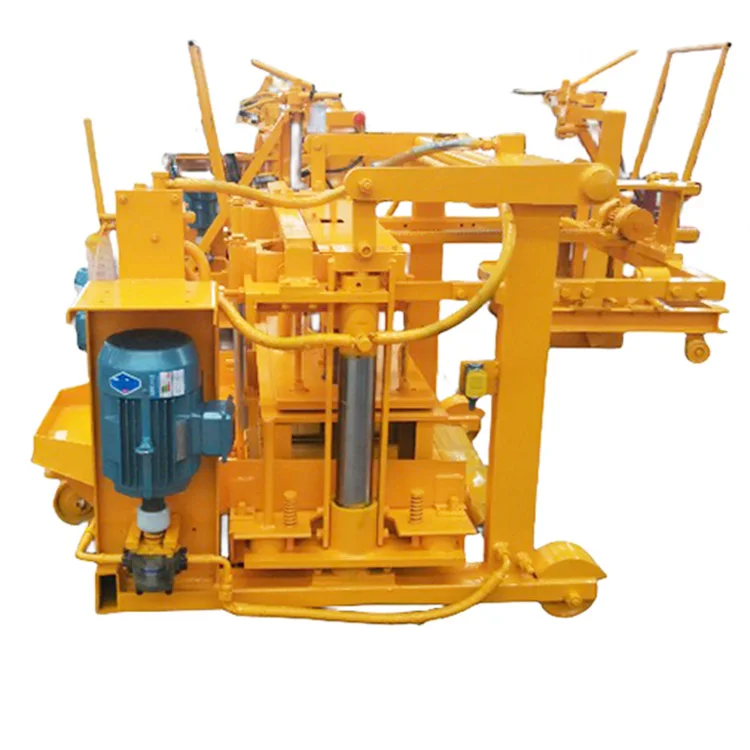
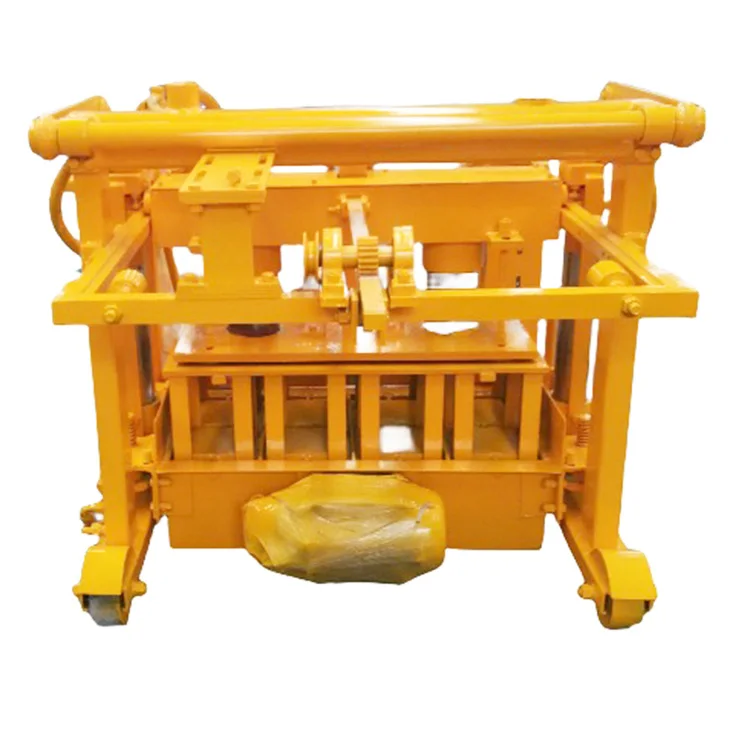
Matched system integration — The QMY4-30 mobile block machine is configured as a complete egg-laying unit where vibration, mould, and ground-laying output are specified together, not sourced from separate vendors and hoped to match on site.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QMY4-30 |
| Product Type | Mobile Concrete Block Making Machine |
| Rated Power | 5 kW |
| Cycle Time | 30 seconds per mould |
| Overall Dimensions (L×W×H) | 1200×1200×1100 mm |
| Net Weight | 950 kg |
| Mould Format | Changeable for hollow block and solid brick |
| Output Capacity | 480 pcs/h based on 400×200×200mm hollow block, 4 pcs/mould |
| Output Capacity | 600 pcs/h based on 400×150×200mm hollow block, 5 pcs/mould |
| Output Capacity | 840 pcs/h based on 400×100×200mm hollow block, 7 pcs/mould |
| Daily Output | 3840 pcs/8h based on 400×200×200mm hollow block |
| Daily Output | 4800 pcs/8h based on 400×150×200mm hollow block |
| Daily Output | 6720 pcs/8h based on 400×100×200mm hollow block |
| Raw Materials | Cement, sand, crushed stones, slag |
| Automation Level | Semi-automatic / mobile (egg-laying type) |
| Voltage & Frequency | Configurable — confirm with target market before production |
| Control System | Available with PLC or manual control — confirm preference |
| Pallet Size | Not applicable (blocks laid directly on ground) |
| Assembly State | Integrated unit, plywood packing approx. 3 m³ |
| Warranty | One year |
| Standards | CE (confirm with manufacturer for specific certificate scope) |
Application Suitability
| Application | Material or Output |
|---|---|
| On-site hollow block production for housing projects | Cement, sand, and crushed stone mixed locally at project sites |
| Solid brick manufacturing for boundary walls and infill | Crusher dust and cement blends common in small-yard production |
| Contractor block production at remote development sites | Locally available river sand or manufactured sand with cement binder |
| First plant setup by entrepreneurs entering the block market | Standard hollow block and solid brick formats using basic aggregate mixes |
What "480 Blocks per Hour" Actually Means on the Ground
A quoted cycle time only holds when your local aggregate cooperates with the mould and vibration settings.
I once stood on a housing project in West Africa where a mobile block machine of this class was rated at 30 seconds per cycle, but the local river sand carried heavy clay content. The mix stuck to the mould walls, operators spent half each cycle scraping, and real output dropped below half the rated figure. Nobody had checked the material before the machine arrived. On the QMY4-30, the 30-second cycle time applies to a clean sand and crushed stone mix producing 400×200×200mm hollow blocks at 4 pieces per mould. [NEED_CITE: impact of clay content in sand on concrete block demoulding time]
If your site sand has high fines or your market demands a block format that uses a different mould cavity count, your actual hourly throughput will shift. That is why the capacity figures here are each tied to a specific block dimension and cavity count — not a single headline number.
How the Upgrade Path Keeps the QMY4-30 Relevant
The QMY4-30 starts as a semi-automatic egg-laying machine where an operator guides the unit across a prepared floor and blocks cure in place. This keeps the initial investment manageable for a first block plant or a contractor producing for a single project. When demand grows, the automation upgrade path allows you to add PLC-controlled batching, automatic pallet feeding on a companion stationary line, or stacking and cubing modules without replacing the core press entirely.
Many small plant owners buy a basic machine and then face a full replacement when they want consistency gains from an automatic mobile block making machine setup. The QMY4-30 approach lets you begin with manual ground-laying and layer in control and handling equipment as your block sales justify the capital.
PLC Control and What It Actually Removes from the Operator
When you choose the PLC-controlled mobile block machine configuration, the system takes over cycle timing, vibration duration, and mix dispensing sequence. What this removes from the operator is the guesswork — each block receives the same vibration energy and the same material volume regardless of who is running the shift. [NEED_CITE: PLC control consistency in concrete block production across operator shifts]
On a semi-automatic egg-laying machine, the operator controls when the mould lifts and when the next cycle begins. With PLC control, the sequence locks in, and batch-to-batch density variation narrows. For buyers producing blocks that must pass a compressive strength test for government housing contracts, this consistency matters more than raw speed.
Mould Change Time, Ground Conditions, and What the Specs Do Not Show
The QMY4-30 uses a changeable mould system for hollow block and solid brick formats, but the ease of a mould swap depends on whether your operators have the right spanners and whether the mould bolts are kept clean of cured concrete. In practice, a well-maintained mould change on a mobile egg-laying machine takes a portion of a shift — plan your format runs in batches rather than switching every few hours.
The rated power of 5 kW drives both vibration and the mould lifting mechanism. On sites where you are laying blocks on uneven or soft ground, the machine will lean and produce blocks with inconsistent wall thickness. A compacted gravel bed or a concrete floor strip is not optional — it directly affects block geometry. The 950 kg net weight gives the machine enough mass to stay planted during vibration, but only on a firm surface. [NEED_CITE: ground preparation requirements for mobile egg-laying block machines]
The overall dimensions of 1200×1200×1100 mm mean the unit fits through standard site gates and can be positioned with a small forklift or a block and tackle, which matters when you are working inside a partially built structure or a confined yard.
The Hidden Cost of Skipping the Voltage and Control Conversation
A mobile block machine that arrives with a motor wound for 380V/50Hz sitting on a site running 220V/60Hz will not start, and rewinding a 5 kW motor in a regional town can take weeks. Beyond the motor itself, the PLC display language and button labels must match your operators’ working language — otherwise the control system becomes a source of mistakes rather than consistency. [NEED_CITE: voltage and frequency standards by export market]
Buyers who treat electrical specifications as an afterthought often find that commissioning delays cost more than the machine itself. Confirming voltage, frequency, and PLC language before the machine enters production avoids a situation where the QMY4-30 sits idle on your site while you source a compatible motor or wait for a technician who speaks the right language.
Why Buyers Source the QMY4-30 Through This Channel
Block machinery is the single focus here, so the QMY4-30 is not one item in a general catalogue — it is specified alongside the moulds, mixing ratio, and ground-laying workflow as one matched system. The configuration is set against your actual local aggregate and target block format, not pulled from a default sheet. Mould design and supply cover the formats your market sells, including custom drawings if your buyers need a non-standard wall thickness or block profile. The automation level is selectable, meaning you can start semi-automatic on the QMY4-30 and add control and handling modules as your plant grows. Installation and commissioning support includes operator training on your site, not just a manual in the crate.
Documentation & Verification
- Line layout and capacity calculation stating the exact block format assumed for the QMY4-30
- Machine specification sheet with confirmed voltage, frequency, and control language
- Mould drawing and format list matching your local market hollow block dimensions
- Factory test record on your specified raw material blend before dispatch
- Hydraulic and electrical schematic for on-site troubleshooting during commissioning
- Operation and maintenance manual with wear parts and mould replacement intervals
Installation, Commissioning & Support
- Compacted gravel or concrete floor strip required for the 1200×1200 mm footprint to prevent leaning during vibration
- 5 kW power supply with dedicated circuit and confirmed voltage and frequency before the QMY4-30 arrives on site
- Integrated unit arrives assembled; position with forklift or block and tackle into the production area
- First-cycle commissioning includes vibration duration tuning to your local sand and crushed stone blend
- Operator training covers mould change procedure, cycle initiation, and daily cleaning of mould cavity surfaces
- Wear parts list identifies vibration pads and mould liner components with replacement intervals for the QMY4-30
What to Include in Your Inquiry
Share the hollow block or solid brick dimensions your market buys most, along with your target daily output and the type of sand or aggregate available on your site. Let us know your local voltage and frequency, the preferred PLC display language, and whether you plan to run the QMY4-30 as a standalone unit or eventually connect it to a batching and stacking line.
Frequently Asked Questions
Q: How do I verify real daily output for my specific block format on the QMY4-30?
A: Request a capacity calculation that states the exact block dimensions and mould cavity count behind each output figure. The QMY4-30 delivers different throughputs depending on whether you are producing 400×200×200mm blocks at 4 per mould or 400×100×200mm blocks at 7 per mould. A single headline number without a format attached will not match your production reality.
Q: What PLC display language options are available, and how do I confirm before shipment?
A: The PLC-controlled mobile block machine configuration supports multiple display languages. Specify your operators’ preferred language during the inquiry stage so it is programmed before the factory test. Confirming this after the QMY4-30 arrives on site leads to commissioning delays while the control panel is reprogrammed or replaced.
Q: How do I plan an automation upgrade from semi-automatic egg-laying to a more controlled line?
A: Start with the QMY4-30 in its semi-automatic ground-laying configuration and add batching accuracy, automatic material feeding, or stacking modules as your output volume justifies the investment. The upgrade path is designed so that the core press remains in service while handling equipment is layered around it.
Q: How does mould change time affect format flexibility on a mobile egg-laying machine?
A: Plan your production runs in batches by format rather than switching moulds frequently. Mould change on the QMY4-30 involves unbolting and realigning the cavity plate, which takes meaningful time when done carefully. Keep spare mould bolts and clean cavity surfaces to avoid cured concrete buildup that extends the swap.
Q: What electrical preparations are needed on-site before the QMY4-30 arrives for commissioning?
A: Confirm your site voltage, frequency, and available amperage against the QMY4-30 motor specification. Install a dedicated circuit with proper grounding near the production area. Have a local electrician verify phase rotation before the machine is powered on to prevent motor damage during first startup.