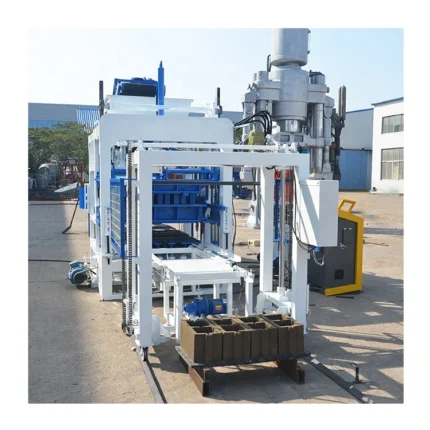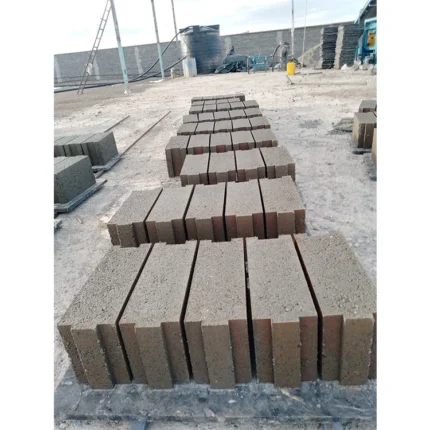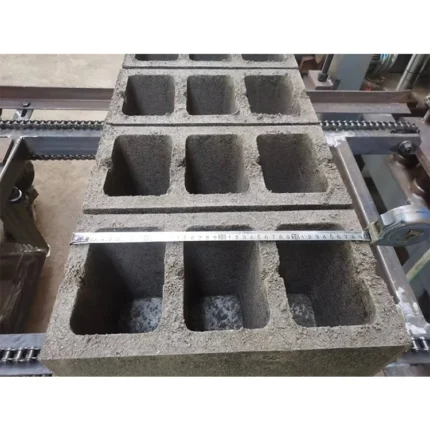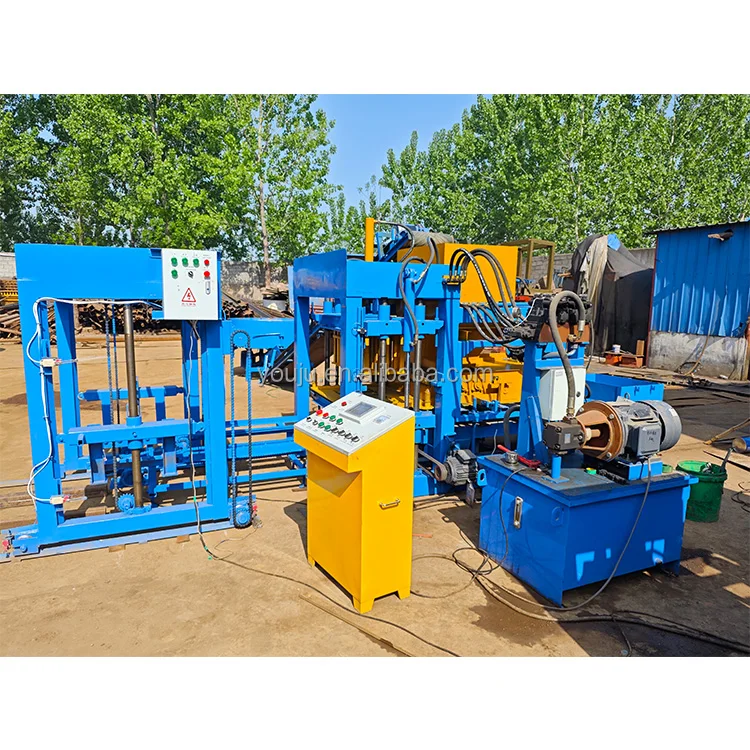

Description
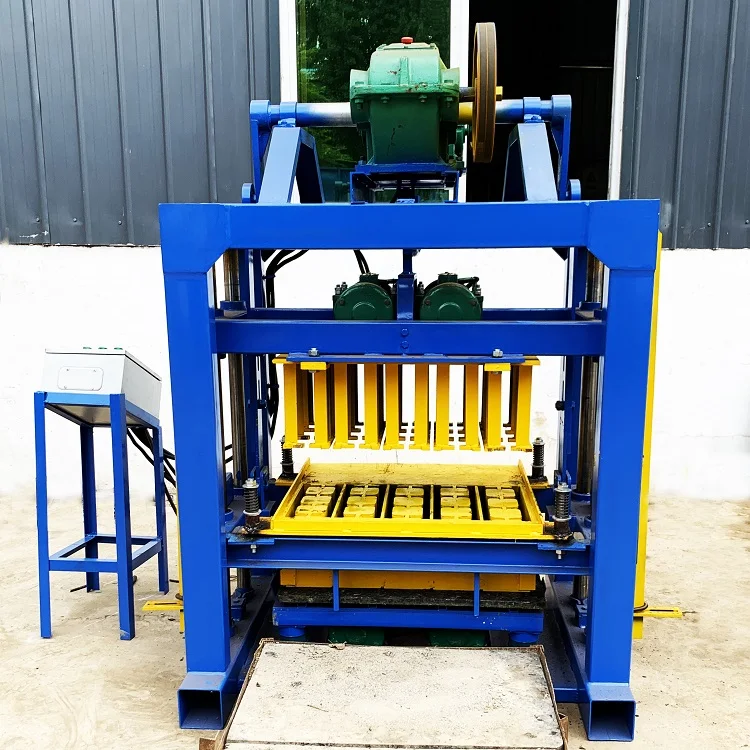
Configurable Control Interfaces — Language and voltage confirmed before build so operators read the screen from the first shift, avoiding commissioning standstills on your QT4-40.
Technical Specifications
| Parameter | Value |
|---|---|
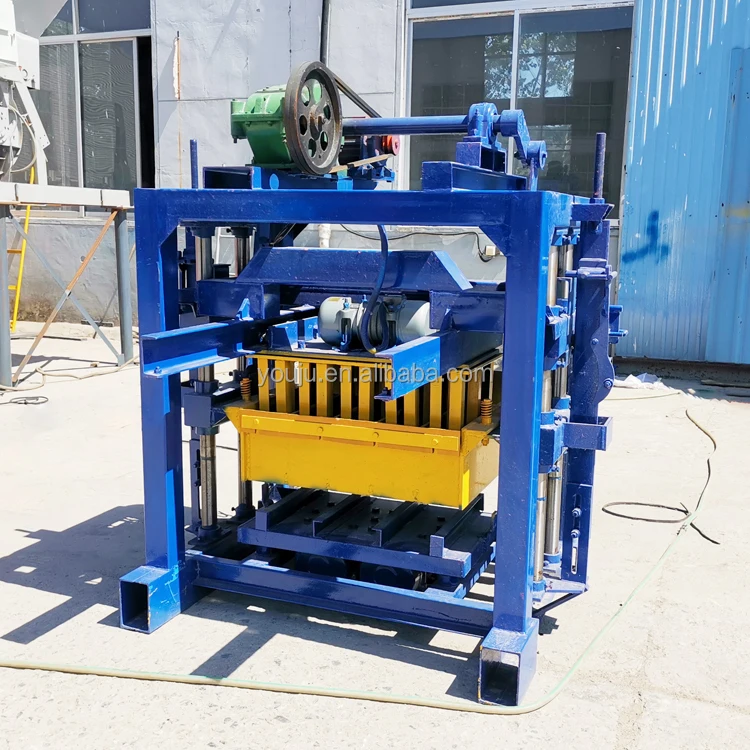
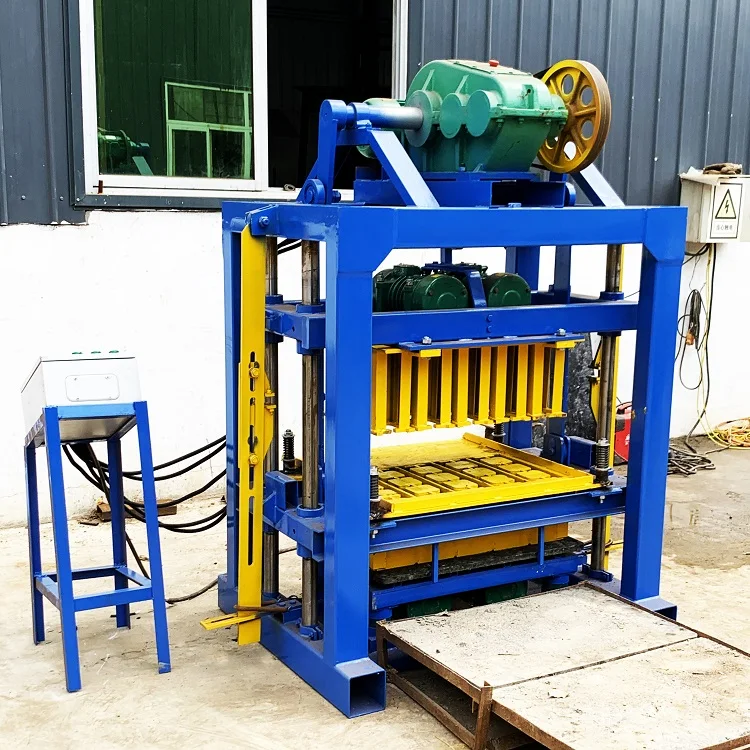
| Model | QTJ4-40 (QT4-40) |
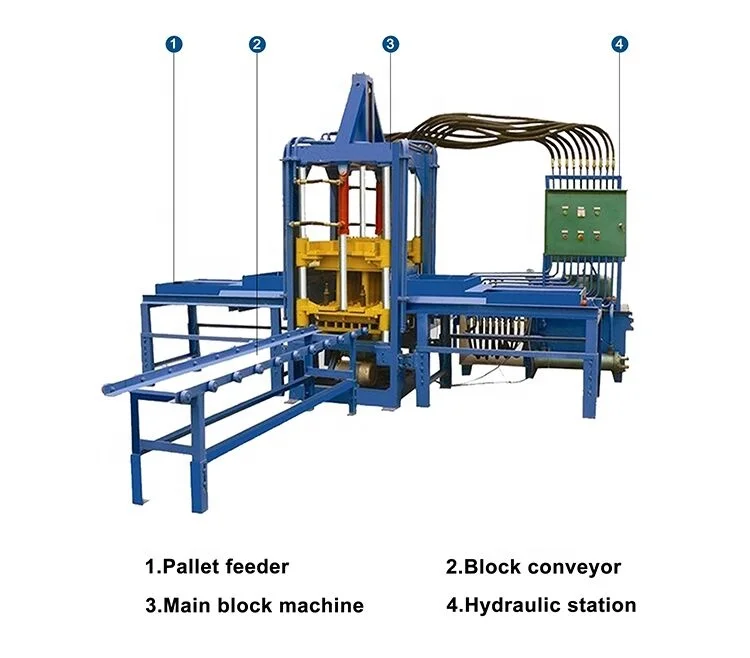
| Product Type | Manual Block Production Line |
| Vibration Form | Platform Vibration |
| Vibration Frequency | 2800 r/min |
| Pallet Size | 850 × 450 mm |
| Overall Dimensions | 1350 × 1460 × 1800 mm |
| Machine Weight | 1 T (source value — verify against manufacturer catalog) |
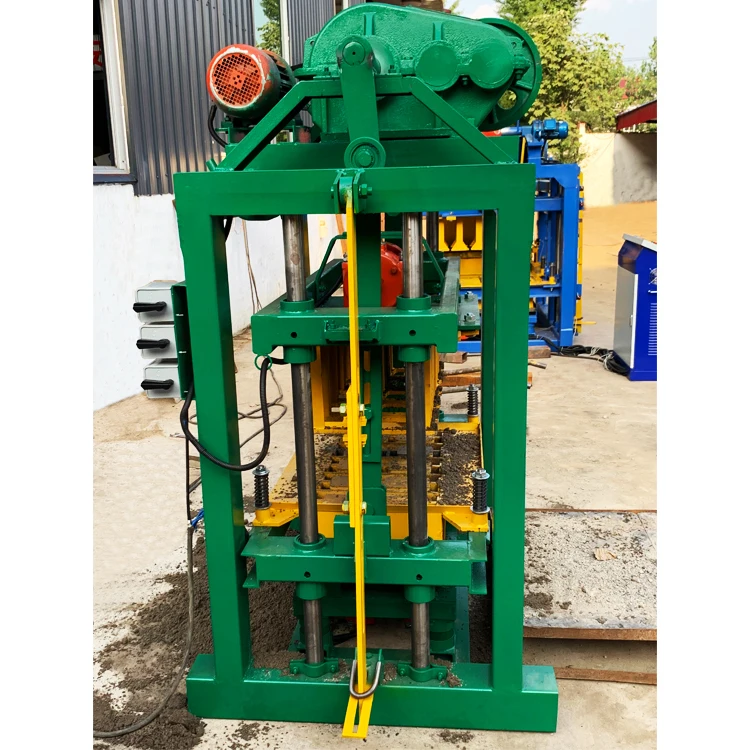
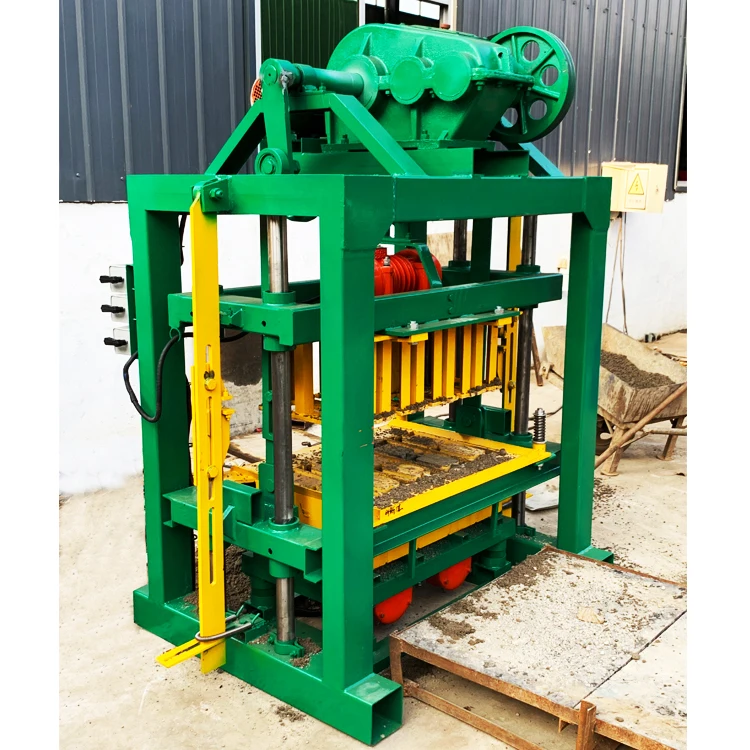
| Control System | Manual operation with top die push/pull and automatic scraper |
| Automation Level | Manual, with upgrade path to PLC-controlled operation |
| Required Factory Area | 200 m² |
| Crew Requirement | 1–3 operators |
| Capacity (400×200×200 mm hollow block) | 360 pcs/h, 2880 pcs/8 h shift |
| Capacity (400×150×200 mm hollow block) | 500 pcs/h, 4000 pcs/8 h shift |
| Capacity (225×112.5×60 mm interlocking brick) | 900 pcs/h, 7200 pcs/8 h shift |
| Raw Materials | Concrete, cement, fly ash, crushed stone, sand, gravel, slag |
| Typical Mix Ratio | Cement 8–10%, sand 30–40%, stone 50–60% (approx. 1:4:5) |
| Key Features | Platform vibration, top die push/pull, automatic scraper, manual pallet handling |
Application Suitability
| Application | Material or Output |
|---|---|
| Small workshop hollow block production | Crushed stone and cement mix on 850×450 mm pallets |
| On-site construction block supply | Fly ash blended concrete for 400×200×200 mm hollow blocks |
| Interlocking brick runs for paving projects | Sand and gravel mix forming 225×112.5×60 mm pavers |
| Startup block plant with future automation plans | Standard concrete blends across hollow, solid, and paver formats |
| Contractor-run curbstone and colored paver batches | Pigmented concrete on dedicated mould setups |
Why the PLC Screen Language Must Be Decided Before Crating
A control panel your operators cannot read is not automation — it is a liability waiting on your factory floor.
I once commissioned a manual block press in West Africa where the default screen language shipped was Chinese. The local crew could not navigate a single menu, and the machine sat idle for the entire first week while we scrambled to source a firmware update. That kind of oversight does not show up in a capacity quote, but it costs real production days. [NEED_CITE: PLC interface language requirements for export machinery]
The automatic QT4-40 block machine starts as a manual press, yet its upgrade path to PLC control means the language, button labels, and display units must be locked during the build — not after arrival. Confirming these details upfront prevents the most common commissioning delay I see on first-time block plants.
The Upgrade Path from Manual to Intelligent Control
Starting with manual pallet handling keeps initial investment low and lets your crew learn the press rhythm before adding automation layers. When daily volume justifies it, the QT4-40 accepts PLC-controlled pallet feeding and stacking modules without replacing the core press.
This staged approach means you purchase the automatic QT4-40 block machine intelligence layer only when your curing area and forklift logistics can actually absorb higher throughput, avoiding the common mistake of automating a bottleneck that sits elsewhere in the line.
Matching Vibration to Your Mix Design
Platform vibration at 2800 r/min must be paired with the right hydraulic pressure and aggregate grading to produce consistent block density. A mix that is too dry will crack under high-frequency vibration, while excess moisture causes slumping before the block reaches the curing rack. [NEED_CITE: concrete block vibration frequency and mix moisture correlation]
During factory testing, we run your actual material sample through a full cycle to verify that the vibration force and dwell time produce the compressive strength your local standard requires, then record those settings on the test sheet that ships with the press.
What the Specification Sheet Actually Tells You
The 850 × 450 mm pallet size is not arbitrary — it aligns with standard curing rack slots and the fork pocket spacing on common warehouse forklifts, so blocks move from press to rack without re-stacking. Choosing a pallet dimension that mismatches your existing racks forces a double-handling step that silently erodes daily output.
Top die push/pull with an automatic scraper reduces the physical effort per cycle compared to fully manual mould stripping, keeping operator fatigue manageable across an eight-hour shift. The stated factory area of 200 m² covers the press, raw material staging, and a basic curing zone, but buyers planning future automatic stacking should reserve additional floor length for the cubing conveyor.
Material ratio guidance — cement 8–10 %, sand 30–40 %, stone 50–60 % — serves as a starting point; your local aggregate shape and absorption rate will shift the optimum water-cement ratio, which is why we request a material sample before finalizing the vibration dwell setting.
The Hidden Cost of Skipping Configuration Details
Ordering a block press without confirming pallet material, curing rack dimensions, and forklift fork spacing leads to pallets that warp under sun exposure or do not seat properly on the rack, causing block damage before curing is complete. [NEED_CITE: pallet material degradation in tropical curing environments]
Skipping voltage and frequency confirmation can leave the vibration motor running on a supply it was not wound for, producing weaker compaction and premature bearing wear that shows up only after several weeks of operation. These are not manufacturing defects — they are specification gaps that shift the cost onto the buyer.
Why Source This Press Here
Block machinery is the sole product focus, so the press, mould, pallet, and handling equipment are specified as one matched system rather than assembled from unrelated suppliers. This prevents the interface mismatches that cause downtime on multi-vendor lines.
Configuration is set against your actual mix design and target block format, not a catalogue default, which means the vibration frequency, mould cavity count, and pallet size all work toward the same output figure. [NEED_CITE: block machine configuration matching local aggregate properties]
Mould design covers the formats your market actually sells, including custom drawings when standard cavities do not match local brick dimensions. The automation level is selectable, letting you begin with manual pallet handling and add PLC-controlled feeding and stacking when volume grows.
Installation support includes operator training on the specific control language you confirmed at order, plus a wear parts and mould list so you know which spares to stock before the first replacement cycle is due.
Documentation & Verification
- Line layout showing 200 m² footprint with pallet flow direction marked
- Capacity calculation per block format — hollow, solid, and paver listed separately
- Voltage and control language confirmation sheet signed before production
- Factory test record using buyer-supplied material sample
- Mould drawing and format list matching confirmed block dimensions
- Operation manual in the operator’s confirmed reading language
Installation, Commissioning & Support
- 200 m² level concrete slab required; anchor bolt plan provided with the 1350 × 1460 mm base footprint
- Dedicated circuit matching confirmed voltage and frequency for the 2800 r/min vibration motor
- Machine ships as a single skid; top die push/pull mechanism is pre-assembled and tested
- First-run parameter setting with your mix ratio (cement 8–10 %, sand 30–40 %, stone 50–60 %)
- Operator training covers mould change procedure and automatic scraper adjustment
- Wear parts list identifies scraper blades and vibration motor bearings for initial spares stock
Preparing Your Inquiry
To size the QT4-40 correctly, share the block formats your market demands, the daily volume you plan to reach, and the aggregate type available locally. Confirm your site voltage, supply frequency, and the control language your operators read.
If you intend to add automatic pallet stacking later, mention your curing rack dimensions and forklift fork spacing so the pallet format is chosen to suit both the manual start and the future automated line.
Frequently Asked Questions
Q: How is daily output verified per block format on the QT4-40?
A: Each capacity figure is calculated for a specific block dimension — for example, 360 pieces per hour assumes a 400×200×200 mm hollow block. We provide a capacity sheet listing output separately for every format you plan to produce, so no single headline number masks the real daily volume.
Q: Can the QT4-40 be upgraded to automatic pallet feeding and stacking later?
A: Yes. The press accepts PLC-controlled pallet feeding and stacking modules without replacement of the core machine. You start with manual pallet handling and add automation when your curing area and logistics can absorb the higher throughput.
Q: What PLC control options are available when upgrading from manual?
A: The PLC package includes a touchscreen with selectable display language, automatic pallet indexing, and batch counting. Button labels and alarm messages are confirmed in your operator’s language before the panel is built and shipped.
Q: How does pallet size affect curing area layout and forklift compatibility?
A: The 850×450 mm pallet aligns with standard curing rack slots and common forklift fork spacing. Confirming your rack dimensions and forklift model at order prevents double-handling and block damage during transport to the curing zone.
Q: What voltage and control language confirmation is needed before shipment?
A: We require written confirmation of your site voltage, frequency, and the operator’s preferred screen language before production begins. This prevents commissioning delays caused by mismatched motor windings or unreadable control panels after the machine arrives.