


Description
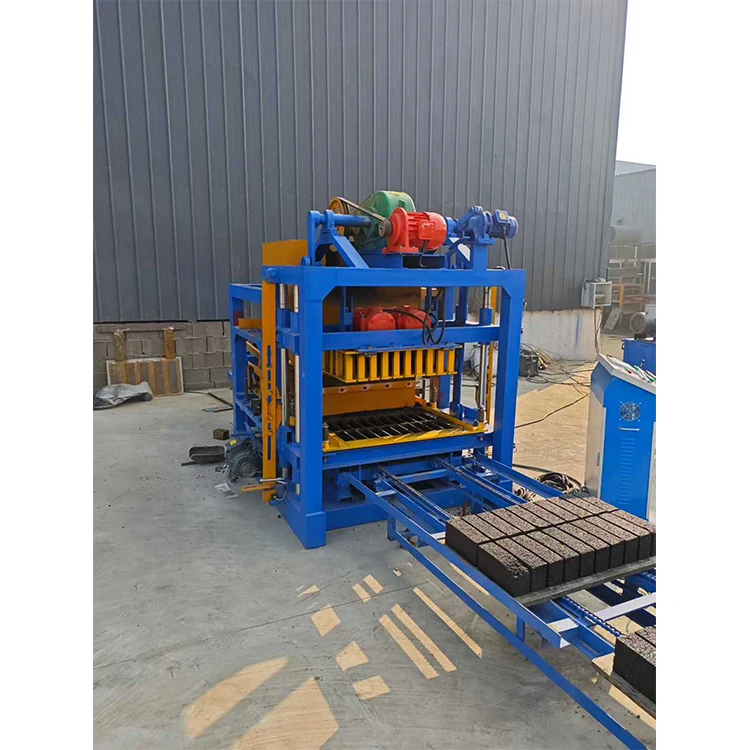
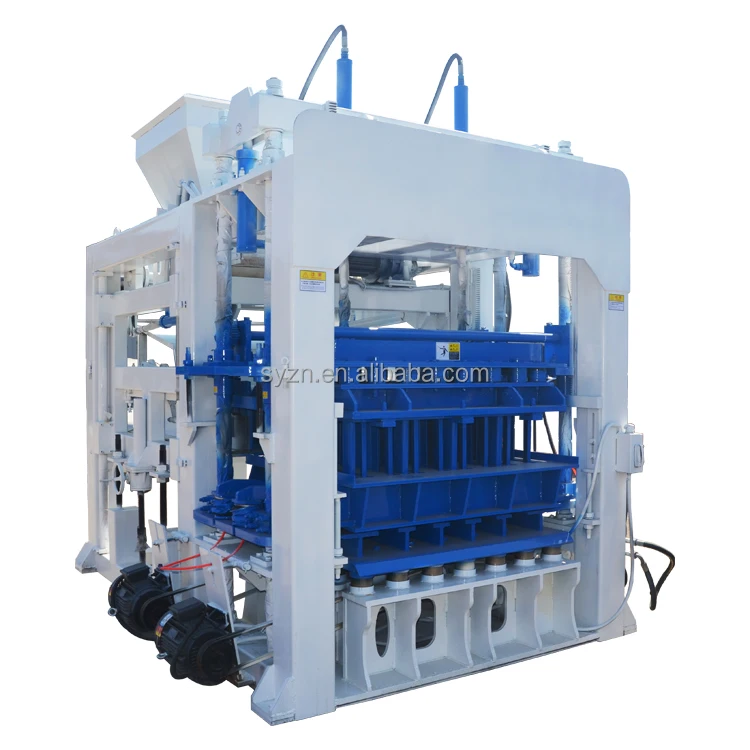
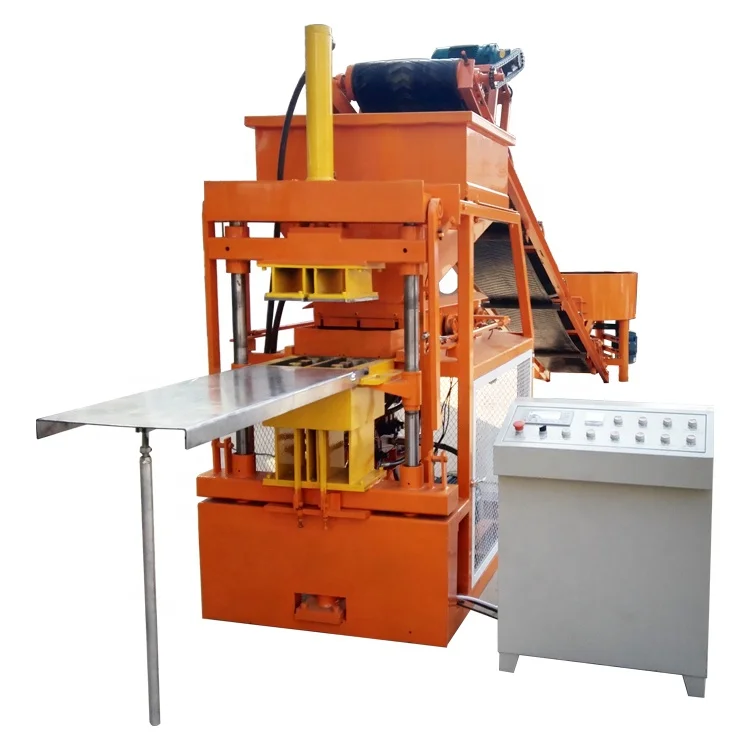
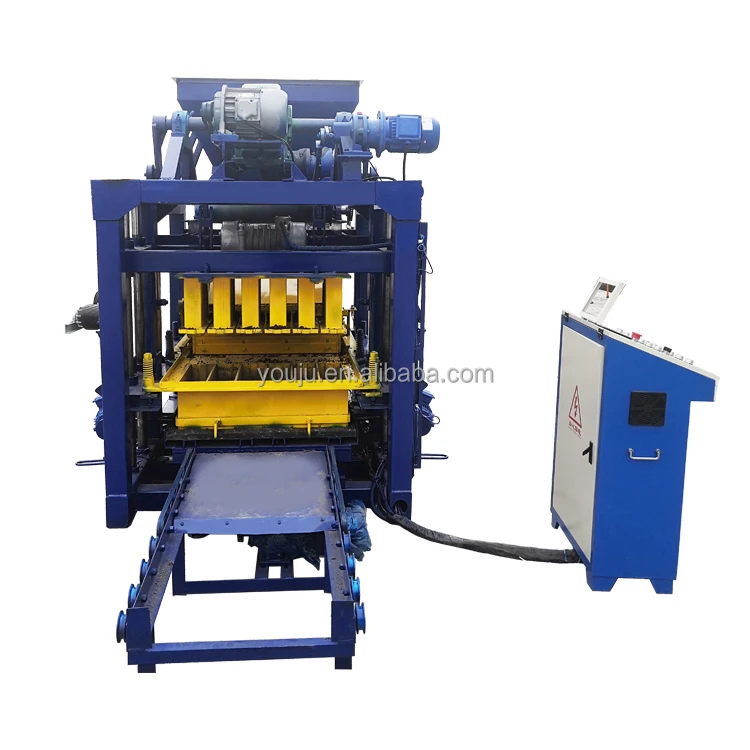
Matched System Configuration — The QTJ4-25 automatic concrete block making machine with PLC control is specified as a complete press, mould, pallet and vibration system rather than assembled from separate component suppliers.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-25 |
| Product Type | Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 3000 × 1800 × 2680 mm |
| Total Mass | 3.5 T |
| Overall Power | 16.58 kW |
| Vibration Force | 60 kN |
| Vibration Frequency | 2800–4500 r/min |
| Main Vibration Form | Platform Vibration |
| Pallet Size | 850 × 480 mm |
| Molding Cycle | 25 s |
| Demolding Method | Mechanical |
| Factory Area Required | 300 m² |
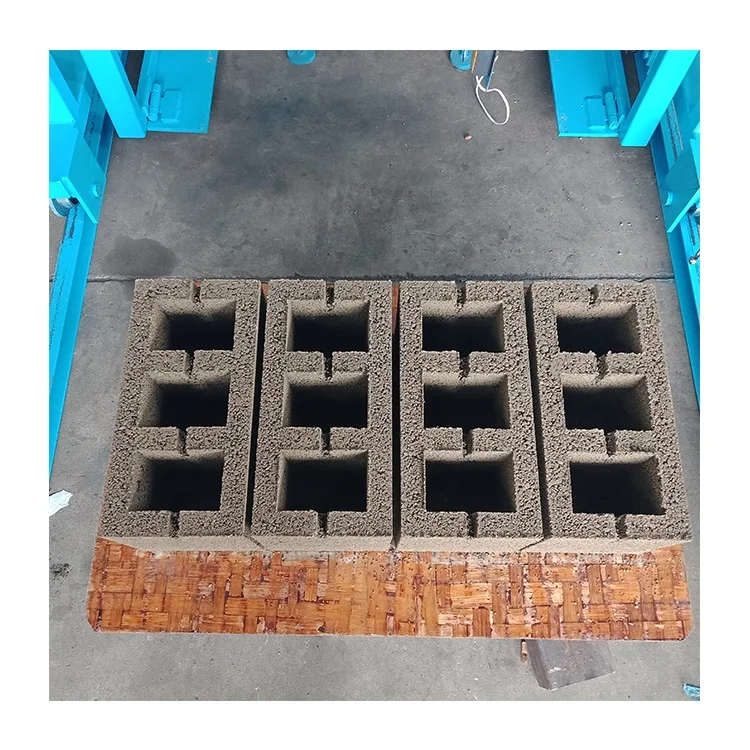
| Output Capacity | 580 pcs/h based on 400×200×200 mm hollow block, 4 pcs/mould |
| Output Capacity | 1400 pcs/h based on 240×115×90 mm porous brick, 9 pcs/mould |
| Output Capacity | 3300 pcs/h based on 240×115×53 mm standard solid brick, 21 pcs/mould |
| Frame Material | National standard manganese steel |
| Guide Column | Four chrome-plated columns, overlong guide design |
| Vibration System | Dual motors under platform + one motor on upper mould |
| Control System | PLC-based (brand and language configurable, basis to be confirmed) |
| Voltage & Frequency | Configurable per target market (basis to be confirmed) |
| Warranty | 1 year for whole machine, excluding spare parts |
Application Suitability
| Application | Material or Output |
|---|---|
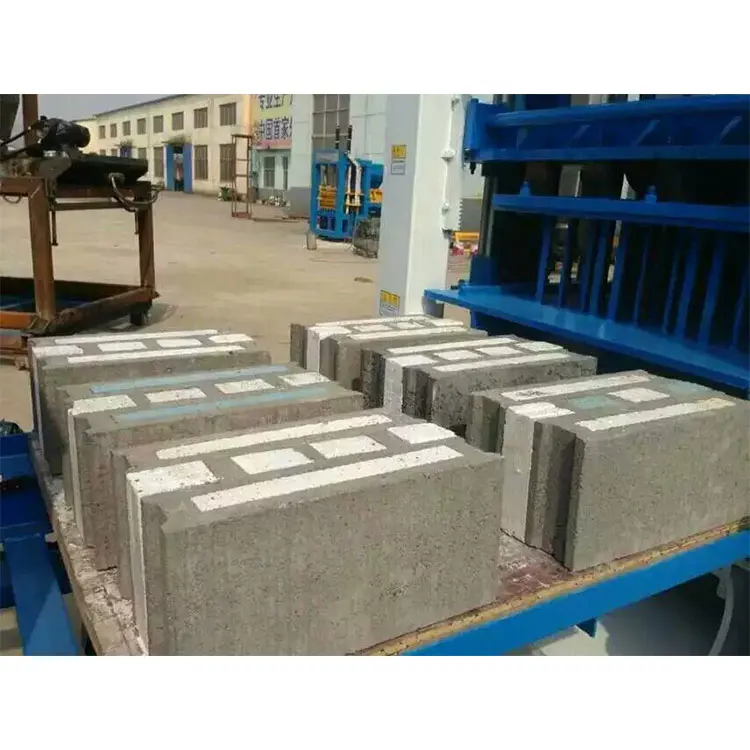
| Hollow block production | Crushed stone, sand, cement, fly ash |
| Solid brick manufacturing | Gravel, slag, cement blends |
| Paving block and colored paver runs | Fine aggregate with pigment additives |
| Interlocking block and kerbstone | Standard concrete mixes with local aggregate |
| Porous brick for wall construction | Lightweight aggregate and cement |
What "Pieces per Hour" Actually Means on the Shop Floor
Every capacity figure for the QTJ4-25 is tied to a specific mould and block dimension so you can calculate real daily throughput before signing.
Sellers frequently quote a single cycles-per-hour number without disclosing which block format that figure assumes. A buyer expecting 3300 pieces hourly may discover that rate only applies to small solid bricks, while the hollow blocks their market actually demands run at a fraction of that volume. This gap between quoted capacity and realized output causes more project delays than almost any other specification mismatch [NEED_CITE: common specification disputes in block machinery procurement]. When evaluating an automatic concrete block making machine with PLC control, the first document you should request is a capacity calculation broken down by each block format you intend to produce.
Control Logic That Removes Operator Guesswork
The PLC system on the QTJ4-25 manages molding cycle timing, vibration frequency selection and demolding sequence as one coordinated routine. Rather than relying on an operator to judge when compaction is complete, the controller executes the 25-second cycle with consistent repeatability across shifts. This matters most when you run multiple block formats in a single day — the automatic concrete block making machine with PLC control recalls stored parameters per mould, eliminating manual dial-in errors.
Vibration Tuning and the Aggregate Variable
Platform vibration at 60 kN across a 2800–4500 r/min range, combined with a separate upper mould motor, delivers compaction from both directions. However, vibration force alone does not guarantee block strength. The frequency and duration must be matched to the buyer’s specific mix design and local aggregate characteristics. A volcanic ash aggregate common in parts of Southeast Asia absorbs vibration energy differently than crushed granite, and running default settings on unfamiliar material produces inconsistent density block to block [NEED_CITE: aggregate variability effects on concrete compaction]. This is why confirming your raw material profile before factory testing is non-negotiable.
Reading the Numbers That Matter
The 60 kN vibration force paired with mechanical demoulding on four chrome-plated guide columns determines how densely the concrete is compacted and how cleanly the block releases from the mould. Overlong guide design keeps the upper mould aligned through thousands of cycles, which directly affects dimensional tolerance on interlocking blocks where even small deviation causes laying problems downstream. The 850 × 480 mm pallet size must be cross-checked against your curing rack spacing and forklift fork width — a mismatch here means rebuilding your curing area or buying new handling equipment after the machine arrives. Mould change across hollow, solid, paver and interlocking formats uses the same pallet footprint, giving format flexibility without requiring separate pallet inventories.
The Hidden Cost of Skipping Control Configuration
Arriving at commissioning to discover the PLC display is in a language your operators cannot read, or that the voltage does not match your plant’s supply, adds weeks of delay and often requires flying in a specialist electrician. Control system mismatches are among the most common avoidable causes of delayed startup in exported block machinery [NEED_CITE: export machinery commissioning delay factors]. Confirming voltage, frequency and display language during the quotation stage — not after production — removes this entire category of risk.
Why Source This Machine Here
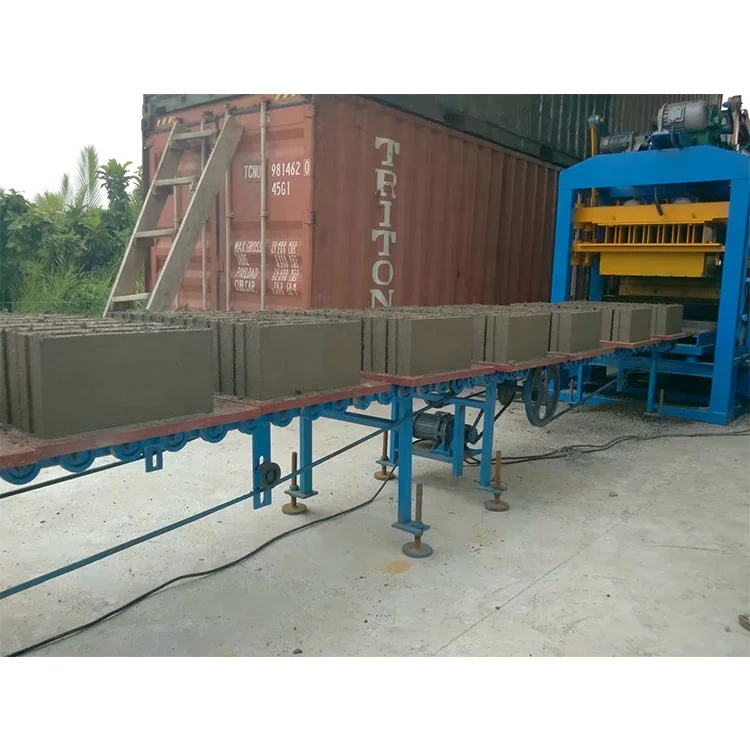
Block machinery is the single focus of this operation, so the QTJ4-25 press, its moulds, pallets and handling equipment are specified together as one matched system. Configuration is set against your actual mix design and local aggregate, not pulled from a catalogue default. Mould design covers the formats your market sells, with custom drawings available when standard options do not fit. Automation level is selectable, meaning you can begin with this machine’s current control setup and add pallet feeding, stacking or cubing modules as your plant grows. Installation support includes operator training and a wear parts supply plan so your first mould replacement does not become a sourcing emergency.
Documentation & Verification
- Line layout drawing showing 300 m² factory area allocation and equipment placement
- Capacity calculation document stating block format assumed for each output figure
- Factory test record with vibration parameters matched to your submitted mix design
- Voltage, frequency and PLC display language confirmation sheet signed before production
- Hydraulic and electrical schematic for on-site maintenance reference
- Mould drawing and format list covering all block types included in your order
Installation, Commissioning & Support
- 300 m² factory area with level concrete floor required for the 3000 × 1800 mm machine footprint
- 16.58 kW total power draw needs dedicated circuit matching confirmed voltage and frequency
- Mechanical demoulding system requires alignment check after transport before first production run
- PLC control language and parameter sets verified on-site during commissioning with your operators
- Chrome-plated guide columns inspected and lubricated per maintenance schedule included in manual
- Wear parts and mould list provided with part numbers for reorder without machine downtime
What to Include in Your Inquiry
Send your target block formats with dimensions, the daily output you need per format, and a sample of your local aggregate or mix design. Confirm your plant’s voltage and frequency supply along with preferred PLC display language. If you already have curing racks, forklifts or pallets on site, include those dimensions so the 850 × 480 mm pallet specification can be verified against your existing infrastructure before the order is finalized.
Frequently Asked Questions
Q: How is capacity verified per block format and what mould does each output figure assume?
A: Each output number on the QTJ4-25 is calculated against a specific mould cavity count and block dimension — 580 pieces hourly assumes a four-cavity mould producing 400×200×200 mm hollow blocks, while 3300 pieces hourly requires a 21-cavity solid brick mould. A capacity document listing every format you intend to run is provided with the quotation.
Q: What PLC control options are available and can the display language be set before shipment?
A: The control system is configurable for brand preference and operator language. Voltage, frequency and display language are confirmed in writing before production begins so the automatic concrete block making machine with PLC control arrives ready for your team to operate without translation delays.
Q: What is the upgrade path from this machine to full pallet feeding, stacking and cubing?
A: The QTJ4-25 platform supports adding automatic pallet feeding, stacking and cubing modules as separate stations connected to the existing PLC. You can start with the current automation level and integrate handling equipment later without replacing the press or changing pallet size.
Q: How does the vibration system need to be tuned for consistent block strength with local aggregate?
A: The dual-motor platform vibration and upper mould motor must have frequency and duration matched to your aggregate type and cement ratio. Factory testing uses your submitted mix sample so parameters are set before dispatch, and on-site fine-tuning during commissioning accounts for any material variation.
Q: How long does a mould change take and what tools are required on site?
A: Mould exchange on the QTJ4-25 involves unbolting the current mould from the vibration platform and securing the replacement using standard hand tools. The four guide columns remain in place across all formats. Specific changeover time depends on operator familiarity and is covered during on-site training after installation.