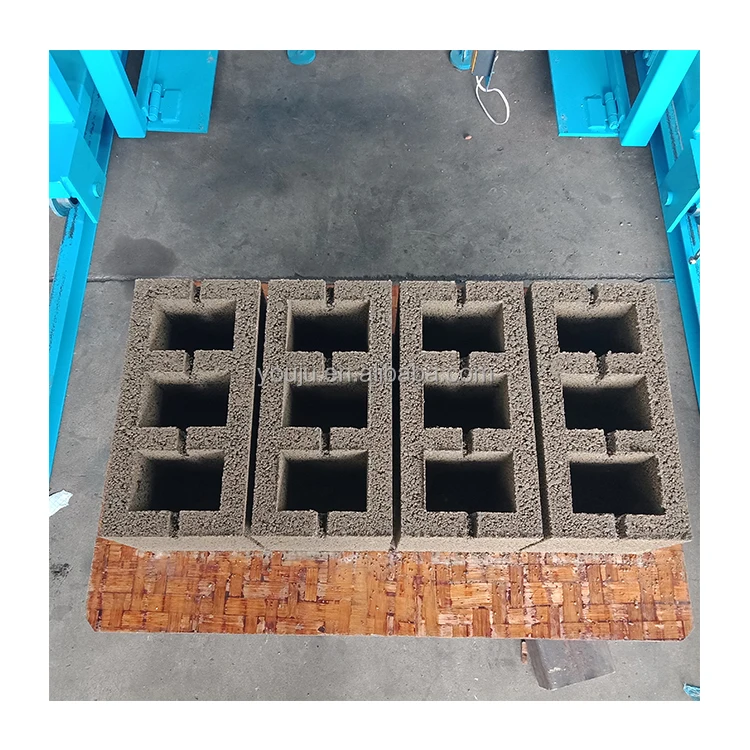
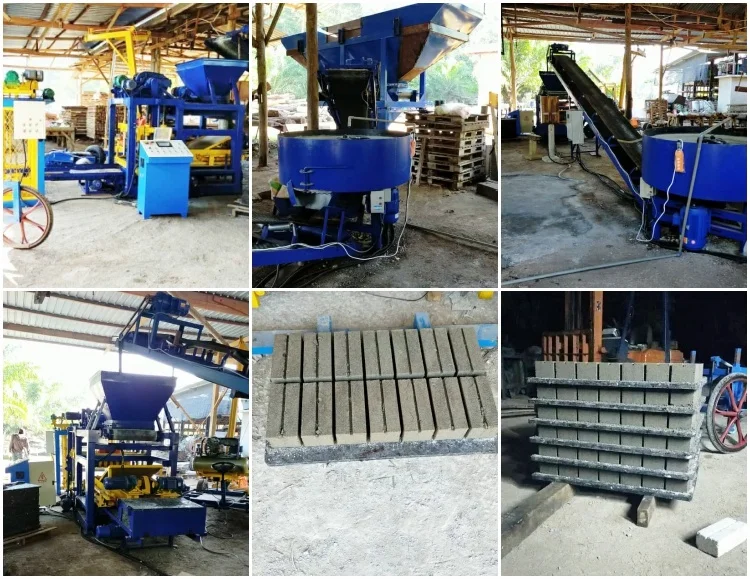
Description
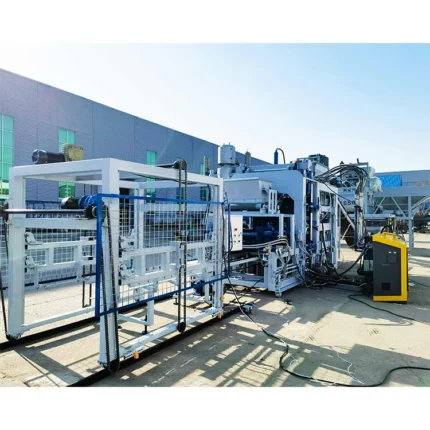
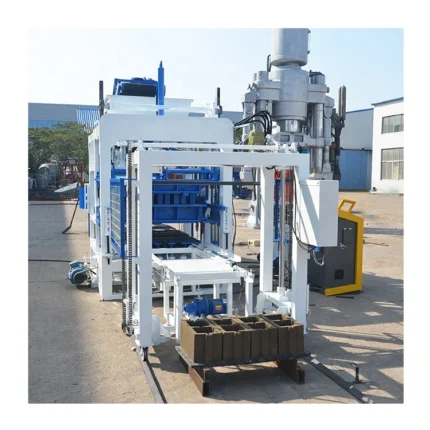
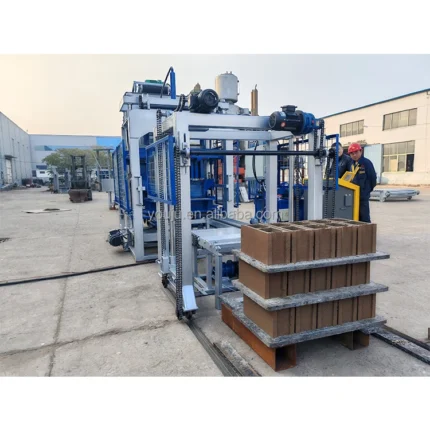
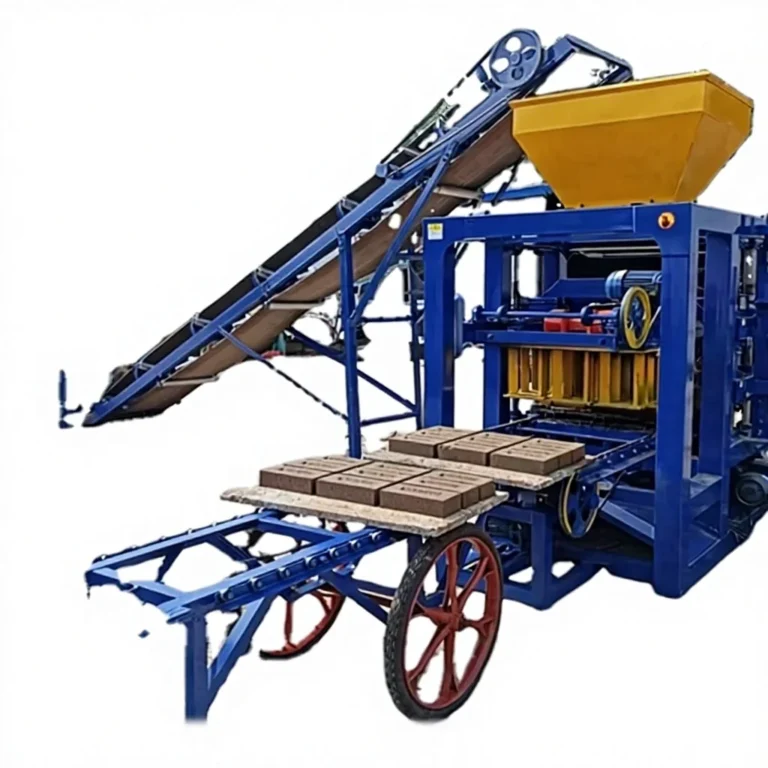
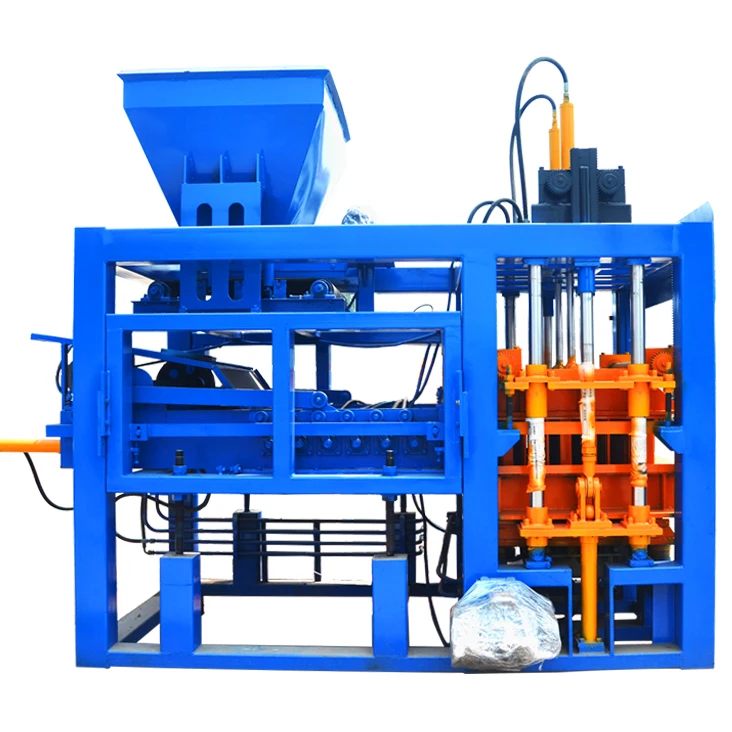
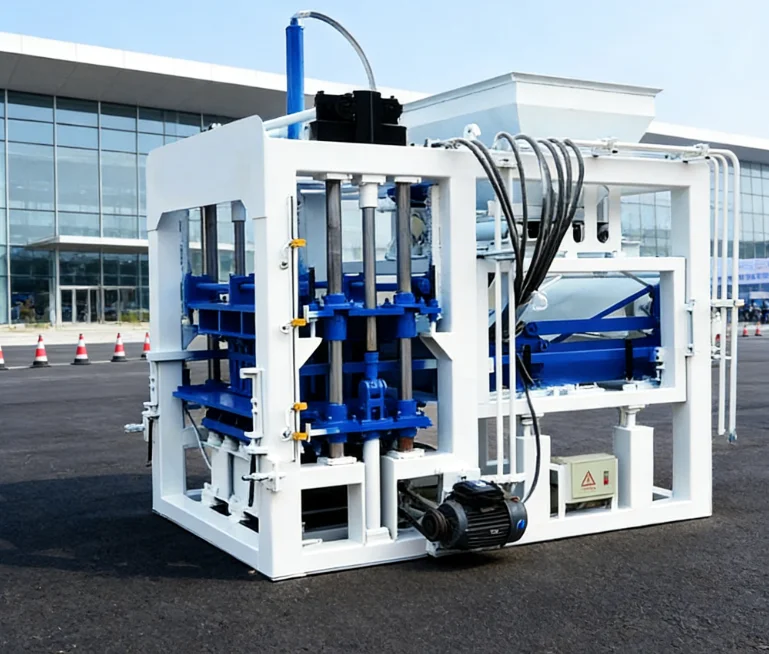
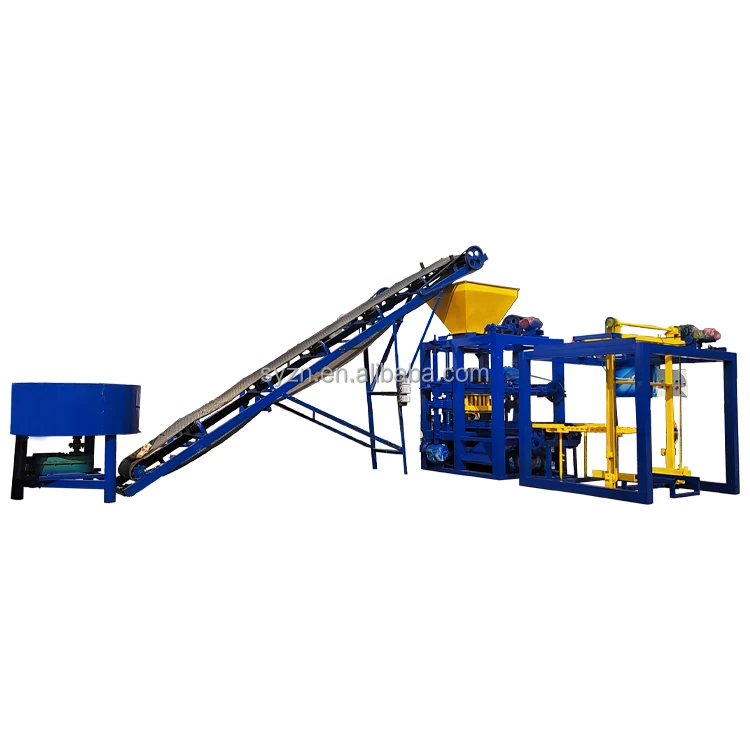
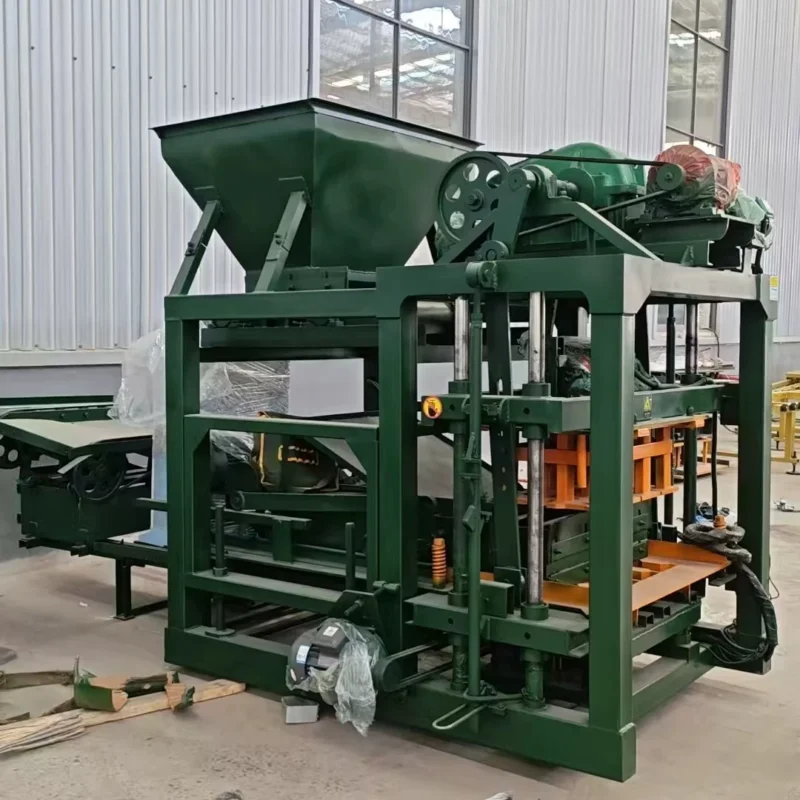
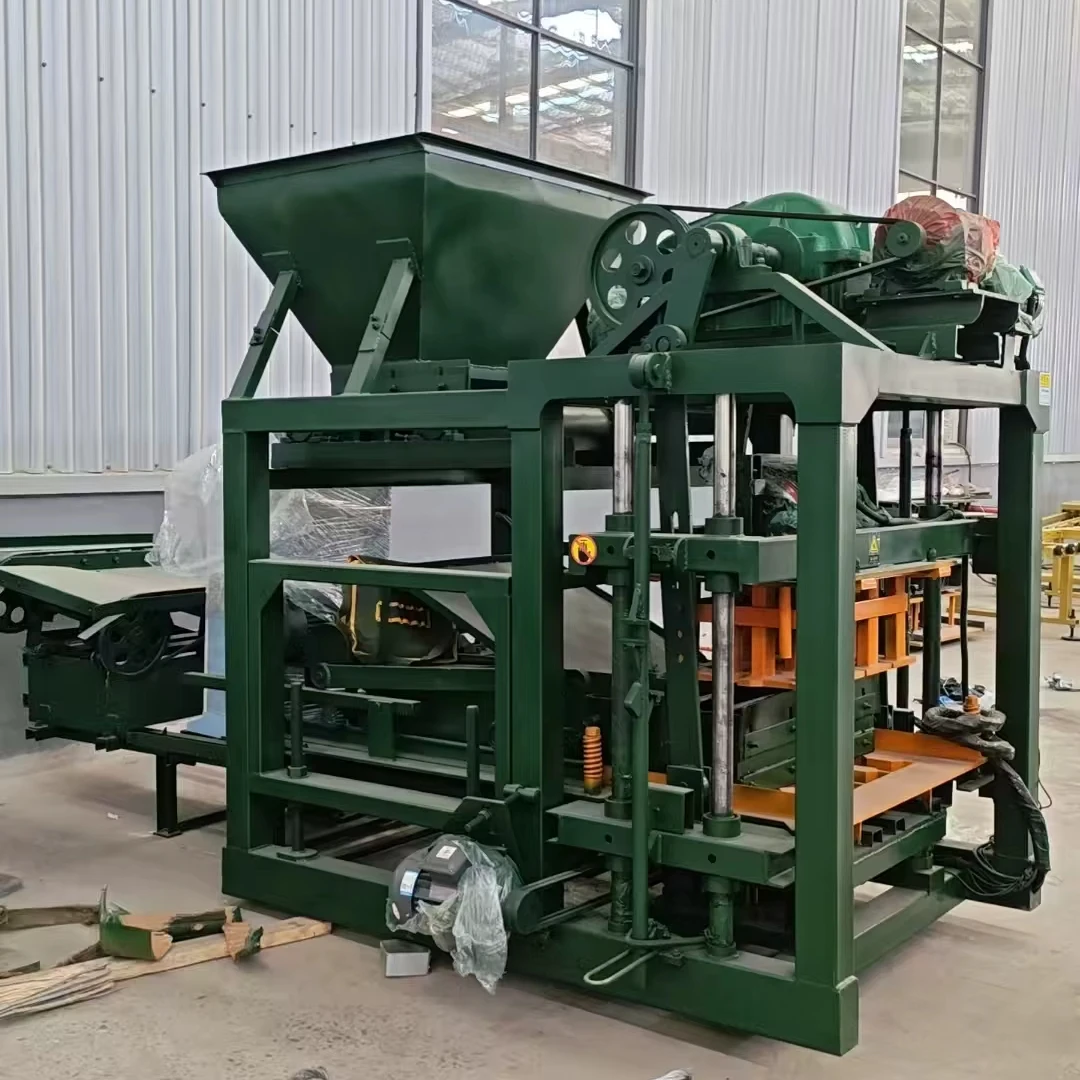
Integrated System Approach — Every QTJ4-25 leaves our facility as a matched set of press, mould, pallet and control logic, not a collection of standalone components.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-25 |
| Product Type | Stationary Concrete Block Making Machine |
| Control System | PLC-controlled with selectable display language |
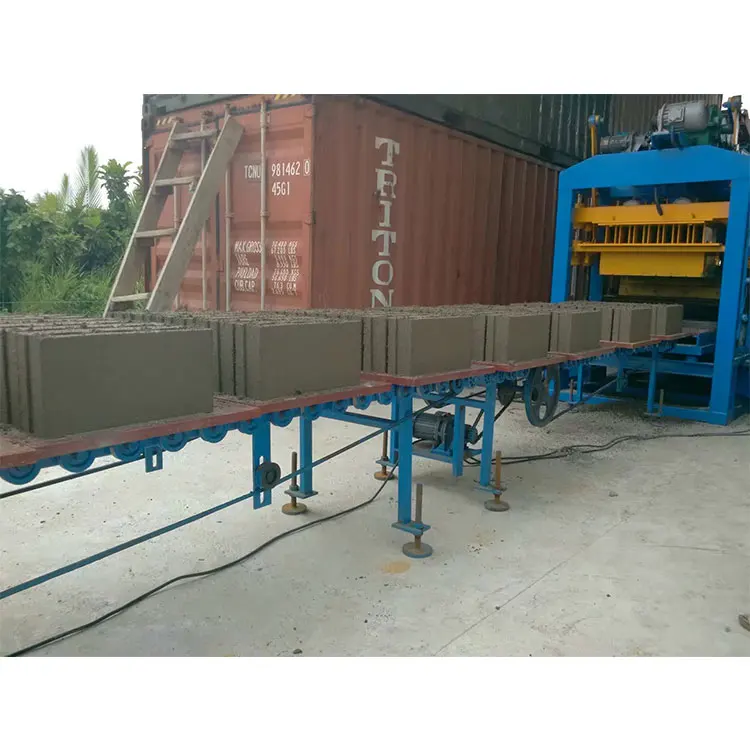
| Automation Level | Semi-automatic base, upgrade path to full stacking and cubing |
| Rated Power | 17.9 kW |
| Vibration Frequency | 2800 r/min |
| Vibration Force (Exciting Power) | 60 kN |
| Moulding Cycle Time | 25 s per mould (basis not stated in source — confirm block format) |
| Output Capacity | 960 pcs/h and 7680 pcs/day for 400×200×200 mm hollow block (basis not stated in source) |
| Pallet Size | 850×550×20 mm |
| Overall Dimensions | 6400×1500×2700 mm |
| Net Weight | 2500 kg |
| Included Mixer | JQ350 |
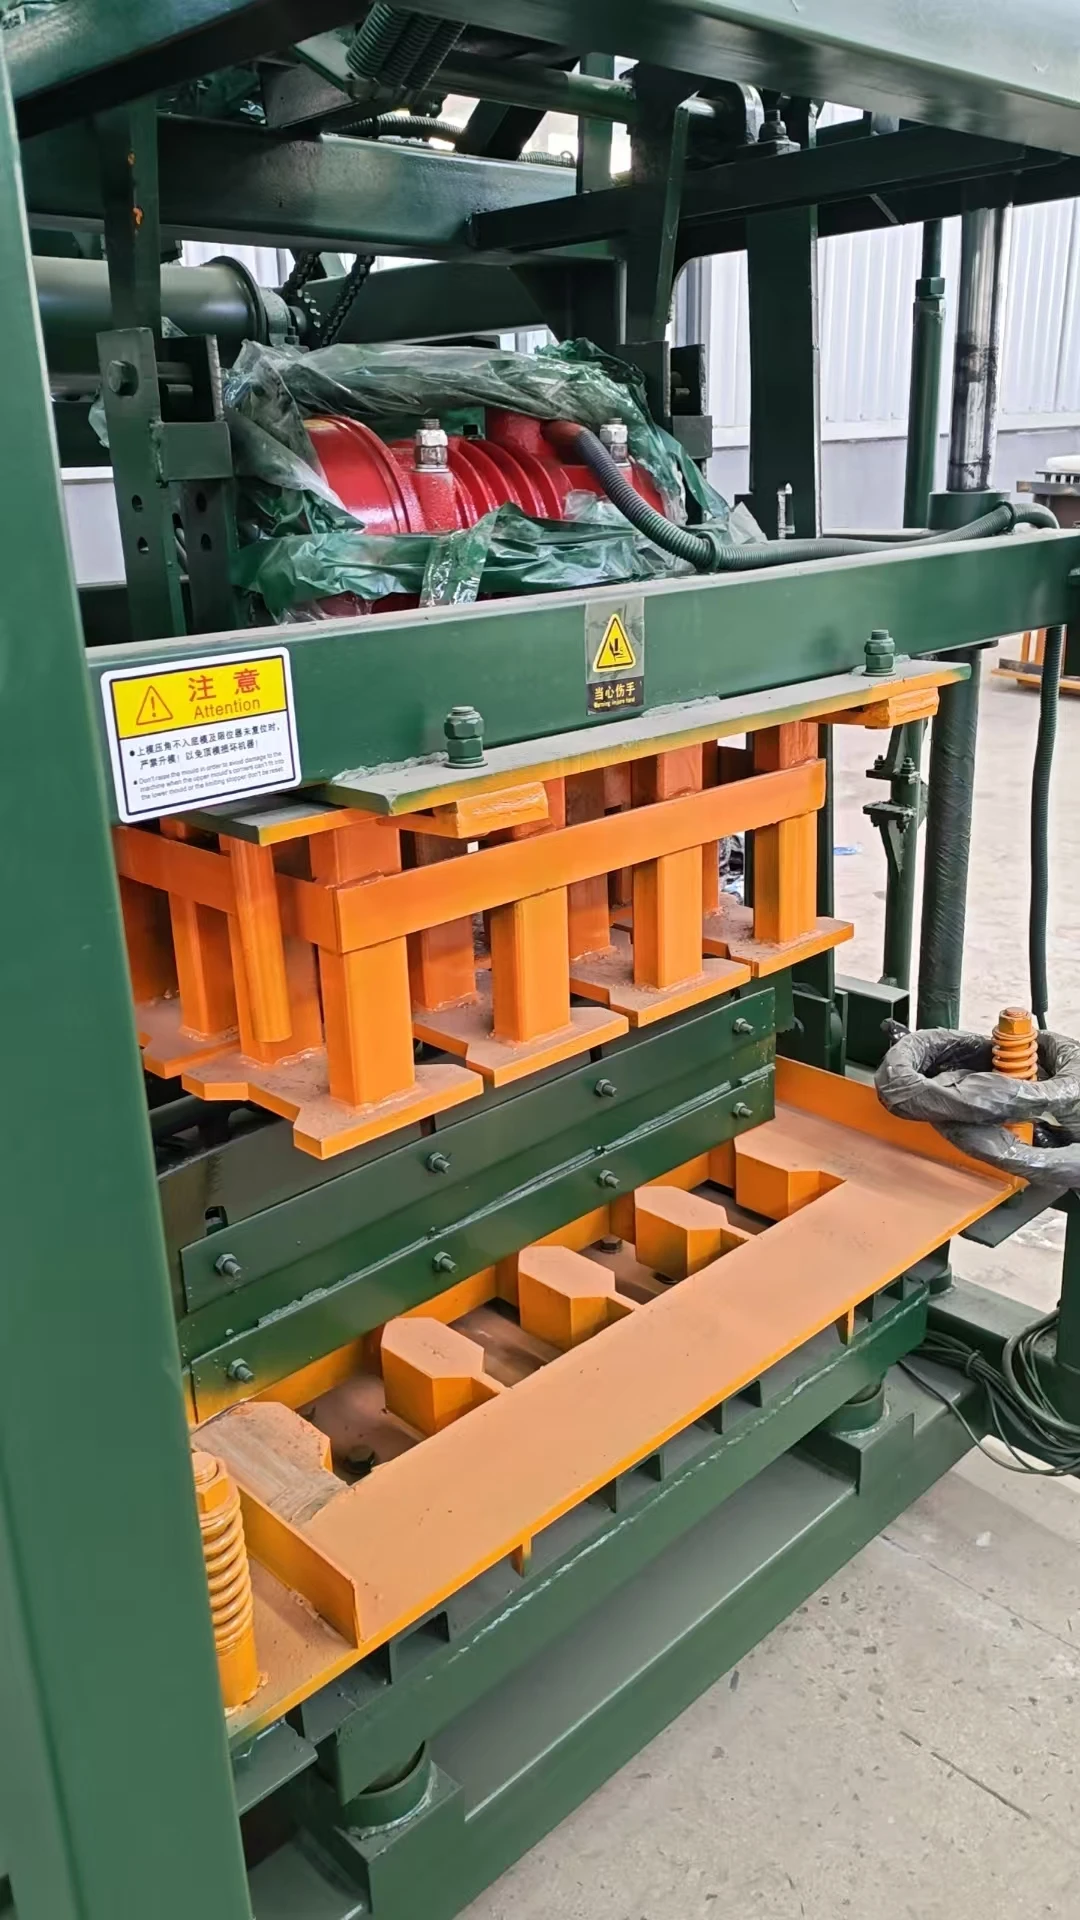
| Included Mould | 1 set block mould |
| Voltage & Frequency | Configurable to target market (confirm before production) |
| Certification | CE declaration available where applicable |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for building walls | Crushed stone, sand, cement, fly ash |
| Solid block production for load-bearing structures | Dense aggregate blended with Portland cement |
| Paving block manufacturing | Fine aggregate with colour pigment additives |
| Kerbstone and interlocking brick | Coarse aggregate with controlled moisture content |
| On-site contractor block production | Locally sourced sand and gravel mixes |
What "Automatic" Really Means on a QTJ4-25 Control Panel
PLC control removes guesswork from the operator, but only if the language, voltage and automation scope are locked down before the machine leaves the factory.
Many buyers assume "PLC-controlled automatic" on a spec sheet means the entire line runs itself. The QTJ4-25 ships with PLC logic governing the press cycle, vibration timing and mould actuation, yet pallet handling and stacking remain manual at the semi-automatic tier. I once stood on a site in West Africa watching an operator scroll through English error codes on a control panel he could not read — the machine sat idle for an entire morning because a simple parameter reset required a phone call across three time zones. [NEED_CITE: PLC interface language options for industrial machinery exports]
How Intelligent Control Shapes Every Press Cycle
The automatic QTJ4-25 block making machine PLC controlled logic sequences vibration start, hydraulic hold and mould release within each 25-second cycle. This repeatability means batch-to-batch density stays consistent as long as the raw material feed remains within the configured moisture and aggregate envelope. The PLC stores recipes so switching from hollow block to solid block becomes a menu selection rather than a manual recalibration.
Where Automation Ends and the Operator Begins
At the semi-automatic tier, an operator places pallets on the feed table and moves cured racks by trolley. The PLC manages everything between raw material drop and pressed block exit, but the upstream and downstream labour is still yours to plan. This split is deliberate — it lets a first-time plant owner start with lower capital outlay and add automatic pallet feeding, stacking and cubing modules once production volume justifies the investment. [NEED_CITE: typical automation upgrade paths for stationary block presses]
Reading the Numbers That Actually Matter
Vibration force at 60 kN combined with a frequency of 2800 r/min determines how tightly aggregate particles pack inside the mould cavity. Higher force alone does not guarantee stronger blocks — the mix design and moisture content must match. The 850×550×20 mm pallet size dictates your curing rack spacing and forklift tine width, so confirm compatibility with existing handling equipment before the machine arrives. Pallets that are too thick will jam the feed table; pallets that are too narrow will leave unsupported edges on wider block formats.
The Cost of Skipping the Configuration Conversation
Ordering a block press without confirming PLC display language, voltage frequency and pallet material leads to a cascade of delays. The machine arrives, the electrician discovers a 60 Hz motor on a 50 Hz supply, and commissioning stalls while replacement components ship internationally. [NEED_CITE: electrical frequency mismatch consequences for industrial motors] Moulds designed for a mix the buyer cannot source locally force a complete material requalification. When stacking is not included in the quotation, daily output sits on the floor waiting for manual handling, turning a rated capacity figure into a theoretical ceiling.
Why Specifying Through This Channel Reduces Risk
Block machinery is our single focus, so the QTJ4-25 press, its mould, pallets and handling equipment are specified as one matched system rather than assembled from separate suppliers. Configuration is set against your actual mix design, local aggregate and target block format — not a catalogue default. Mould design covers the formats your market sells, including custom drawings when standard sizes do not match. Automation level is selectable, meaning you can commission the line semi-automatic today and integrate stacking and cubing upgrades without replacing the press. Installation support includes on-site commissioning and operator training so the first production run happens under supervision, not trial and error.
Documentation & Verification
- Line layout with capacity calculation stating the block format assumed for each output figure
- Machine specification sheet covering PLC parameters, vibration settings and power draw
- Mould drawing and format list with dimensional tolerances per block type
- Voltage and control language confirmation signed off before production begins
- Factory test record demonstrating cycle timing on your specified block format
Installation, Commissioning & Support
- Foundation pad sized to 6400×1500 mm footprint with level tolerance specified for vibration isolation
- Dedicated circuit rated for 17.9 kW with voltage and frequency confirmed before wiring
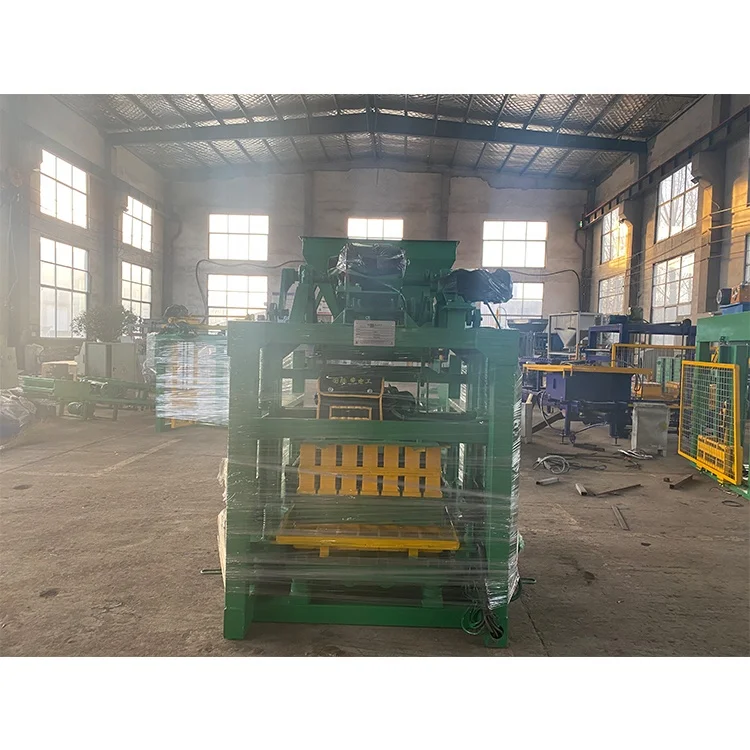
- Machine shipped partially dismantled for container loading with reassembly guide included
- PLC parameter set loaded and tested on your block format during commissioning visit
- Operator training covers recipe selection, mould change procedure and daily maintenance checkpoints
- Wear parts list with hydraulic seals and mould liner replacements identified for first reorder
What to Include in Your Inquiry
Tell us which block format your market demands — hollow, solid, paver or kerbstone — along with the target daily output and the raw materials available locally. Share your existing pallet dimensions and curing rack layout so we can confirm the 850×550 mm pallet fits your handling system. Specify the voltage, frequency and PLC display language required at your site to avoid commissioning delays once the automatic QTJ4-25 block making machine PLC controlled system arrives.
Frequently Asked Questions
Q: How do I verify output capacity for each block format I plan to produce?
A: Request a capacity calculation that states the mould type, cycle time and block dimensions for each format. A 25-second cycle applies to a specific mould and mix; switching to a denser solid block or a thinner paver changes the timing. We provide per-format output tables so your daily production plan reflects what the line actually delivers.
Q: What PLC language and voltage options should I confirm before production starts?
A: The control panel can be configured to your operator’s language, and the electrical system is built to match your local voltage and frequency. Confirm these during the quotation stage — changing a PLC display or motor after the machine ships causes avoidable commissioning delays on site.
Q: Can I start semi-automatic and add full stacking and cubing later?
A: Yes. The QTJ4-25 platform supports a defined upgrade path from manual pallet handling through to automatic stacking and cubing. You can commission the line semi-automatic and integrate downstream automation modules when production volume and floor space justify the addition.
Q: How is vibration force matched to my local raw material and mix design?
A: The 60 kN exciting force and 2800 r/min frequency are baseline settings. We adjust vibration duration and hydraulic pressure to suit your specific aggregate gradation and cement ratio, then validate block density during factory testing before the machine is approved for shipment.