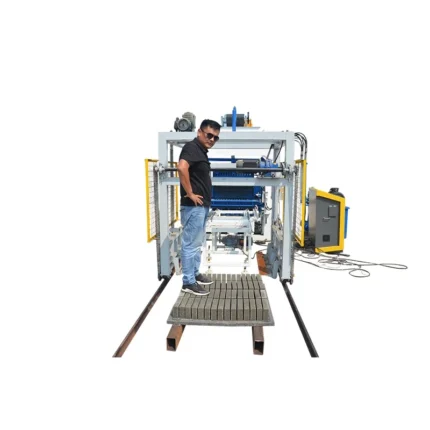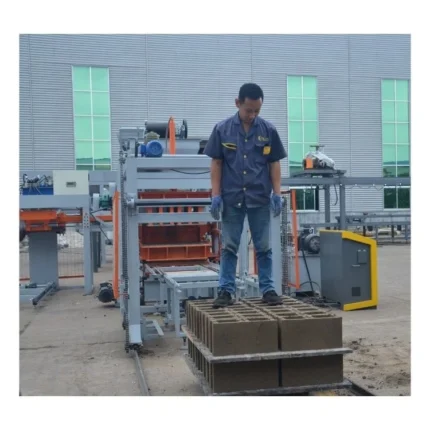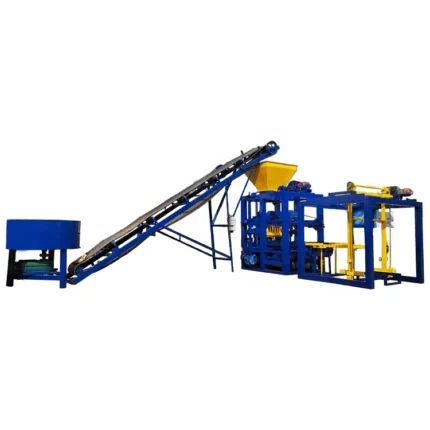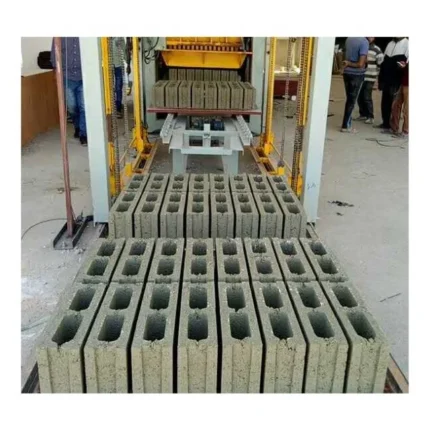



Description
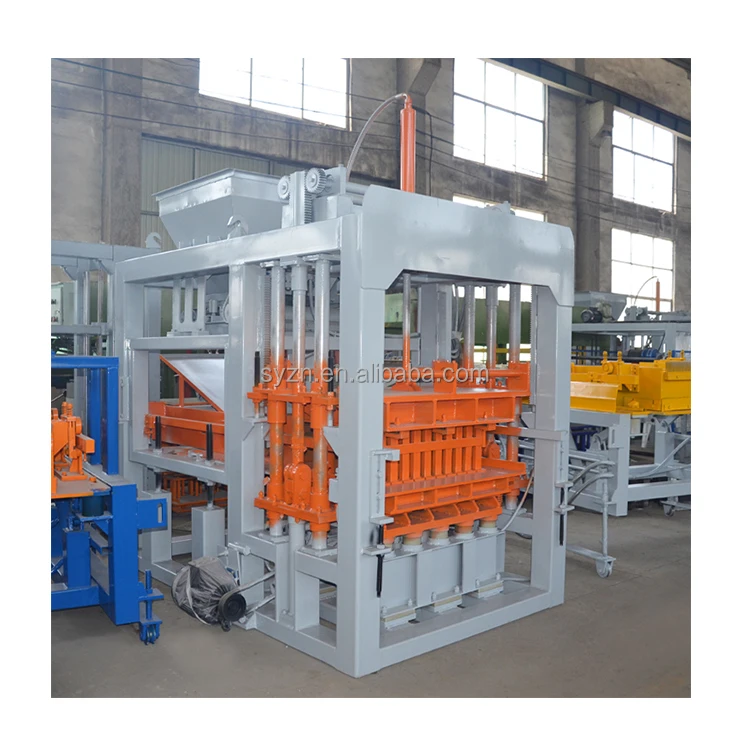
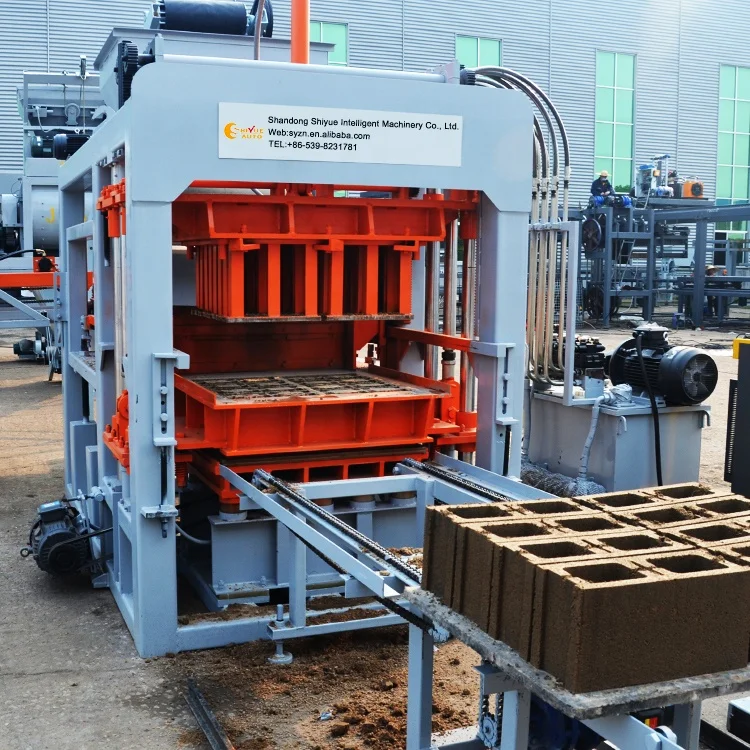
Matched Vibration and Pressure — The QT6-15 hydraulic station and vibration frequency are configured together against the buyer’s actual mix design rather than pulled from a default catalogue, keeping block density consistent shift after shift.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Fully Automatic Hydraulic Block Making Machine |
| Model | QT6-15 |
| Overall Dimensions | 7400 × 1900 × 2660 mm |
| Molding Cycle | 15–25 s |
| Vibration Frequency | 4600 r/min |
| Exciting Power (Vibration Force) | 40–50 kN |
| Total Power | 31.25 kW |
| Mixer Model | JQ350 |
| Pallet Size | 850 × 550 × 25 mm |
| Total Weight | 7 T |
| Control System | PLC control system |
| Hydraulic Station | Included |
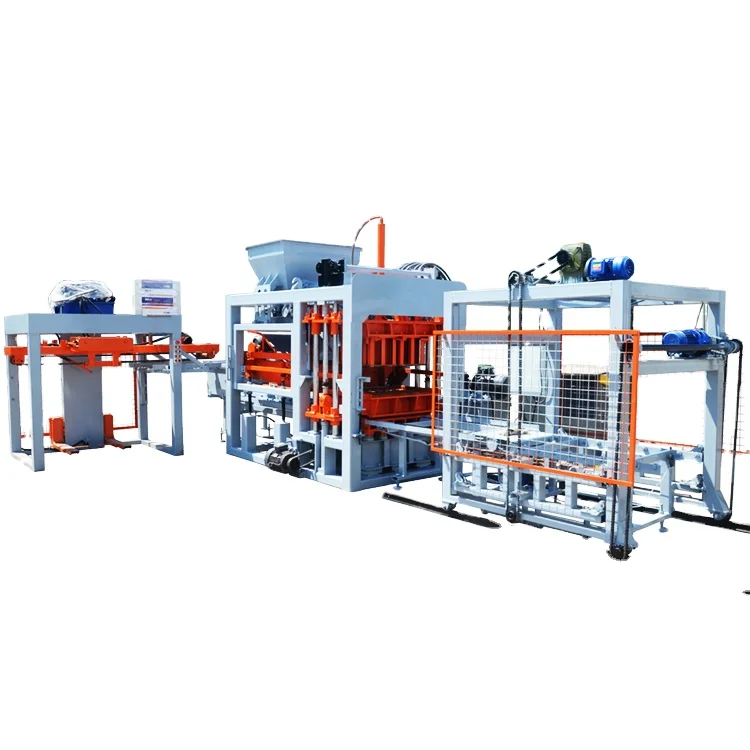
| Included Equipment | Block making machine, hydraulic station, PLC control system, pallet feeder, brick conveyor, block sweeper |
| Free Accessories | Manual hydraulic trolley, spare parts and tools |
| Applied Products | Paver, solid brick, hollow block, curbstone |
| Raw Materials | Crushed stones, sand, cement, dust, fly ash |
| Output — Hollow Block 400×200×200 mm | 1200–1680 pcs/h, 9600–13440 pcs/8 hr (basis: 400×200×200 mm hollow block, cycle 15–20 s) |
| Output — Hollow Block 400×150×200 mm | 1800–2400 pcs/h, 14400–19200 pcs/8 hr (basis: 400×150×200 mm hollow block, cycle 15–20 s) |
| Output — Solid Brick 240×115×53 mm | 3240 pcs/h, 16200–19440 pcs/8 hr (basis: 240×115×53 mm solid brick, cycle 15–20 s) |
| Automation Level | Fully automatic |
| Packing | Nude packing in 20GP container, approx. 500 pcs pallets loaded |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for wall construction | Crushed stone, sand, cement and fly ash mixes |
| Solid brick manufacturing for load-bearing structures | Standard concrete mixes with local aggregates |
| Interlocking paver production for roads and yards | Pigmented face-mix and base-mix concrete |
| Curbstone and kerbstone forming | High-density concrete with coarse aggregate |
| On-site block production for housing projects | Locally sourced sand, dust and cement blends |
What "Fully Automatic" Should Actually Mean on the Shop Floor
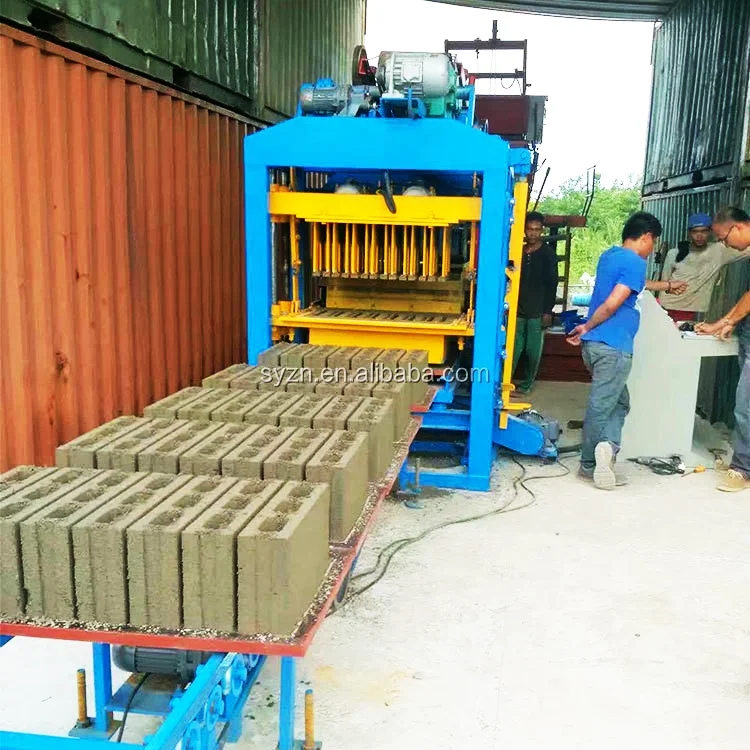
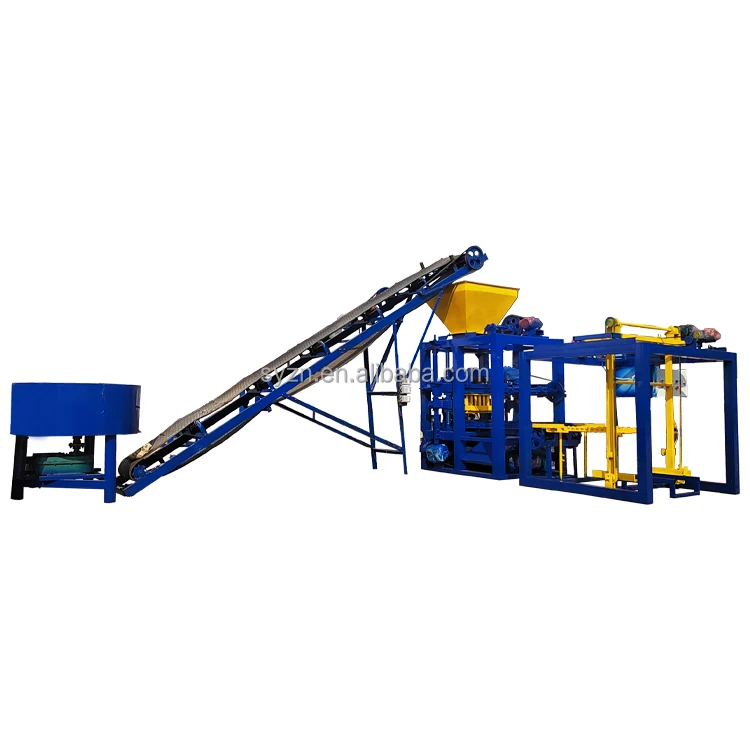
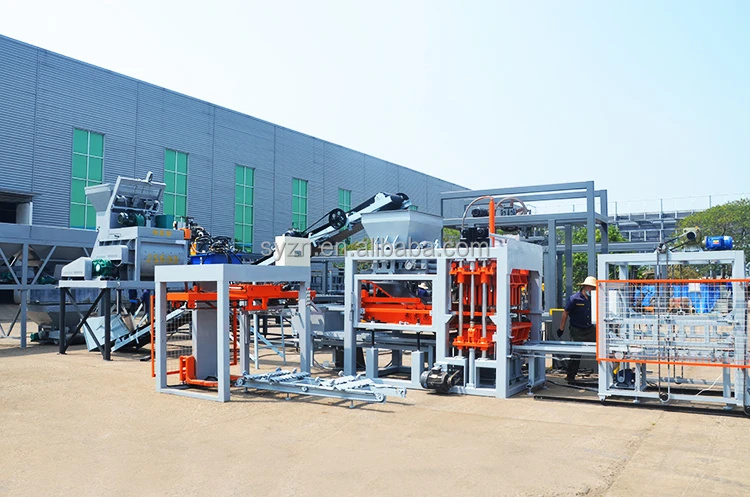
Many quotations list an automatic PLC controlled block making machine but leave pallet feeding, stacking and conveying to the buyer’s labour force. The QT6-15 package includes a pallet feeder, brick conveyor and block sweeper so the press cycle is never interrupted by manual handling gaps.
I once visited a plant where the press was rated for respectable output, yet two workers stood at the discharge end pulling pallets by hand because the line stopped every few cycles waiting for someone to clear the conveyor. The actual daily tally fell well below what the brochure promised. That kind of mismatch is exactly what pushes a buyer to ask for a line-level drawing before signing [NEED_CITE: typical block plant line layout and station synchronisation].
Removing the Operator from the Pressing Cycle
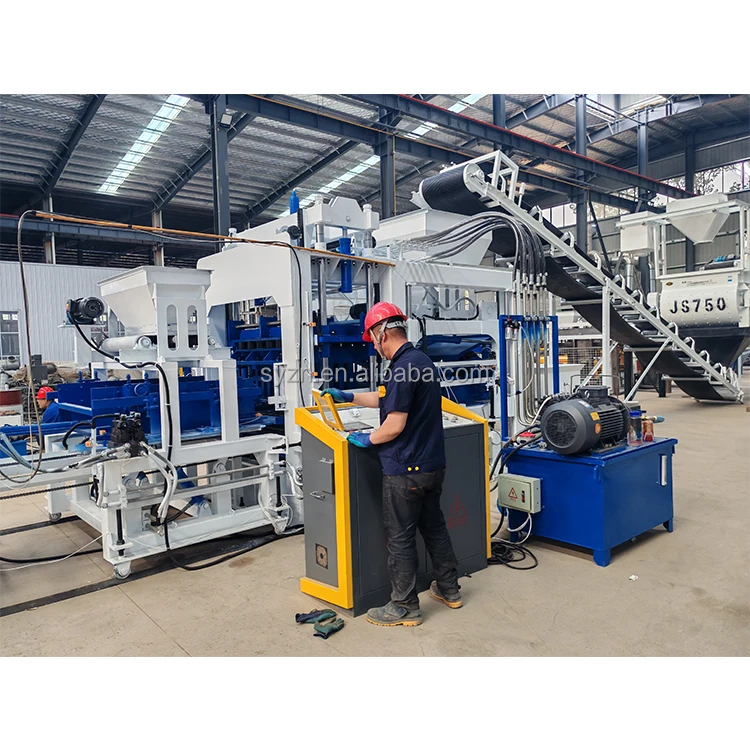
The PLC control system on the QT6-15 manages mould filling, vibration timing, hydraulic pressure application and demoulding in a single programmed sequence. The operator monitors the HMI panel and intervenes only for mould changes or material adjustments. This shifts the role from manual lever-pulling to supervision, which matters when you run two shifts and need the second shift to produce blocks that match the first.
Where Consistency Comes From
Batch-to-batch consistency in block strength depends on keeping vibration force and hydraulic pressure aligned across every cycle. The QT6-15 hydraulic station holds pressure steady while the 4600 r/min vibration compacts the mix. When both values are set to match a specific aggregate profile, the blocks leaving the machine at hour eight carry the same density as those from hour one [NEED_CITE: hydraulic pressure and vibration matching for concrete block density].
Reading the Numbers That Matter
The 40–50 kN vibration force combined with hydraulic pressure determines how tightly the aggregate particles lock together inside the mould. Higher vibration without sufficient hydraulic clamping produces blocks with good surface finish but weak cores; higher pressure without enough vibration leaves unmixed pockets. The 15–25 s molding cycle range lets the operator extend dwell time when the mix contains more fines or fly ash, giving the material extra seconds to consolidate. Pallet size at 850 × 550 × 25 mm defines the mould footprint and must match the curing rack spacing and forklift tine width already in the plant. The JQ350 mixer feeds the press at a rate aligned with the cycle time so the hopper never starves.
The Cost of Ignoring the Pallet Question
Buyers who confirm the press but skip pallet specification often discover that the pallets arriving with the machine do not fit their existing curing racks or forklift. Replacing several hundred pallets after arrival adds a cost line nobody budgeted for. The pallets also have to match the vibration frequency — undersized pallets crack under 4600 r/min, while oversized ones jam the feeder [NEED_CITE: pallet sizing for vibration block machines].
Why Buyers Specify Here
Every component around the QT6-15 press — pallet feeder, conveyor, sweeper, hydraulic station and PLC panel — is sourced and tested as one system, so cycle times match across stations. The machine configuration is set against the buyer’s actual aggregate sample and target block format, not a generic default. Mould designs cover the formats the buyer’s market actually sells, with custom drawings available. Automation is selectable, so a plant can start with the standard QT6-15 package and add stacking or cubing modules later. Commissioning includes operator training at the site so the crew knows mould change procedure and daily maintenance before the first production run [NEED_CITE: block machine commissioning and training practices].
Documentation & Verification
- Line layout drawing with capacity calculated per target block format
- Machine specification sheet matching the quoted QT6-15 configuration
- Mould drawing and format list for every block type ordered
- Hydraulic and electrical schematic with confirmed voltage and frequency
- Factory test record on buyer’s mix design before dispatch
- Operation and maintenance manual in operator’s language
Installation, Commissioning & Support
- Foundation plan sized to the QT6-15 footprint of 7400 × 1900 mm with vibration isolation
- Dedicated power circuit rated for the 31.25 kW total draw at confirmed voltage and frequency
- Machine arrives dismantled for 20GP container loading with reassembly on site
- First-run parameter tuning matched to local aggregate and target block density
- Operator training covering PLC navigation, mould change and daily lubrication points
- Wear parts list with reorder codes for hydraulic seals and vibration components
Before You Send the Inquiry
Share your target block formats, the daily output you need per format, and the local aggregate you plan to use — a sieve analysis helps. Confirm your site voltage, frequency and the language your operators read so the PLC display and manuals arrive in a usable form. Let us know what pallet size and curing rack setup you already have, so the feeder and pallets are specified to fit.
Frequently Asked Questions
Q: How is the capacity figure verified and what block format is it based on?
A: Every capacity number we quote states the exact block format and cycle time it assumes. For the QT6-15, hollow block output of 1200–1680 pcs/h is based on 400×200×200 mm blocks at a 15–20 s cycle. If your target format differs, we recalculate against that specific mould and provide the revised figure before you commit.
Q: What automation level does the QT6-15 include, and what is the upgrade path?
A: The standard package is fully automatic with PLC control, automatic pallet feeding, brick conveying and block sweeping. If you later need automatic stacking or cubing, the line layout reserves space and the PLC program supports adding those modules without replacing the press or control cabinet.
Q: Is the PLC display language configurable for the operator’s market?
A: Yes. Before production starts we confirm the display language, manual language and electrical labels so everything arrives in the language your crew reads. This avoids a situation where operators guess at alarm messages during the first week of production.
Q: How are hydraulic pressure and vibration force matched to local aggregate?
A: We ask for a sample or sieve analysis of your crushed stone, sand and any fly ash you plan to use. The vibration frequency and hydraulic pressure on the QT6-15 are then adjusted so the mix compacts fully without segregating, keeping block strength consistent across the shift.