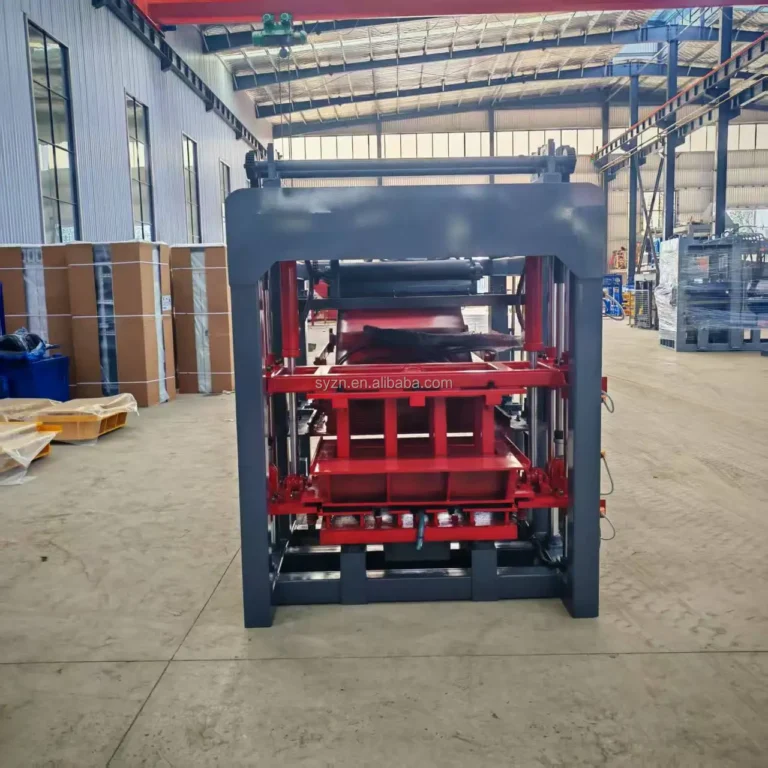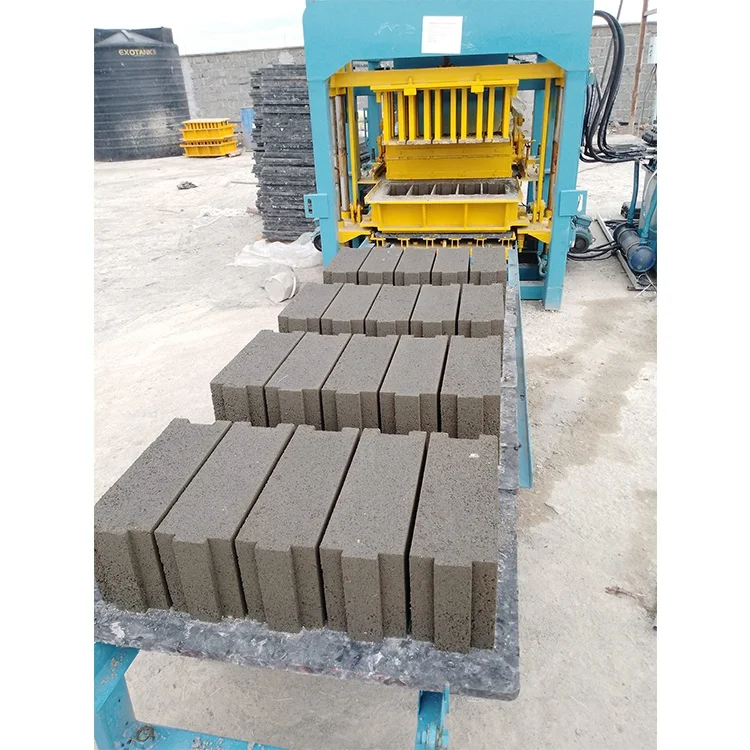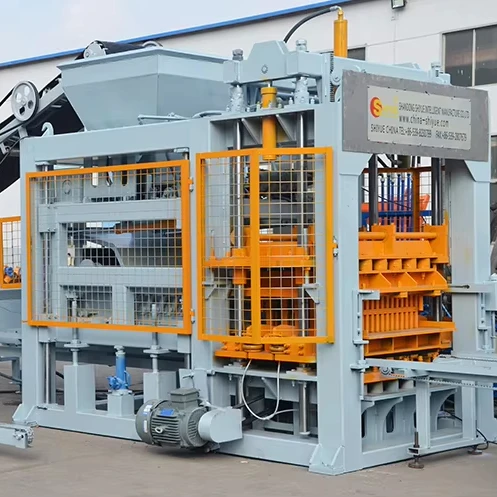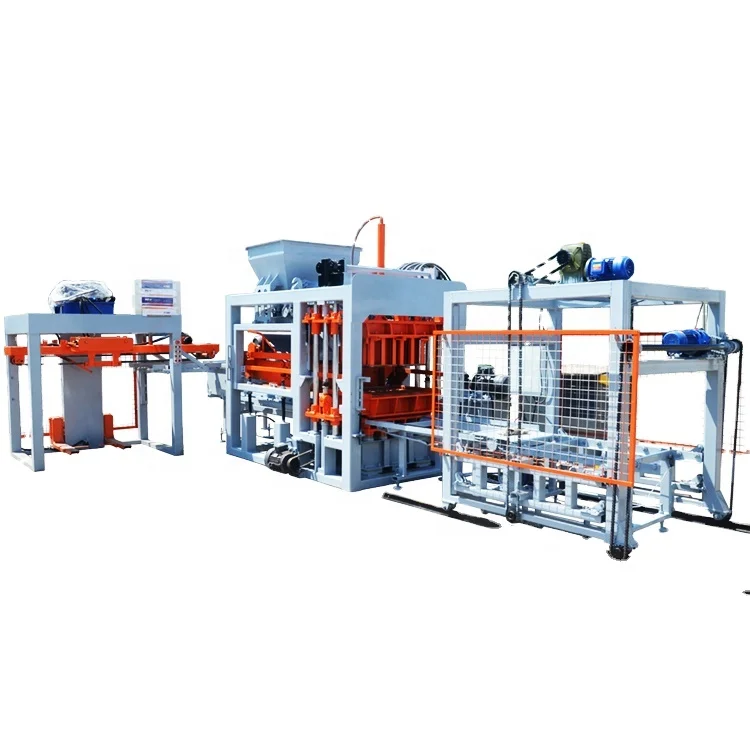


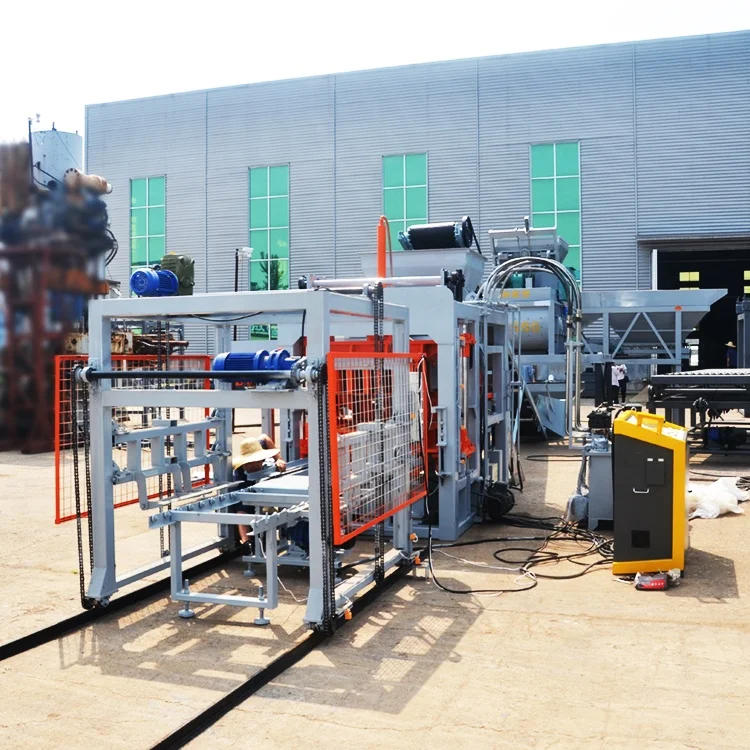
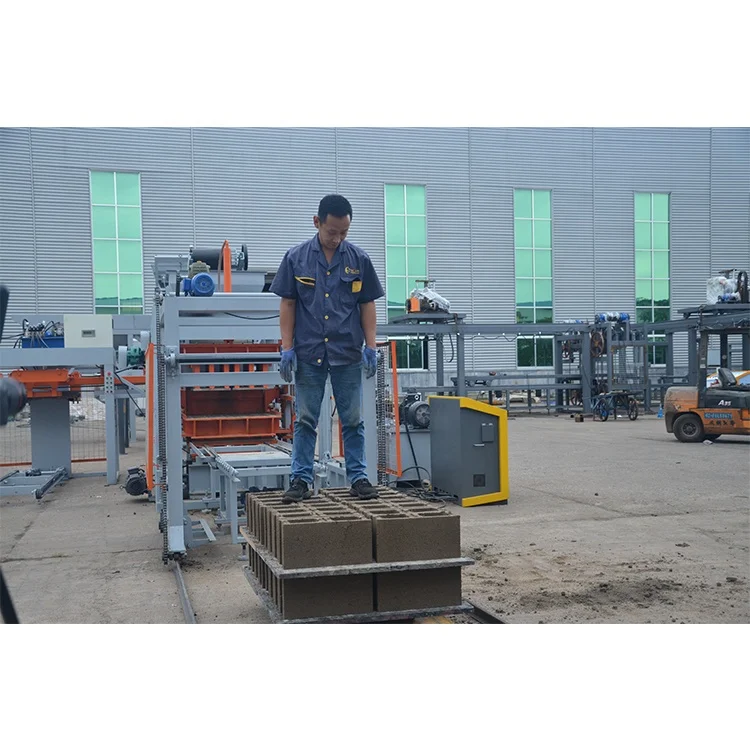
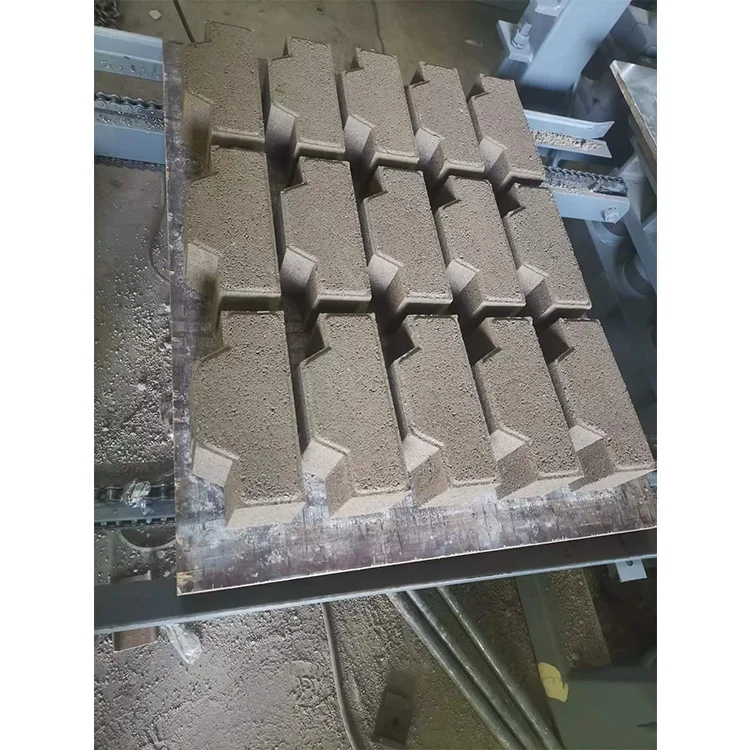
Description
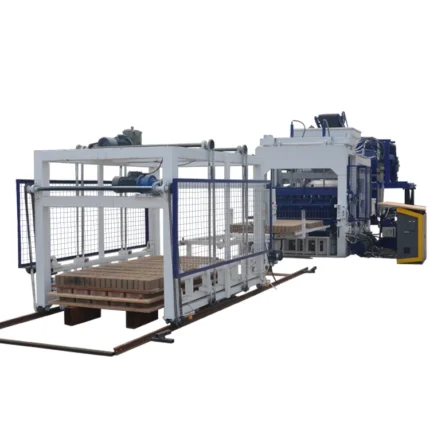
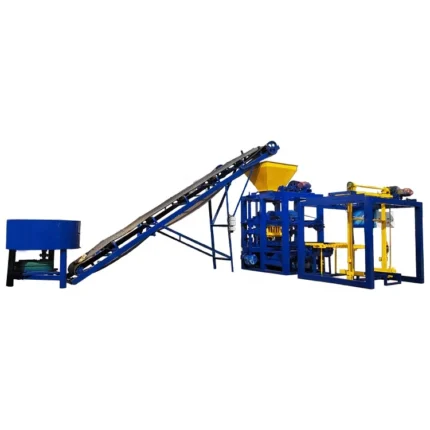
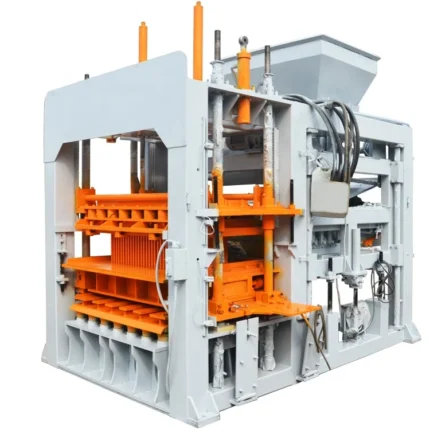
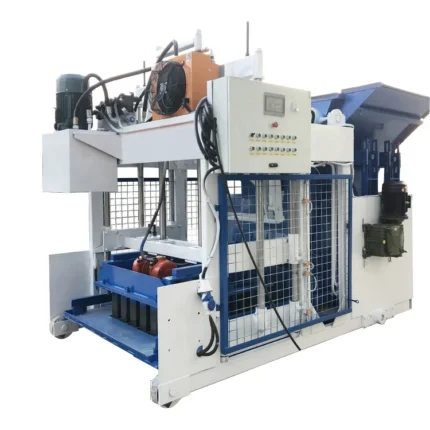
Intelligent PLC integration — every control loop on the QT6-15 is mapped to the buyer’s actual interlocking brick format, so automation reduces variables rather than hiding them.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT6-15 |
| Product Type | Interlocking Block Making Machinery |
| Overall Dimension | 8200 × 1700 × 2950 mm |
| Total Mass | 7 T |
| Overall Power | 37 kW |
| Control System | PLC (Programmable Controller) with touch screen interface |
| Vibration Form | Platform Vibration |
| Vibration Frequency | 0–60 Hz (adjustable) |
| Vibration Force | 45 kN |
| Moulding Mode | Automatic load, vibration moulding |
| Demolding Method | Hydraulic |
| Hydraulic System | Independent integrated type hydraulic station |
| Pallet Size | 880 × 850 mm |
| Molding Cycle | 15–20 s |
| Block Compressive Strength | More than 15 MPa |
| Output Capacity (Hollow block 400×200×200 mm) | 1080–1440 pcs/hour (basis: 6 pcs/mould, 15–20 s cycle) |
| Output Capacity (Hollow block 400×150×200 mm) | 1440–1920 pcs/hour (basis: 8 pcs/mould, 15–20 s cycle) |
| Output Capacity (Solid brick 240×115×53 mm) | 5760–7680 pcs/hour (basis: 32 pcs/mould, 15–20 s cycle) |
| Output Capacity (Rectangular brick 200×100×60 mm) | 2160–2880 pcs/hour (basis: 21 pcs/mould, 20–25 s cycle) |
| Output Capacity (Zigzag brick 225×112.5×60 mm) | 2160–2880 pcs/hour (basis: 15 pcs/mould, 20–25 s cycle) |
| Factory Area | 1200 m² |
| Raw Material Adaptability | Waste ash, slag, cement reduction capability |
| Standards | CE declaration where applicable |
Application Suitability
| Application | Material or Output |
|---|---|
| Interlocking brick production | Waste ash and slag blends with cement binder |
| Hollow block manufacturing | Crushed stone, sand, and cement mixes |
| Solid brick production | Fine aggregate and cement reduction formulations |
| Paving block production | High-density concrete with coarse aggregate |
| Construction material manufacturing | Industrial by-product ash and slag recycling |
What Happens When PLC Settings Ignore Your Local Aggregate
An automatic interlocking block making machinery PLC controlled system only delivers consistency when its parameters reflect the buyer’s actual mix, not a factory default.
I have stood on production floors in West Africa where a fully automated line produced interlocking bricks with visible density variation from one pallet to the next. The PLC was running cycle timings calibrated for river sand, while the plant was using laterite crushed on-site. The vibration frequency, hydraulic pressure, and dwell time were all technically correct — just not correct for that material [NEED_CITE: aggregate-specific vibration tuning in concrete block presses]. The operator had no way to adjust without the original programmer present.
Removing Operator Variables Without Removing Operator Control
The automatic interlocking block making machinery PLC controlled logic on this press manages load sequencing, vibration timing, and hydraulic demolding as one coordinated cycle. The touch screen interface displays each stage, and fault diagnosis routines isolate the fault to a specific sensor or actuator rather than triggering a generic alarm. When a plant upgrades from manual pallet handling, this level of control shortens the period before new operators produce saleable blocks.
Where Automation Reveals Hidden Line Bottlenecks
Once the PLC takes over moulding decisions, every upstream and downstream station becomes visible. If the mixer discharge takes longer than the press cycle, the automatic interlocking block making machinery PLC controlled system will wait — and the touch screen logs that idle time. Plant owners who previously blamed the press for low daily output often discover that raw material feeding or pallet circulation was the real constraint [NEED_CITE: line-balancing principles in concrete product plants]. Automation does not create bottlenecks; it exposes them.
Reading the Spec Sheet Against Your Production Reality
The 45 kN vibration force and 0–60 Hz adjustable frequency define what the platform can deliver to the mould, but the actual block density depends on how that energy transfers through your specific aggregate gradation. A coarse slag mix absorbs vibration differently from fine sand, which is why the PLC stores multiple recipe profiles rather than a single set of parameters.
The independent integrated hydraulic station sits away from the main press frame, isolating it from dust ingress and vibration fatigue. This matters most at the demolding stage: a 7-tonne machine generating 45 kN of vibration force transfers significant shock through the frame, and hydraulic valves contaminated with concrete dust fail unpredictably. The isolation extends component service intervals noticeably.
Pallet size at 880 × 850 mm determines not just what fits in the press but what fits the buyer’s existing curing racks and forklift tines. Specifying pallets without confirming curing area layout leads to double-handling that cancels out the labour savings automation was supposed to deliver.
The Cost of Getting the Control Language Wrong After Arrival
A PLC with full fault diagnosis is only useful if the operator can read the display. I have seen commissioning delayed because the touch screen arrived in a language the local electricians could not follow, and reprogramming required a software license the buyer did not have [NEED_CITE: PLC language configuration requirements for exported industrial machinery]. Voltage and frequency confirmation, display language, and PLC program backup should all be locked before the machine leaves the factory — not discovered during installation.
Why Sourcing the Control System and the Press Together Matters
Block machinery as a single focus means the PLC program is written around the same mould catalogue the buyer selects from, not adapted from an unrelated press. Configuration is set against the buyer’s actual mix design, local aggregate, and target interlocking brick format rather than defaulting to a generic cycle.
Automation level is selectable: a buyer can commission the QT6-15 in semi-automatic mode with manual pallet handling and upgrade to automatic stacking and cubing later, without replacing the PLC. Mould design covers the formats the buyer’s market actually sells, and custom drawings are accepted for non-standard interlocking profiles.
Installation and commissioning include operator training on the specific PLC interface, and the wear parts and mould list is confirmed before shipment so the first replacement cycle does not halt production.
Documentation & Verification
- Factory test record run on your specified interlocking brick format before dispatch
- PLC control logic document showing action interlocks and fault diagnosis parameters
- Voltage, frequency, and display language confirmation signed off prior to shipment
- Hydraulic and electrical schematic matching the as-built independent integrated station
- Machine specification sheet stating capacity per format with cycle time assumptions
Installation, Commissioning & Support
- Foundation plan sized to the 8200 × 1700 mm footprint and 7-tonne operating mass
- Dedicated 37 kW power circuit with voltage and frequency confirmed to local grid standards
- PLC touch screen language set and verified during pre-shipment factory test
- Hydraulic station commissioned and cycle timings tuned to buyer’s aggregate on-site
- Operator training covers fault diagnosis reading and recipe profile selection
- Wear parts and mould list locked before shipment to prevent unplanned line stoppage
What We Need to Size the Right Configuration
Share the interlocking brick profile you intend to produce and your target daily output so the cycle time and mould configuration can be calculated per format rather than quoted as a generic figure. Confirm your local voltage, frequency, and preferred PLC display language so commissioning proceeds without delay on arrival. If you already have curing racks or forklifts on-site, send the pallet dimensions they accept so the 880 × 850 mm pallet specification can be verified or adjusted.
Frequently Asked Questions
Q: What PLC display languages are available for local operators?
A: The touch screen interface supports multiple language configurations confirmed before shipment. The buyer selects the preferred display language during the voltage and control confirmation stage, and the factory test verifies all fault diagnosis messages and recipe labels render correctly in that language. Changes after dispatch require software access that may delay commissioning.
Q: Can the automation level be upgraded after initial installation?
A: Yes. The QT6-15 can be commissioned in semi-automatic mode with manual pallet handling and later upgraded to automatic pallet feeding, stacking, and cubing. The PLC program accommodates the upgrade path, and additional stations are integrated without replacing the main controller. The buyer should confirm the intended upgrade timeline during initial specification.
Q: How is cycle time verified for a specific interlocking brick format?
A: The factory test record runs the buyer’s specified mould through complete cycles, and the resulting molding cycle is documented per format. For the QT6-15, the molding cycle ranges from 15–20 seconds depending on block geometry and mix characteristics. The specification sheet states output capacity per format with the pallet and cycle assumptions included.
Q: Does the PLC support remote diagnostics for troubleshooting?
A: The fault diagnosis system isolates issues to specific sensors and actuators, displaying them on the touch screen. Remote diagnostics capability depends on the plant’s network infrastructure and should be discussed during the configuration stage. Hydraulic and electrical schematics are supplied so local technicians can perform independent troubleshooting without waiting for remote support.
Q: How does the system integrate with existing pallet handling equipment?
A: The 880 × 850 mm pallet size must match the buyer’s existing curing racks and forklift equipment. The automatic pallet feeding system is configured to accept pallets within that dimension range. If the buyer’s existing pallets differ, pallet specification is adjusted during the configuration stage to avoid double-handling after installation.