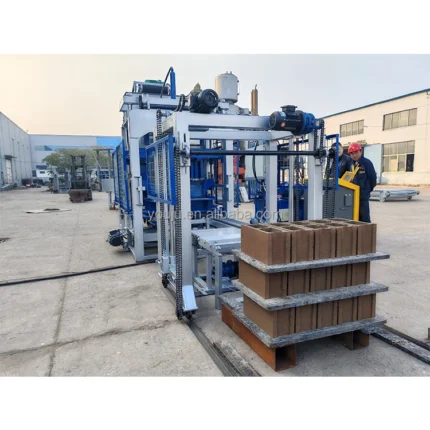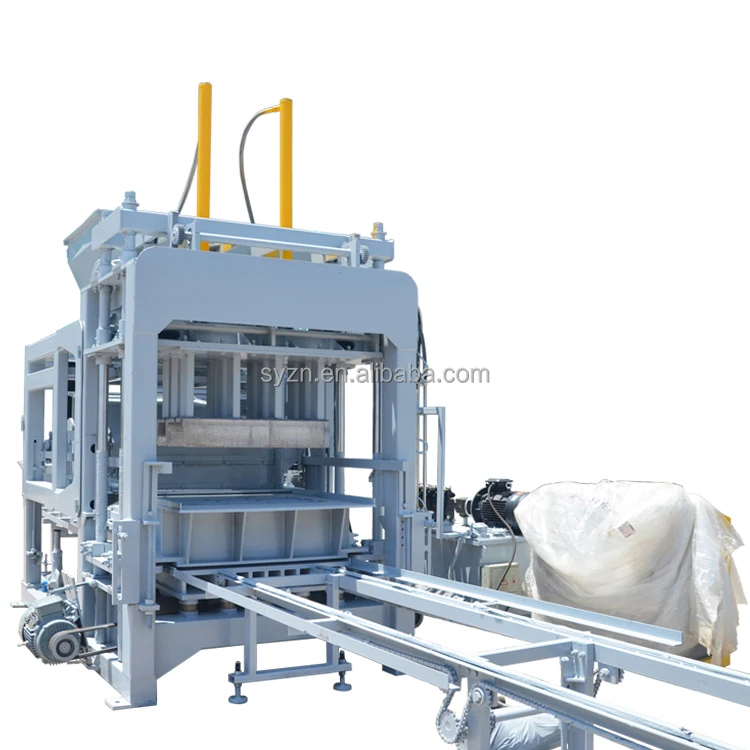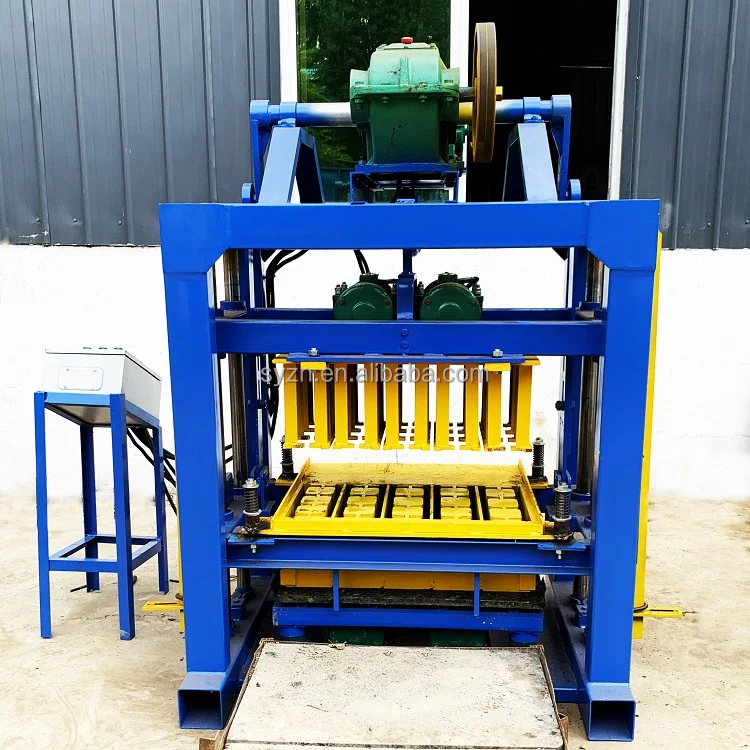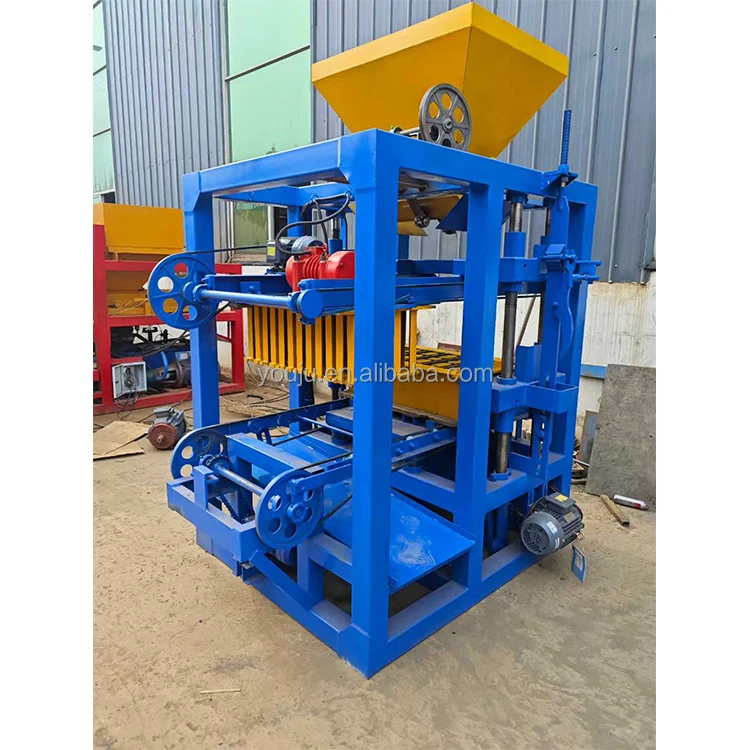
Description
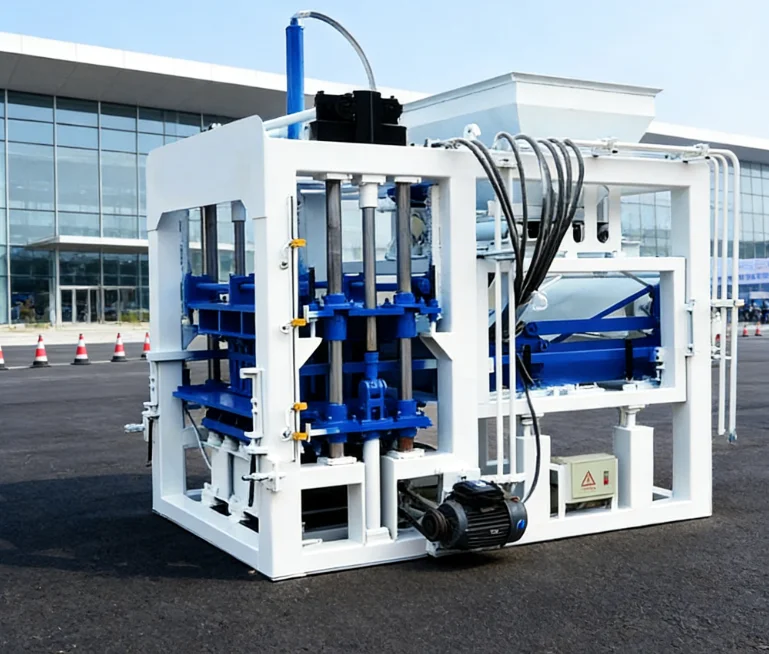
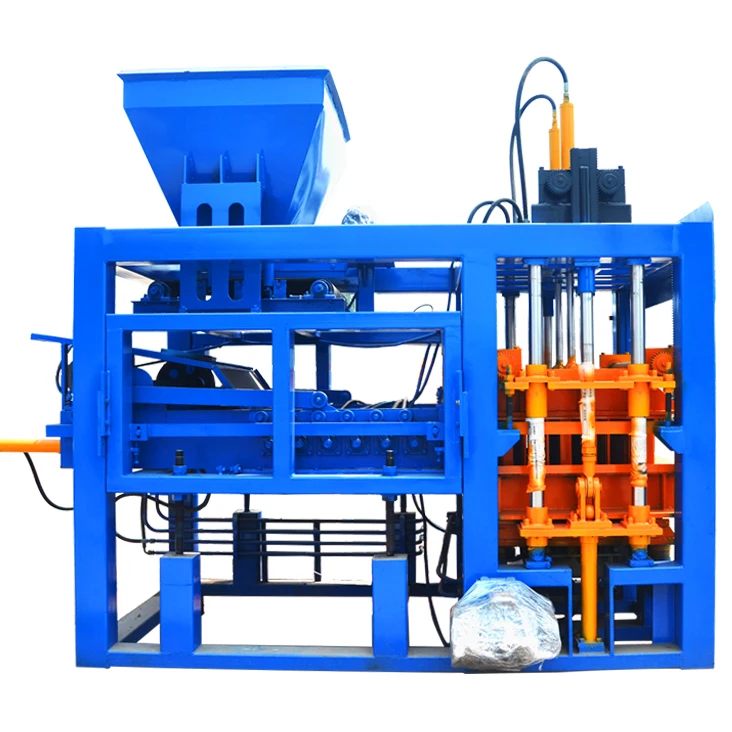
Consistency by Design — The QT8-15 automatic stationary concrete block making machine PLC controlled integrates fault diagnosis and remote monitoring so every cycle repeats within tight tolerances, removing guesswork from the operator.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT8-15 |
| Product Type | Automatic Stationary Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 8400 × 1700 × 2950 mm |
| Overall Power | 37 kW |
| Molding Cycle | 15–25 s (basis not stated in source — confirm block format / material / thickness) |
| Vibration Frequency | 2800–4500 r/min (variable) |
| Main Vibration Form | Platform vibration |
| Pallet Size | 950 × 900 mm |
| Machine Weight | 10,000 kg |
| Control System | PLC with fault diagnosis and remote monitoring |
| Automation Level | Automatic |
| Voltage | Customized to buyer’s local supply |
| Factory Area Required | 600 m² |
| Warranty | 1 year (excluding spare parts) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production | Crushed stone, sand, cement, fly ash aggregates |
| Solid block manufacturing | Dense concrete mixes for load-bearing walls |
| Paving block and colored paver runs | Fine aggregate blends with pigment dosing |
| Interlocking brick and kerbstone | Stiff zero-slump concrete on 950 × 900 mm pallets |
Why Stated Cycle Time Means Nothing Without the Block Format
The QT8-15 automatic stationary concrete block making machine PLC controlled states 15–25 seconds per cycle, but that range only becomes meaningful once the exact block format, wall thickness, and target density are defined.
Buyers frequently compare machines on a headline cycle figure, then discover on commissioning day that the hollow block they actually sell requires the slower end of the band. Vibration frequency and hydraulic dwell must match the mix design and local aggregate gradation; otherwise the press either under-compacts or over-stresses the green block [NEED_CITE: relationship between vibration frequency, aggregate size and compaction time in zero-slump concrete]. Without a format-specific capacity calculation, daily output projections remain guesswork.
How PLC Automation Removes Operator Variability
On a manually operated press, the cycle depends on the operator’s judgement of fill depth, vibration duration, and demould timing. The PLC on the QT8-15 locks each phase into a repeatable sequence, so batch-to-batch density stays uniform whether the shift starts at dawn or ends at dusk. Fault diagnosis routines flag hydraulic pressure drops or vibration motor anomalies before they produce off-spec output, giving the maintenance team a diagnostic code rather than a pile of rejected blocks.
Remote Monitoring for Off-Site Oversight
Remote monitoring and long-distance controlling capability let a plant manager review cycle logs, alarm history, and parameter settings from an office terminal. When an alarm triggers, the PLC identifies the subsystem at fault, cutting the time spent tracing wiring or swapping sensors blindly. For operations running multiple shifts, this visibility reduces unplanned stoppages and keeps the automatic stationary concrete block making machine PLC controlled within its intended duty envelope [NEED_CITE: remote diagnostics adoption in mid-size concrete product plants].
Reading the Specifications Against Your Mix and Format
The variable vibration frequency band of 2800–4500 r/min serves a specific purpose: the lower end settles the feed material into the mould cavity, while the upper end drives compaction once the head applies pressure. If the local aggregate is coarse crushed stone, the higher frequency may be required to achieve target block strength, whereas finer sand blends respond better to the mid-range. Platform vibration distributes force across the full 950 × 900 mm pallet area, so density variation from centre to edge stays within acceptable limits. The 37 kW overall power rating covers hydraulic pack, vibration motors, and pallet feed drives running simultaneously, so no auxiliary supply circuit is needed beyond the main breaker. Voltage and frequency are configured to the buyer’s local grid before production begins, avoiding transformer rentals on arrival.
The Hidden Cost of Skipping Configuration Verification
A pallet size chosen without checking the buyer’s existing curing racks and forklift capacity forces a workshop redesign after delivery. Unconfirmed PLC display language leaves operators reading alarm codes in a language they cannot parse, turning a minor sensor fault into a full-shift stoppage. Moulds ordered for a format the local market does not buy leave the press sitting idle while replacement tooling is fabricated and shipped [NEED_CITE: common causes of commissioning delays in exported block making equipment]. These oversights are not machine failures; they are specification failures that surface only when the line is expected to run.
Why Sourcing This Press Here Makes Sense
Block machinery is the single focus, so the QT8-15 press, mould, pallet, and handling equipment are specified as one matched system rather than assembled from unrelated suppliers. Configuration is set against the buyer’s actual mix design and local aggregate, not a catalogue default. Mould design covers the formats the buyer’s market sells, with custom drawings accepted. Automation level is selectable, allowing a buyer to start with the core press and add stacking or cubing stations later. Installation support includes on-site commissioning and operator training so the crew can run independent shifts from the first week.
Documentation & Verification
- Capacity calculation sheet stating block format and cycle time for each output figure
- Machine specification with hydraulic and vibration values matched to confirmed mix design
- Voltage, frequency, and PLC display language confirmation signed before production
- Factory test record showing cycle repeatability on buyer’s specified pallet and mould
- Packing photographs and customs documentation support for export clearance
Installation, Commissioning & Support
- 600 m² factory area required with level concrete slab rated for 10,000 kg static load
- Dedicated 37 kW power circuit with voltage and frequency confirmed before shipment
- PLC fault diagnosis walk-through during commissioning so crew reads alarm codes independently
- Operator training covers mould change sequence and vibration frequency adjustment per format
- Wear parts list identifies hydraulic seals and vibration motor bearings for first reorder
- Remote monitoring link established during commissioning for ongoing off-site diagnostics
Before You Request a Quotation
Confirm the exact block formats your market sells, the target daily output per format, and the local aggregate gradation available year-round. Share your site voltage, frequency, and preferred PLC display language so the electrical cabinet is wired correctly before dispatch. Indicate your existing pallet dimensions and forklift capacity, and whether you plan to add automatic stacking or cubing at a later stage.
Frequently Asked Questions
Q: How is daily output verified per block format and what cycle time is assumed?
A: Each quotation includes a capacity calculation that names the exact block format, wall thickness, and mould cavity count used to derive the output figure. The 15–25 second cycle band is mapped to specific formats, so you see realistic throughput for the hollow block or paver you actually sell, not a single headline number based on an unspecified product.
Q: What does the PLC remove from the operator and what consistency does it add?
A: The PLC automates fill depth timing, vibration duration, and demould sequence, eliminating manual judgement calls that cause density variation. Fault diagnosis codes direct maintenance to the exact subsystem, and cycle repeatability keeps block weight and strength uniform across every shift and every pallet.
Q: How are voltage, frequency, and PLC display language confirmed before shipment?
A: A written confirmation sheet covering supply voltage, phase configuration, frequency, and PLC interface language is signed before the electrical cabinet is wired. This prevents the need for on-site transformers or operator confusion over alarm messages in an unfamiliar language.
Q: What is the upgrade path from the current automation level to full stacking and cubing?
A: The QT8-15 is designed so automatic pallet stacking and cubing stations can be added to the existing PLC architecture without replacing the main controller. The upgrade adds the necessary sensors and drive interfaces while retaining all current cycle parameters and fault diagnosis routines.
Q: How does remote monitoring reduce unplanned downtime on site?
A: Remote monitoring lets a supervisor or service engineer review alarm logs and cycle parameters from off-site. When a fault occurs, the diagnosis code narrows the search to a specific component, so the technician arrives with the correct spare part instead of spending hours tracing circuits blindly.