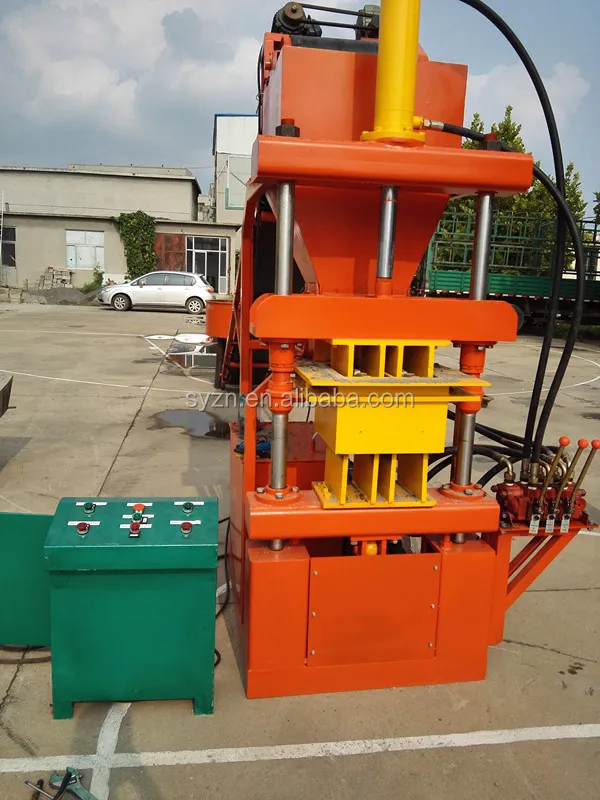
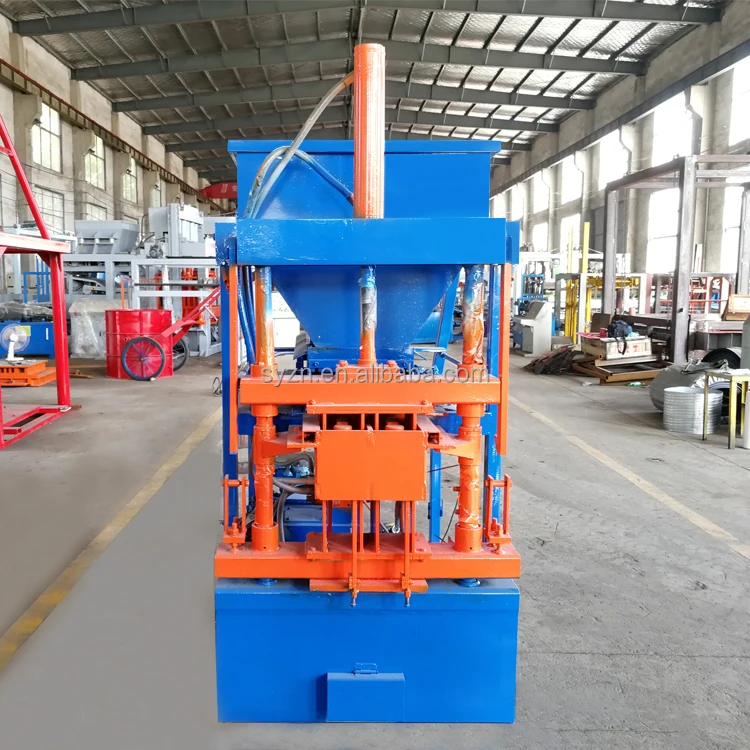
Description
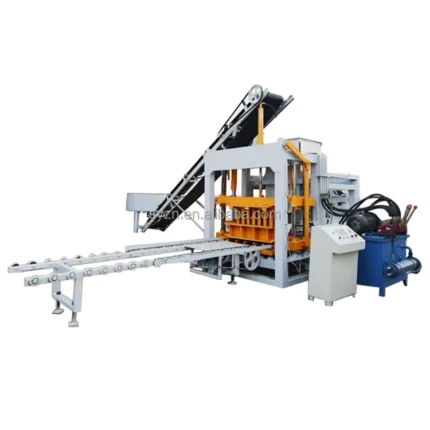
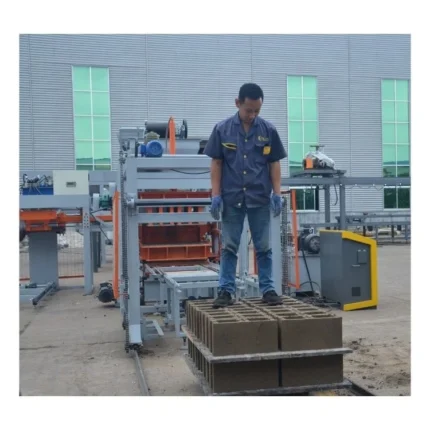
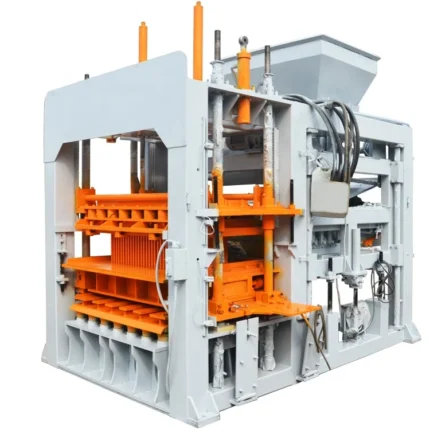
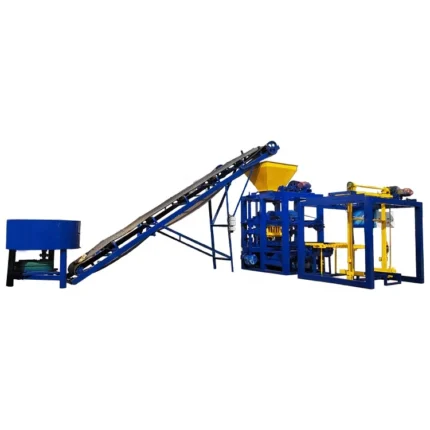
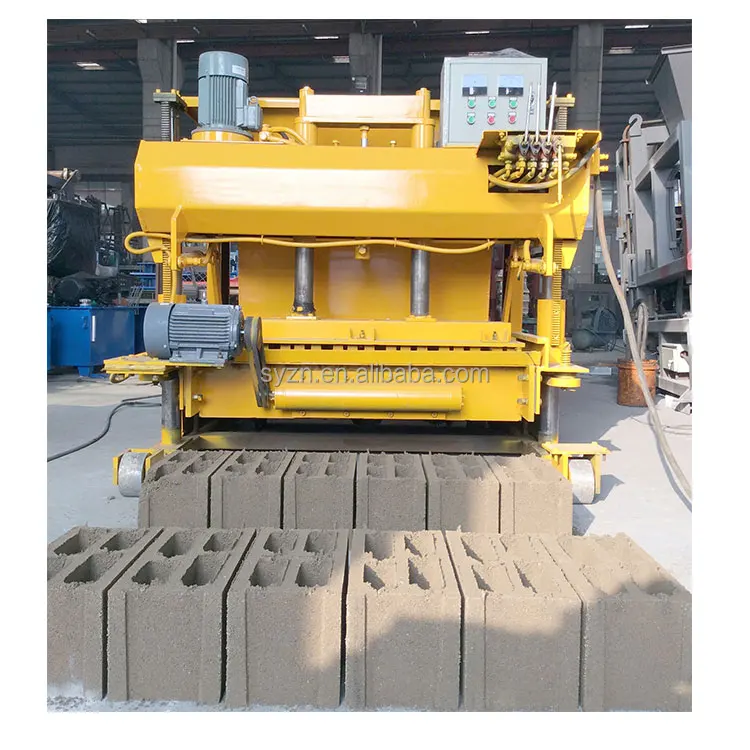
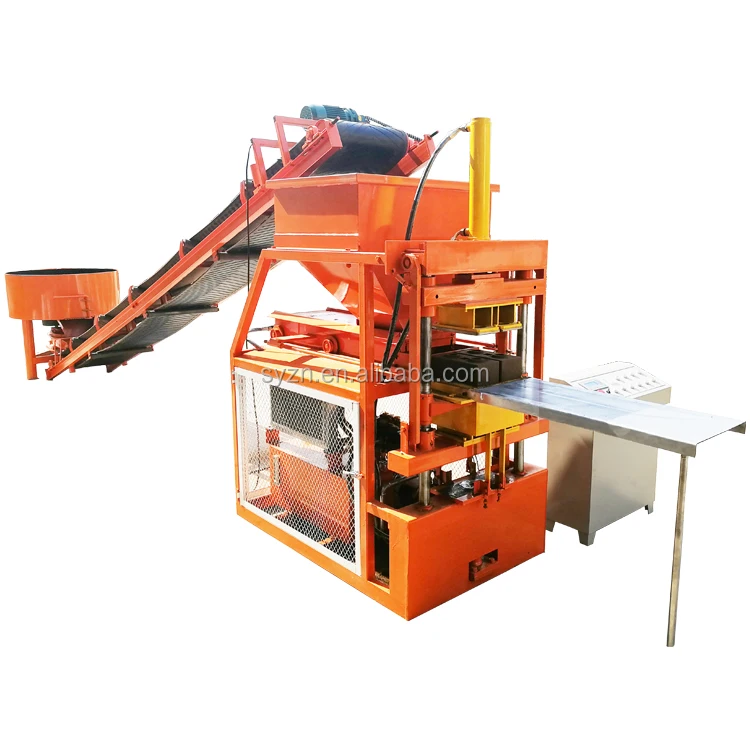
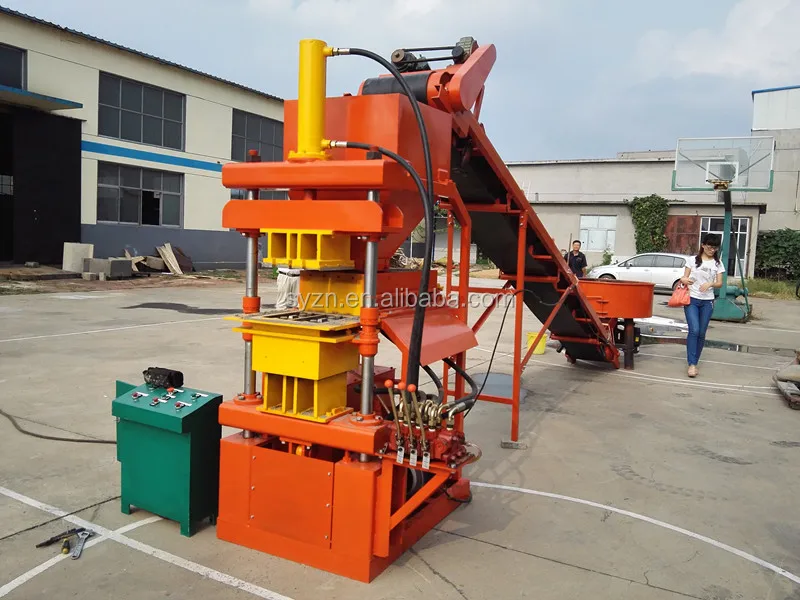
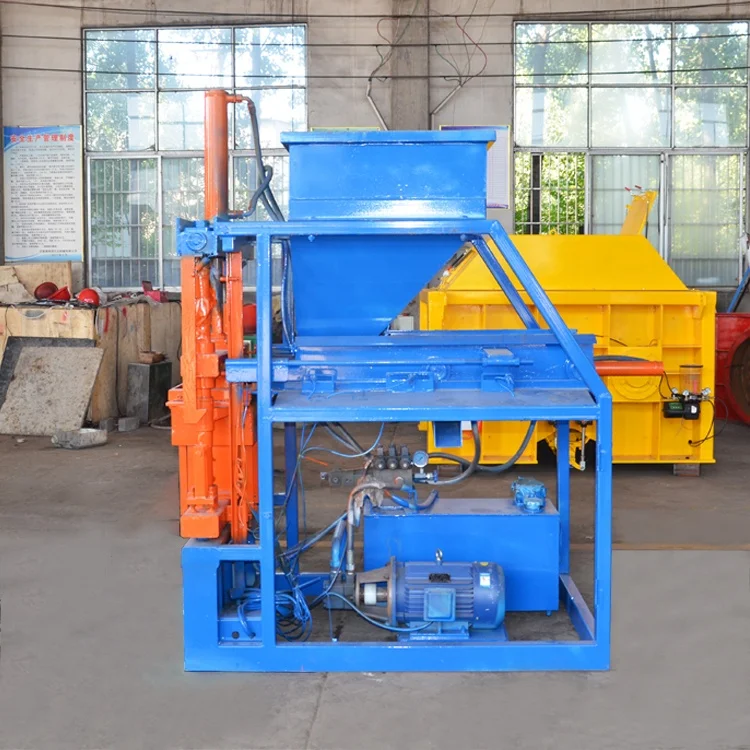
Configured as one matched system — the LY2-10 clay interlocking brick machine, its moulds, pallets and handling equipment are specified together against your actual clay mix and target brick format, so the press is never left waiting on upstream or downstream stations.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Clay Interlocking Brick Making Machine |
| Machine Type | Semi-automatic clay brick machine |
| Machine Power | 7.5 kW |
| Molding Cycle | 10 s |
| Output Capacity | 6000 pcs / 8 hours (basis not stated in source — confirm block format / material / thickness) |
| Raw Material | Clay, soil, earth, mud, concrete, cement, fly ash |
| Overall Dimensions | 1300 × 1800 × 2400 mm |
| Automation Level | Semi-automatic base, selectable PLC upgrade path |
| Mould Format Options | 300 × 150 × 100 mm (1 pc/mould), 250 × 125 × 75 mm (1 pc/mould), 230 × 220 × 115 mm (1 pc/mould) |
| Output per Mould Format | 750 pcs/hour (based on 10 s molding cycle, 1 pc/mould) |
| Key Features | Multi-format mould capability, semi-automatic operation, PLC upgrade path, wide raw material flexibility |
Application Suitability
| Application | Material or Output |
|---|---|
| Interlocking brick production for small to medium plants | Clay, soil, earth, and mud blends |
| On-site construction block production | Concrete, cement, and locally sourced aggregate |
| First brick plant for entrepreneurs | Fly ash, cement, and soil mixes depending on local availability |
Why "6000 Bricks per Shift" Can Mislead Your Planning
Capacity numbers only matter when tied to a specific brick format and mix design.
I once shipped a paver block machine to a South Asian buyer who sized his daily plan on the sample output figure. The local river sand had high silt content, so after vibration and pressing the brick surface dusted and strength never came up to spec. Daily output ended up at roughly half the quoted number because they had to slow the cycle and reject weak pieces. That is the gap a catalogue number leaves open. With this automatic clay interlocking brick making machine, we set the configuration against your actual material sample and the exact brick size your market sells, not a default assumption. [NEED_CITE: impact of local aggregate properties on block compressive strength]
From Manual Handling to Intelligent Control
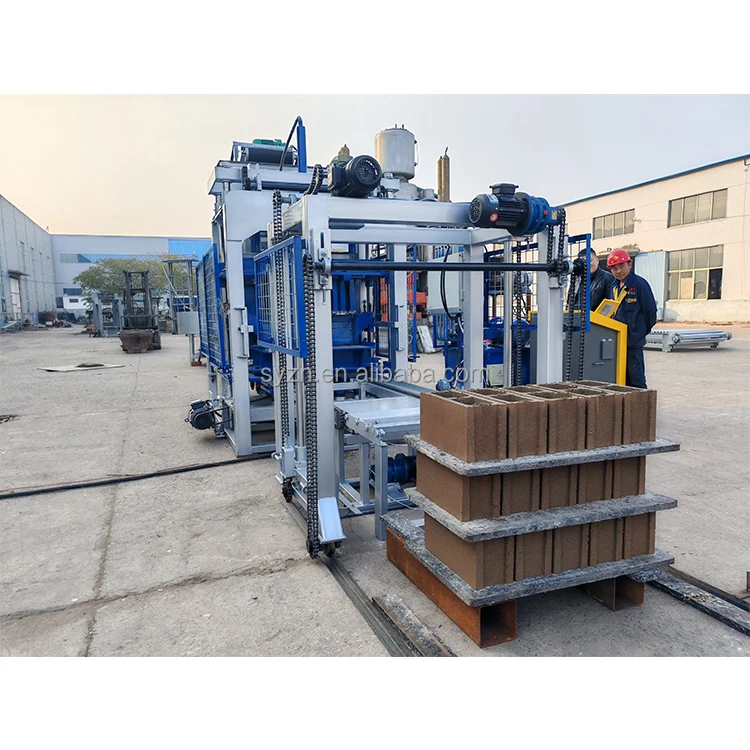
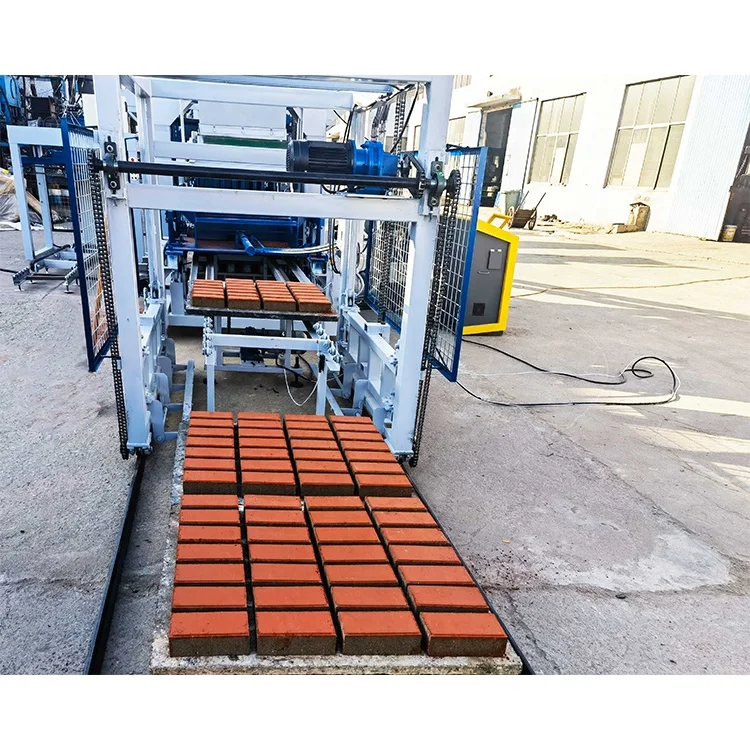
The LY2-10 starts as a semi-automatic clay brick machine where pallet feeding and stacking are handled by operators. The PLC controlled brick machine upgrade path lets you add automatic pallet feeding, stacking, and eventually cubing without replacing the press itself. This means a buyer setting up a first interlocking brick plant can begin with lower initial investment and add automation stations as volume grows and labour becomes the bottleneck.
Batch Consistency Through Automation Layers
When operators feed pallets and stack output by hand, cycle timing drifts across a shift and brick density varies from morning to afternoon. Moving to PLC control locks the molding cycle at a repeatable 10-second interval and standardises vibration and pressure application across every mould. The control system also logs cycle counts and alarm history, which gives a plant owner real data for maintenance scheduling rather than relying on operator memory. [NEED_CITE: PLC control systems in concrete block production lines]
Reading the Specifications That Actually Matter
The 7.5 kW motor rating sets the available power budget for both vibration and hydraulic pressure, which together determine how densely the clay or cement mix is compacted in the mould. Under-powered vibration leaves air pockets in interlocking profiles where the tongue-and-groove geometry requires full compaction. The three mould format options — 300 × 150 × 100 mm, 250 × 125 × 75 mm, and 230 × 220 × 115 mm — each present a different volume to fill within that 10-second cycle, which is why output per hour must be stated against the specific format being produced. The overall footprint of 1300 × 1800 × 2400 mm is compact enough for on-site contractor use but still requires clear space around the press for pallet staging and mould change access.
The Cost of Skipping the Configuration Step
Buyers who choose a machine based on a headline output figure and skip the material matching step often discover the problem only after the press is installed. Blocks crack during curing, interlocking profiles chip during handling, or the local aggregate simply will not compact at the default pressure setting. [NEED_CITE: common causes of block rejection in small-scale brick plants] Reworking the mix on site wastes weeks of production while the plant owner experiments with ratios that should have been tested before the machine left the factory.
What Sets This Machine Apart in Practice
Block machinery is the single focus of the factory, so the LY2-10 press, its moulds, pallets, and any handling equipment are specified as one matched system rather than assembled from separate suppliers. The configuration is set against your actual clay or cement mix and target brick format before a quotation is issued. Mould design covers the interlocking profiles your market actually sells, with custom drawings available when standard formats do not match. The automation level is selectable — you can start semi-automatic and upgrade individual stations later. Installation support includes commissioning and operator training so your team is producing saleable bricks before the engineer leaves site.
Documentation & Verification
- Line layout and capacity calculation stating the exact interlocking brick format assumed
- Mould drawing and format list confirming interlocking profile dimensions
- Voltage, frequency, and PLC display language confirmation before shipment
- Hydraulic and electrical schematic matching your installed automation level
- Factory test record on your clay or cement mix before dispatch
- Operation and maintenance manual with wear parts list
Installation, Commissioning & Support
- Floor plan based on 1300 × 1800 × 2400 mm footprint with pallet staging area marked
- Power supply matched to 7.5 kW motor with confirmed voltage and frequency
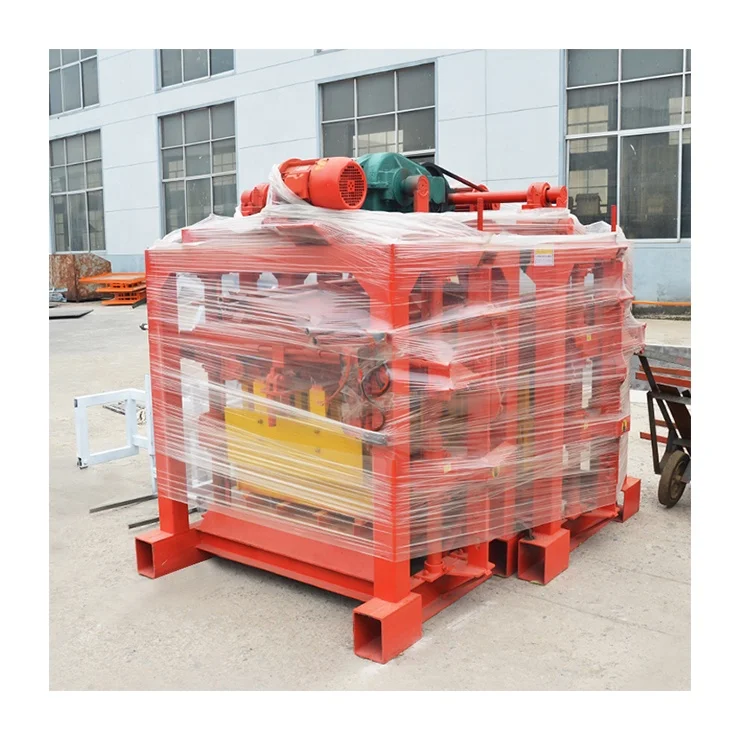
- Assembly state confirmed before shipment for your site lifting equipment
- First-run parameter setting against your clay sample and chosen mould format
- Operator training on mould change procedure across all three interlocking formats
- Wear parts and mould list provided with first recommended replacement intervals
What We Need to Size Your Line Correctly
Send us a sample of the clay, soil, or cement mix you plan to use, along with the interlocking brick dimensions your market requires. Tell us your target daily output, the automation level you want to start with, and the voltage and frequency at your site. If you already have pallets, a curing area, or a forklift in place, share those details so the handling configuration matches what you have on the ground.
Frequently Asked Questions
Q: How is the output capacity verified, and which brick format does it assume?
A: The quoted output figure must be read against a specific brick size, mix design, and shift length. We provide a capacity calculation sheet that states exactly which of the three interlocking mould formats was assumed, the molding cycle used, and the raw material composition, so you can plan your daily production against real numbers rather than a catalogue default.
Q: What automation upgrades are available from the semi-automatic base?
A: The LY2-10 supports a step-by-step upgrade path starting with PLC control to lock cycle timing, then automatic pallet feeding to remove manual pallet handling, and finally automatic stacking and cubing to reduce end-of-line labour. Each station can be added independently as your production volume grows.
Q: How are voltage, frequency, and PLC display language confirmed before shipment?
A: We confirm your site voltage and frequency during the quotation stage and specify the PLC display language before the control panel is wired. This avoids commissioning delays where the operator cannot read the screen or the motor will not start on the local power supply.
Q: How is the machine configured to match my local clay mix for consistent block strength?
A: We ask you to send a raw material sample before the configuration is finalised. The vibration force and hydraulic pressure settings are then matched to your clay or cement blend and the specific interlocking profile, so blocks reach target strength without surface dusting or cracking during curing.
Q: What is the mould change procedure between the three interlocking brick formats?
A: Each of the three mould sizes is designed for exchange on the same press frame. We provide a mould change procedure in the operation manual along with the required tools, and the commissioning engineer walks your team through the first changeover so the downtime between formats is predictable for your production schedule.