Description
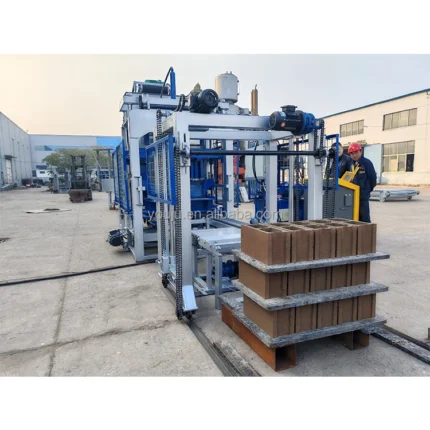
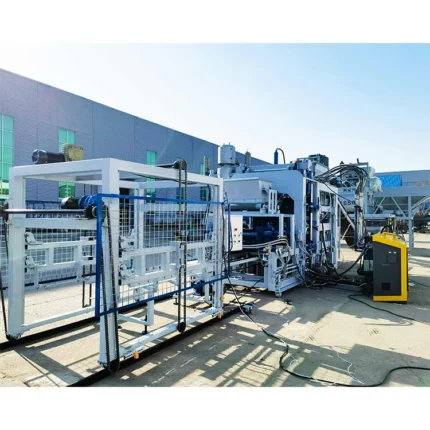
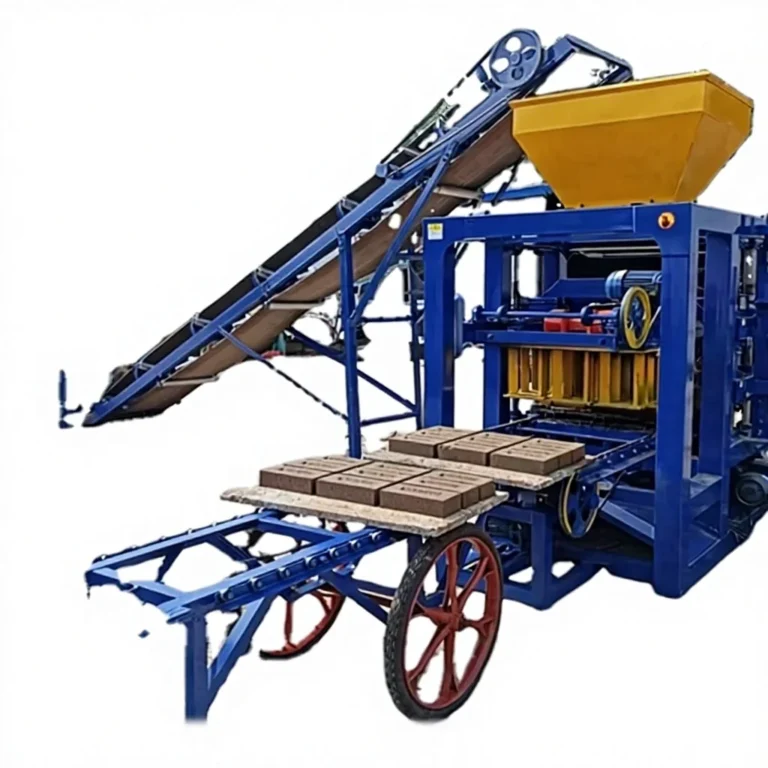
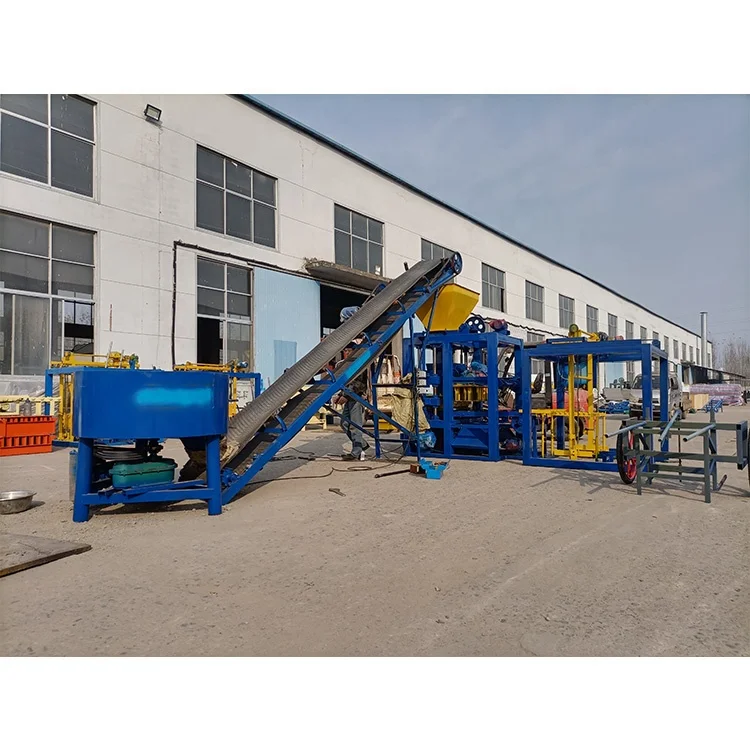
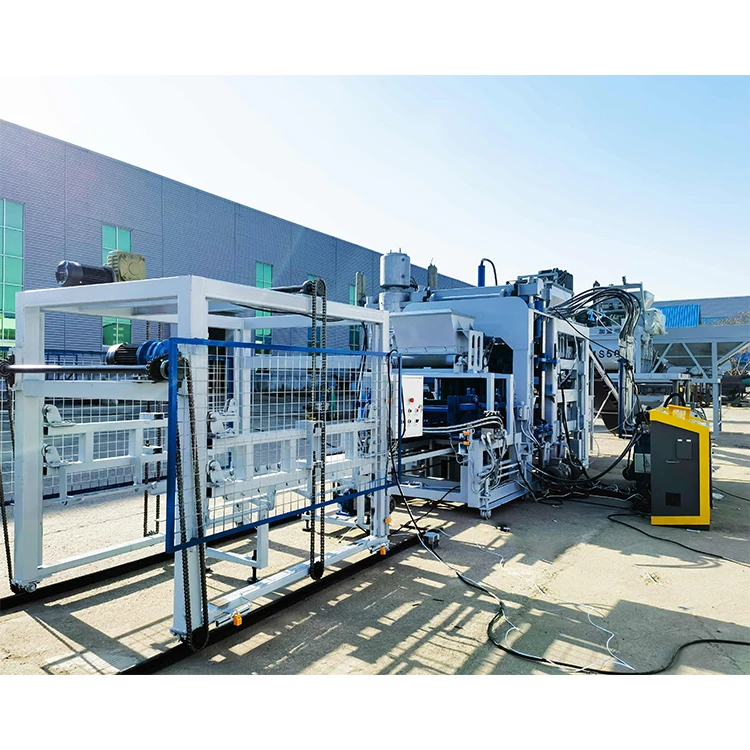
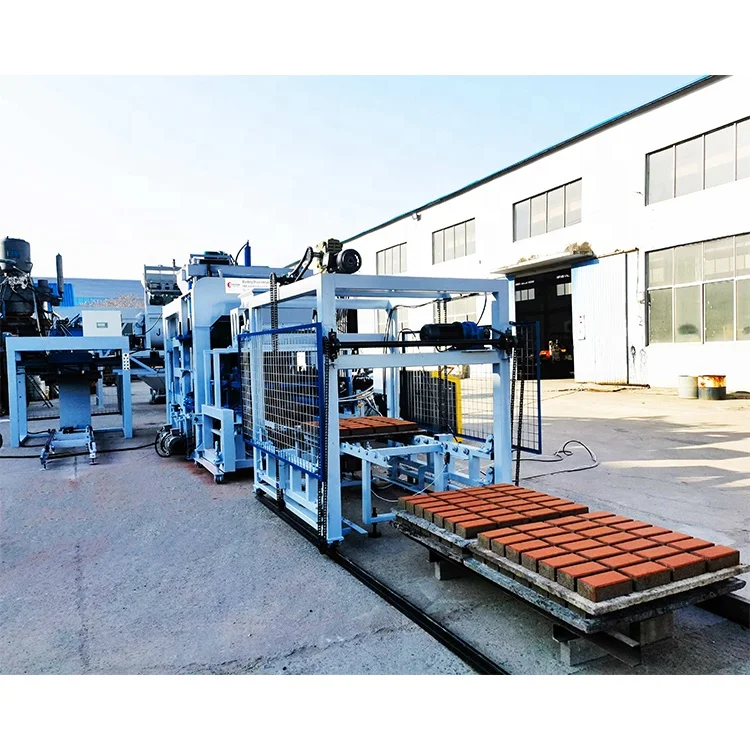
Single-Focus Machinery Design — every station from the mixer to the stacker is matched to the same mould format and cycle rhythm, so the press never waits on upstream bottlenecks or downstream pallet shortages.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Automatic Hydraulic Concrete Block Making Machine |
| Model | QT8-15 |
| Overall Dimensions (L×W×H) | 8300 × 1860 × 3000 mm |
| Total Mass | 9 T |
| Rated Pressure | 21 MPa |
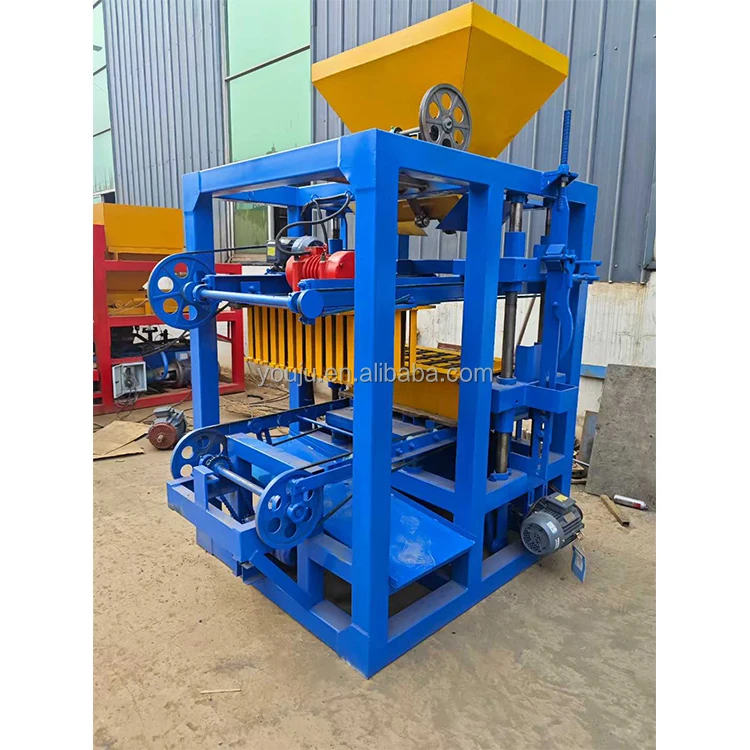
| Vibration Form | Platform Vibration |
| Vibration Frequency | 2800–4500 r/min |
| Vibration Force | 60 kN |
| Pallet Size | 950 × 900 mm |
| Molding Cycle | 15–25 s (basis to be confirmed per block format and material) |
| Overall Power | 55.5 kW |
| General Water Consumption | 12 T/Day (basis to be confirmed per production hours and format) |
| Factory Area Requirement | 600 m² |
| Control System | PLC with human-machine interface |
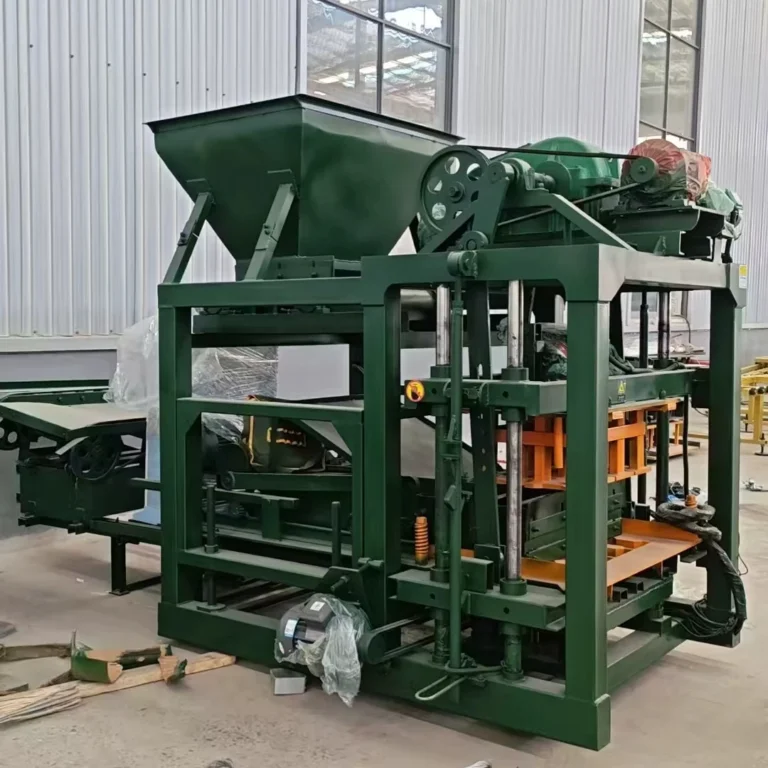
| Feeding System | Semi-closed screen reticular rotational forced feeding |
| Demolding Method | Hydraulic |
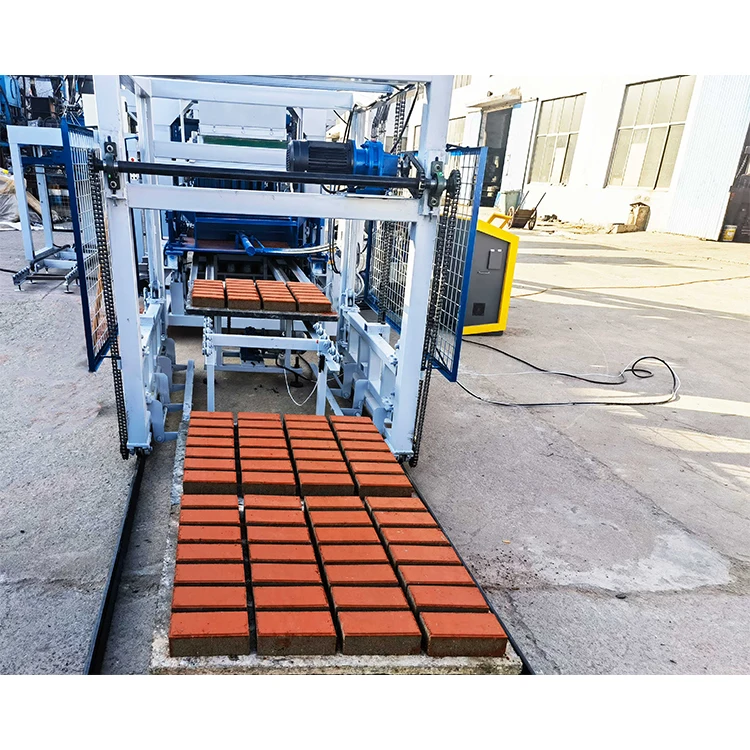
| Automation Level | Fully automatic (material feeding and stacking) |
| Raw Material Compatibility | Crushed stone, sand, cement, fly ash, gravel, slag, dust |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for commercial and residential walls | Crushed stone, sand, cement, and fly ash blends |
| Solid block manufacturing for load-bearing structures | Gravel and cement mixes with controlled moisture |
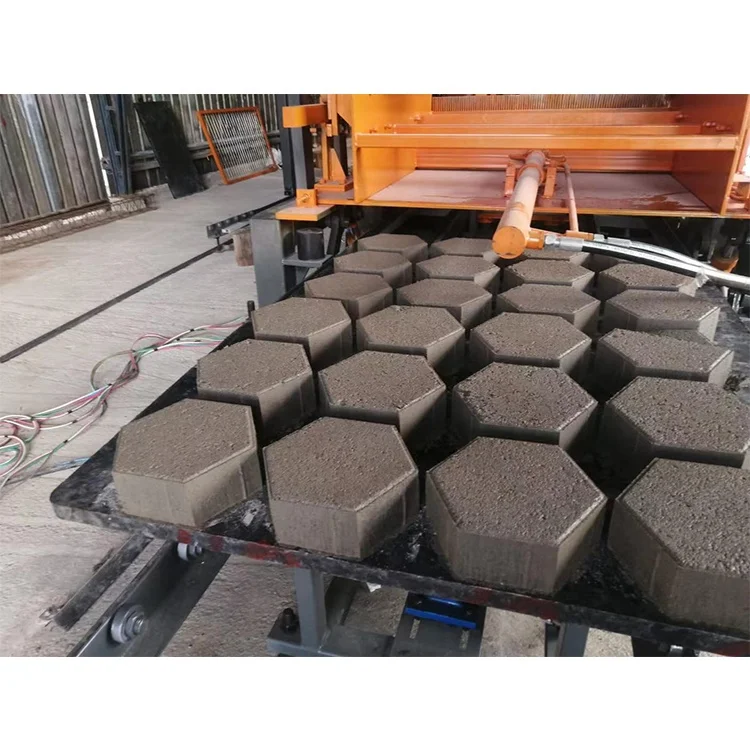
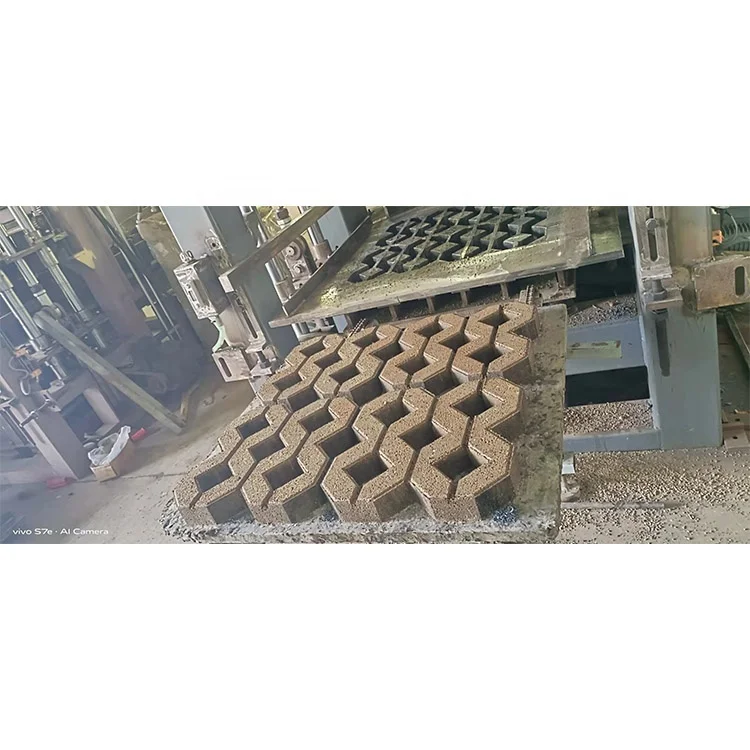
| Interlocking paver production for driveways and walkways | Fine aggregates with pigment additives |
| Curb stone forming for road and pavement edges | Coarse aggregate and high-strength cement ratios |
| Colored paving slab production for landscaping | Sand, cement, and iron-oxide pigments |
Why the PLC Question Should Come Before the Quotation
The automatic QT8-15 concrete block machine PLC controlled system is only as intelligent as the parameters loaded into it before shipment.
I once watched a buyer spend two weeks on commissioning because the PLC display arrived in a language his operators could not read, and the voltage tolerance did not match the local grid fluctuation pattern. The machine itself was fine; the configuration conversation simply never happened before production started [NEED_CITE: PLC language and voltage confirmation practices in export machinery]. When a plant owner is upgrading from manual or semi-automatic operation, these details determine whether the first week of production is a training exercise or a troubleshooting marathon.
Removing the Operator from the Cycle
The PLC human-machine interface uses a dialogue system that performs real-time signal analysis during each molding cycle. This means the automatic QT8-15 concrete block machine PLC controlled logic adjusts vibration timing and hydraulic pressure sequencing without requiring manual intervention at the press. For a plant transitioning from semi-automatic operation, this removes the most skill-dependent step from the production floor and places it inside a repeatable program.
Building an Upgrade Path That Actually Works
Starting with a semi-automatic pallet handling arrangement and adding automatic stacking later is a configuration choice, not a compromise. The control architecture on this machine allows stations to be added sequentially as the plant scales. A buyer who initially handles pallets manually can introduce automatic feeding and cubing modules without replacing the core press or rewriting the PLC program from scratch [NEED_CITE: modular automation expansion in stationary block production lines].
Matching Pressure and Vibration to Your Actual Mix
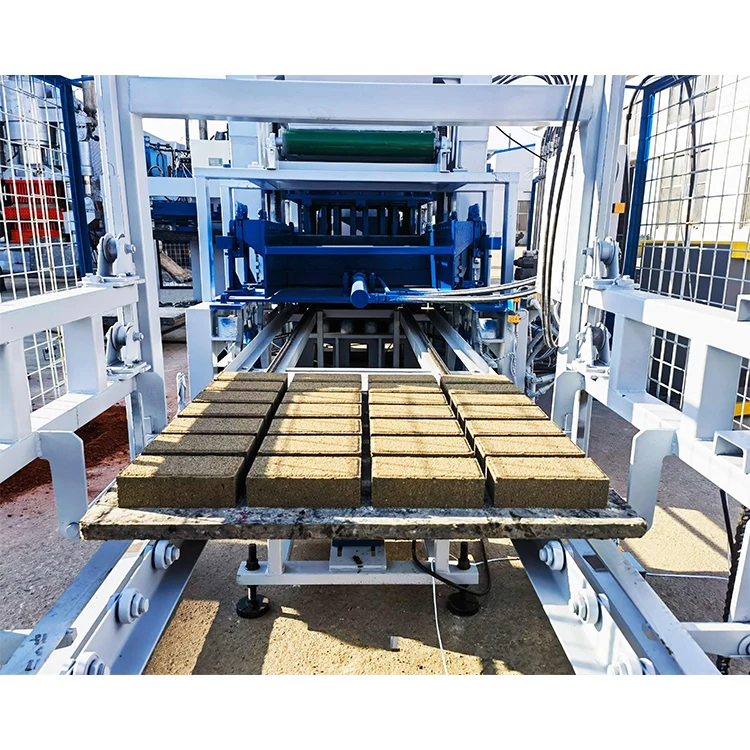
The rated pressure of 21 MPa and the platform vibration force of 60 kN are not independent numbers — they work together to compact the mix into the mould cavity. If your local aggregate has a high clay content, the vibration frequency range of 2800–4500 r/min may need to sit at the upper end to break air pockets that a cleaner material would not produce. This is why the automatic QT8-15 concrete block machine PLC controlled configuration must be set against your specific material sample, not a default catalogue profile. The semi-closed screen reticular rotational forced feeding system distributes material across the mould cavity uniformly, which matters most when particle size variation is wide.
What Happens When the Pallet Spec Is an Afterthought
The 950 × 900 mm pallet size was chosen to match the press output, but if your curing area uses a different pallet dimension or your forklift cannot handle the loaded weight, every pallet becomes a manual handling problem. I have seen plants where the stacking station sat idle for weeks because the pallet specification was never checked against the existing curing racks and transport equipment [NEED_CITE: pallet handling compatibility in block plant layout design].
Why We Configure Before We Quote
The machine, mould, pallet, and handling equipment are specified as one matched system rather than assembled from unrelated suppliers. Every quotation includes a capacity calculation that states which block format the cycle time assumes. Voltage, frequency, and PLC display language are confirmed before the machine enters production, not discovered during unpacking. Factory test records are run on the buyer’s target format. Mould drawings and a format list ship with the machine. Hydraulic and electrical schematics are provided so local maintenance teams can plan before the first replacement part is needed.
Documentation & Verification
- Line layout showing station spacing matched to the 8300 × 1860 mm machine footprint
- Capacity calculation sheet stating the specific block format behind each cycle time figure
- Mould drawing and format list for every block type in your initial production plan
- Hydraulic and electrical schematic matching the as-built configuration
- Voltage, frequency, and PLC display language confirmation record before production
- Factory test record run on your target block format and material blend
Installation, Commissioning & Support
- Foundation plan reflecting the 9 T total mass and platform vibration load distribution
- Power supply specification for 55.5 kW overall draw with dedicated circuit recommendations
- Dismantling and container loading plan with reassembly sequence at your site
- PLC parameter loading against your confirmed voltage, frequency, and language settings
- Operator training covering mould change procedure and semi-closed feeding system maintenance
- Wear parts list matching the hydraulic and vibration components specific to this configuration
What We Need from You to Start
Share your target block formats with dimensions, your daily output requirement by format, and a sample of your local aggregate so we can run a press trial before finalizing the vibration and pressure settings. Let us know your existing pallet size, curing area layout, and forklift capacity so the handling equipment is specified to match. Confirm your site voltage, frequency, and the PLC language your operators will use — these are locked in before production begins, not after arrival.
Frequently Asked Questions
Q: How is the QT8-15 cycle time verified per block format, and what daily output can I expect for my specific product?
A: The 15–25 second molding cycle range depends on block format, wall thickness, and material composition. We verify cycle time by running your specific block design on your material sample during factory testing. The capacity calculation we provide states the assumed format so daily output projections are honest, not based on the fastest possible cycle on the thinnest product.
Q: What automation stations are included, and what is the upgrade path from semi-automatic?
A: The base configuration covers automatic material feeding and stacking after forming. Pallet feeding, curing rack handling, and cubing can be added as separate modules. The PLC architecture allows these stations to be integrated later without replacing the press or reprogramming the core control system, giving you a genuine upgrade path rather than a full replacement.
Q: How is the PLC configured for my local voltage, frequency, and operator language before commissioning?
A: We confirm voltage, frequency, and PLC display language during the quotation stage and lock these values before production starts. The human-machine interface is loaded with your chosen language, and the electrical system is built to match your grid specification. This eliminates the most common commissioning delays we see on export shipments.
Q: How do I match vibration force and hydraulic pressure to my local aggregate and mix design?
A: Send us a sample of your local aggregate and your target mix ratio. We run a press trial adjusting vibration frequency within the 2800–4500 r/min range and hydraulic pressure up to 21 MPa to find the combination that produces consistent block density. These settings are then programmed into the PLC so every batch repeats the same cycle.
Q: What is the mould change procedure, and how long does a format switch take on the QT8-15?
A: Mould change time depends on the format difference and whether your operators have practiced the sequence. We provide a mould drawing and format list with every shipment, and our commissioning includes hands-on mould change training. The hydraulic demolding system simplifies removal since the mould releases under controlled pressure rather than mechanical force.