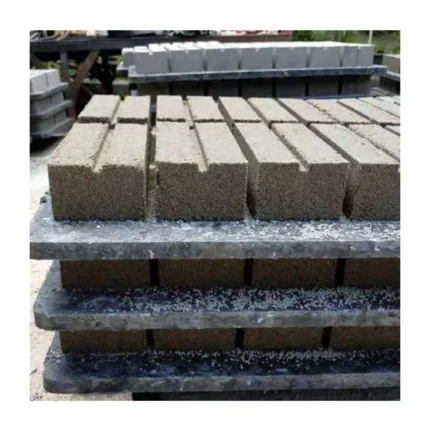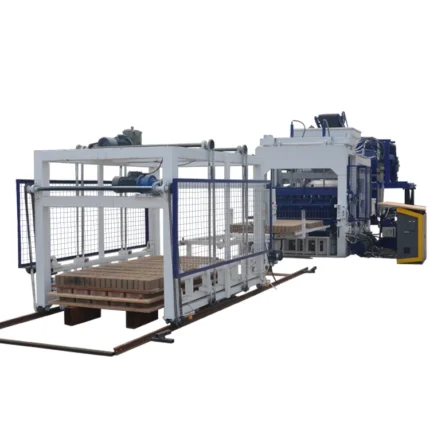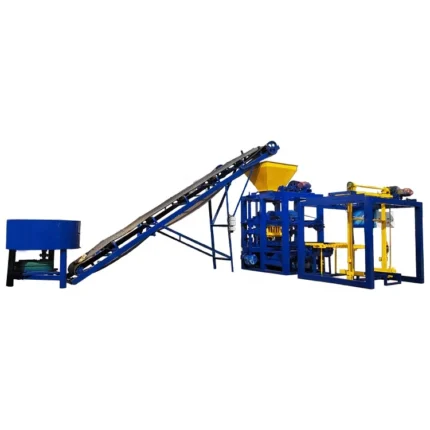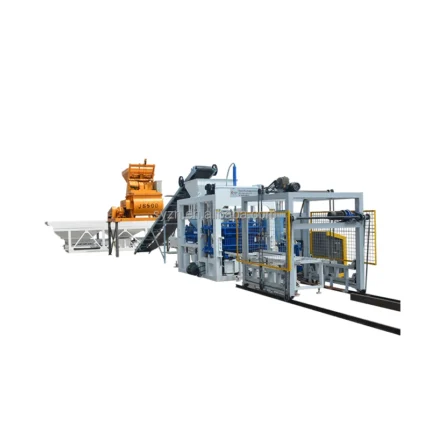
Description
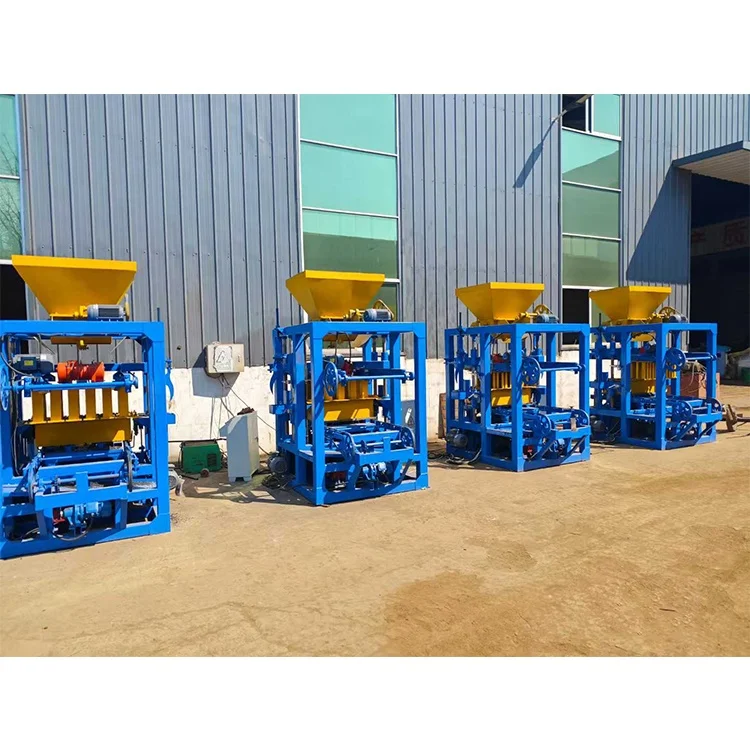
Electrical-mechanical interworking reduces faulty operation damage — the QTJ4-24 couples its control cabinet logic directly to the press mechanics so that an out-of-sequence operator input simply does not execute, keeping the semi-automatic cycle honest and laying the groundwork for a later PLC controlled semi-automatic block machine expansion.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-24 |
| Product Type | Semi-Automatic Concrete Block Making Machine |
| Rated Power | 11.95 kW |
| Overall Dimensions (L×W×H) | 3600 mm × 1700 mm × 2560 mm |
| Net Weight | 3.5 T |
| Pallet Size | 900 mm × 450 mm |
| Molding Cycle | 24–26 s |
| Mould Format Options | 400×200×200 mm (4 pcs/mould), 390×240×190 mm (3 pcs/mould), 390×120×190 mm (6 pcs/mould), 240×115×53 mm (21 pcs/mould) |
| Vibration Type | Table vibration feeding, fluctuation vibration molding |
| Feed Method | Manual feeding (two feed ways available) |
| Recommended Mixer | JQ350 or JQ500 vertical mixer |
| Recommended Conveyor | 6 m or 8 m belt conveyor |
| Control System | Electrical control cabinet with mechanical interworking (PLC / language / voltage to be confirmed per order) |
| Voltage & Frequency | To be confirmed per destination country |
| Automation Level | Semi-automatic (mechanical and manual combination), upgrade-ready |
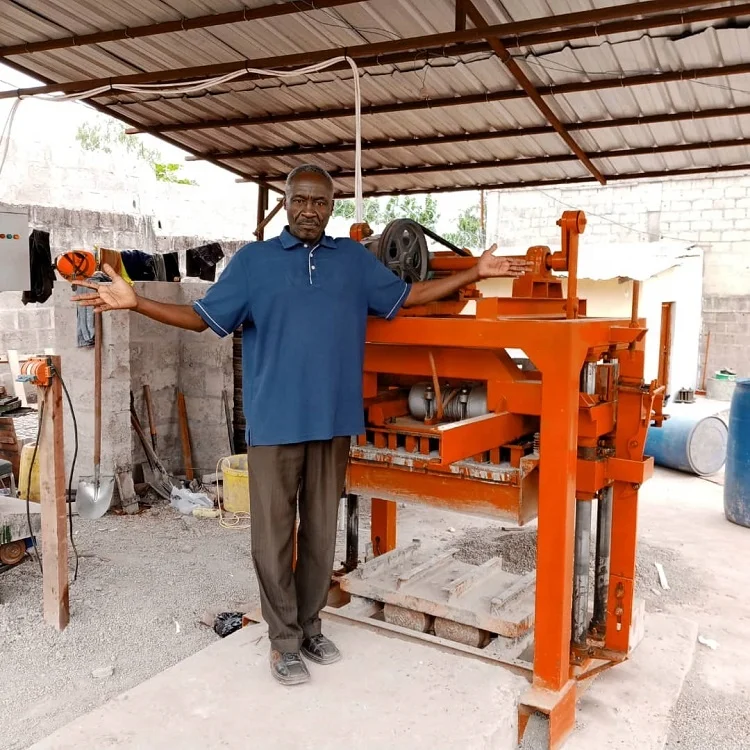
| Assembly State | Stationary, requires precast concrete ground installation |
| Warranty | 1 year (excluding spare parts) |
| Output Capacity | Cycle time 24–26 s per mould format (daily throughput basis to be confirmed against buyer’s block format, mix design and shift length) |
Application Suitability
| Application | Material or Output |
|---|---|
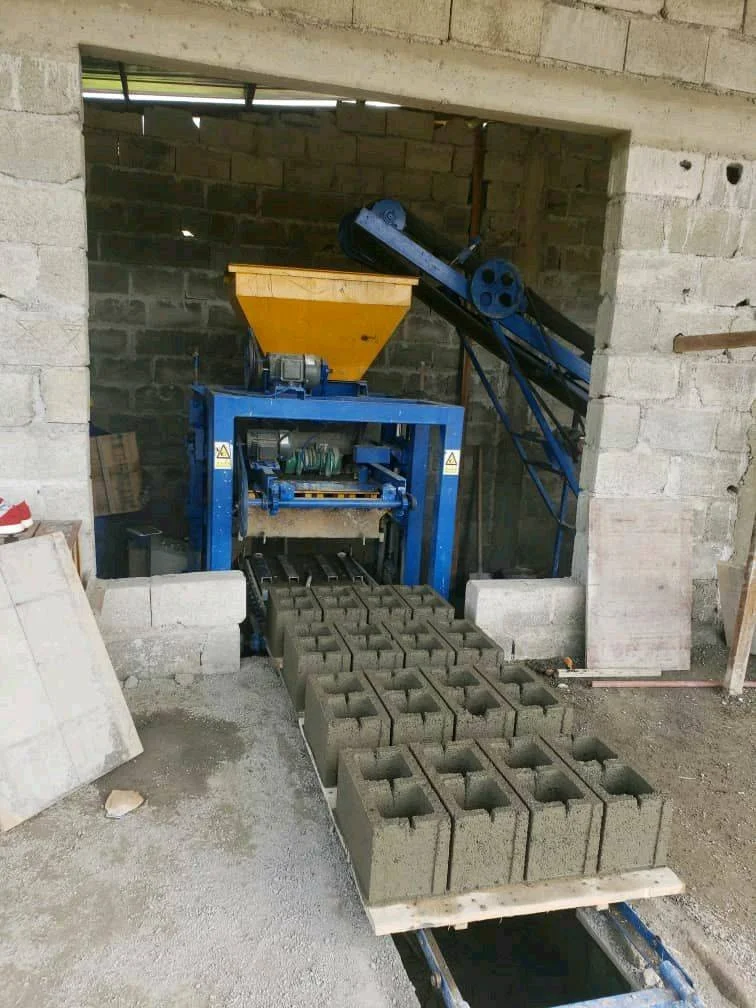
| Hollow block production | Cement, crushed stone, sand, water — standard lightweight and dense aggregate mixes |
| Solid block production | Cement with local river sand or quarry dust |
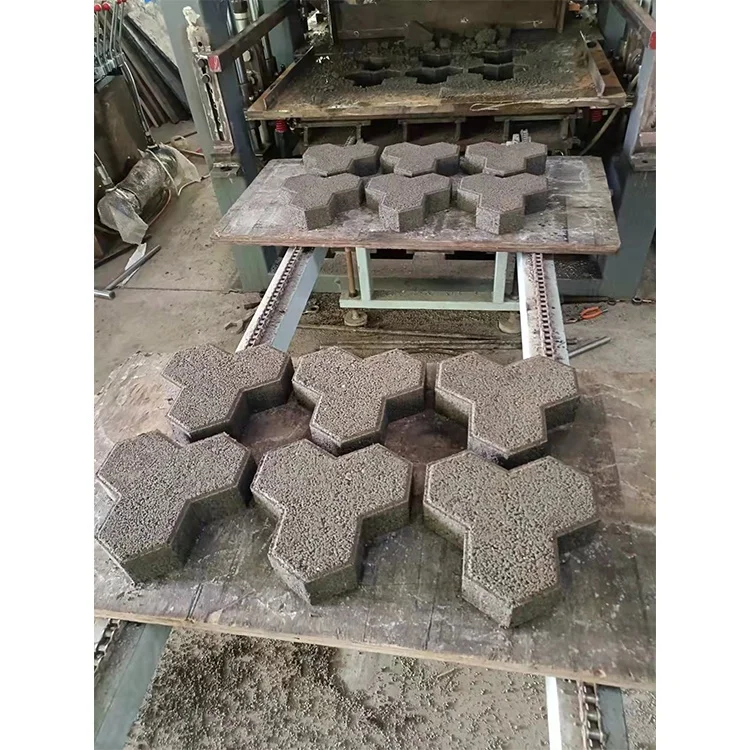
| Paving block production | Cement, fine aggregate, pigment for colored surface layers |
| Standard brick production | Cement, sand, fly ash or stone dust blends |
| Multi-cellular brick production | Lightweight aggregate or foamed concrete mixes within mould compatibility |
| Small-scale block plants | Start-up facilities producing for local construction projects |
| On-site contractor production | Housing or infrastructure contractors making blocks directly at the build location |
Why the Voltage Question Must Precede the Mould Order
Confirming voltage, frequency, and control language before the machine leaves the factory prevents a machine that sits idle on arrival.
Too many first-time block plant buyers focus on mould count and cycle time, then discover after container discharge that the local grid runs at a frequency the motor was never wound for, or that the operator cannot read the display. When an automatic block machine upgrade is the long-term plan, the electrical foundation has to be right from day one; rewiring a control cabinet in the field costs more and takes longer than specifying it correctly at order [NEED_CITE: voltage and frequency standards by export market]. I once watched a crew in a West African yard spend a full week tracing control faults that turned out to be a 50 Hz motor running on 60 Hz supply.
Control Logic That Protects the Operator and the Press
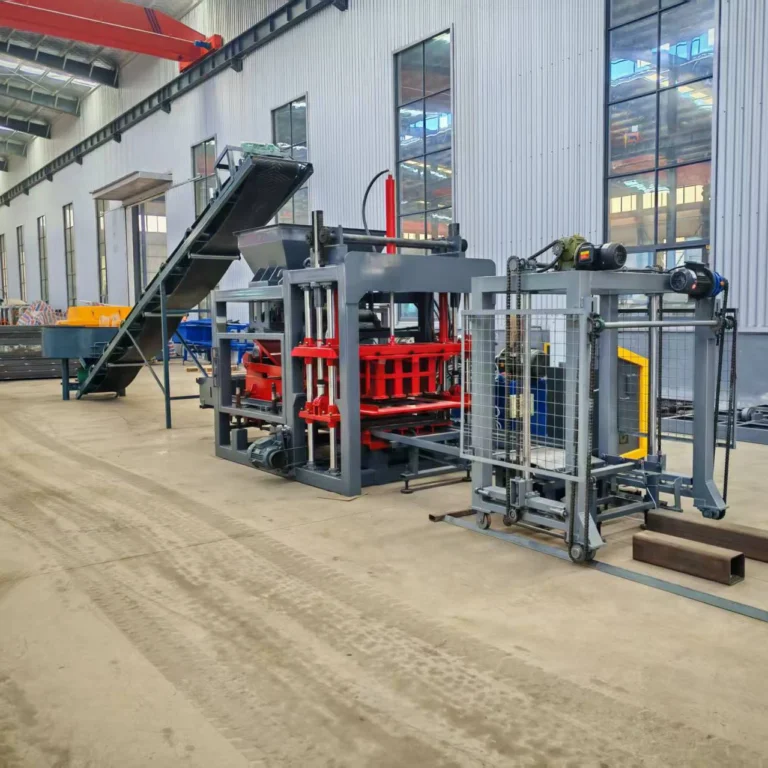
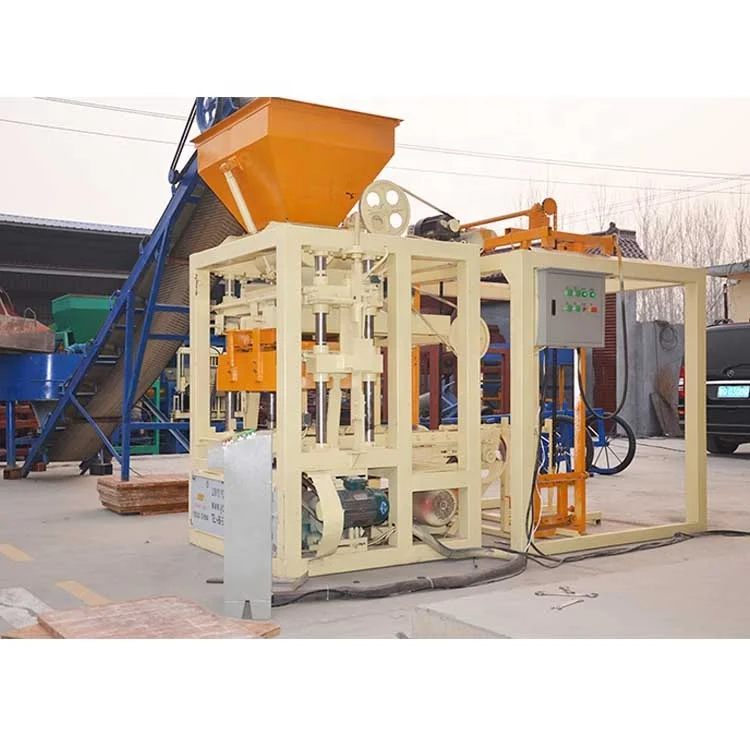
The QTJ4-24 places an electrical control cabinet at the heart of what is otherwise a mechanically driven press. The interworking circuit monitors sequence positions — mould closed before vibration starts, upper head retracted before pallet ejects — so an incorrect manual input is blocked rather than executed. This matters most during shift changes and operator handovers when attention drifts. For a plant owner evaluating a PLC controlled semi-automatic block machine as the entry point to higher automation, this cabinet is the interface that will later accept sensor upgrades and pallet-feed signals.
Vibration Consistency as the Foundation of Block Strength
Table vibration feeds the mix into the mould cavity, then fluctuation vibration compacts it under the upper head. The two stages must be timed precisely within the 24–26 s cycle; when they drift apart, the bottom of the block is dense but the face shells remain loose. Because the electrical cabinet governs this timing rather than leaving it to operator feel, batch-to-batch compactness stays repeatable across a ten-hour shift. That repeatability is what separates a credible block producer from one whose product fails the local compressive strength test at the building inspector’s yard [NEED_CITE: CE machinery directive requirements for industrial equipment].
Reading the Specs That Actually Shape Daily Output
The 900 mm × 450 mm pallet size determines the mould footprint and, indirectly, the curing rack dimensions the buyer must build or buy. The 11.95 kW rated power covers vibration motors, feed mechanism and control — but does not include the mixer or conveyor, so the plant’s total electrical draw needs separate calculation before selecting the main breaker. The four listed mould formats each place a different number of blocks per cycle: four hollow blocks versus twenty-one standard bricks means daily throughput swings widely depending on which format dominates the order book, so the capacity discussion must name the target block before any number is meaningful. The stationary assembly requirement means the machine bolts to a precast concrete slab; a poured-in-place floor with level tolerances keeps the vibration table from walking during long runs. Mould change time is not published in the source data, so a buyer planning frequent format switches should request a timed change demonstration before shipment.
The Hidden Cost of Skipping the Automation Conversation
When a buyer orders a press without specifying which stations remain manual, pallets move by hand from the press to the curing yard and stacked output is carried one block at a time. The press itself may run its cycle consistently, but the bottleneck simply shifts downstream, and the operator count stays higher than the brochure implied. A plant that plans to scale within twelve to eighteen months needs to know now whether the control cabinet has spare relay positions and pre-wired terminals for an automatic pallet feeder, so the later automatic block machine upgrade is a bolt-on rather than a rebuild [NEED_CITE: electrical interface standards for block line automation].
Why Source the QTJ4-24 From This Line
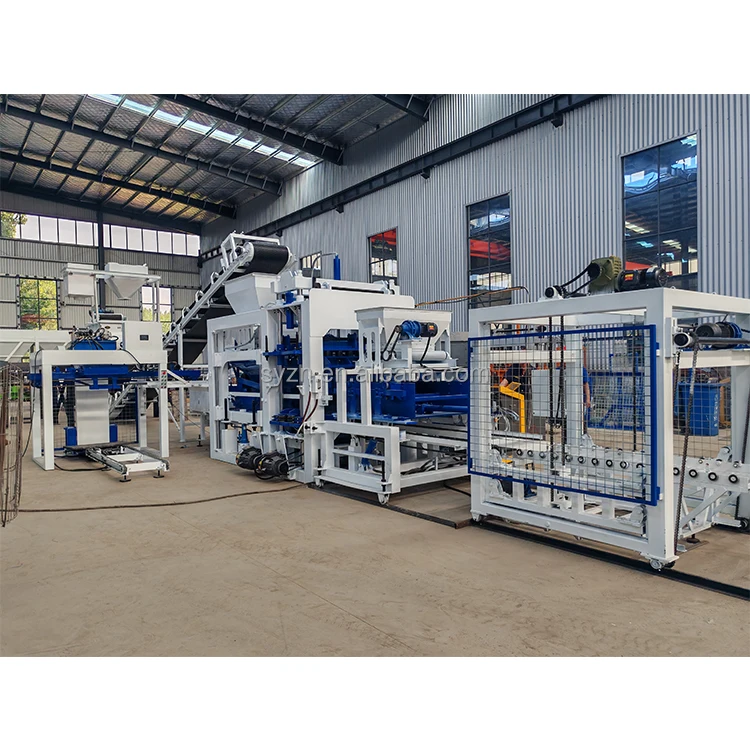
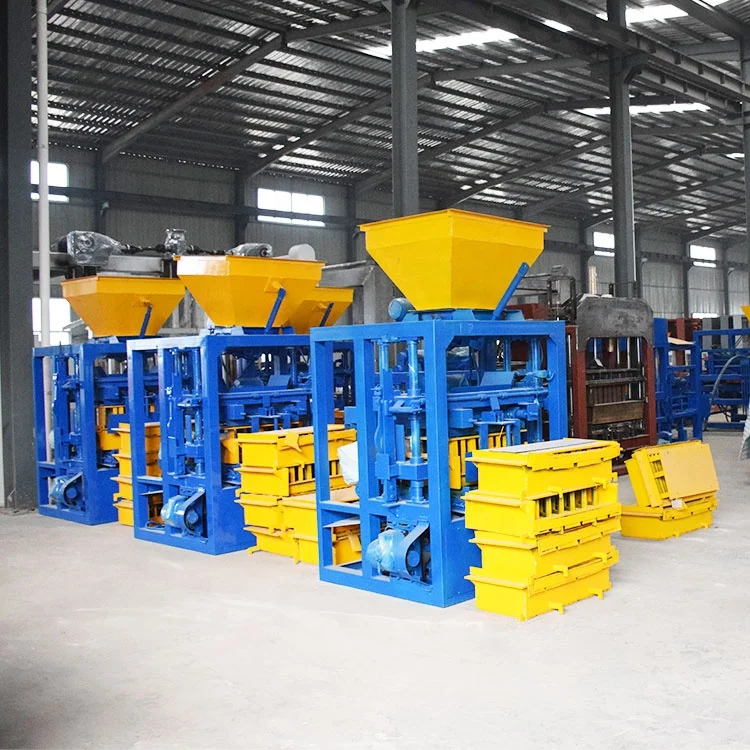
The machine, mould, pallet and handling equipment are specified as one matched system, not assembled from unrelated suppliers, so the 900 mm × 450 mm pallet actually fits the curing racks quoted in the same proposal. Configuration is set against the buyer’s local aggregate and target block format rather than a catalogue default, which is why I insist on running a sample of the buyer’s sand and cement mix before the press leaves Shandong. Mould design covers the formats the buyer’s market actually sells, including custom drawings when the local standard dimension differs from the four listed options. Automation level is selectable from this semi-automatic starting point upward, so a buyer can add pallet feeding and stacking stations later without replacing the core press. Installation support includes operator training at the buyer’s site, and the electrical cabinet language is confirmed before dispatch so the first shift runs without a translator standing by.
Documentation & Verification
- Machine specification sheet stating the QTJ4-24 automation level and which stations remain manual
- Mould drawing and format list matching the four cavity options to buyer’s block dimensions
- Factory test record on buyer’s supplied aggregate mix demonstrating cycle consistency
- Electrical schematic confirming voltage, frequency, and control display language per destination
- Line layout showing pallet size against curing area dimensions and forklift turning radius
Installation, Commissioning & Support
- Precast concrete ground slab required to anchor the 3.5 T press and absorb vibration transmission
- Dedicated electrical circuit sized for the 11.95 kW press plus mixer and conveyor draw
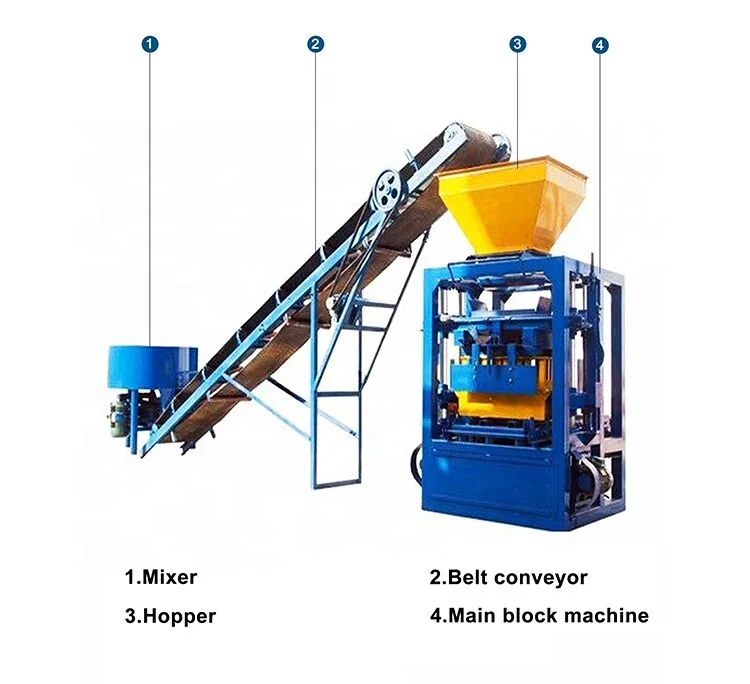
- Machine ships stationary; on-site assembly covers conveyor alignment and mixer feed height
- First-run parameter tuning of vibration timing and cycle duration against local mix design
- Operator training on electrical cabinet interlocks and safe mould change sequence
- Wear parts list covering vibration table springs, mould liners, and electrical contactors
What to Prepare Before Requesting a Quotation
Share the exact block format and dimension your market requires, the local aggregate type and cement grade available, and the daily output target stated per that specific block. Confirm your site’s voltage, frequency, and the operator language for the control display. If you already run a mixer or belt conveyor, send their model and capacity so the line can be balanced around them.
Frequently Asked Questions
Q: What does semi-automatic actually include on the QTJ4-24?
A: The electrical control cabinet automates the vibration sequence and upper-head timing within the 24–26 s cycle. Pallet feeding onto the press, pallet transfer to the curing area, and stacking of finished blocks remain manual operations at this configuration level.
Q: Can I add automatic pallet feeding and stacking later?
A: Yes, provided the control cabinet is ordered with spare relay capacity and pre-wired interface terminals. Confirming this at the quotation stage avoids rewiring the cabinet during the automatic block machine upgrade.
Q: How is the control system set up for my country’s power grid?
A: Voltage, frequency, and phase are confirmed per destination before production. The operator display language is also specified at order so the electrical cabinet arrives ready for your local team.
Q: How do I ensure consistent block strength with my local aggregate?
A: Send a sample of your sand, crushed stone, and cement to the factory before shipment. The vibration force and cycle timing are then tuned to that specific mix during the factory test, not left at a catalogue default.
Q: What automation level should I choose if I plan to scale output within a year?
A: Starting with the QTJ4-24 semi-automatic configuration and specifying pre-wired upgrade interfaces gives you immediate production while keeping the path open to add pallet feeding and stacking stations without replacing the press.