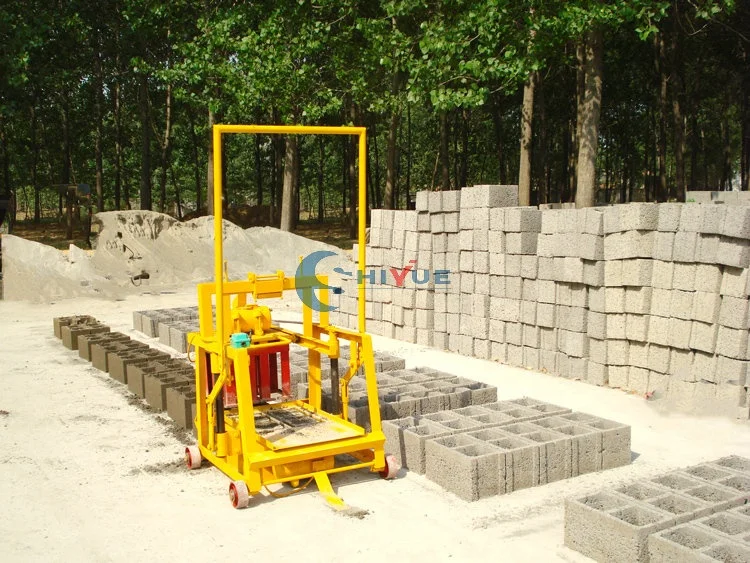
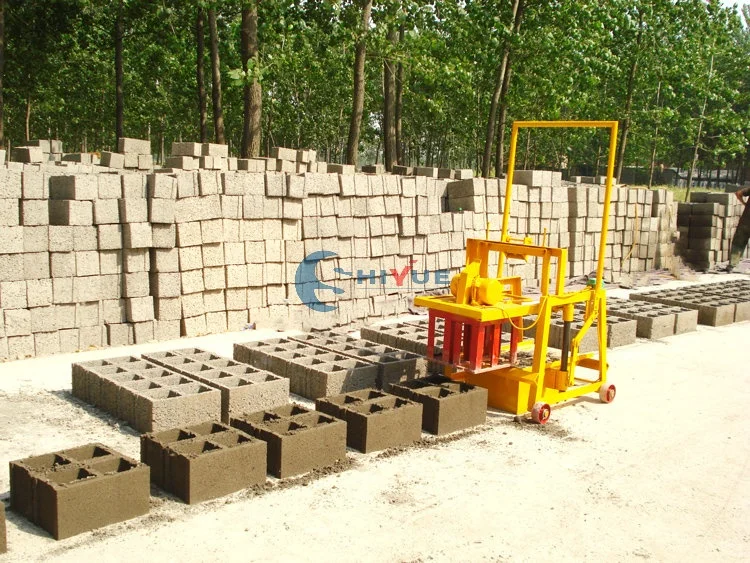
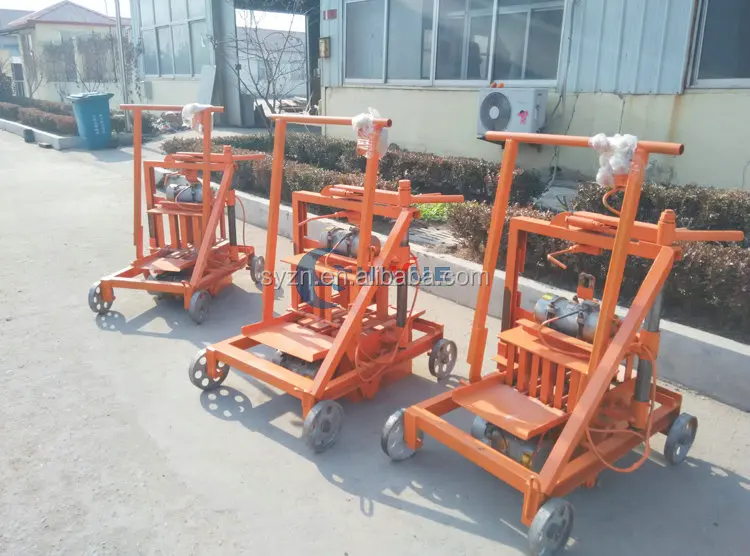
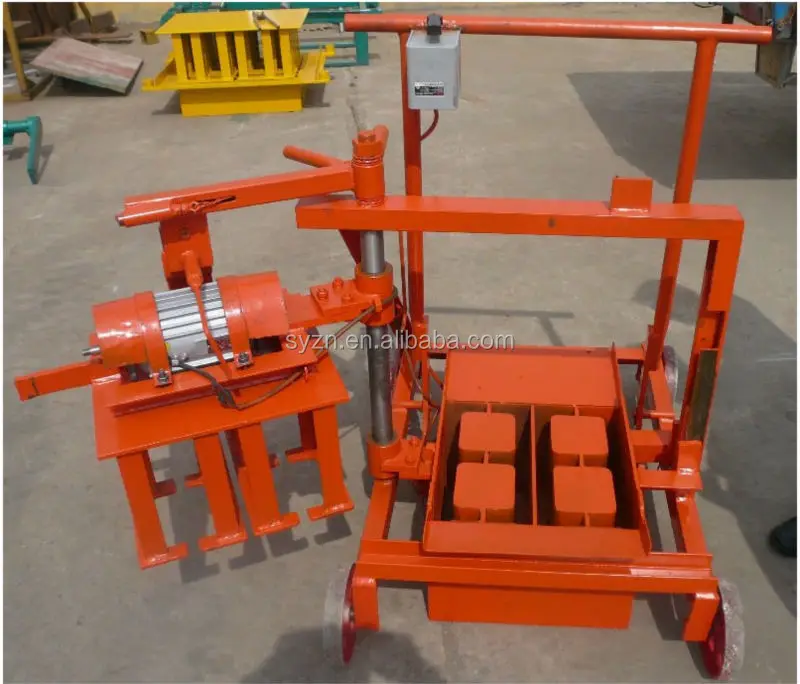
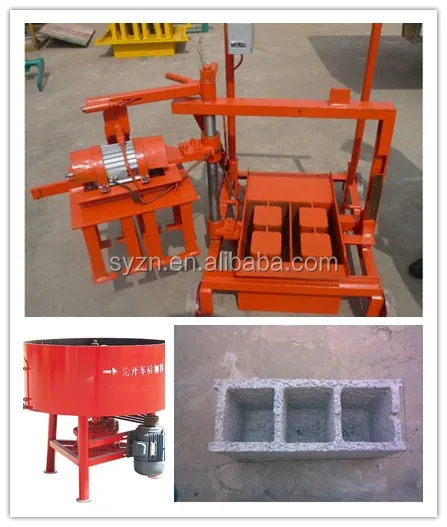
Description
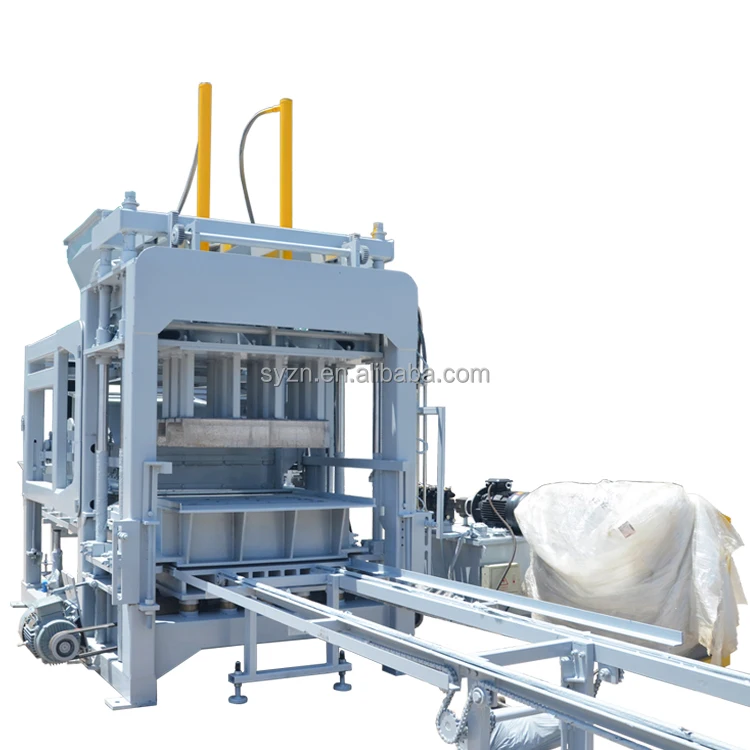
Matched Vibration Control — dual-motor vibration tuned to your local aggregate, not a catalogue default, so the QMJ2-45 produces uniform block density from the first cycle.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QMJ2-45 |
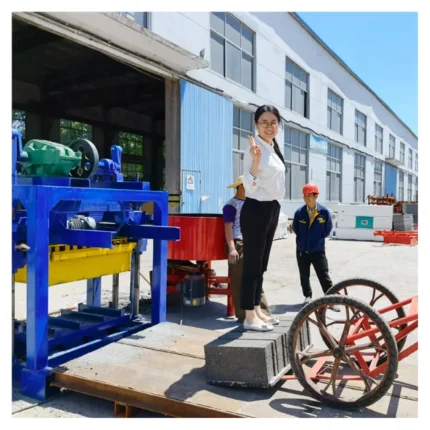
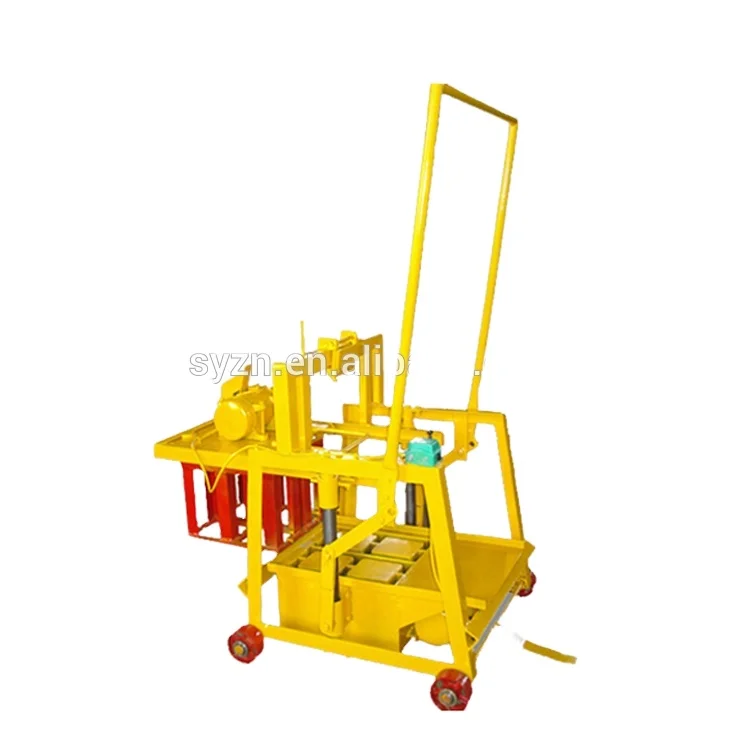
| Product Type | Mobile Egg-Laying Block Making Machine |
| Automation Level | Semi-automatic (manual pallet handling) |
| Rated Power | 1.5 kW |
| Molding Cycle | 45 s (basis not stated in source) |
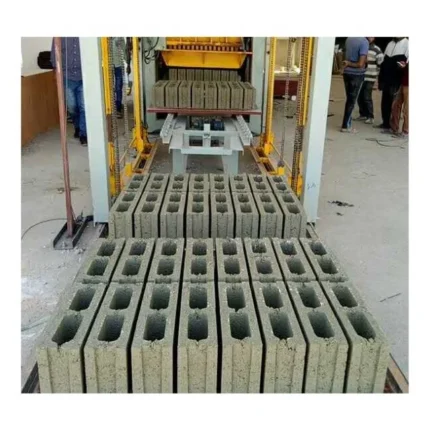
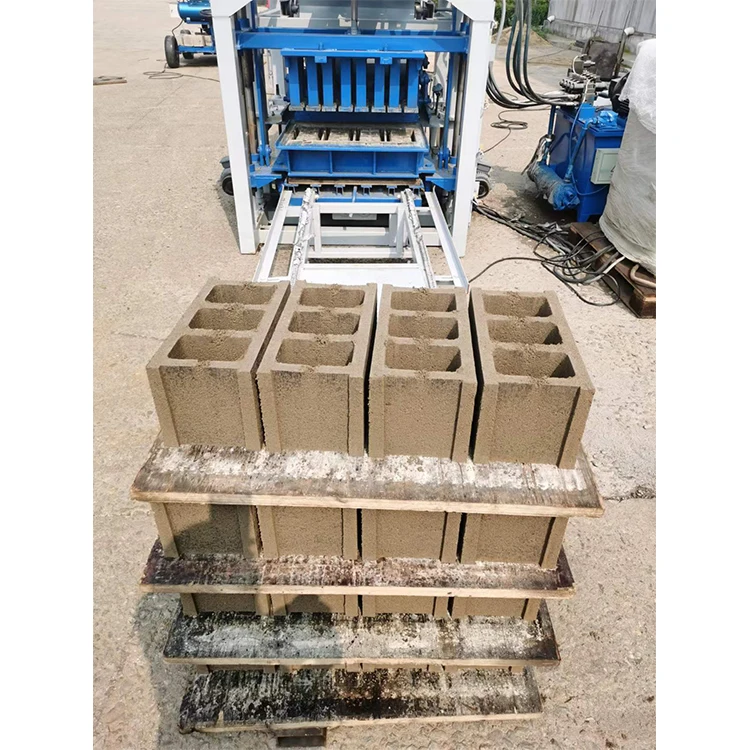
| Theoretical Output — 400×200×200 mm hollow block | 150 pcs/h, 1200 pcs/day (based on 2 pcs/mould) |
| Theoretical Output — 400×150×200 mm hollow block | 220 pcs/h, 1760 pcs/day (based on 3 pcs/mould) |
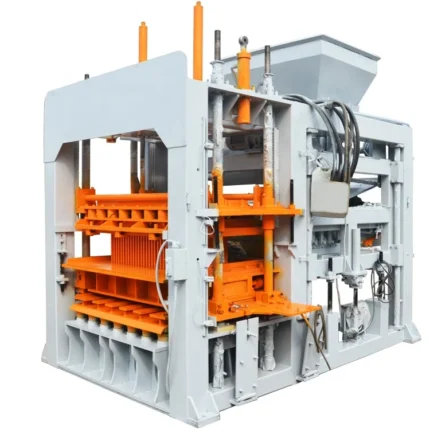
| Vibration System | Bed mould vertical vibration + upper mould compression vibration; 2 vibrating motors per mould |
| Mould Actuation | Top die push-pull with automatic scraper |
| Raw Materials | Concrete, sand, cement, fly ash, lime, gypsum |
| Machine Weight | 400 kg |
| Overall Dimensions (L×W×H) | 1300 × 1300 × 1150 mm |
| Voltage | Configurable to buyer’s local supply (verify exact rating and frequency) |
| Control System | Available with relay-based or PLC control options (basis to be confirmed) |
| Certification | CE declaration where applicable |
Application Suitability
| Application | Material or Output |
|---|---|
| Small-scale block workshops | Hollow blocks from sand, cement and locally available fine aggregate |
| On-site production by housing contractors | Concrete hollow blocks laid directly on a prepared ground surface |
| First-time plant startups | Fly ash or gypsum-based mixes at low investment entry point |
| Rural building material supply | Porous and solid block formats using crusher dust and lime |
Why the Control Language Question Beats the Price Question
Confirming the PLC display language and voltage before production prevents commissioning from stalling the moment the crate is opened.
When a mobile egg-laying machine arrives with an English-only interface in a region where operators read French or Swahili, the first two days on site are spent deciphering menus instead of producing blocks. I have watched this happen more than once, and the automatic QMJ2-45 block machine is no exception — the fix costs time, not money, but only if it is caught before the machine leaves the factory floor. Voltage mismatches create a similar bottleneck: a 380 V/50 Hz machine plugged into a 220 V/60 Hz supply simply will not start, and rewinding the motor on site is nobody’s idea of a smooth commissioning [NEED_CITE: common export machinery commissioning delays].
How the PLC Controlled Mobile Block Machine Removes Operator Variance
On a semi-automatic machine, the operator controls the feed, the cycle start and the mould release. Every hesitation or early button press changes how the concrete settles. The PLC controlled mobile block machine addresses this by locking the vibration duration and top-die compression into a repeatable sequence, so cycle-to-cycle variation narrows even when the person at the controls changes shifts.
The Upgrade Path From Semi-Automatic to Hands-Off Pallet Handling
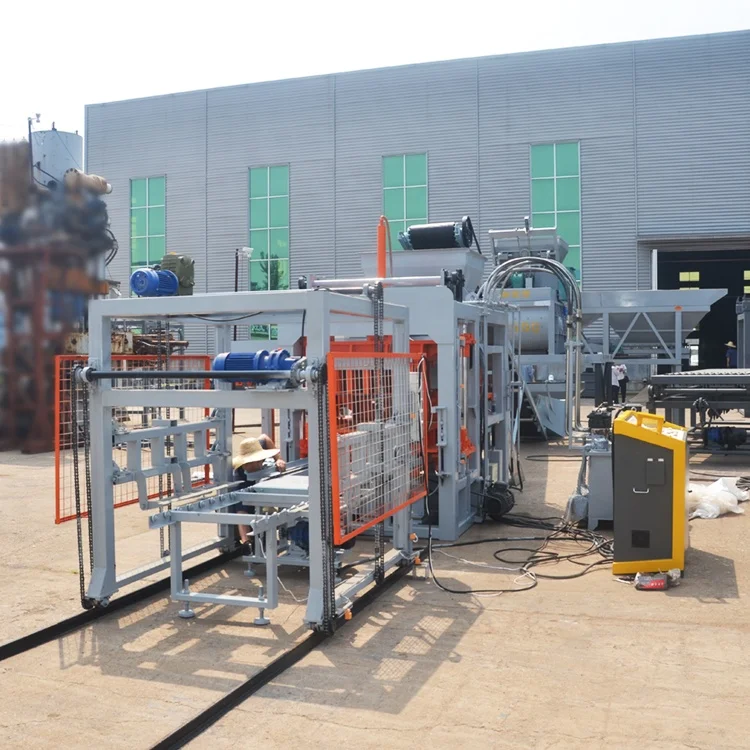
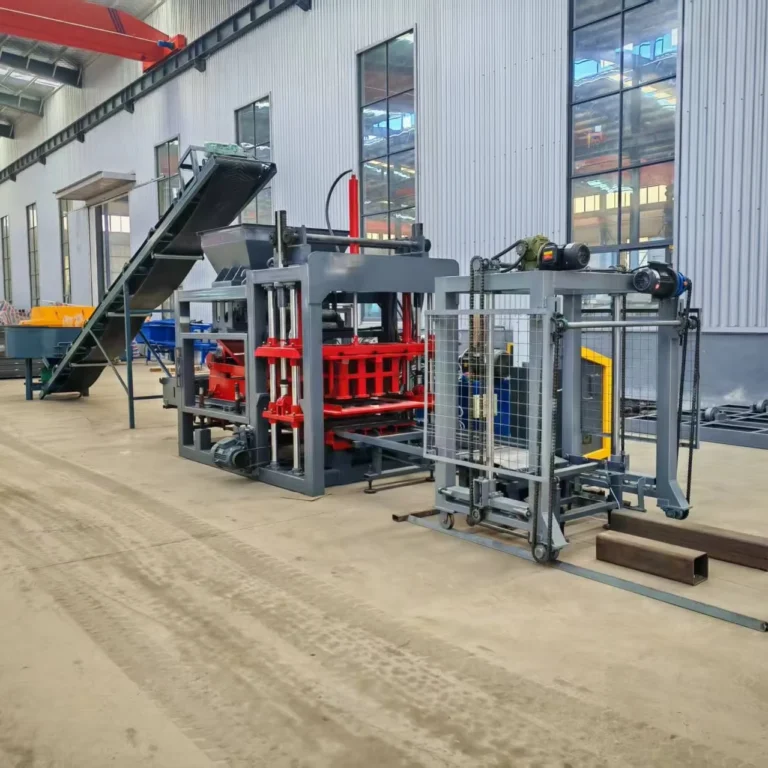
Starting with the QMJ2-45 as a manual pallet unit keeps capital outlay low. When daily volume grows, the same machine frame can accept an automatic pallet feeder and a stacking station, converting the line without replacing the press. This staged approach means the initial purchase does not become obsolete the moment output targets rise [NEED_CITE: automation upgrade paths for small block plants].
Reading the Spec Sheet Beyond Cycles Per Hour
The 45-second molding cycle is a baseline figure. In practice, that number shifts depending on mix workability and the block format being run. The dual vibration system — bed mould vertical vibration paired with upper mould compression vibration — works to compact the mix uniformly across the mould cavity. Higher vibration force is needed when the aggregate is coarse or the cement content is low; the two vibrating motors per mould deliver that force symmetrically, reducing density differences between the left and right sides of the block. The top die push-pull mechanism with its automatic scraper ensures each mould fill is level before compression begins, which is where most of the dimensional consistency is won or lost.
What Happens When Vibration Settings Ignore Your Local Mix
Set the vibration too high for a fine-sand mix and the block surface cracks before it leaves the mould; set it too low for a coarse-aggregate mix and the core stays loose, failing a drop test. These are not rare events — they show up on the first production day and halt output until someone adjusts the motor eccentric weights. On a mobile egg-laying machine, that adjustment is mechanical and accessible, but only if the buyer knows the setting exists and has been told what range to target [NEED_CITE: vibration tuning for concrete block density].
Why Configuration Transparency Matters Here
Block machinery is the single focus of this production line, which means the QMJ2-45 is specified alongside its mould, vibration motors and control panel as one matched set rather than assembled from separate suppliers. Configuration starts with the buyer’s actual mix design and target block format, not a catalogue default. Mould design covers the formats the local market sells, and custom drawings are accepted when standard options do not fit. Voltage, frequency and PLC display language are confirmed in writing before the machine enters production, so the unit that arrives is the unit that was ordered. Automation level is selectable, letting a buyer start semi-automatic and add pallet feeding or stacking later. Installation and commissioning support includes operator training on vibration adjustment and mould change procedure.
Documentation & Verification
- Line layout stating block format assumed in capacity calculation
- Machine specification sheet with confirmed voltage and frequency
- Mould drawing and format list matching ordered block types
- Factory test record showing actual cycle time and block density
- Operation and maintenance manual in confirmed display language
- Wear parts and mould list with part numbers for first reorder
Installation, Commissioning & Support
- Ground surface must be level concrete to support 400 kg machine weight during egg-laying operation
- Dedicated 1.5 kW circuit at confirmed voltage and frequency, isolated from welding equipment
- Machine ships assembled; vibration motor eccentric weights adjustable on site to match local aggregate
- PLC display language set and locked during factory test before crating
- Mould change training covers top die push-pull release and scraper alignment
- Spare vibrating motor and scraper blade included in first-shipment wear parts kit
- Daily greasing points marked on bed mould guide rails for vibration system longevity
Preparing Your Inquiry
Send the block format you sell most — dimensions and whether hollow or solid — along with your target daily output for that specific format. Include your local voltage and frequency, the language your operators read, and the aggregate you plan to use so the vibration settings can be matched before the machine ships.
Frequently Asked Questions
Q: How is output capacity calculated for the QMJ2-45, and which block format does each figure assume?
A: Capacity is stated per block format, not as a single headline number. For a 400×200×200 mm hollow block at 2 pieces per mould, the theoretical rate is 150 pieces per hour. For a 400×150×200 mm hollow block at 3 pieces per mould, the rate is 220 pieces per hour. Both assume a 45-second molding cycle and continuous operation.
Q: What control system does this machine use, and can the PLC display be set to my operator’s language?
A: The QMJ2-45 is available with relay-based or PLC control depending on configuration. When PLC is selected, the HMI display language is confirmed in writing before production and locked during the factory test. This prevents commissioning delays caused by operators unable to read menu prompts on arrival.
Q: What automation upgrades are available from this semi-automatic base?
A: The machine frame accepts an automatic pallet feeder and a stacking station as volume grows. These additions convert manual pallet handling into powered feed and removal without replacing the press. Batching automation can also be added upstream to improve mix consistency across shifts.
Q: How should vibration settings be adjusted to match my local aggregate and mix design?
A: The two vibrating motors per mould have adjustable eccentric weights. Coarse aggregate with low cement content typically requires higher vibration force, while fine sand mixes need less to avoid surface cracking. The adjustment is mechanical and accessible on site, and target settings are included in the commissioning documentation.
Q: What voltage and frequency options are available, and how is this confirmed before shipment?
A: Voltage and frequency are configured to the buyer’s local supply. The exact rating is confirmed in writing during the inquiry stage and verified during the factory test. This written confirmation is included in the shipment documentation so the receiving team can match the machine to the correct electrical circuit on arrival.