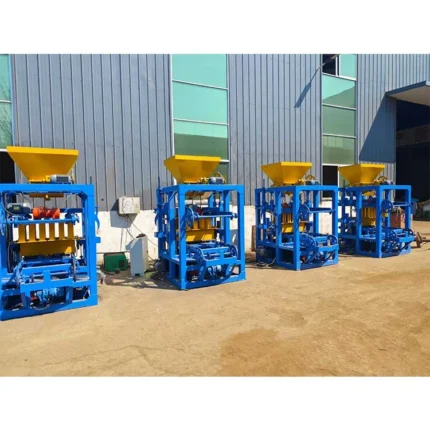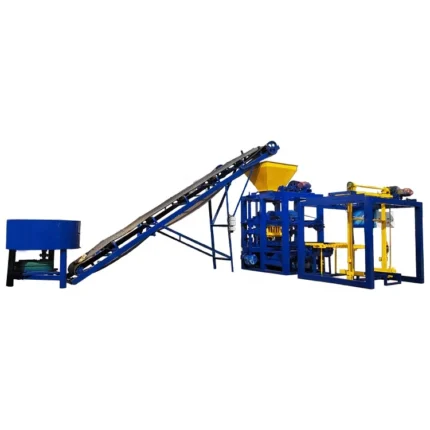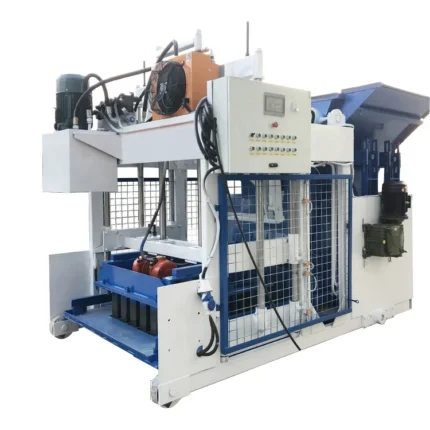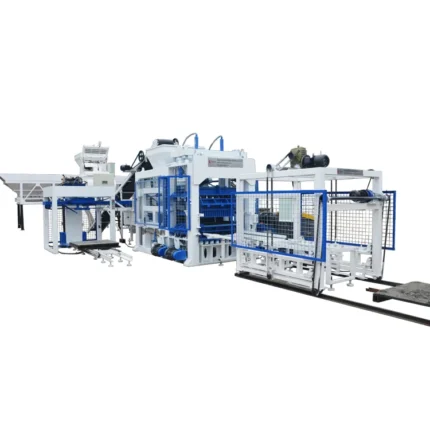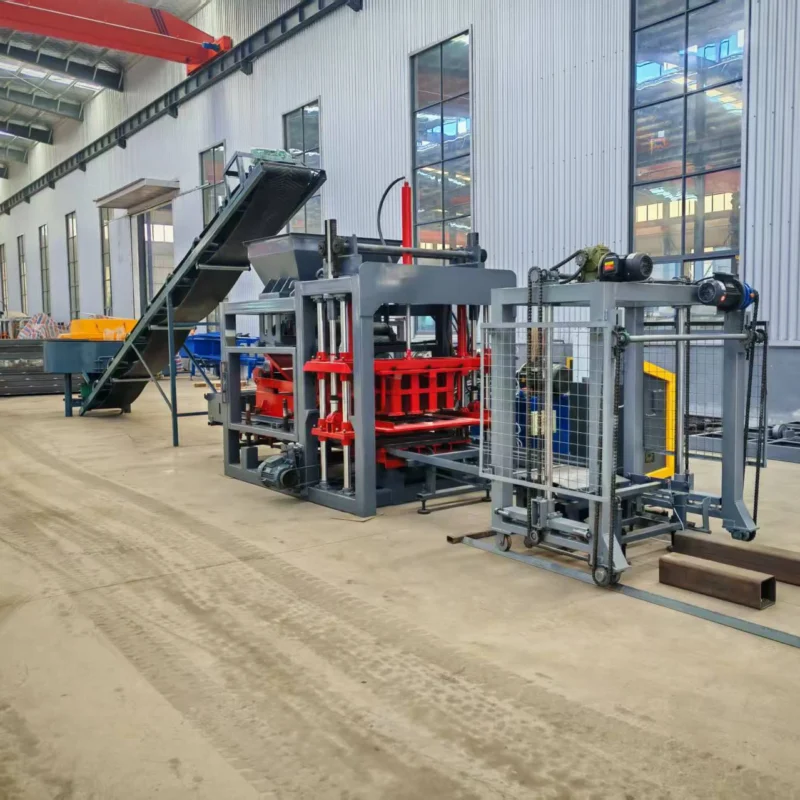

Description
Matched Control Logic — the QT4-15A’s PLC parameters are calibrated against your actual block format and local aggregate before the control language is locked in, eliminating the on-site guesswork that burns commissioning days.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-15A |
| Product Type | Fully Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 4100×1600×2600 mm |
| Rated Pressure | 16–21 MPa |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency | 4200 r/min |
| Vibration Force | 55 kN |
| Pallet Size | 880×550 mm |
| Molding Cycle | 25–30 s (basis not stated in source — confirm block format / material / thickness) |
| Overall Power | 18.45 kW |
| Total Mass | 4 T |
| Demolding Method | Hydraulic |
| Control System | PLC with configurable HMI language |
| Automation Level | Fully Automatic |
| Key Features | Platform vibration, hydraulic demolding, multi-format mould compatibility |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for load-bearing walls | Crushed stone, sand, cement, fly ash |
| Solid block manufacturing for foundations | Gravel, cement, slag blends |
| Interlocking paver production for driveways and walkways | Colored concrete mixes with fine aggregate |
| Curbstone forming for municipal infrastructure | High-density concrete with coarse aggregate |
| Porous permeable brick for sponge-city projects | Open-graded aggregate with controlled cement content |
What "25-30 Seconds per Cycle" Actually Means for Your Daily Output
Cycle time is meaningless without the block format it was measured on.
I have watched plant owners quote a cycle figure from a supplier brochure and then discover on commissioning day that their 200 mm hollow block needs a longer vibration window than the thin paver the factory tested with. The automatic QT4-15A block making machine PLC controlled setup addresses this because the PLC program stores separate recipes — vibration duration, pressure hold, feed cycles — for each mould you install. [NEED_CITE: PLC recipe management standards in concrete product machinery] When your operator switches from hollow blocks to interlocking pavers, the control recalls the matched parameters rather than leaving timing to manual adjustment. This removes the batch-to-batch density variation that causes breakage during pallet transport or fails a compressive strength test weeks later.
How PLC Recipe Storage Removes Operator Guesswork
On a manual or relay-controlled press, the operator sets vibration time by watching a clock and adjusts feed volume by eye. Every shift change introduces drift. The automatic QT4-15A block making machine PLC controlled system stores the exact feed weight, vibration duration, and hydraulic hold pressure for each block format, so the first block of a Monday morning shift matches the last block from Friday afternoon.
Batch Consistency Across Format Changeovers
When a plant runs hollow blocks in the morning and pavers after lunch, the transition is where quality typically drops. The PLC recalls the paver recipe the moment the new mould is clamped, adjusting vibration force and demolding speed to match the thinner, denser product. [NEED_CITE: impact of vibration force variation on concrete paver compressive strength] The operator’s job shifts from timing and guessing to loading the correct pallet stack and monitoring raw material levels.
Reading the Pressure and Vibration Numbers Together
Rated pressure of 16–21 MPa sets the compaction ceiling, while platform vibration at 55 kN and 4200 r/min determines how thoroughly the mix settles into the mould cavity before pressure locks it. A high-pressure press with weak vibration leaves air pockets inside a hollow block wall. Strong vibration with low pressure produces a block that crumbles at the corners during demolding. The QT4-15A pairs both within a range that covers standard hollow blocks up to dense interlocking pavers, provided the mix design is confirmed beforehand. Pallet size at 880×550 mm defines the maximum mould footprint and must match the curing rack spacing and forklift tine width already in your yard — a mismatch here means new racks or manual re-stacking before blocks enter the curing zone.
The Hidden Cost of Unmatched Automation Scope
A quotation that lists "fully automatic" may cover only the press itself, leaving pallet feeding, stacking, and cubing as manual tasks or separate line items. I have seen buyers discover at installation that blocks were being stacked by hand while the press cycled automatically — the automation they paid for stopped at the press table. [NEED_CITE: typical scope boundaries in block plant automation quotations] Always confirm whether automatic pallet feeding, stacking, and cubing are included in the written proposal or listed as optional stations.
Why Procurement Decisions Land Here
Block machinery is the single product focus, so the QT4-15A is specified as part of a matched system — press, mould, pallet, and handling — rather than assembled from unrelated suppliers. The configuration is set against the buyer’s actual mix design and target block format, not pulled from a catalogue default. Mould design covers the formats the buyer’s market sells, with custom drawings accepted for non-standard shapes. Automation level is selectable, allowing a plant to begin with semi-automatic pallet handling and add stacking or cubing stations later. Installation includes on-site commissioning with operator training that covers PLC recipe entry and mould changeover procedure.
Documentation & Verification
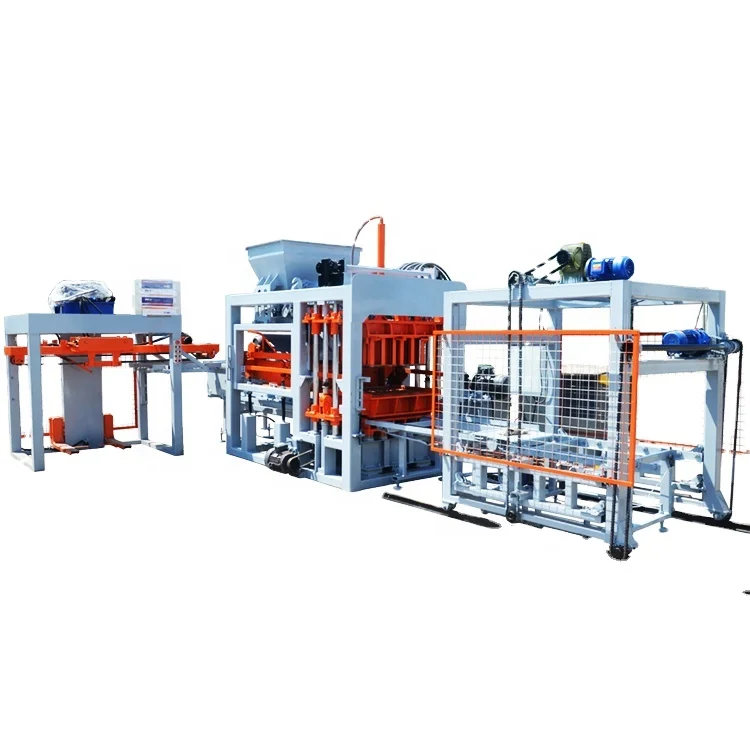
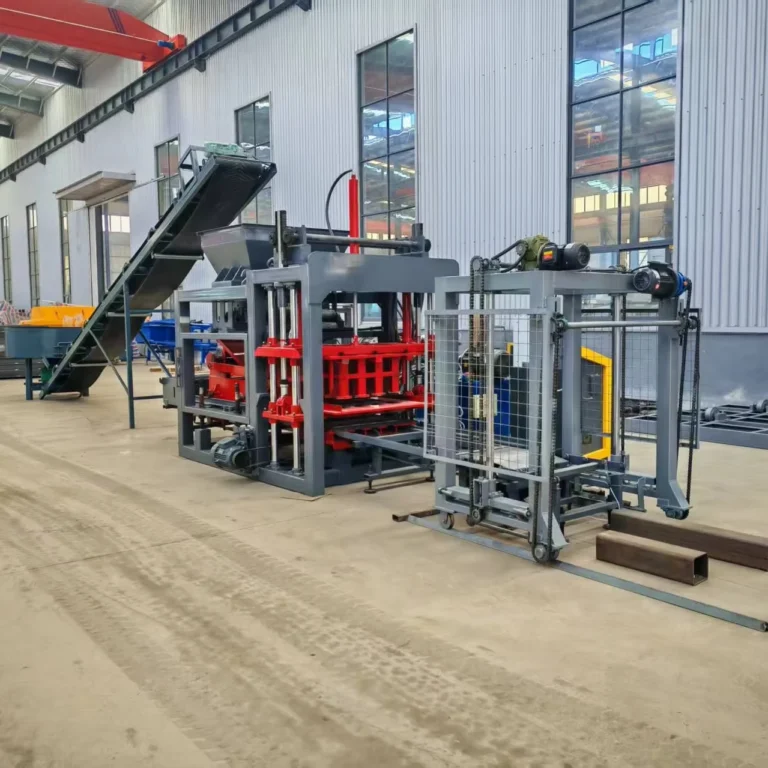
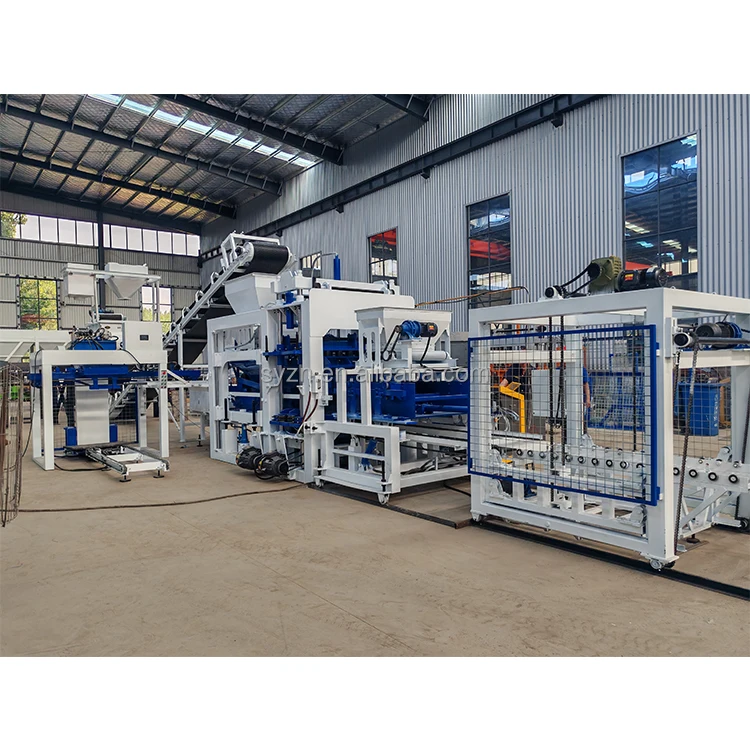
- Line layout showing press, pallet feed, and stacking station positions with cycle timing per block format
- Machine specification sheet with confirmed voltage, frequency, and HMI display language
- Mould drawing and format list with pallet compatibility noted for each cavity
- Factory test record demonstrating cycle time and block output on your specified format
- Hydraulic and electrical schematic for local maintenance team reference
- Operation and maintenance manual in the operator’s confirmed language
Installation, Commissioning & Support
- Foundation pad leveled to 4100×1600 mm footprint with anchor bolt template provided before machine arrival
- Dedicated 18.45 kW circuit with voltage and frequency confirmed in writing prior to production start
- PLC display language locked to operator’s language before dispatch, verified on power-up at site
- Hydraulic system pressure set to 16–21 MPa range and tested against your actual mix during commissioning
- Platform vibration frequency checked at 4200 r/min with accelerometer during first production run
- Mould changeover procedure trained on-site with your team using the specific formats ordered
What to Include in Your Inquiry
Send the specific block formats your market sells — dimensions, wall thickness, and target compressive strength. Provide your local aggregate type and a recent sieve analysis if available. Confirm the voltage and frequency at your site, the PLC display language your operators read, and whether existing curing racks and forklifts constrain pallet size. If you already run upstream mixing or downstream stacking equipment, note the interface points so the line can be matched end to end.
Frequently Asked Questions
Q: How does the 25–30 s molding cycle translate into daily output for different block formats?
A: The 25–30 s figure was recorded without a stated block format, so realistic daily output depends on the specific mould installed — a thin paver cycles faster than a 200 mm hollow block. During proposal stage we calculate capacity per format you intend to produce, so the figure you plan against matches what the press actually delivers on your products.
Q: Which PLC brands are available and can the HMI be set to my operator’s language?
A: PLC brand and HMI language are confirmed during the quotation stage based on availability and your preference. The critical step is locking the display language before the machine leaves the factory — I have seen commissioning delayed because the touchscreen defaulted to a language the site team could not read.
Q: How do you match vibration force and hydraulic pressure to my local aggregate before shipment?
A: We request a sample or sieve analysis of your aggregate and the cement ratio you plan to use. Vibration duration and pressure hold are then adjusted in the PLC recipe so that the 55 kN platform vibration and 16–21 MPa hydraulic pressure produce the target density without corner damage on demolding.
Q: Can I add automatic stacking or cubing stations to a semi-automatic QT4-15A later?
A: The automation level is selectable, and stations such as automatic pallet feeding, stacking, and cubing can be added as the plant scales. The PLC architecture allows additional I/O modules and program routines to be loaded without replacing the main controller.
Q: Does the quotation cover automatic pallet feeding and stacking, or only the press?
A: Automation scope varies by quotation. We specify in writing exactly which stations — press, pallet feeder, stacker, cuber — are included and which are optional, so there is no gap between what you expect and what arrives on site.