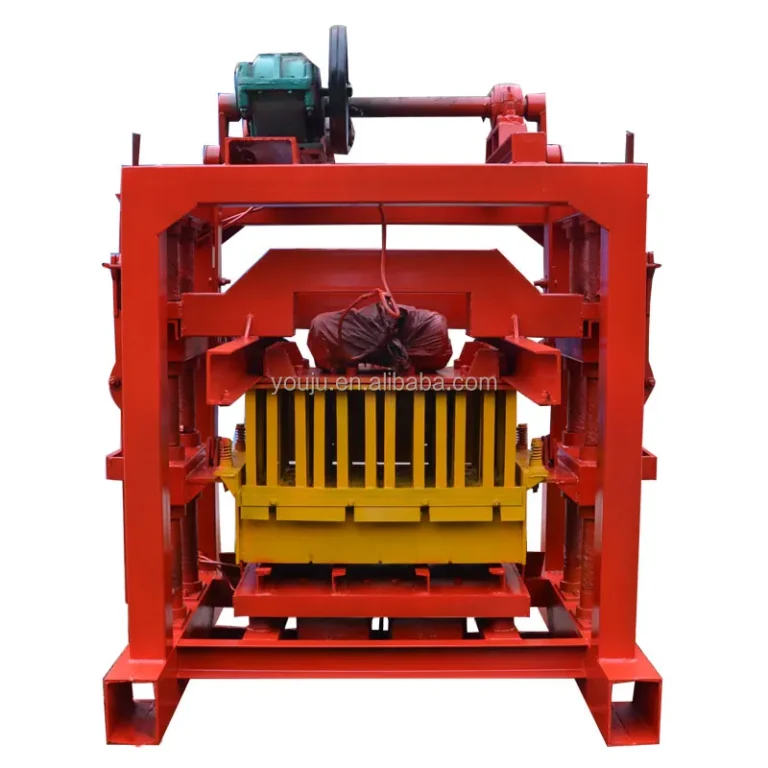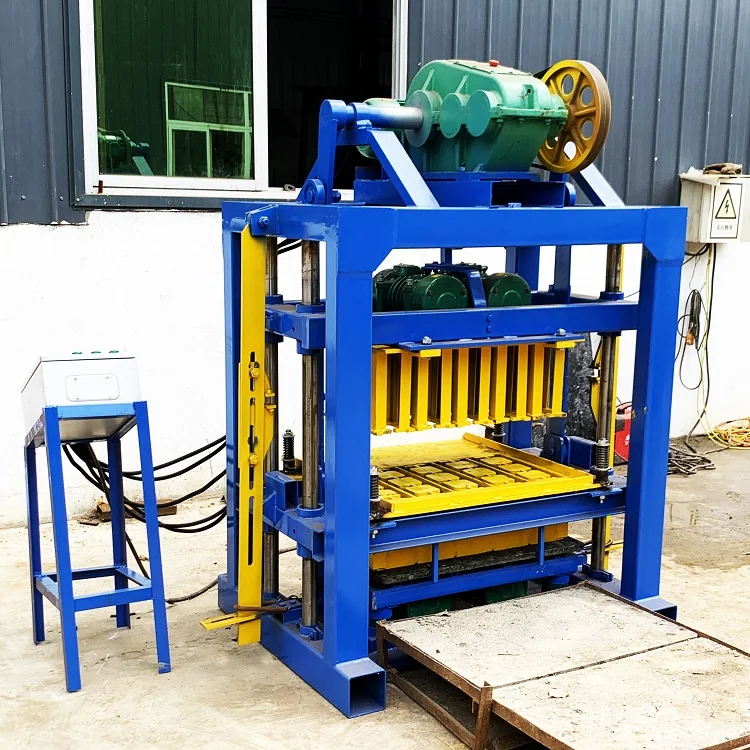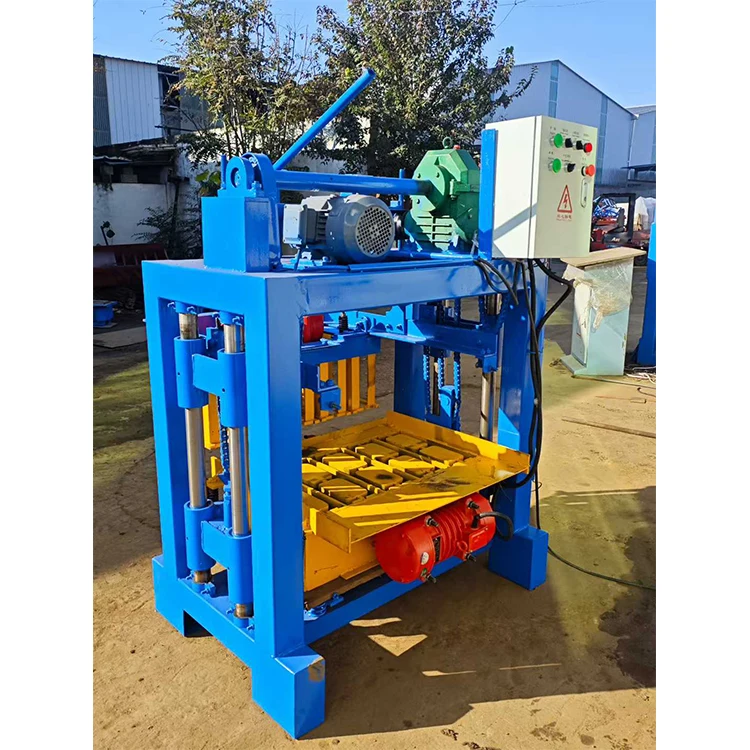
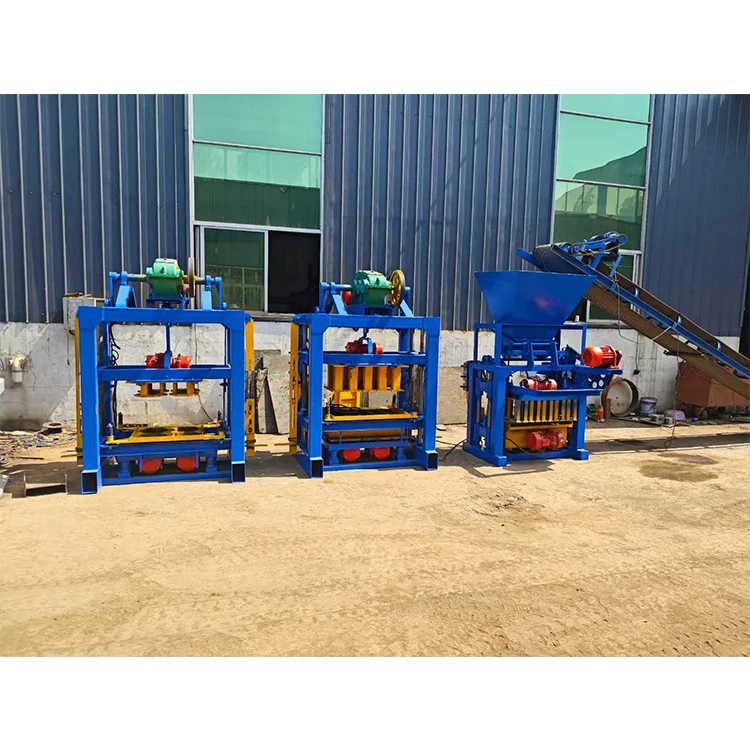
Description
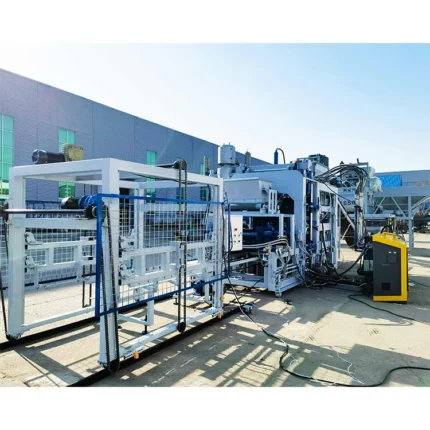
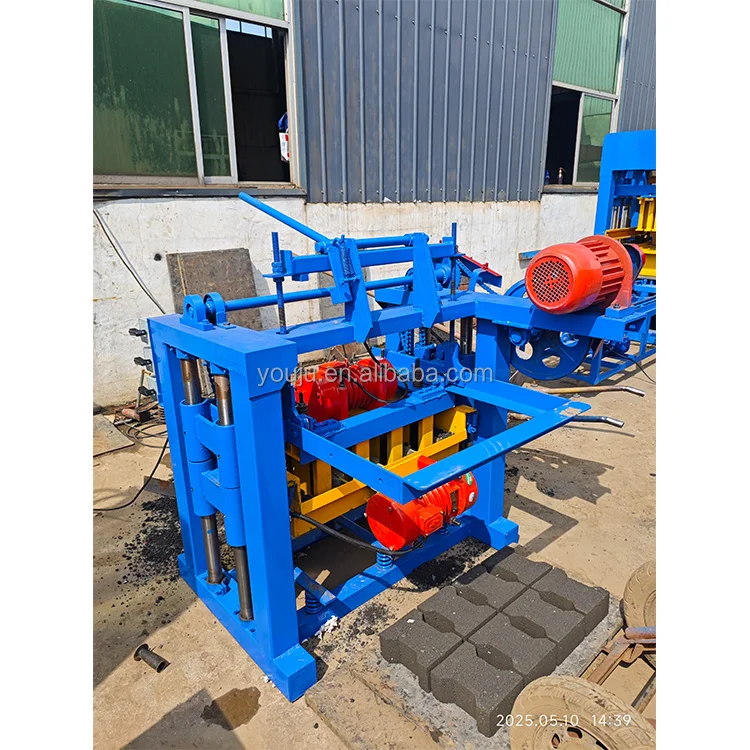
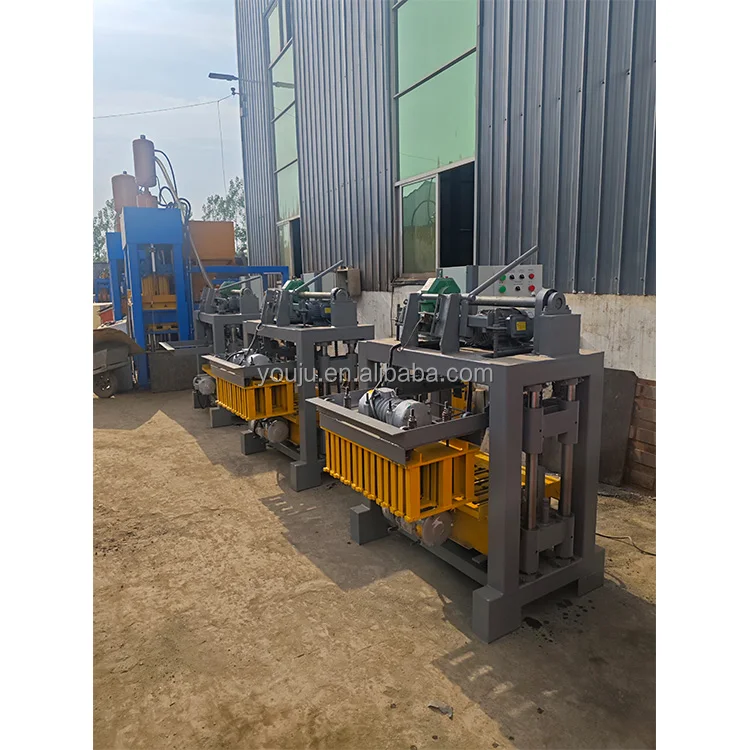
Block machinery focus — machine, mould, pallet and handling are specified as one matched system rather than assembled from separate suppliers.
Technical Specifications
| Parameter | Value |
|---|---|
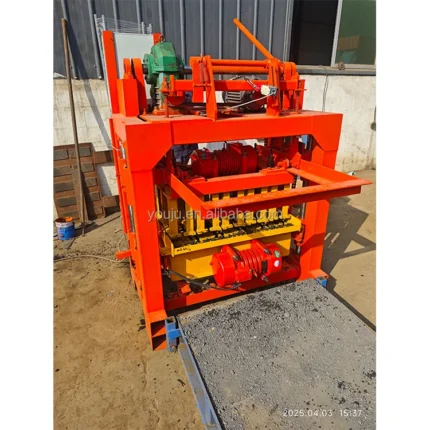
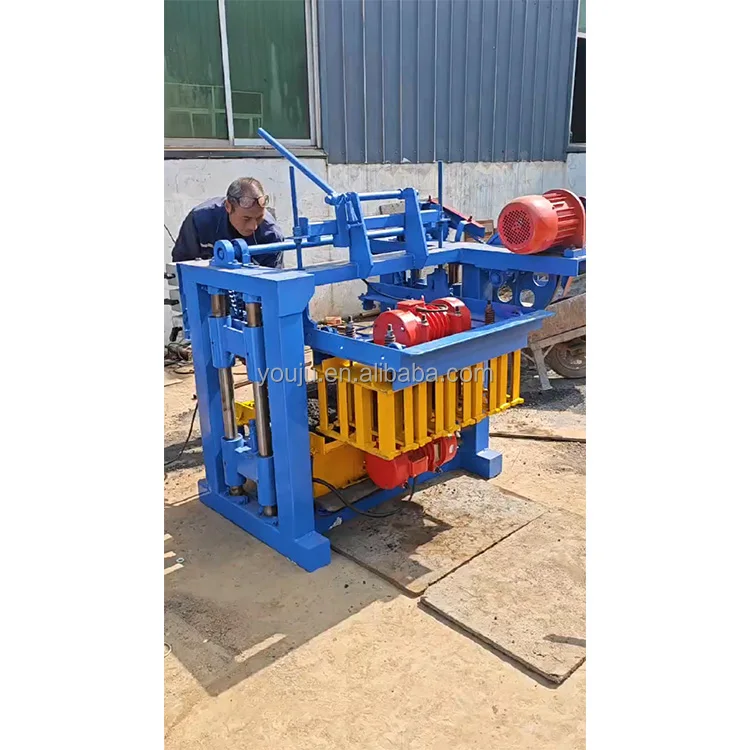
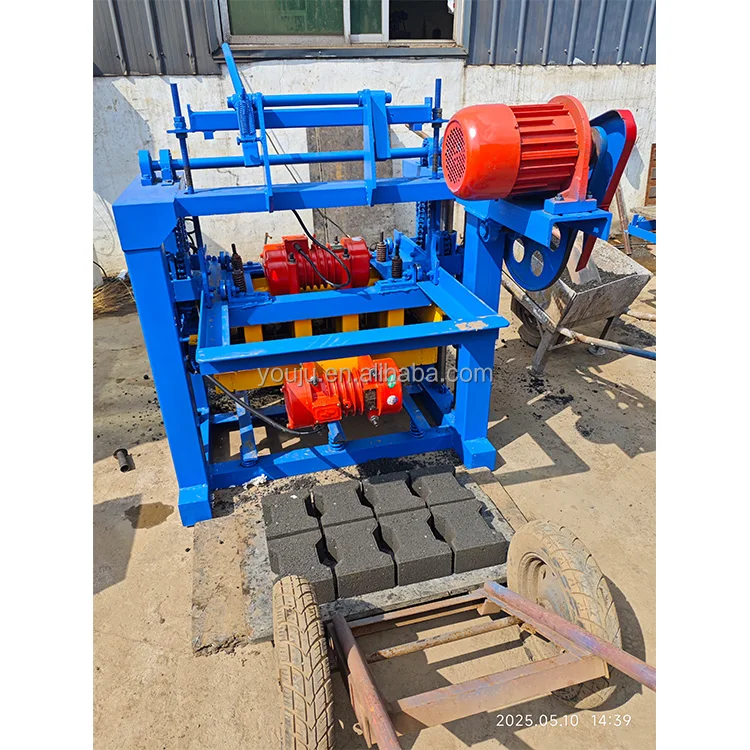
| Model | QTJ4-40 |
| Product Type | Manual Concrete Block Making Machine |
| Rated Power | 10.4 kW |
| Voltage & Frequency | Three-phase four-wire (basis to be confirmed) |
| Control System | Electrical control and mechanical interworking |
| Overall Dimensions (L×W×H) | 1350×1460×1800 mm |
| Net Weight | 1200 kg |
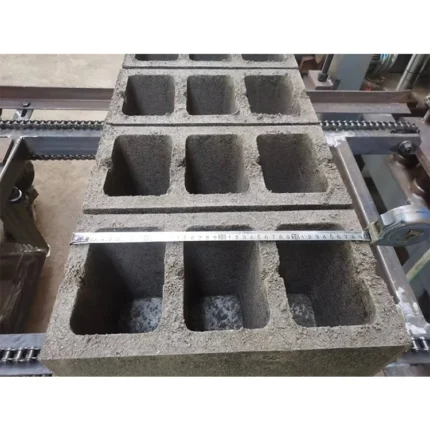
| Output Capacity | 2400 pcs/hour based on 400×200×200 mm hollow block, 5 pcs/mould |
| Molding Cycle | 40 s |
| Pallet Size | 850×450×20 mm |
| Vibration Frequency | 2800 r/min |
| Vibration System | Table vibration feeding with upper and lower vibrators |
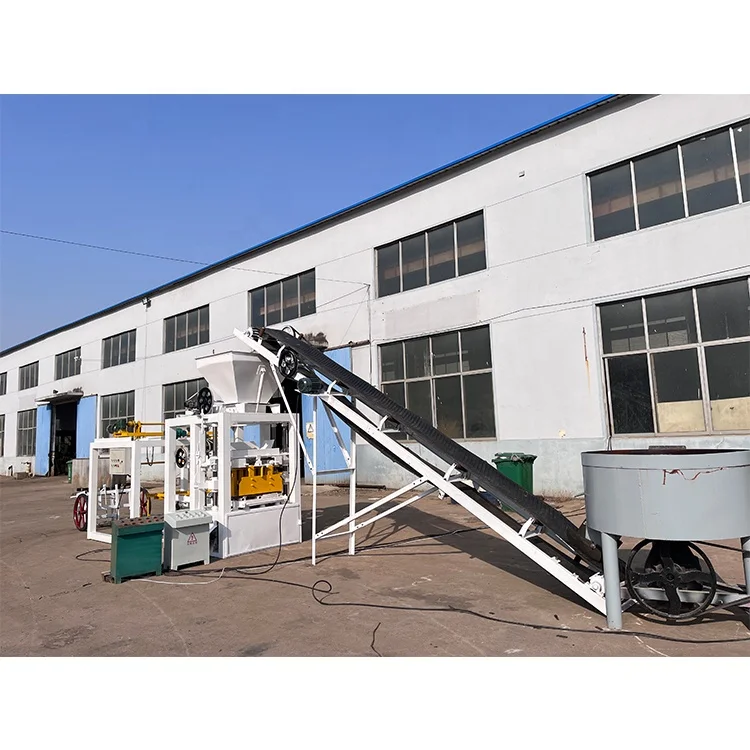
| Assembly State | Host machine, 1 set block mould, JQ350 mixer |
| Mixer Type | JQ350 vertical type (requires 35# gear oil) |
Application Suitability
| Application | Material or Output |
|---|---|
| Small-scale hollow block production | Crushed stone, sand, cement, water |
| On-site construction block manufacturing | Local aggregate mixed to contractor specification |
| Start-up block plant operations | Solid block and hollow block formats |
| Basic concrete masonry unit supply | Standard concrete mix without full automation |
Why the Language and Voltage Question Should Come Before the Price
The QTJ4-40 electrical-mechanical interworking reduces faulty operation damage, but a PLC controlled block machine upgrade is what actually delivers repeatability across shifts.
I once saw a manual panel shipped to West Africa with the control labels in Chinese, and the site crew spent two full days just trying to power it on through a remote video call. When an operator has to manually time each pallet feed and mould release on the QTJ4-40, batch consistency depends entirely on their pace [NEED_CITE: voltage and frequency standards by export market]. An automatic QTJ4-40 block machine upgrade path replaces that manual rhythm with a programmable cycle, removing the variable of human fatigue from the equation.
What the Operator Still Does by Hand
The QTJ4-40 requires the operator to position each pallet, trigger the vibration cycle, and move finished blocks to the curing area manually. This works for a first plant where labour is available and production targets are moderate. When a buyer later adds a PLC controlled block machine to the line, those repetitive tasks shift from human hands to programmed sequences. The result is not just labour reduction — it is cycle-to-cycle timing that stays constant whether it is the first hour of a shift or the last.
Where Manual Control Hits Its Ceiling
Electrical-mechanical interworking on this machine prevents certain misoperations, but it cannot store recipes or enforce a fixed cycle sequence [NEED_CITE: CE machinery directive requirements for industrial equipment]. A PLC controlled block machine records the vibration duration, pressure timing and pallet feed interval, then repeats them identically for every block produced. For buyers who plan to supply blocks with a consistent strength requirement, this repeatability is the dividing line between a workshop output and a commercial product.
Reading the Specs That Actually Matter on Site
The 850×450×20 mm pallet size must match the curing racks and forklifts already on site — otherwise the buyer either replaces the curing infrastructure or runs a mismatched system from day one. The 2800 r/min vibration frequency, paired with upper and lower vibrators, is designed for standard concrete mixes with local aggregate, but the hydraulic and vibration forces must be confirmed against the buyer’s actual mix design rather than a catalogue default. The 40-second moulding cycle delivers the stated output only when pallet feeding keeps pace; manual pallet handling typically stretches the real cycle time beyond the rated figure.
The Hidden Cost of Leaving Automation Out
When pallet handling, stacking and curing are not included in the initial line specification, the operator ends up moving every pallet and stacking every block by hand. This is not just a labour cost — it is a bottleneck that caps real daily output below the quoted figure [NEED_CITE: manual versus automated cycle time impact on daily output]. Buyers who later realise they need an automatic stacking system often discover that the original press was not configured with the sensor mounting points or control interfaces to accept one, forcing a full machine replacement instead of a staged upgrade.
Why Buyers Source the Full Line Here
Block machinery is the single focus of this operation, so the press, mould, pallet and handling equipment are specified as one matched set rather than pulled from unrelated suppliers. The configuration is built around the buyer’s actual mix design and target block format, not a catalogue default. Mould design covers the formats the buyer’s local market actually sells, including custom drawings when standard formats do not apply. Automation level is selectable, meaning a buyer can start with the manual QTJ4-40 and add pallet feeding or stacking later without replacing the press. Installation includes on-site commissioning and operator training so the crew understands the machine before the service team leaves.
Documentation & Verification
- Line layout with capacity calculation stating the 400×200×200 mm hollow block format assumed
- Voltage, frequency and control language confirmation sheet signed before dispatch
- Factory test record on the buyer’s specific mould format and mix proportion
- Mould drawing and format list covering all block types included in the order
- Wear parts and mould replacement list for first-year maintenance planning
Installation, Commissioning & Support
- Foundation pad sized to the 1350×1460 mm machine footprint with level tolerance confirmed
- Dedicated three-phase circuit matched to the confirmed voltage and frequency before arrival
- JQ350 mixer installed upstream with 35# gear oil filled and drive belt tension checked
- Vibration frequency and moulding cycle calibrated on site against the buyer’s local aggregate
- Operator training covering manual pallet feeding, mould change sequence and daily lubrication points
What to Include in Your Next Inquiry
A clear specification starts with the block format your market sells, the realistic daily output target, and the raw materials available locally. Include your site voltage and frequency, the control language your operators read, and whether you already have curing racks and forklifts that the pallet size must match. If you are planning a future automatic QTJ4-40 block machine upgrade path, state that upfront so the press can be delivered with the correct interfaces.
Frequently Asked Questions
Q: What manual tasks does the QTJ4-40 leave to the operator, and what does a PLC-controlled upgrade remove?
A: On the QTJ4-40, the operator handles pallet feeding, cycle triggering and finished block stacking manually. A PLC controlled block machine automates pallet feeding and stacking, locks the moulding cycle to a fixed duration, and removes operator pace as a variable in daily output and block strength consistency.
Q: How do I confirm voltage, frequency and control language before the machine ships?
A: These three items are confirmed in writing during the quotation stage and recorded on a sign-off sheet before production begins. The control panel language is set to the operator’s working language so commissioning starts without delay on arrival [NEED_CITE: export documentation requirements for industrial machinery].
Q: What is the realistic daily output when pallet feeding and stacking are done by hand?
A: The stated capacity of 19,200 pieces per day is based on a 400×200×200 mm hollow block at 5 pieces per mould with a 40-second cycle. Manual pallet feeding and stacking typically extends the actual cycle time, so real daily output depends on operator pace and curing area logistics.
Q: Can the QTJ4-40 be upgraded to semi-automatic pallet feeding without replacing the press?
A: When the press is specified with the correct sensor mounting points and control interfaces at the time of order, semi-automatic pallet feeding and stacking modules can be added later. This avoids the cost of replacing the entire press when production volume grows beyond manual handling capacity.