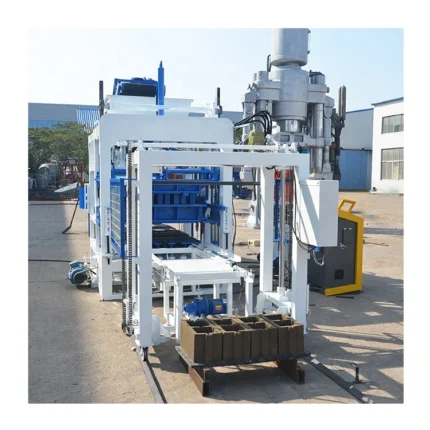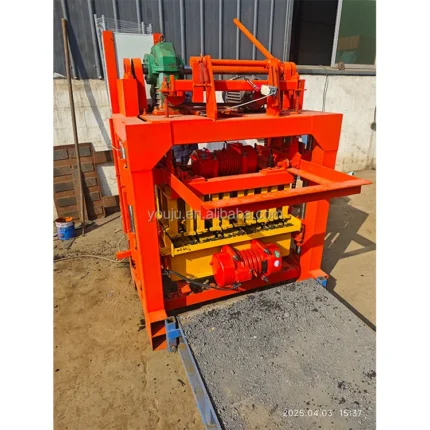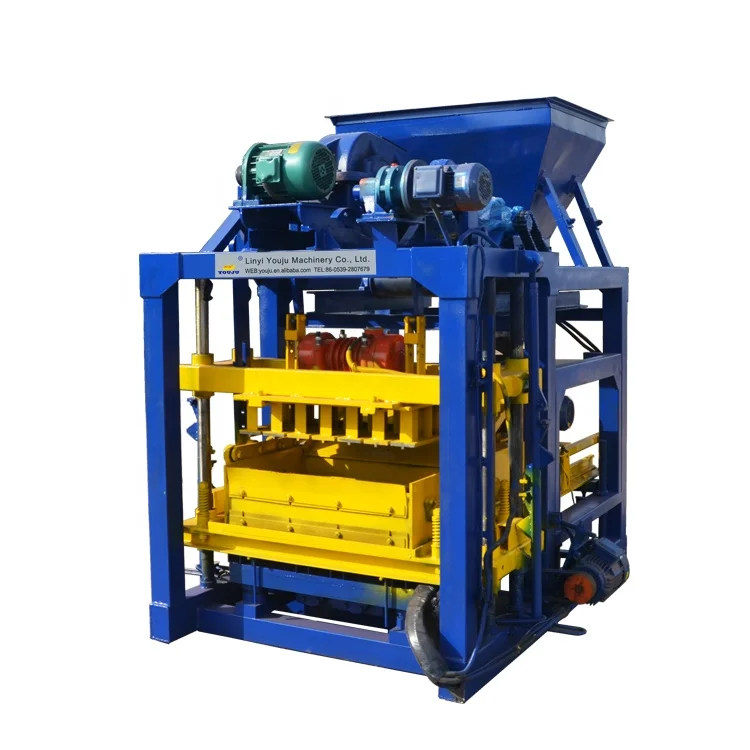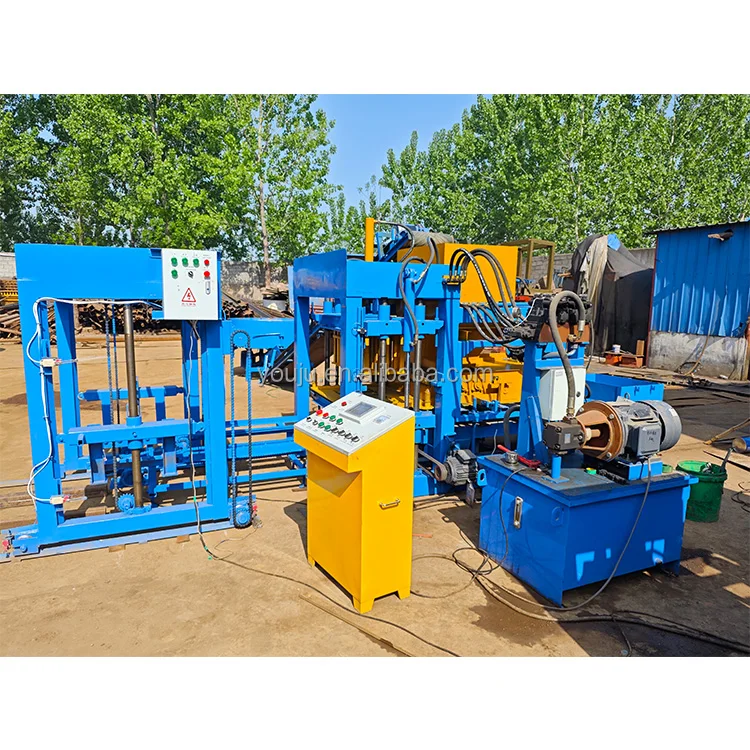


Description
PLC Automation as a Matched System — every control parameter on the QT4-15 is set against the buyer’s actual block format and local voltage, not left at factory default.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-15 |
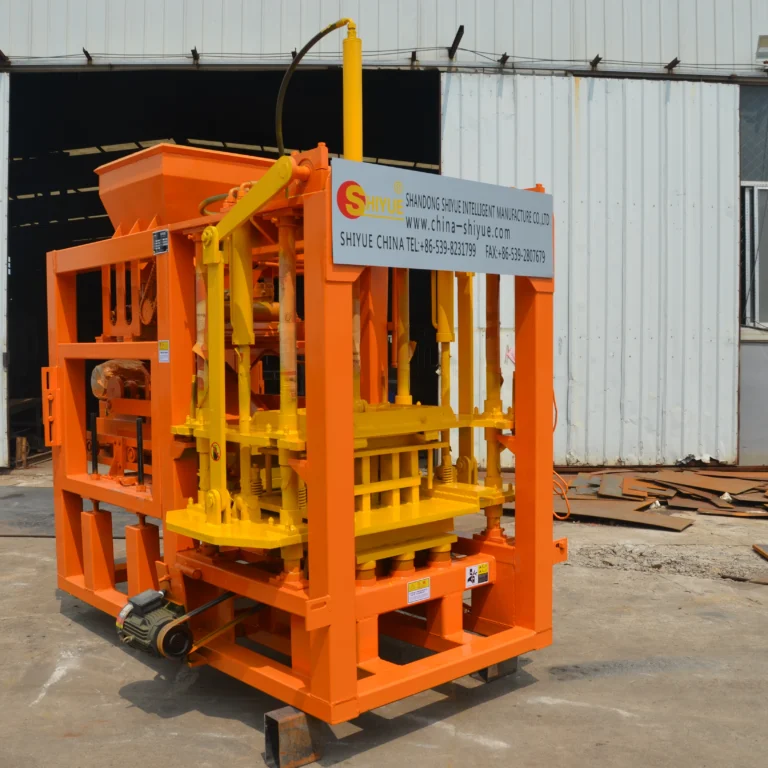
| Product Type | Hydraulic Concrete Block Making Machine |
| Control System | PLC controlled |
| Demolding Method | Hydraulic |
| Molding Cycle | 15-30 s |
| Pallet Size | 900 × 500 mm |
| Vibration Type | Platform vibration |
| Vibration Frequency | 50-70 Hz |
| Product Height Range | 50-220 mm |
| Overall Power | 24.5 kW |
| Voltage & Frequency | Configurable to site requirement (basis to be confirmed) |
| Hydraulic Pressure | To be confirmed per site specification |
| Vibration Force | To be confirmed per site specification |
| Block Compressive Strength | >15 MPa |
| Automation Level | Automatic pallet feeding, material feeding, vibrating, and demoulding |
| Electrical & Hydraulic Components | Original imported or China famous brand (specific brands to verify against manufacturer catalog) |
| Output Format | Capacity (basis: 15-20 s cycle) |
|---|---|
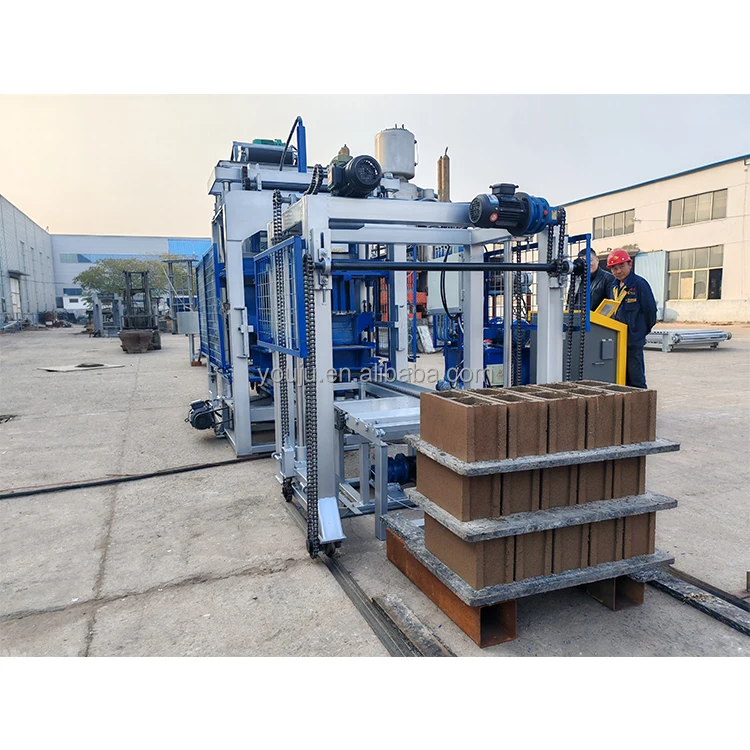
| Hollow Block 400×200×200 mm | 900-1200 pcs/h, 7200-9600 pcs/8 hr (4 pcs/mould) |
| Hollow Block 400×150×200 mm | 1080-1440 pcs/h, 8640-11520 pcs/8 hr (5 pcs/mould) |
| Hollow Block 400×100×200 mm | 1440-1920 pcs/h, 11520-15360 pcs/8 hr (8 pcs/mould) |
| Paver 200×100×60 mm | 2880-3840 pcs/h, 23040-30720 pcs/8 hr (16 pcs/mould) |
| Solid Brick 240×115×53 mm | 5930-6720 pcs/h, 47400-53700 pcs/8 hr (28 pcs/mould) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for masonry walls | Fly ash, slag, sand, crushed stone mixed with cement |
| Paver brick manufacturing for walkways and yards | Crushed stone and cement with fine aggregate face mix |
| Solid brick production for load-bearing structures | Gangue, sand, and cement at high compaction density |
| Medium-scale block plants upgrading from manual operation | Industrial residue materials as primary raw feed |
What the PLC Screen Actually Shows When the Power Comes On
An automatic QT4-15 block machine is only as automatic as the language its operator can read and the voltage its contactors can accept.
I once shipped a unit to a Southeast Asian site where the control panel arrived fully in Chinese characters. The local crew stared at the HMI on day one of commissioning, unable to start a single cycle. We spent two full days remotely flashing the firmware before the press could run, and the contractor lost an entire week of production against a project deadline that did not move. Since then, the PLC display language and the control circuit voltage are locked in before production starts, not discovered when the container is opened [NEED_CITE: PLC HMI language configuration standards for export machinery]. The QT4-15 automatic block making machine is configured so that the intelligent side — what the PLC removes from the operator and what it adds in consistency — actually works from the first shift.
Removing the Operator from the Pressing Cycle
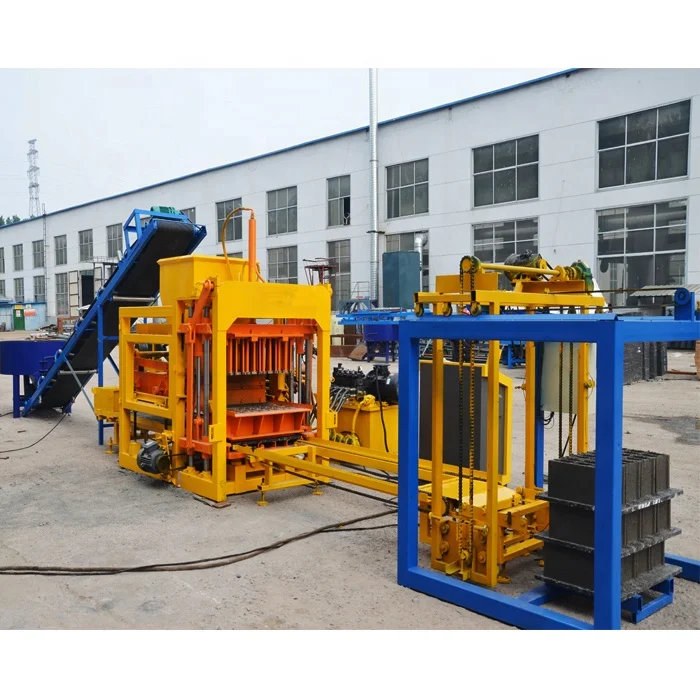
The PLC on the QT4-15 covers pallet feeding, material dosing, vibration timing, and hydraulic demoulding as one sequenced loop. Once the cycle parameters are set for a given mould, the operator loads raw material and monitors the line rather than pulling levers at each station. This is where automation stops being a label and starts being batch-to-batch repeatability — the twentieth pallet of hollow blocks carries the same density as the first.
Where Automation Ends and the Line Begins
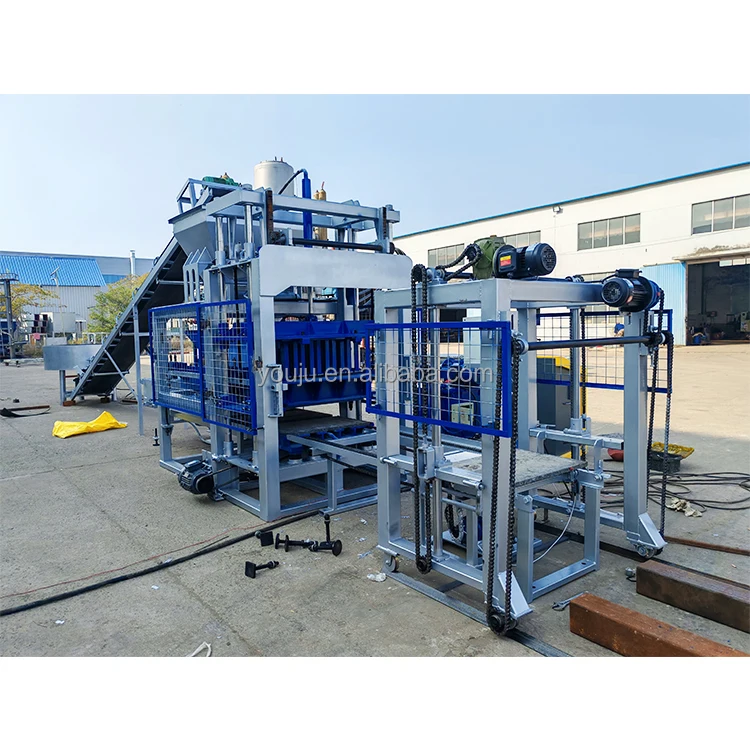
A PLC-controlled concrete block making machine presses blocks at a fixed cycle, but the line around it determines whether the press ever waits. Pallet return speed, material hopper refill timing, and the stacking station downstream must all match the 15-30 s cycle or the press idles. The QT4-15 automation level is selectable, meaning a buyer can start with automatic pressing and manual pallet handling, then add automatic stacking and cubing later when volume justifies the labour shift [NEED_CITE: block production line automation upgrade stages].
Reading the Numbers That Matter
Platform vibration at 50-70 Hz works with hydraulic pressure to compact the mix into the mould cavity. The two forces must be matched to the buyer’s aggregate — a coarse crushed stone mix needs different vibration amplitude than a fine fly ash blend, and getting this wrong produces blocks that pass the press but crumble at the curing rack. The 900 × 500 mm pallet size dictates how many blocks per cycle, which is why output figures above are stated per mould count and cycle time rather than as a single peak number. Mould interchangeability across hollow block, paver, and solid brick formats means the same press serves different product lines, provided the mould change procedure is planned into the shift rather than left as a surprise.
When the Control Cabinet Speaks the Wrong Language
A PLC display in a language the local operator cannot read turns an automatic machine into a manual one that nobody knows how to run. Voltage mismatch is worse — contactors chatter, fuses blow, and the servo valves in the hydraulic station respond erratically, producing blocks with inconsistent density that may not surface until the compressive strength test fails days later. Both issues are entirely preventable before shipment, yet they remain among the most common commissioning delays on export machinery [NEED_CITE: common causes of export machinery commissioning failure].
Why This Is Where the Conversation Starts
Block machinery is the single focus here, so the QT4-15 press, its moulds, pallets, and handling equipment are specified as one matched system rather than assembled from separate suppliers. The automation level is selectable, letting a buyer begin with PLC-controlled pressing and add automatic stacking when production volume grows. Voltage, frequency, and PLC display language are confirmed before production so the machine runs on day one. Mould design covers the formats the buyer’s market actually sells, and the configuration is set against the buyer’s mix design and local aggregate, not a catalogue default. Installation includes operator training so the crew understands the PLC sequence rather than memorising button positions.
Documentation & Verification
- Line layout showing pallet flow from feeder through press to stacking station
- Capacity calculation listing each block format and its assumed cycle time
- PLC display language and control voltage confirmed in writing before production
- Electrical and hydraulic schematic with component brand list for local sourcing
- Factory test record run on the buyer’s specified mould format before dispatch
- Operation and maintenance manual in the confirmed operator language
Installation, Commissioning & Support
- Foundation plan matched to the 24.5 kW overall power and hydraulic station footprint
- Dedicated circuit sized to the confirmed voltage and frequency before machine arrival
- PLC parameters loaded for the buyer’s mould format and verified at first cycle
- Operator training covering the full automatic sequence from pallet feed to demoulding
- Mould change procedure with tools and estimated change time documented per format
- Wear parts list covering hydraulic seals and vibration components with reorder intervals
What to Prepare Before Enquiry
Share the block formats your market sells and the daily volume you need per format so the capacity calculation is honest from the start. Confirm your site voltage, frequency, and the language your operators read so the PLC cabinet arrives ready to run. Describe your raw material source — whether fly ash, slag, or local crushed stone — and any existing pallet size or curing rack layout, so the line fits what you already have on the ground.
Frequently Asked Questions
Q: How is the output capacity calculated, and which block format does each figure assume?
A: Every capacity figure is stated with the mould count and cycle time behind it. For example, hollow block output at 400×200×200 mm is based on 4 blocks per mould at a 15-20 s cycle. Different formats produce different counts per pallet, so the daily output you plan against must match the format you will actually run.
Q: What automation level is included in the quotation?
A: The base QT4-15 covers automatic pallet feeding, material dosing, vibration, and hydraulic demoulding. Stacking and cubing downstream are selectable additions. The quotation states exactly which stations are automatic and which remain manual so there is no gap between expectation and delivery.
Q: Can the PLC display language and control voltage match my site before shipment?
A: Both are confirmed in writing before production begins. The HMI is loaded in the operator’s language, and the control circuit is wound to the site’s voltage and frequency. This is locked into the order so the machine runs on the first day of commissioning.
Q: How long does a mould change take, and what is required?
A: Mould change procedure and estimated time are documented per format and supplied with the quotation. The tools needed are listed, and the operator training covers the full swap so format changeover is planned into the shift rather than consuming it.
Q: What is the upgrade path if production volume grows?
A: The automation level is selectable in stages. A buyer can start with PLC-controlled pressing and manual pallet handling, then add automatic stacking and cubing later. The press itself does not need replacement — the line around it extends as volume justifies the investment.