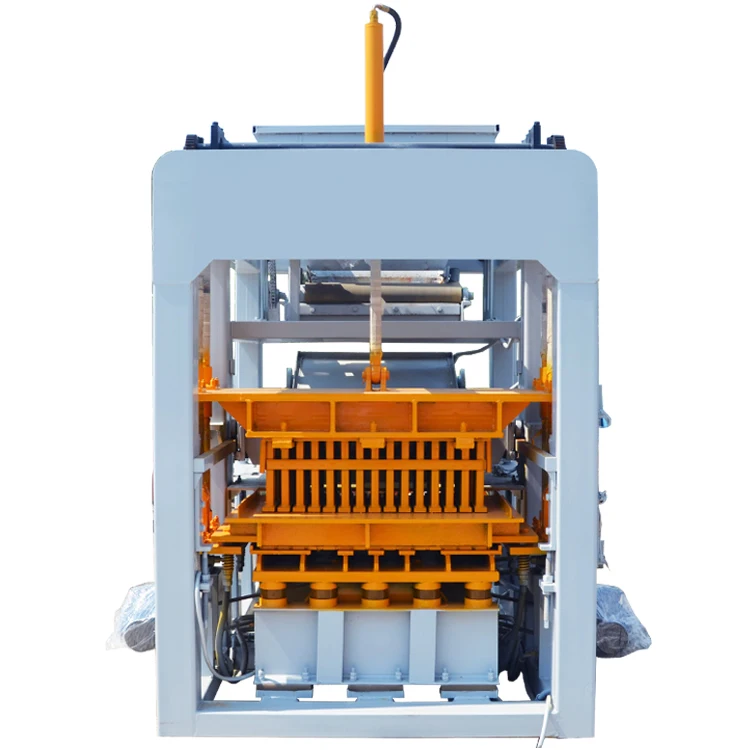
Description
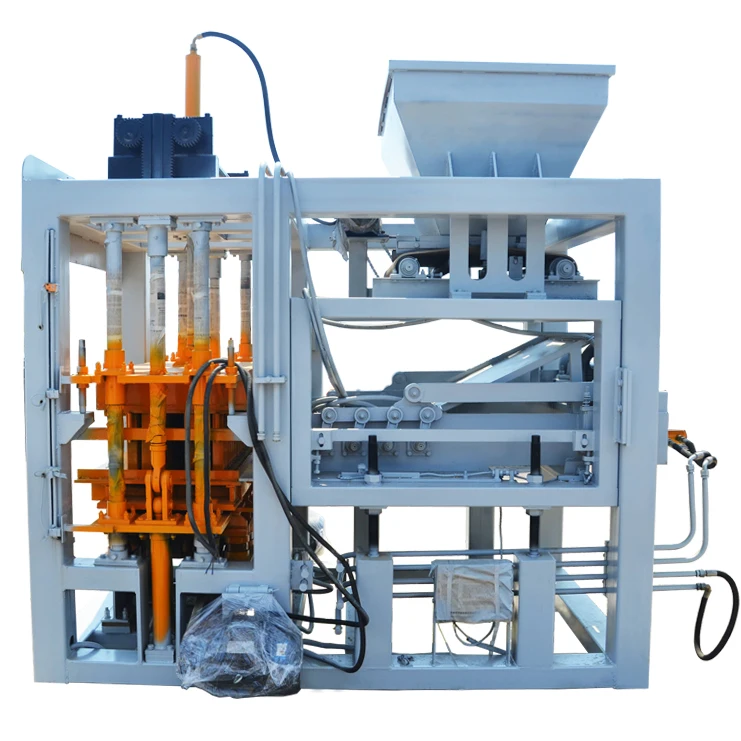
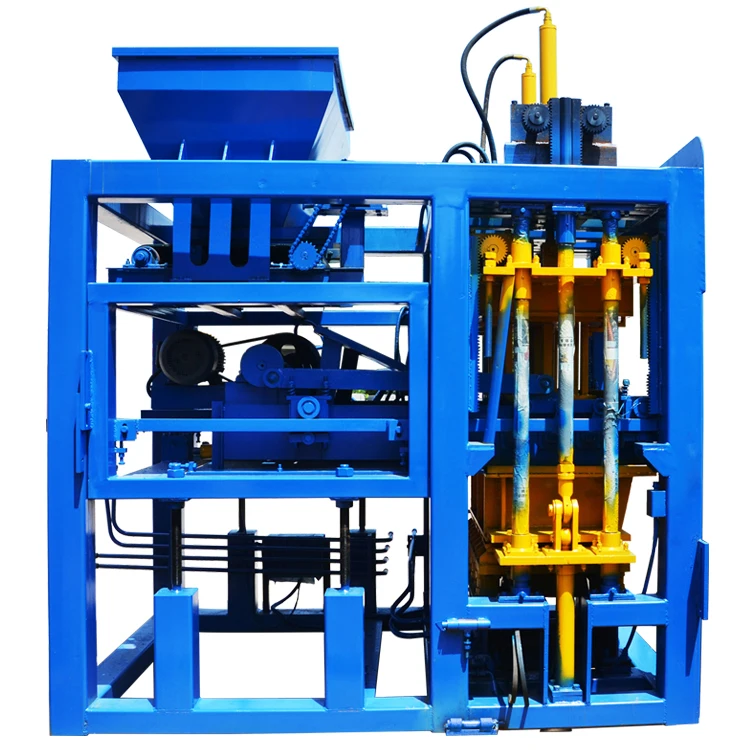
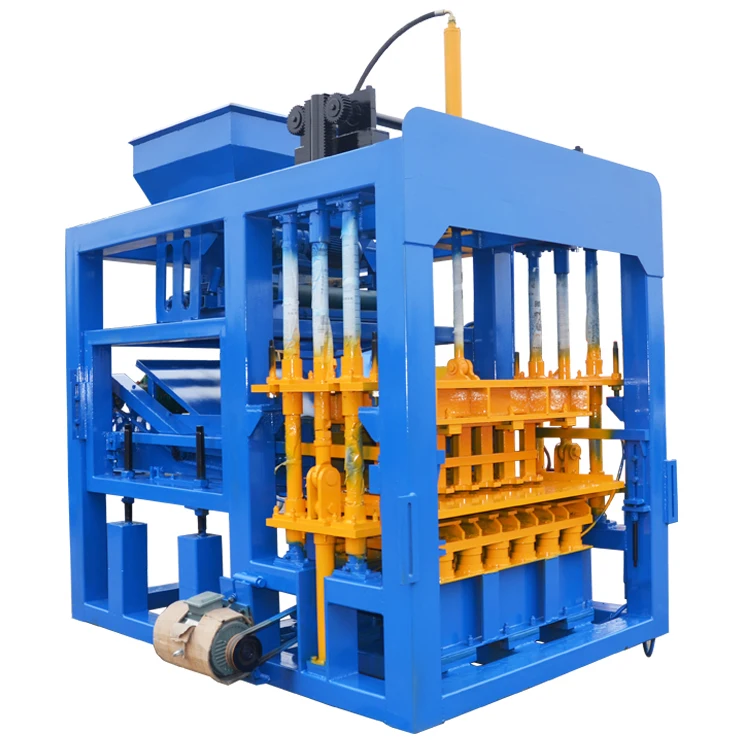
Intelligent control logic — every parameter from vibration timing to pallet feed rate is governed by the PLC, eliminating operator guesswork across block formats on the QT14-15 line.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Automatic Concrete Block Making Machine |
| Model | QT14-15 |
| Control System | PLC computer control, fully automatic |
| Vibration Mode | Multiaxis synchronizer vibration (vertically downward) |
| Hydraulic System | High thermal efficiency, low heat productivity |
| Mixer System | Multiaxis forced mixer system |
| Guide Bearing | Long-period over-length guide bearing for upper mould and mould box alignment |
| Rack Construction | High-strength steel with special welding technique (vibration shock resistant) |
| Moulding Cycle | 15–20 s (basis not stated in source) |
| Output — 400×200×200 mm hollow block | 900–1,200 pcs/h, 7,200–9,600 pcs/8 hr |
| Output — 400×150×200 mm hollow block | 1,080–1,440 pcs/h, 8,640–11,520 pcs/8 hr |
| Output — 400×100×200 mm hollow block | 1,440–1,920 pcs/h, 11,520–15,360 pcs/8 hr |
| Output — 200×100×60 mm paving block | 2,880–3,840 pcs/h, 23,040–30,720 pcs/8 hr |
| Output — 240×115×53 mm solid brick | 5,930–6,720 pcs/h, 47,400–53,700 pcs/8 hr |
| Automation Level | Fully automatic |
| Mould Formats | Hollow block, solid brick, paving block, kerb stone |
| Warranty | 1 year for whole machine (excluding spare parts) |
| Rated Power | Available upon request |
| Voltage & Frequency | Configurable before production |
| Pallet Size | Determined by buyer’s curing area and handling equipment |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production plants | Crushed stone, cement, sand, fly ash aggregates |
| Paving block manufacturing | Dense aggregate blends for high compressive strength |
| Solid brick runs | Fine sand and cement mixes for standard masonry units |
| Kerb stone production | Coarse aggregate with high cement content for weather resistance |
| Multicellular brick lines | Lightweight aggregate or aerated concrete blends |
Why PLC Logic Matters More Than the Cycle Time Claim
A cycle number without a control architecture behind it is just a guess.
I have watched buyers compare machines based on "15-second cycles" from brochure tables, only to discover on commissioning day that the PLC could not hold the timing when the ambient temperature dropped and the hydraulic fluid thickened. The automatic block making machine PLC controlled system on the QT14-15 adjusts vibration duration and pressure dwell within parameters set during factory testing, so the cycle stays stable across shifts. Without that feedback loop, operators manually trim cycle times and block density drifts from batch to batch [NEED_CITE: PLC closed-loop control standards for hydraulic forming presses].
Removing Operator Variance from the Pressing Cycle
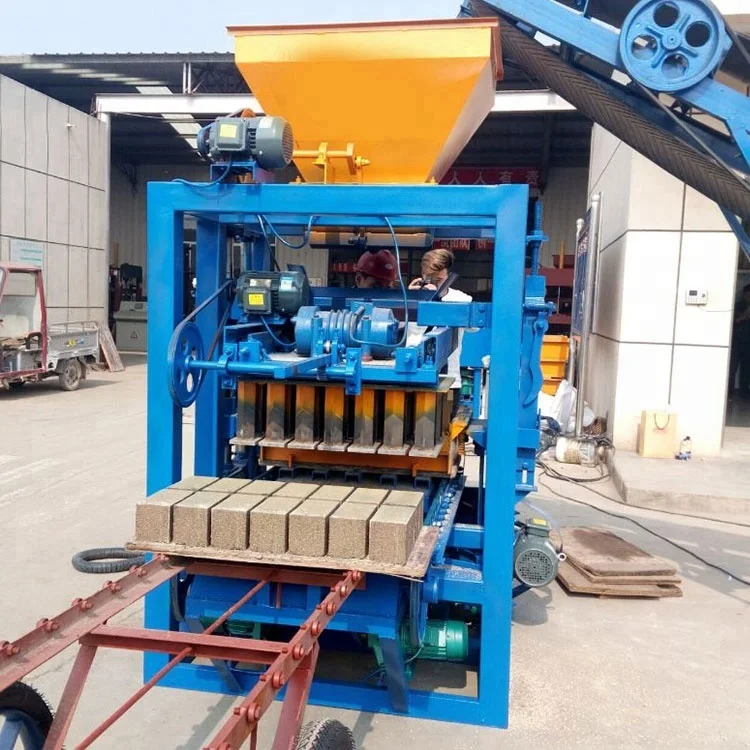
On manual and semi-automatic lines, the operator decides when the mould box fills, when vibration starts, and when the pallet advances. Every decision introduces variance. The automatic block making machine PLC controlled sequence on the QT14-15 takes those decisions away. The PLC fires the feeder, monitors mould box fill level, triggers multiaxis synchronizer vibration, and advances the pallet on a fixed timeline — so block weight and dimensional tolerance stay within spec whether it is the first pallet of the morning or the last before shift change.
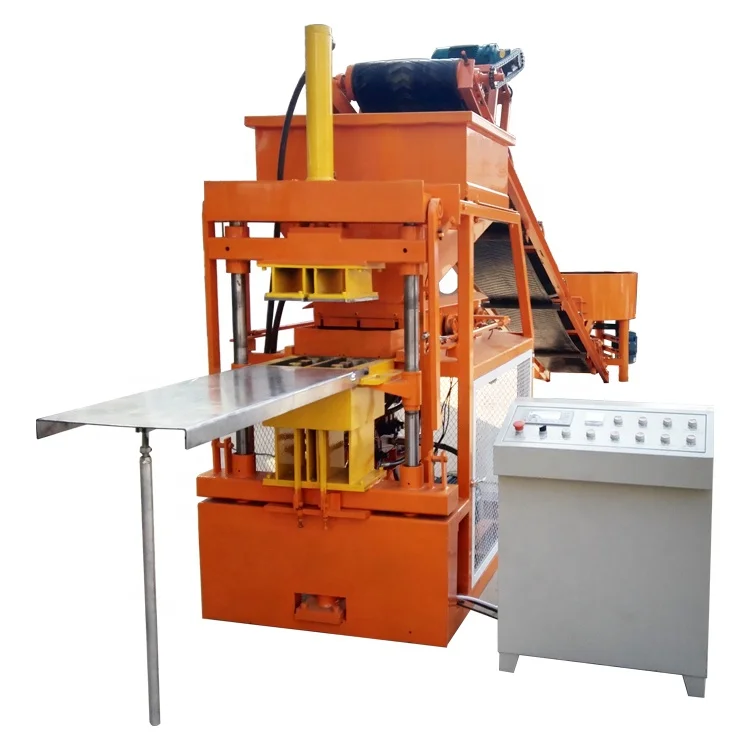
What the Control Panel Actually Shows the Operator
The HMI displays real-time moulding cycle countdown, hydraulic pressure reading, vibration frequency, and alarm codes in the language confirmed before shipment. When a sensor detects a pallet misalignment or a mould box overfill, the system pauses and flags the station rather than letting a defective pallet continue down the line. This is the difference between catching a fault at the press and discovering it at the curing rack hours later [NEED_CITE: HMI alarm response standards for automated building material lines].
Reading the Specs That Actually Move the Needle
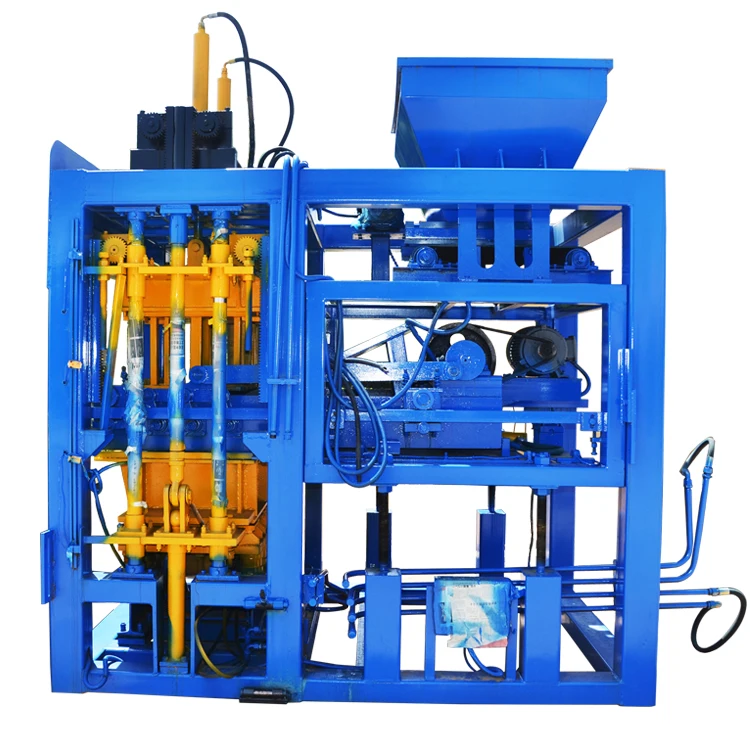
The multiaxis synchronizer vibration delivers vertically downward force, which means compaction energy travels straight through the mould cavity instead of scattering laterally — this directly affects block density and early-stage compressive strength. The long-period over-length guide bearing keeps the upper mould and mould box aligned over thousands of cycles; when that alignment drifts, you see it as uneven block height across the pallet. The high-strength steel rack with special welding technique resists the fatigue cracking that vibration shock causes in lighter frames, so the machine geometry stays true through extended production runs.
When the Wrong Automation Level Costs More Than the Machine
Buyers who jump to fully automatic without confirming their pallet handling and curing rack capacity end up with output stacking faster than it can be moved, forcing them to throttle the press back to semi-automatic speeds anyway. The QT14-15 can be configured with the automation level matched to the buyer’s actual downstream setup — pallet feeding, stacking method, and curing rack handling all need to be specified before the PLC program is locked [NEED_CITE: production line bottleneck analysis for concrete block plants].
Why Buyers Choose This Configuration Path
Block machinery is the single focus here, so the QT14-15 press, mould, pallet, and handling equipment are specified as one matched system rather than sourced separately. The configuration is set against the buyer’s actual mix design and local aggregate, not a catalogue default. Mould design covers the formats the buyer’s market actually sells, including custom drawings. Automation level is selectable, so a plant can start semi-automatic and add stacking or cubing later. Installation and commissioning include operator training so the PLC parameters make sense to the people running the line daily.
Documentation & Verification
- Line layout with capacity calculation tied to each block format assumed
- Machine specification sheet with hydraulic and electrical schematic
- Mould drawing and format list with changeover procedure
- Voltage, frequency, and PLC display language confirmation record
- Factory test record on buyer’s target block format before dispatch
- Operation and maintenance manual with wear parts list
Installation, Commissioning & Support
- Foundation plan matched to QT14-15 vibration load and rack footprint
- Electrical supply verification for confirmed voltage and dedicated circuit rating
- Machine dismantling state documented for container loading and reassembly sequence
- PLC parameter set loaded from factory test and fine-tuned with buyer’s aggregate on site
- Operator training on HMI navigation, alarm response, and mould change procedure
- Wear parts and mould list supplied with first recommended reorder interval
What to Include in Your Inquiry
Tell us the block formats you sell and the daily volume each format must hit, along with your local aggregate type and available mix design report. Confirm your site voltage, frequency, and preferred PLC display language so the control panel arrives ready for commissioning. If you have existing pallets, curing racks, or forklifts, share the dimensions — the pallet size and handling configuration on the QT14-15 will be set to match.
Frequently Asked Questions
Q: How is output capacity verified for each block format on the QT14-15?
A: Each capacity figure is tied to a specific block dimension and moulding cycle. The line layout document states the format assumed, the cycle time used, and the pallet pattern, so you can calculate realistic daily output for your product mix before placing the order.
Q: What PLC language and HMI options are available?
A: The display language is confirmed during the voltage and control confirmation step before production. The HMI shows cycle countdown, pressure, vibration frequency, and alarm codes in the agreed language, so operators can navigate menus and respond to faults without translation delays on site.
Q: How does automation affect labour and what is the upgrade path?
A: The QT14-15 removes manual intervention from the pressing cycle, reducing the operator’s role to monitoring and mould changes. Plants starting with semi-automatic pallet handling can add automatic stacking and cubing later, since the PLC architecture supports module expansion without replacing the core controller.
Q: What voltage and frequency must be confirmed before shipment?
A: Your site voltage, frequency, and phase are locked during the confirmation step so the motor, hydraulic pump, and PLC power supply match your supply on arrival. Shipping a machine with the wrong voltage configuration delays commissioning until replacement transformers or drives arrive.
Q: How are mould changes handled and what is the expected changeover time?
A: The mould drawing package includes the changeover procedure with tool list and alignment checkpoints. Changeover time depends on the format jump and operator familiarity — the long-period guide bearing keeps alignment repeatable, so the new mould seats true without extended trial-and-error adjustment.