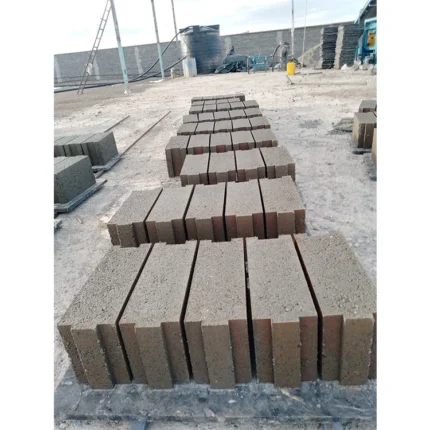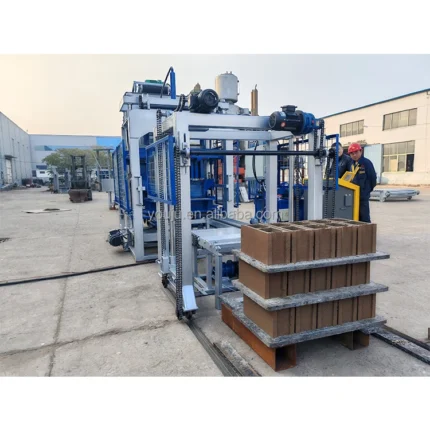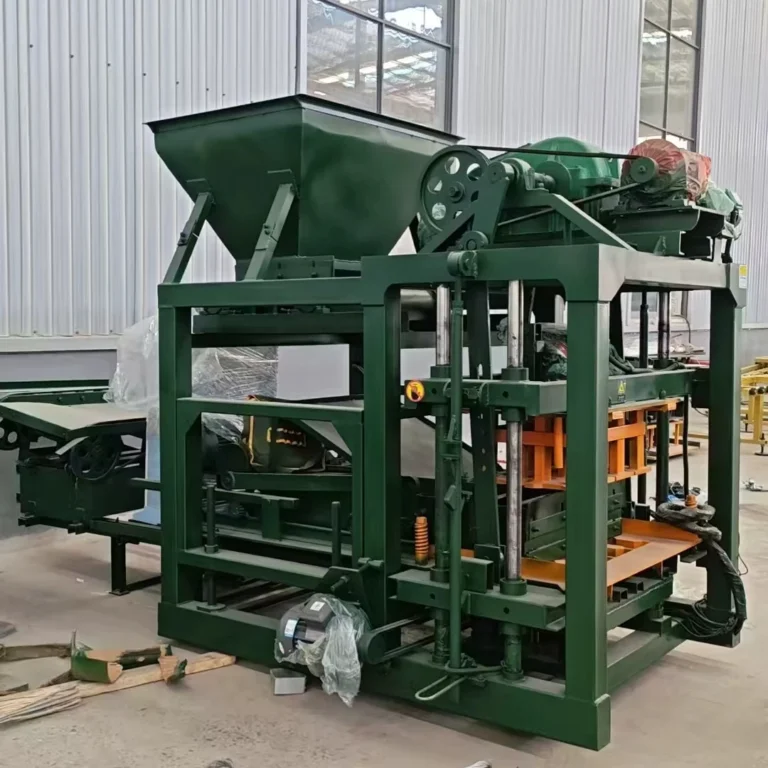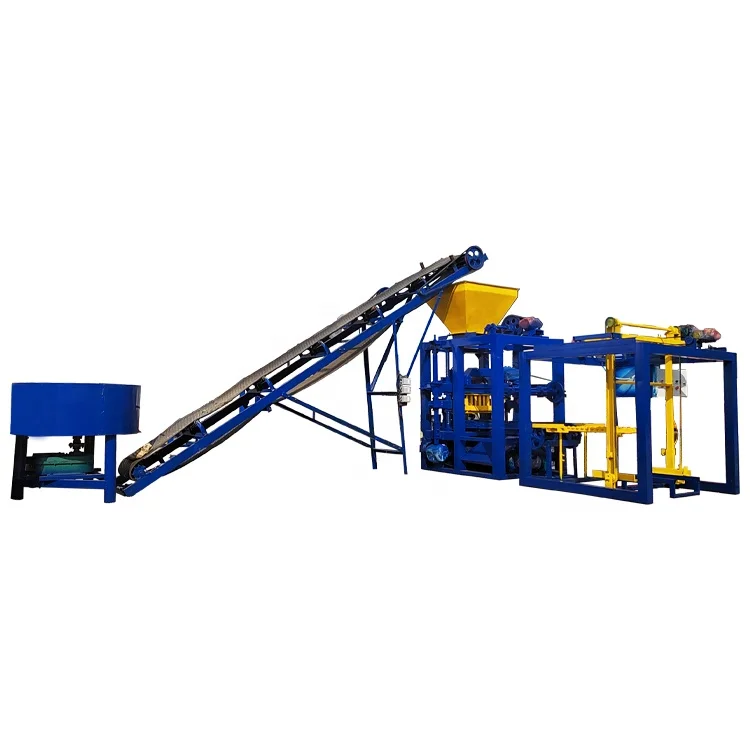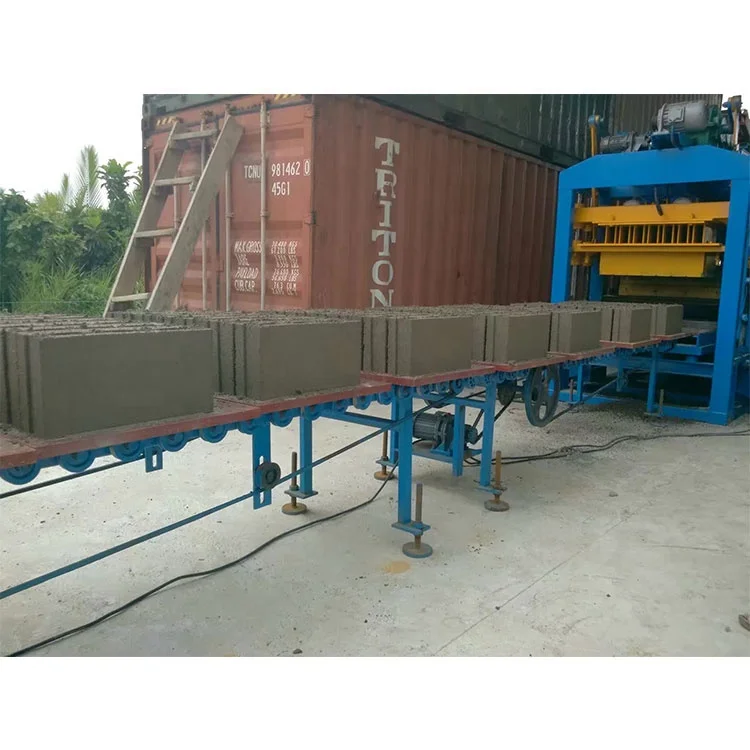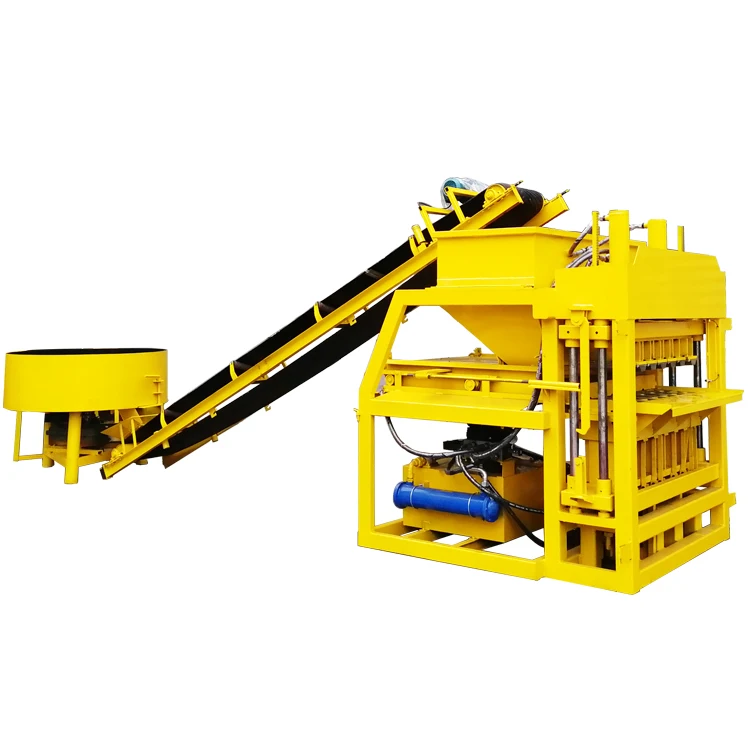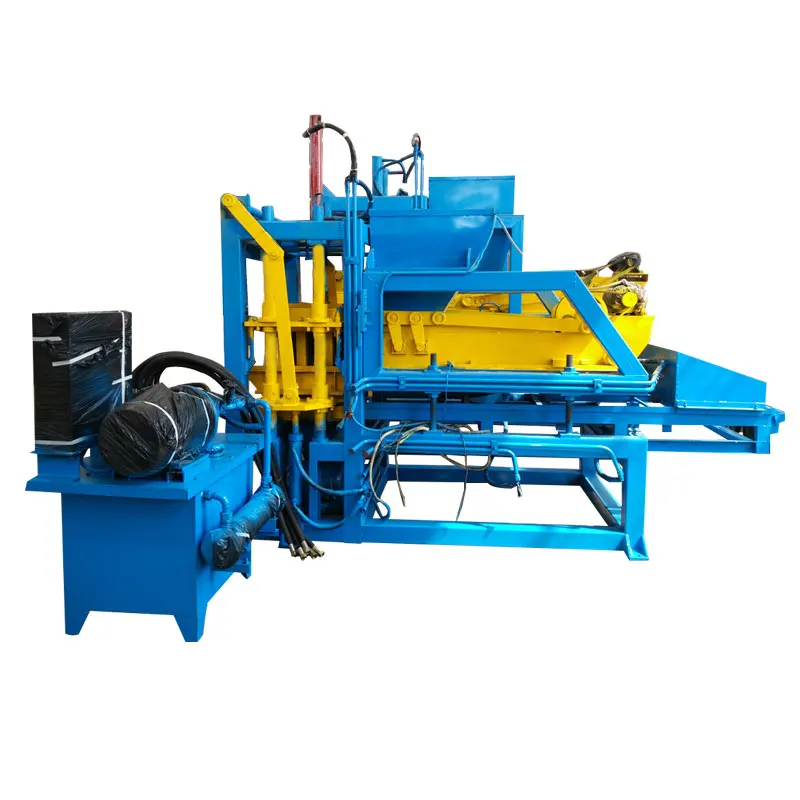
Description
Synchronized Control Logic — Every molding sequence coordinates hydraulic pressure with platform vibration through the PLC, removing timing guesswork from the operator’s daily routine.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-20 |
| Product Type | Stationary Block Machine |
| Overall Dimensions (L×W×H) | 7100×1600×2610mm |
| Molding Area | 400×800mm |
| Pallet Size | 1020×570mm |
| Rated Hydraulic Pressure | 16-21MPa |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency | 4600 r/min |
| Vibration Force | 40KN |
| Molding Cycle | 15-25s |
| Demolding Method | Hydraulic |
| Overall Power | 27.5KW |
| Total Mass | 5T |
| Control System | Intelligent PLC Controlled |
| Factory Area Required | 500m2 |
| Raw Materials | Crushed stone, sand, cement, dust, fly ash, gravel, slag |
| Output Capacity | 7200-9600 pcs/day (based on 400×200×200mm hollow block, 4 pcs/mold) |
| Output Capacity | 20200-26800 pcs/day (based on 240×115×90mm porous brick, 14 pcs/mold) |
| Output Capacity | 47400-53700 pcs/day (based on 240×115×53mm standard brick, 28 pcs/mold) |
| Cycle Time | 15-20s (Hollow Brick), 15-20s (Porous Brick), 15-17s (Standard Brick) |
| Warranty | One year guarantee for the whole machine |
| Payment Terms | 30% deposit by T/T, 70% balance before delivery |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block manufacturing | Concrete mix with crushed stone and gravel aggregates |
| Solid block production | Sand, cement, and fly ash blends for load-bearing walls |
| Paving brick manufacturing | High-density mix designs for interlocking and kerbstone formats |
| Porous brick production | Lightweight aggregate blends for thermal insulation applications |
| On-site contractor block supply | Local aggregate and cement combinations adjusted to regional sources |
What "Automatic PLC Controlled" Actually Removes From Your Operator’s Plate
The PLC coordinates hydraulic demolding pressure and vibration timing as a single sequence, so the operator monitors instead of adjusting.
When a plant runs two or three block formats across a shift, manual timing adjustments introduce variation that accumulates into inconsistent block density. On construction sites across the Middle East, I have watched operators second-guess cycle timing on every format change because the machine response felt different each time. An automatic PLC controlled stationary block machine eliminates that guesswork by storing cycle parameters per mould and recalling them on demand. [NEED_CITE: PLC programming standards for industrial concrete equipment]
The real value appears during the third shift when fatigue sets in. The control system maintains the same 15-25s molding cycle whether the operator is fresh or running on caffeine. Vibration force at 40KN and hydraulic pressure between 16-21MPa execute in the programmed sequence regardless of who stands at the panel.
Control Logic That Coordinates Pressure and Vibration
The QT4-20 sequences platform vibration at 4600 r/min with hydraulic pressure application through the PLC, ensuring compaction happens under consistent force every cycle. This coordination is what separates repeatable block density from batch-to-batch variation that shows up as strength test failures weeks later.
The system stores separate parameter sets for each block format in production. Switching from 400×200×200mm hollow blocks to 240×115×53mm standard bricks means loading a different program rather than manually adjusting timers and pressure valves. Format flexibility becomes practical only when changeover does not consume half a shift recalibrating the press.
Language, Voltage, and the Details That Stall Commissioning
I once spent three days on a project site waiting for a translator because the PLC display arrived in a language the local electricians could not read. The automatic PLC controlled stationary block machine must arrive with interface language, voltage rating, and frequency confirmed before production starts. These are not optional extras.
Electrical compatibility affects more than whether the motor spins. The control cabinet components, sensors, and solenoid valves all operate within the specified voltage range. A mismatch in any one circuit can prevent the PLC from executing its sequences correctly, turning a fully automated line into a machine that requires manual intervention at every station. [NEED_CITE: voltage and frequency standards by export market]
Matching Vibration Force to Your Local Aggregate
The 40KN vibration force and 16-21MPa hydraulic pressure are rated specifications, but their effectiveness depends on whether they match your actual mix design. Dense granite aggregate requires different compaction energy than lightweight volcanic scoria or recycled demolition material.
The 1020×570mm pallet size defines the molding area at 400×800mm, which in turn determines how many cavities fit per cycle for each block format. Hollow blocks at 400×200×200mm yield 4 pieces per mold with cycle times of 15-20s. Porous bricks at 240×115×90mm fit 14 per mold. Standard bricks at 240×115×53mm pack 28 per mold with cycles of 15-17s. These figures assume the mix design achieves proper flow and compaction within the programmed cycle.
The 27.5KW total power rating covers vibration motors, hydraulic pump, and control systems running simultaneously. If your local power supply experiences voltage fluctuation beyond the system tolerance, the PLC may trigger fault protection mid-cycle, leaving partially compacted blocks on the pallet.
When Automation Stops at the Press
Selecting a PLC-controlled press without specifying how pallets move through feeding, stacking, and curing creates a bottleneck that negates the automation investment. The operator may no longer adjust cycle timing, but they still haul pallets manually if upstream and downstream stations remain unconfigured.
I have seen plants where the press runs at full automatic capacity while workers stack wet blocks by hand because the stacking station was never included in the quotation. The daily output figures assume continuous pallet flow. Any interruption in pallet supply or removal forces the press to idle, and those idle minutes accumulate across the shift into lost production that never appears in the capacity calculation. [NEED_CITE: production line integration standards for block plants]
The curing area must also match the pallet dimensions and daily throughput. Pallets carrying freshly pressed blocks need rack space for the full curing period before they can return to the press. If curing capacity falls short, pallets pile up on the factory floor and the line stops waiting for them to cycle back.
Why Procurement Through This Channel Reduces Configuration Risk
Every order starts with confirmation of your target block format, local aggregate type, and existing equipment layout rather than shipping a catalogue default. The vibration frequency and hydraulic pressure are evaluated against your specific mix design before production begins.
PLC display language, voltage, and frequency are confirmed in writing before the control cabinet is assembled. This prevents the three-day commissioning delay I encountered when a display arrived in the wrong language for the local team.
Mould design covers the formats your market actually sells, including custom drawings when standard cavity layouts do not match your product range. The mould change system specification includes time estimates so you can plan format changeovers into your production schedule.
Capacity calculations state the block format and cavity count assumed for each output figure. Hollow block output of 7200-9600 pieces per day is based on the 400×200×200mm format at 4 pieces per mold, not an abstract maximum across all possible configurations.
Documentation & Verification
- Factory test record demonstrating molding cycle timing on your specified block format before dispatch
- PLC program backup with parameter sets for each confirmed mould configuration
- Hydraulic and electrical schematic matching the as-built cabinet layout and component list
- Voltage rating and control language confirmation document signed before production release
- Pallet specification sheet detailing dimensions and material grade for curing area planning
Installation, Commissioning & Support
- Foundation preparation for 7100×1600mm footprint with leveling tolerances for vibration platform stability
- Dedicated power circuit rated for 27.5KW continuous draw with voltage monitoring at the main disconnect
- PLC parameter loading and cycle verification on your actual raw material mix during commissioning
- Operator training covering format changeover procedure and fault code response on the control display
- Hydraulic system pressure verification against 16-21MPa operating range with local ambient temperature compensation
- Wear parts inventory list matched to your production volume and regional supplier availability
What We Need to Configure Your Line Correctly
Provide your target block formats with dimensions and daily volume requirements so we can calculate cycle counts and confirm the press capacity matches your production plan. Share your local aggregate types and any existing mix designs so vibration force and hydraulic pressure can be evaluated against your material.
Confirm your site voltage, frequency, and the language your electricians and operators need on the PLC display. Let us know what pallet handling and curing equipment you already have so the press cycle time can be coordinated with your upstream and downstream stations.
Frequently Asked Questions
Q: How are daily output figures calculated for different block formats?
A: Each capacity figure is tied to a specific block dimension and cavity count. Hollow block output of 7200-9600 pieces per day assumes the 400×200×200mm format with 4 pieces per mold at 15-20s cycles. Changing to a different format changes the cavity count and cycle time, which changes the daily total accordingly.
Q: Can the PLC interface be set to our local language before shipment?
A: Yes, the display language is confirmed during the ordering process and programmed before the control cabinet leaves the factory. This includes alarm messages, parameter labels, and menu navigation. Confirming this upfront avoids commissioning delays caused by language barriers on site.
Q: Which stations are automated and which still require manual operation?
A: The PLC controls the molding cycle, hydraulic pressure application, and vibration timing. Pallet feeding, block stacking, and curing rack handling may remain manual unless specified in the line configuration. Clarifying automation scope before ordering prevents expectations that do not match the installed system.
Q: How do you match vibration settings to our local raw materials?
A: We review your aggregate type, gradation, and mix proportions before finalizing the vibration frequency and hydraulic pressure settings. Dense crushed stone requires different compaction energy than lightweight aggregates or fly ash blends, and the PLC parameters are adjusted to match your available materials.