

Description
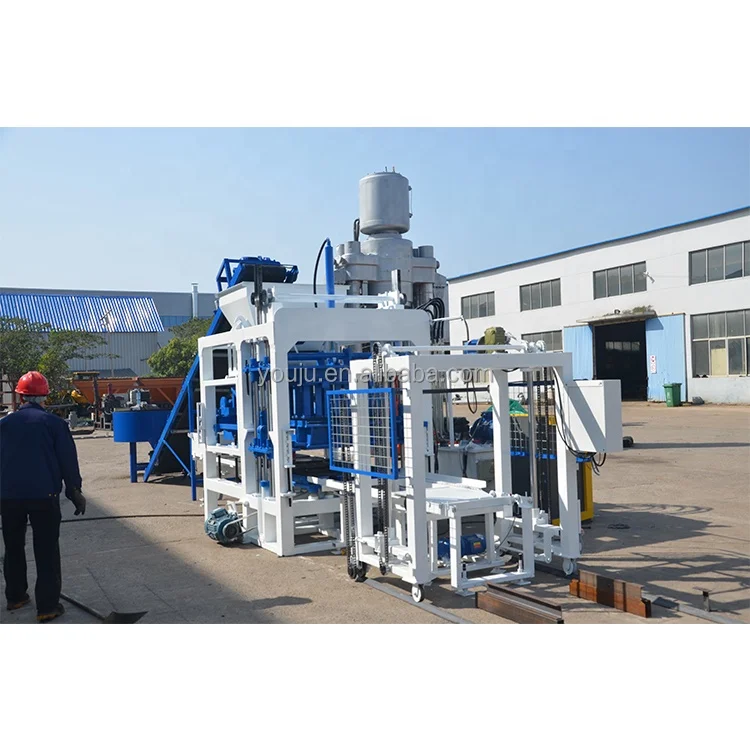
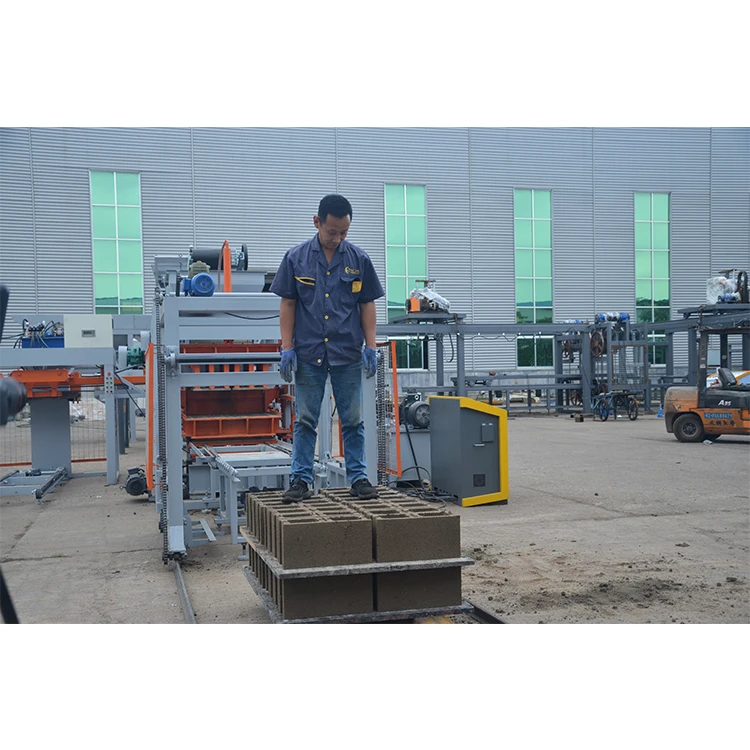
Configurable Automation Level — The QT6-15 block making machine is designed with a scalable automation architecture, allowing buyers to begin with a semi-automatic simple line and advance to full pallet loading, stacking, and cubing without replacing the press.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT6-15 |
| Product Type | Automatic Hydraulic Block Making Machine |
| Molding Way | Vibration and hydraulic pressing |
| Rated Pressure | 21 MPa |
| Molding Cycle | 15s–20s |
| Pallet Size | 900×700 mm |
| Main Machine Weight | 6000 kg |
| Output Capacity (Hollow Block) | 1440 pcs/h, 11520 pcs/8h (basis: 400×200×200 mm, 6 pcs/pallet) |
| Output Capacity (Paving Brick) | 5040 pcs/h, 40320 pcs/8h (basis: 200×100×60 mm, 21 pcs/pallet) |
| Output Capacity (Solid Brick) | 7680 pcs/h, 61440 pcs/8h (basis: 240×115×53 mm, 32 pcs/pallet) |
| Raw Materials | Cement, sand, fly ash, stone powder, slag |
| Control System | PLC (language and voltage configurable per buyer) |
| Automation Options | Simple line (JS500 mixer, 8m belt, stacker) or full automatic line (silo, batching, pallet loader, separator) |
| Warranty | 1 year (excluding wearing parts) |
Application Suitability
| Application | Material or Output |
|---|---|
| Building Construction | Hollow blocks from cement and crushed stone aggregates |
| Hardscaping & Sidewalks | Paving bricks and interlocking pavers using stone powder and sand |
| Infrastructure & Roads | Curbstones and solid bricks from high-strength concrete mixes |
| Fly Ash Utilization | Solid and hollow formats incorporating industrial fly ash or slag |
Why "Cycles Per Hour" is a Dangerous Metric for the automatic QT6-15 block making machine PLC controlled
Capacity is meaningless without stating the exact block format and pallet configuration used for the calculation.
Many buyers receive quotations boasting high hourly cycles, only to realize the machine was tested on a small solid brick format. When they switch to the large hollow blocks their market actually demands, the daily output drops significantly. I always insist on seeing the capacity calculation sheet that matches your specific target block dimensions and local raw material density before we lock in the vibration settings [NEED_CITE: block machine capacity calculation standards].
PLC Logic and Batching Consistency
The control system on this press handles more than just starting and stopping the motor. It manages the batching accuracy and the vibration duration for each specific mould installed. When you run a porous brick mix, the PLC adjusts the pressure and vibration time differently than it would for a dense paving stone. This batch-to-batch consistency is what removes the guesswork from the operator’s daily routine.
Mould Change and Format Flexibility
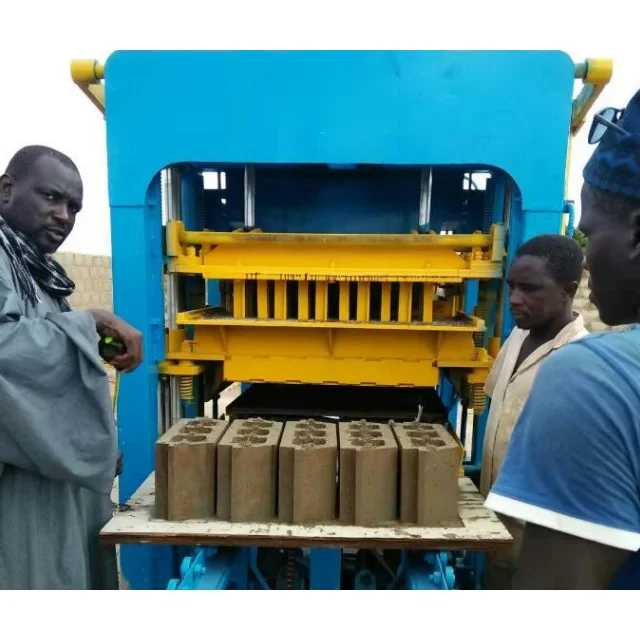
A single press can produce hollow blocks, interlocking pavers, and curbstones, but the speed of that transition defines your plant’s real flexibility. The QT6-15 automatic block making machine PLC controlled system supports various mould sizes within the 900×700 mm pallet envelope. The hydraulic clamping and vibration table are calibrated to the specific weight and resonance of the installed mould, ensuring that a switch from hollow blocks to solid bricks does not result in a shift of rejected, crumbled product [NEED_CITE: concrete block mould engineering and vibration force matching].
Vibration Force and Hydraulic Pressure Balance
The 21 MPa rated pressure works in tandem with the vibration table to compact the concrete mix. If the vibration is too high for a dry mix, the block surface tears; if the pressure is too low, the block lacks structural strength. This balance must be set according to your local aggregate—whether you use river sand, volcanic ash, or crushed granite. The hydraulic system allows for fine-tuning these parameters to match the specific friction and flow characteristics of your raw materials.
The Hidden Cost of Mismatched Pallets and Automation
I have seen plants where the press was excellent, but the pallet size was chosen without regarding the buyer’s existing curing racks or forklifts. This forces a manual re-stacking process that negates the investment in the automatic stacker. Furthermore, if the automation level is not matched to the plant’s labor availability, you end up with a bottleneck at the pallet return station. The simple line with a JS500 mixer is a good start, but the pallet feeding mechanism must be robust enough to handle the cycle times without stalling the main press [NEED_CITE: concrete block plant layout and pallet handling logistics].
Sourcing a Matched System Rather Than Isolated Parts
- Single Focus on Block Lines: We specify the machine, mould, pallet, and handling equipment as one matched system to ensure cycle times align across all stations.
- Mix Design Configuration: The vibration and pressure settings are calibrated against your actual local aggregate and mix design, not a generic catalogue default.
- Scalable Automation Path: You can start with a semi-automatic setup and upgrade to full automatic stacking and cubing using the same press foundation.
- Local Voltage and Language: The PLC display language and motor voltage are confirmed and built to your local grid specifications before assembly.
- Mould Engineering Support: We provide custom mould design and supply based on the specific formats your local construction market requires.
Documentation & Verification
- Line layout showing capacity calculations for your specific hollow block and paving brick formats.
- Hydraulic and electrical schematics matching the installed PLC and valve configuration.
- Factory test record using a mix design similar to your local raw materials.
- Mould drawing and format list with estimated changeover procedures.
- Voltage and control language confirmation sheet signed before production.
Installation, Commissioning & Support
- Top cylinder removed for container loading; reassembled and aligned on your foundation.
- PLC parameters set to your local voltage and frequency during the first power-on.
- Operator training on mould change procedures and vibration force adjustments.
- Wear parts list provided for hydraulic seals and vibration table components.
- Maintenance schedule based on the 21 MPa hydraulic system operating cycles.
Sizing the Line to Your Site and Grid
To provide a realistic proposal, we need to know your target block formats and the specific daily volume you intend to sell. Please share your local voltage and frequency, as well as the type of aggregate you have available for the mix. If you have an existing curing area or specific forklift dimensions, include those so we can select the correct pallet size and stacking height for the automatic QT6-15 block making machine PLC controlled system.
Frequently Asked Questions
Q: How is the output capacity verified and what block format does each figure assume?
A: Every capacity figure we quote is linked to a specific block dimension and pallet count. For example, the hollow block output is based on 400×200×200 mm blocks at 6 pieces per pallet. We provide a capacity calculation sheet that shows the theoretical and realistic daily output for the exact formats you plan to produce.
Q: How do I choose between the semi-automatic simple line and the full automatic line?
A: The choice depends on your labor availability and curing space. The simple line uses a JS500 mixer and an 8m conveyor, which is suitable for smaller sites. The full automatic line adds batching machines and pallet loaders to reduce manual handling and increase consistency for larger daily volumes.
Q: What voltage, frequency, and PLC language options are available for my country?
A: The control system and motors are configurable. We confirm your local industrial voltage and frequency before production begins. The PLC interface language can also be set to match your operators’ preference to ensure accurate monitoring of the batching and molding cycles.
Q: How long does a mould change take, and what formats can one press produce?
A: The press supports any format that fits the 900×700 mm pallet, including hollow blocks, pavers, and curbstones. Mould change time depends on the specific clamping system and the operator’s familiarity with the procedure, which we cover during the on-site commissioning and training phase.
Q: What is the upgrade path if I start semi-automatic and want full automation later?
A: The press is designed to accept automatic pallet feeders and stackers as add-on stations. You can start with a manual or simple line configuration and later install the automatic handling equipment without needing to replace the main vibration table or hydraulic press unit.