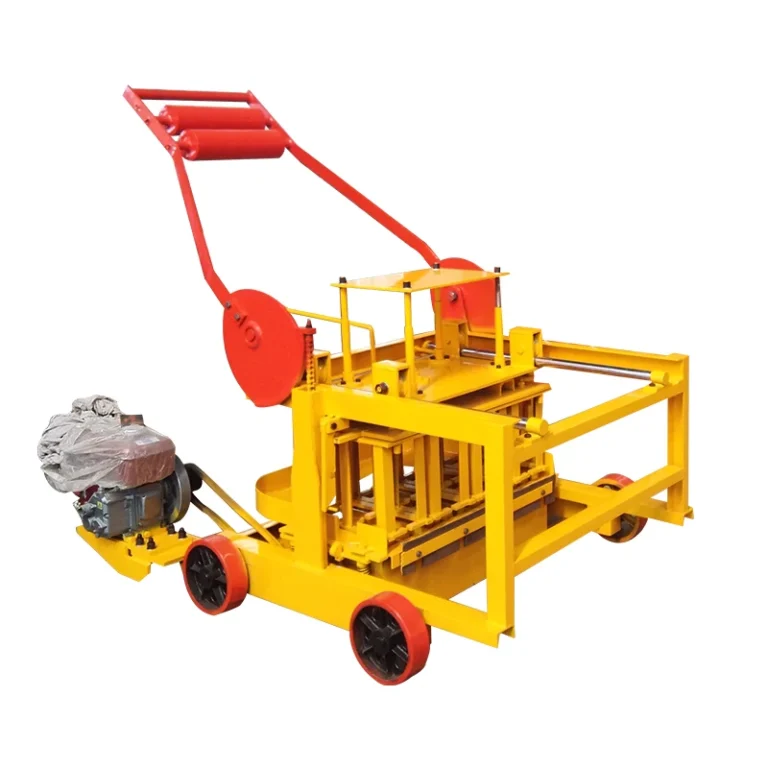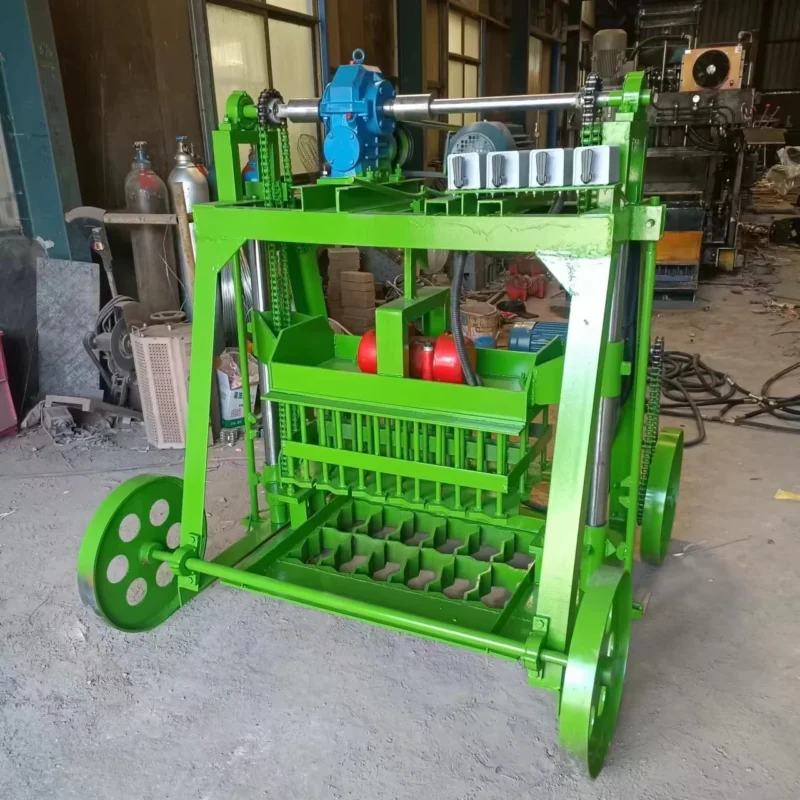
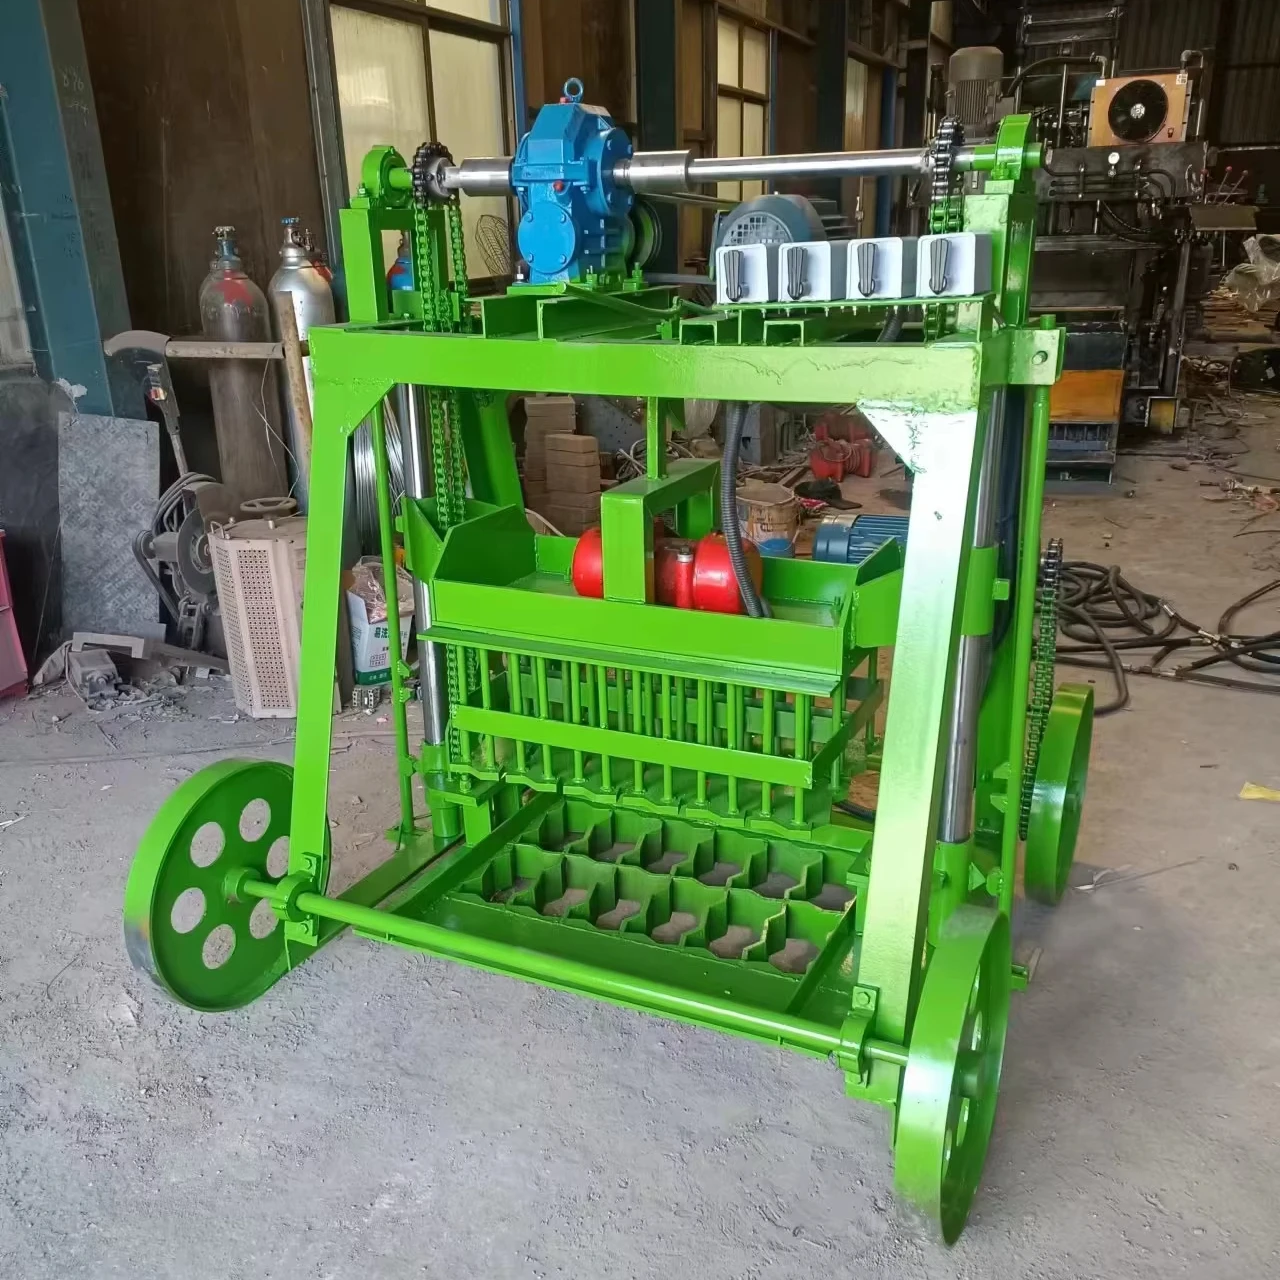
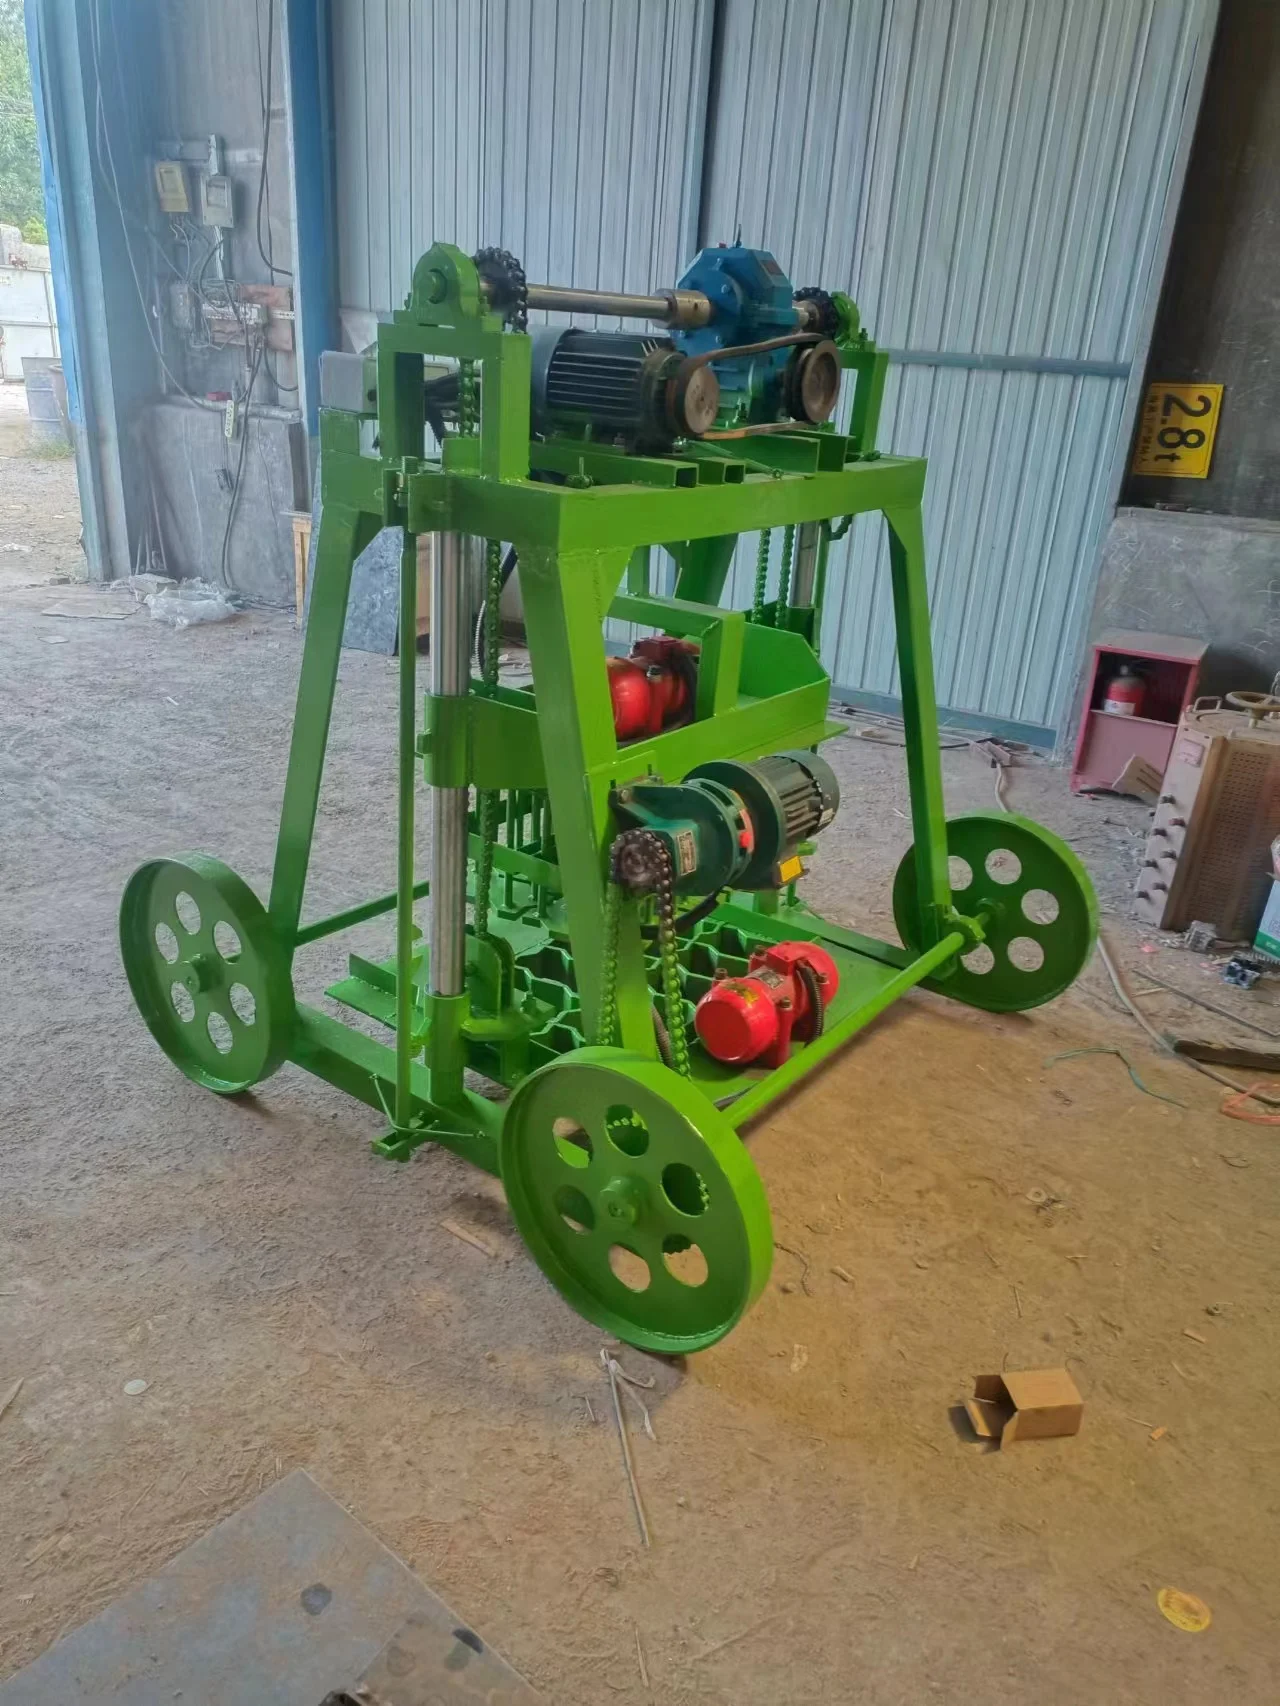
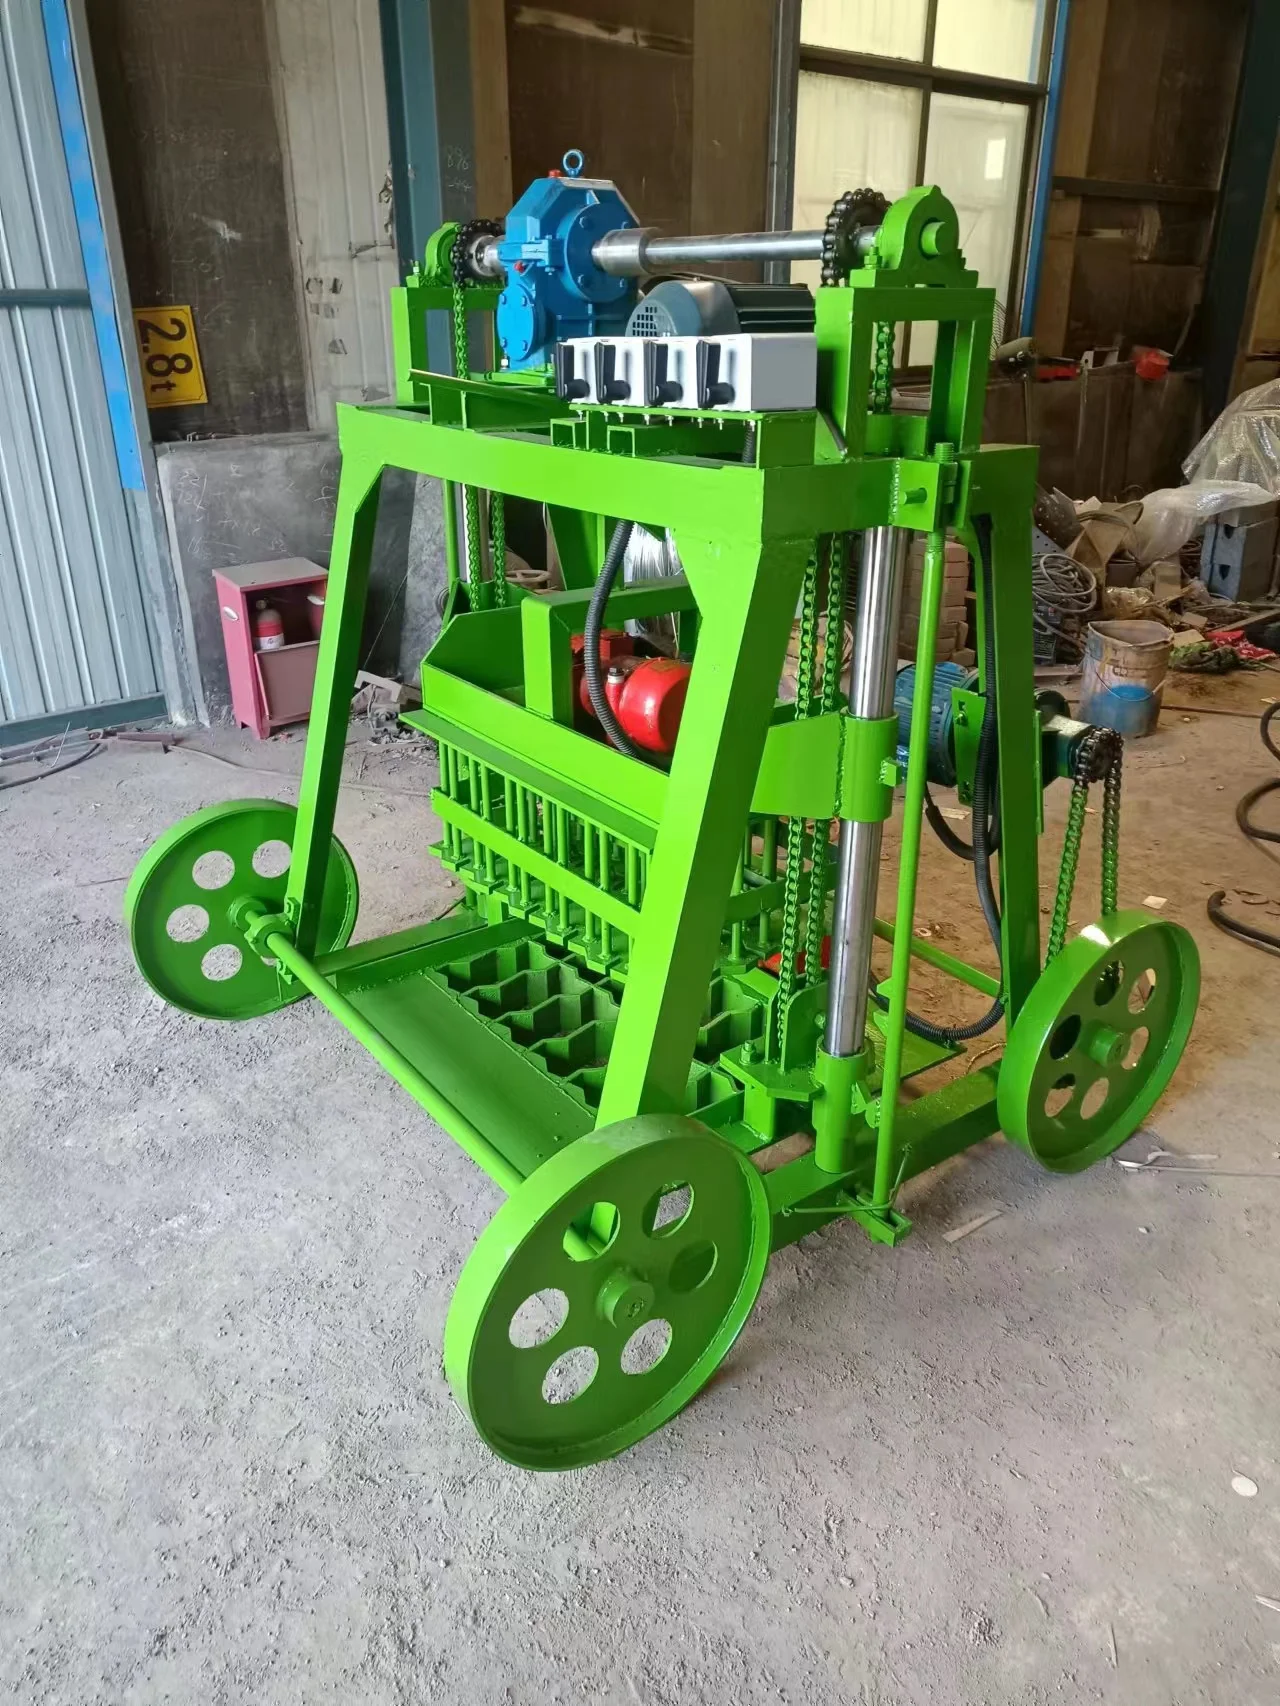
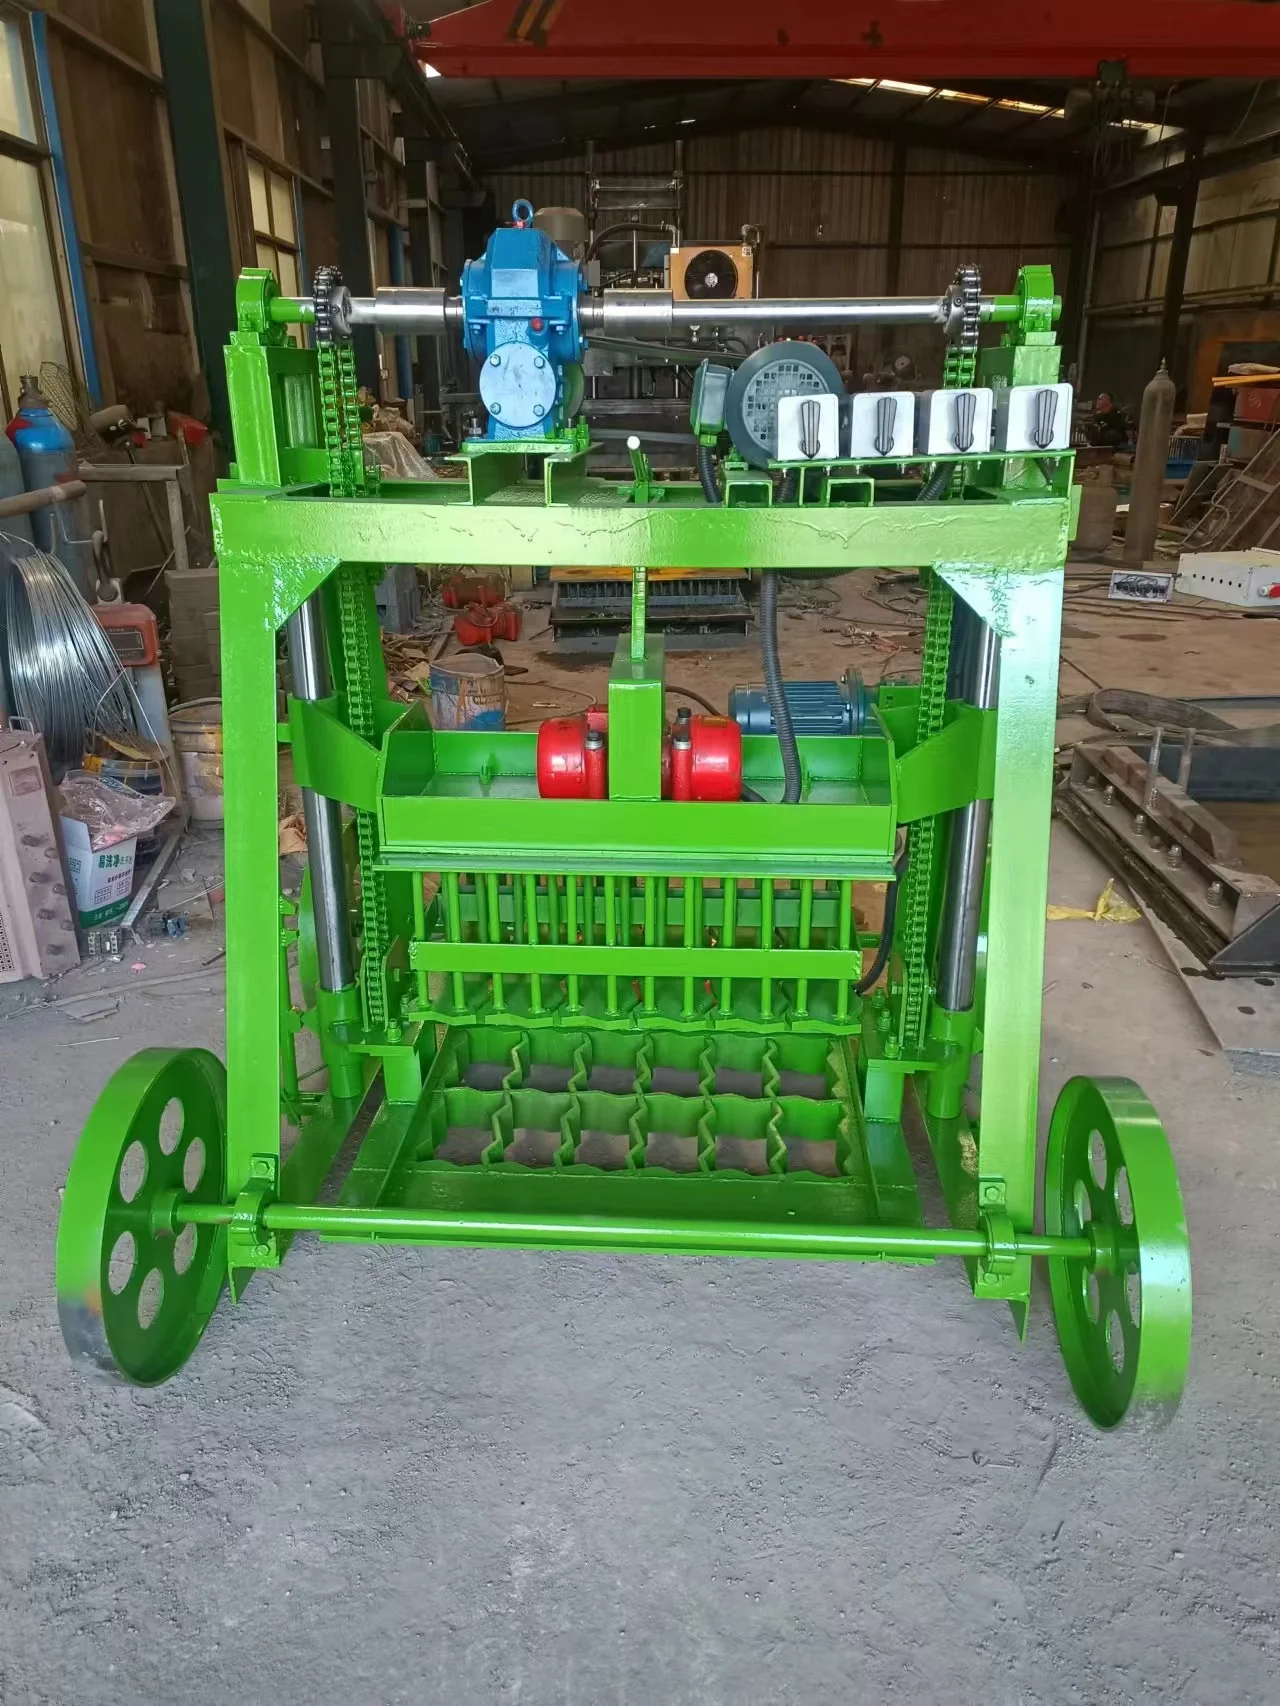
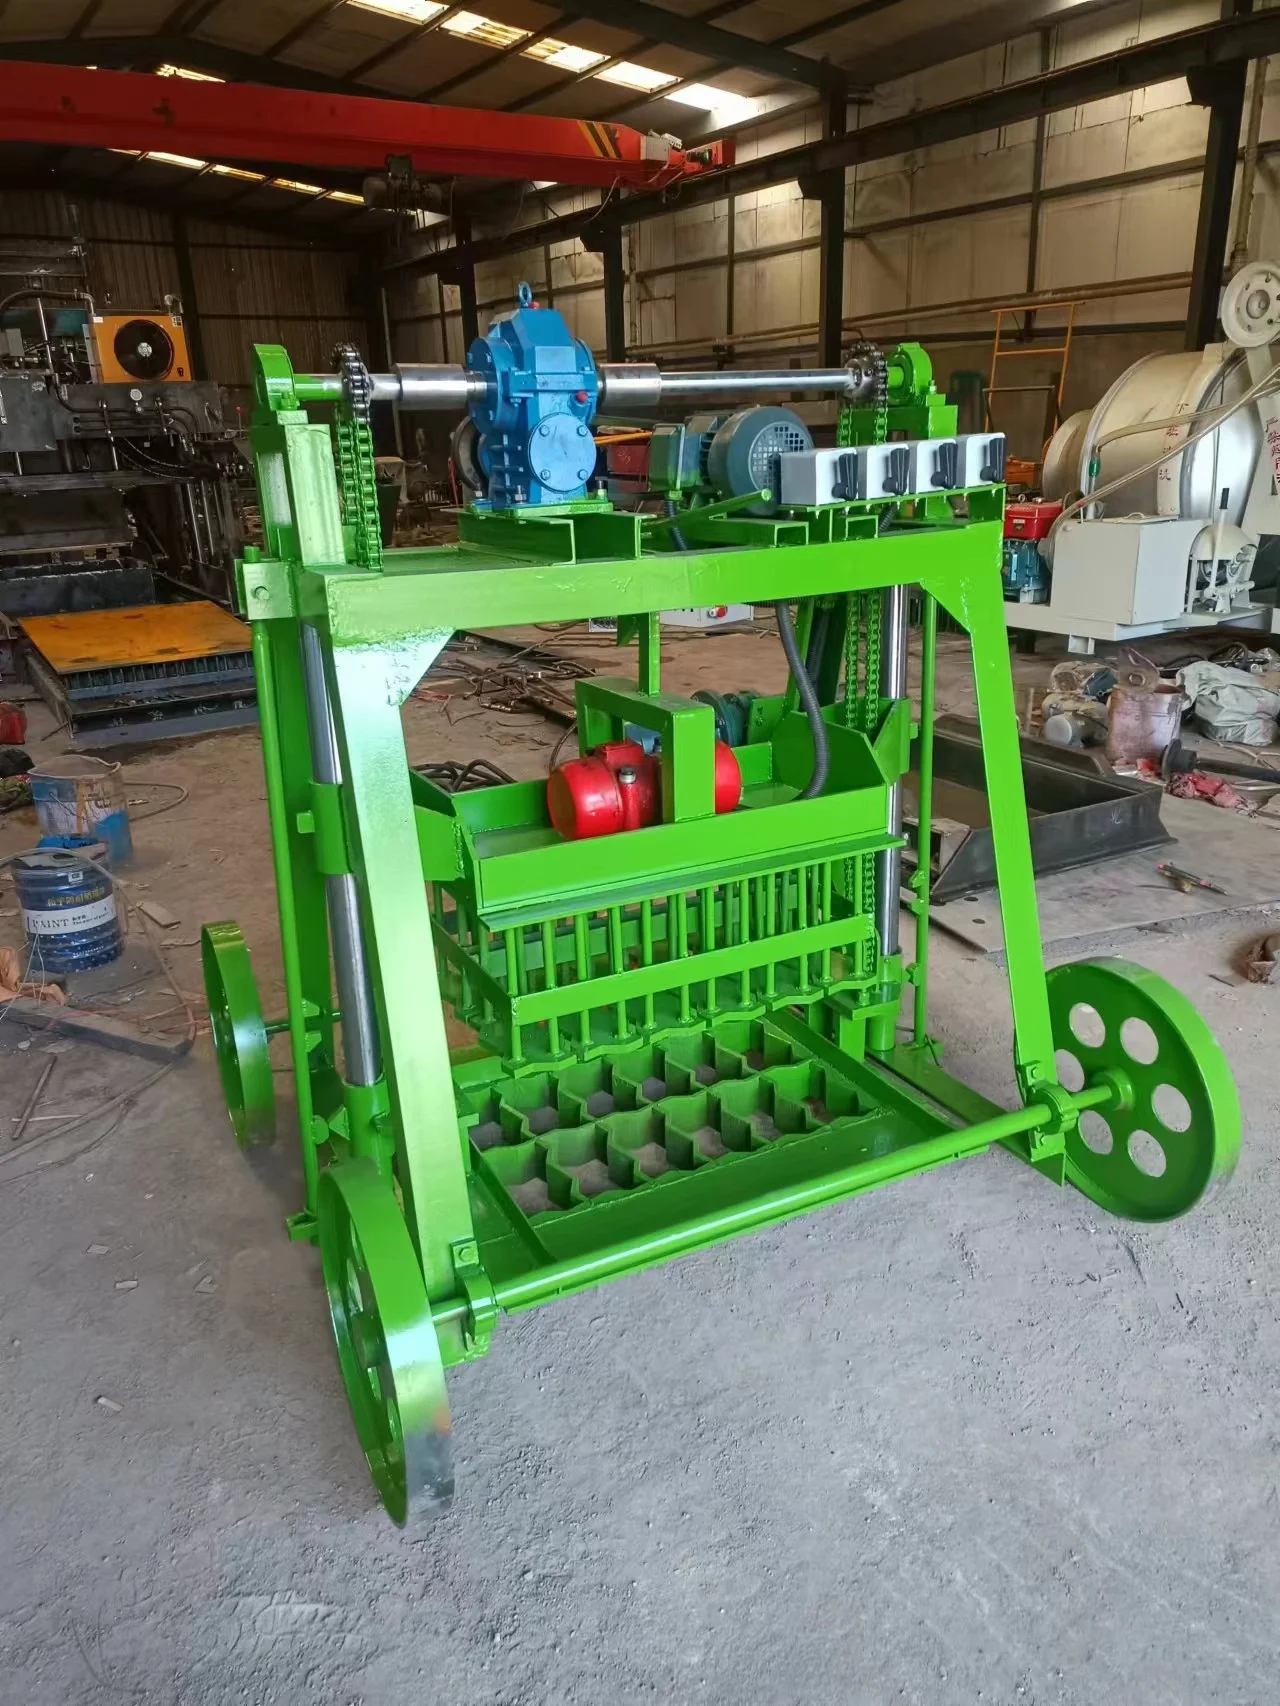
Description
Configuration set against the buyer’s actual mix design, local aggregate and target block format — QMJ4-45 parameters are validated against your specific raw material samples before the machine leaves the factory, ensuring the vibration force matches what your site actually uses.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QMJ4-45 |
| Product Type | Egg Laying Block Making Machine |
| Molding Capacity | 4 pcs/mould for 400×200×200 mm block (basis to be confirmed for other formats) |
| Vibration Frequency | 2400 r/m |
| Daily Productivity | 2600-4000 pcs/day (basis to be confirmed) |
| Vibration Method | Mold vibration |
| Demold Method | Manual |
| Total Power | 6 kW |
| Power Source | Diesel / Petrol engine |
| Molding Cycle | 45 s |
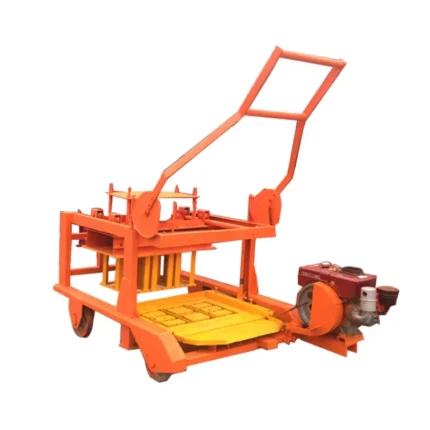
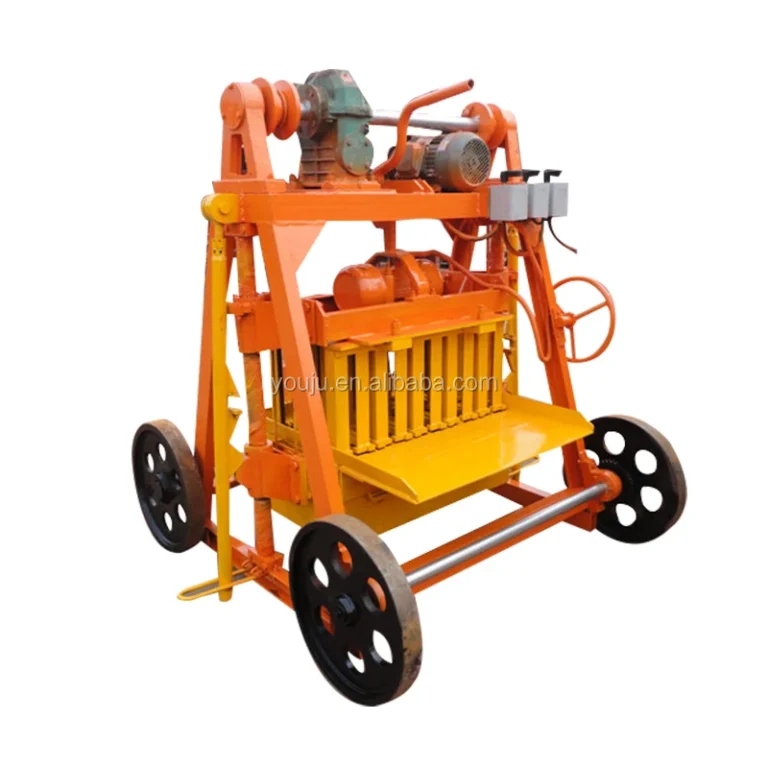
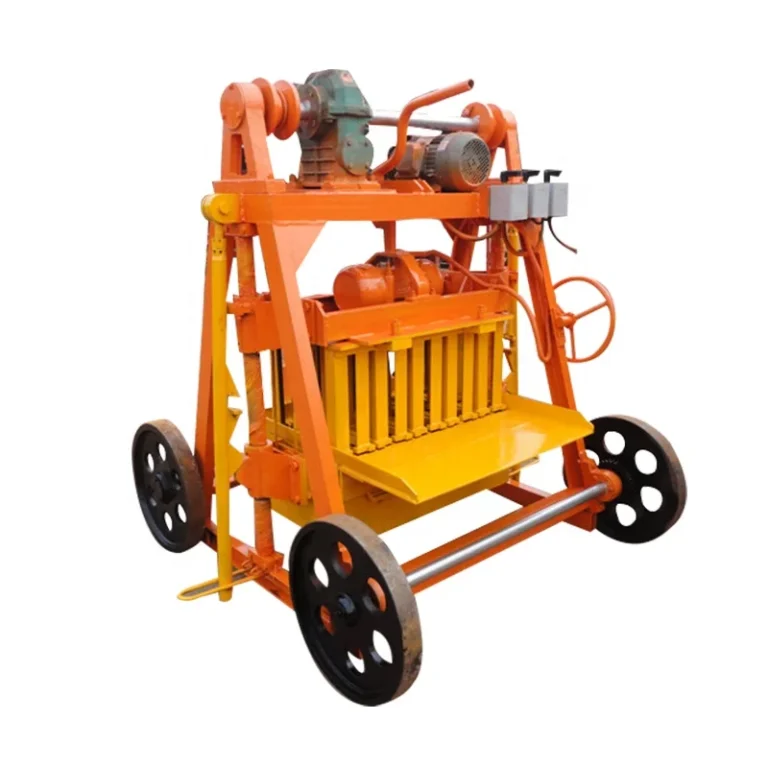
| Automation Level | Manual (egg-laying / mobile) |
| Pallet Requirement | Not required (blocks laid directly on ground) |
| Warranty | 1 year |
Application Suitability
| Application | Material or Output |
|---|---|
| On-site hollow block production without a fixed plant | Standard cement, sand and aggregate mixes |
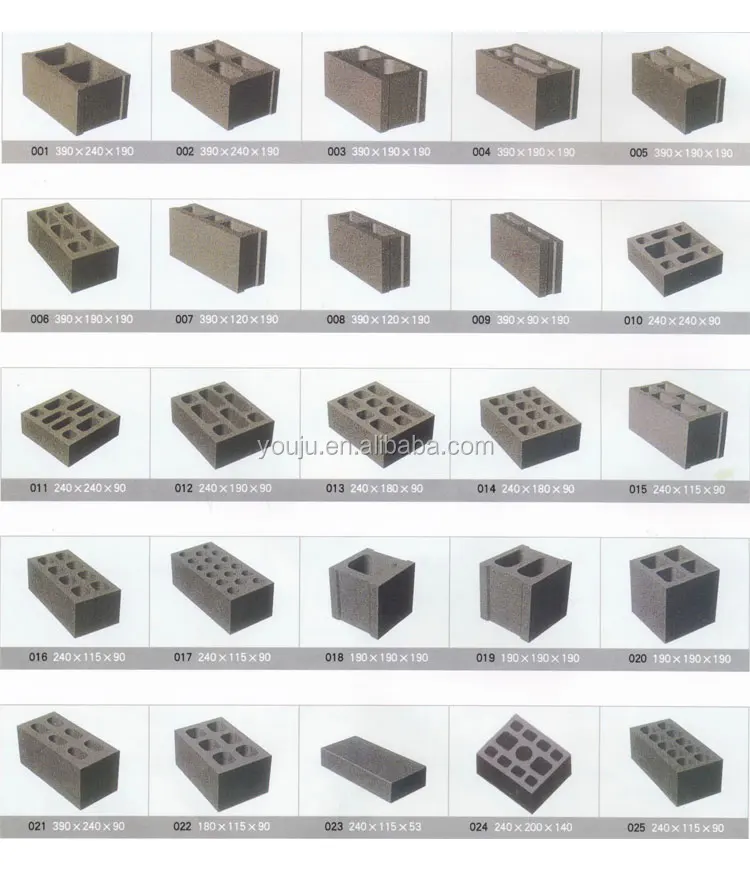
| Small-scale block production for construction contractors | 400×200×200 mm, 400×150×200 mm, 400×120×200 mm hollow blocks |
| Remote or off-grid housing project sites | Engine-powered operation where grid electricity is unavailable |
| First block plant for entrepreneurs | Low initial investment with upgrade path to PLC-controlled mobile block machine |
What Your Local Aggregate Does to a 45-Second Cycle
The cycle time on the label means nothing until the vibration force is matched to the stone you can actually buy.
I learned this the hard way. We shipped an egg laying block making machine to a site where the local aggregate was volcanic rock instead of the standard river sand we tested with. The blocks came out crumbling because the vibration frequency was not calibrated for that material’s density and friction. Now every configuration starts with a sample of the buyer’s actual raw material. The 2400 r/m vibration frequency on the QMJ4-45 is a baseline; the real question is whether that frequency delivers enough force through your specific mix to produce a block that survives handling and curing [NEED_CITE: effect of aggregate type on vibration requirements].
What the Operator Actually Does During a Shift
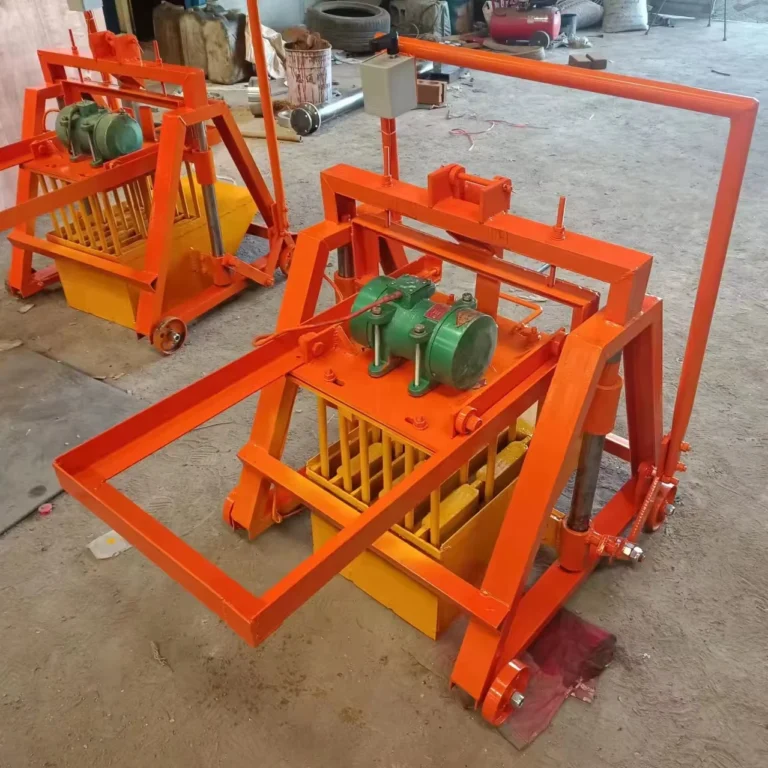
The QMJ4-45 is a manual egg-laying unit. The operator feeds the mix, triggers the mold vibration, and moves the machine forward to lay the next block directly on the ground. There is no pallet feeding system and no stacking mechanism. This keeps the initial investment low and removes two consumable costs from the daily operation. An automatic egg laying block making machine removes more steps; this model leaves the operator in control of pace and positioning.
Where the Upgrade Path Begins
When daily volume grows, the manual cycle becomes the bottleneck — not because the press is slow, but because the operator cannot maintain consistent timing across an eight-hour shift. A PLC-controlled mobile block machine replaces the operator’s judgment with fixed intervals for vibration duration and feed volume. The QMJ4-45 sits at the starting point of that progression, and the automation level is selectable so a buyer can begin here and move toward semi-automatic control when the market demands it [NEED_CITE: automation upgrade paths for mobile block machines].
Vibration Force, Molding Cycle and What They Mean Together
The 2400 r/m vibration frequency and 45-second molding cycle together determine block density. In an egg-laying machine, vibration must be strong enough to consolidate the mix while the block is still supported by the mold, because once the machine moves forward, the block has only its own green strength to hold shape. The twice-vibration molding core in this unit delivers consolidation in two passes rather than one, which produces more even density through the block height. For a 400×200×200 mm hollow block, the stated cycle yields 4 pieces per mold at approximately 3000 pieces over an 8-hour shift. For the smaller 400×120×200 mm format, the mold holds 6 pieces and daily output reaches approximately 4500 pieces over the same 8-hour period. These figures assume continuous operation with a prepared mix and clear ground for laying.
When the Wrong Power Source Costs You a Week
Specifying a diesel engine for a site that already has stable three-phase power means carrying fuel costs and engine maintenance indefinitely. Specifying an electric motor for a remote site with no grid connection means the machine sits idle until a generator arrives. The QMJ4-45 is available with diesel or petrol engine power, but an electric motor variant may be configured if the buyer confirms voltage, frequency and control language before production begins. Getting this wrong after the machine arrives delays commissioning by weeks [NEED_CITE: voltage and frequency confirmation before export].
Why This Machine Is Configured Before It Is Quoted
Block machinery is our single focus, so the QMJ4-45 is specified as one matched system — mold, vibration setting and power source — rather than assembled from catalog defaults. Configuration is set against the buyer’s actual mix design and local aggregate, not a standard test material. Molds are designed for the hollow block formats the buyer’s market actually sells, including custom drawings where needed. Installation and commissioning support includes operator training on the specific mix and cycle routine. Every specification is documented before the order is placed, so there are no surprises at the factory gate.
Documentation & Verification
- Capacity calculation stating the exact hollow block format assumed for the 45-second cycle
- Mould drawing and format list for every hollow block size in your order
- Voltage and control language confirmation sheet when electric motor variant is selected
- Factory test record using your submitted raw material sample before dispatch
- Operation and maintenance manual with wear parts and mould replacement schedule
- Packing photographs and customs documentation support for your shipping agent
Installation, Commissioning & Support
- Ground must be level and cured concrete; the QMJ4-45 lays blocks directly on the surface with no pallet system
- Diesel engine variant requires fuel supply and basic engine maintenance tools on site
- First commissioning includes vibration force adjustment to match your confirmed mix design and aggregate type
- Operator training covers mold change procedure, cycle timing and manual demold technique
- Wear parts list provided with lead times for first replacement order of vibration components and mold liners
- Daily maintenance routine centered on mold cleaning and engine oil level for engine-powered units
What We Need From You to Build the Right Configuration
Send us the hollow block formats your market sells, the daily volume you need to hit, and a sample of the aggregate you can source locally. Tell us whether your site has grid electricity or if engine power is required, and confirm the voltage and frequency if electric. If you have existing curing space or a forklift on site, share those dimensions so we can confirm the laying pattern will fit your operation.
Frequently Asked Questions
Q: How is daily output calculated and which block format does each figure assume?
A: Daily output is calculated from the 45-second molding cycle multiplied by the number of pieces per mold and the number of working hours. For the 400×200×200 mm hollow block, the mold holds 4 pieces and output is approximately 3000 pieces over 8 hours. For the 400×120×200 mm format, the mold holds 6 pieces and output reaches approximately 4500 pieces. All figures assume continuous operation with prepared mix.
Q: Can the QMJ4-45 be upgraded from manual to semi-automatic or PLC-controlled operation?
A: The automation level is selectable. A buyer can start with the manual egg-laying configuration and later move toward semi-automatic control as production volume grows. A PLC-controlled mobile block machine replaces manual timing with fixed intervals for vibration and feed, improving batch-to-batch consistency and reducing operator fatigue over long shifts.
Q: What voltage and control language options are available if an electric motor variant is chosen?
A: Voltage and frequency are configurable based on your site’s electrical supply. The PLC display language is confirmed before production begins so operators can read instructions in their working language at first commissioning. These details must be locked in before the machine enters production to avoid delays after arrival.
Q: How long does a mould change take and what tools are required on site?
A: Mould change on the QMJ4-45 is manual and requires basic hand tools. The exact time depends on operator familiarity and the specific format being installed. We provide a mould drawing and format list with each order so your team can practice the procedure and confirm it fits within your shift schedule before committing to format switches during production.