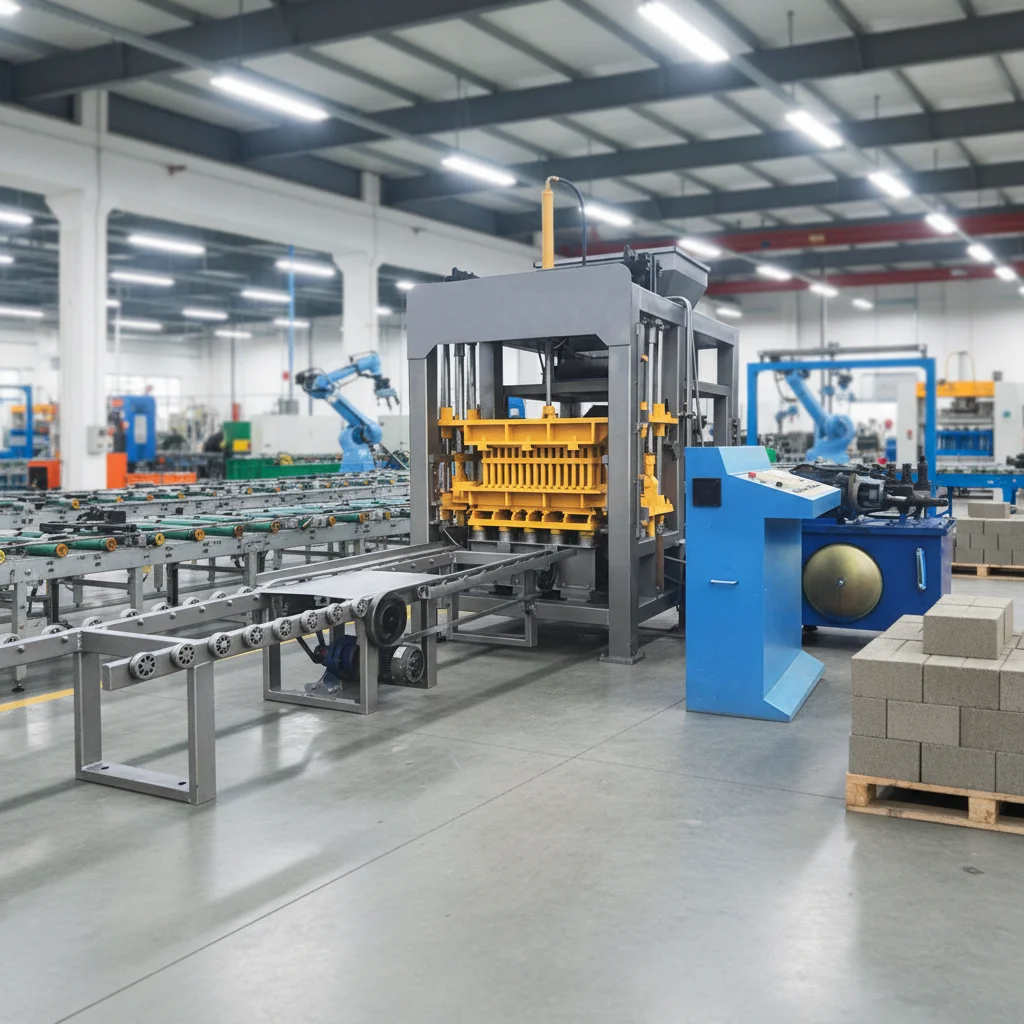
Description
Intelligent Press Control — the QT10-15 holds vibration and hydraulic parameters constant across every cycle through PLC automation, eliminating the operator timing drift that causes strength variation on manual lines.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT10-15 |
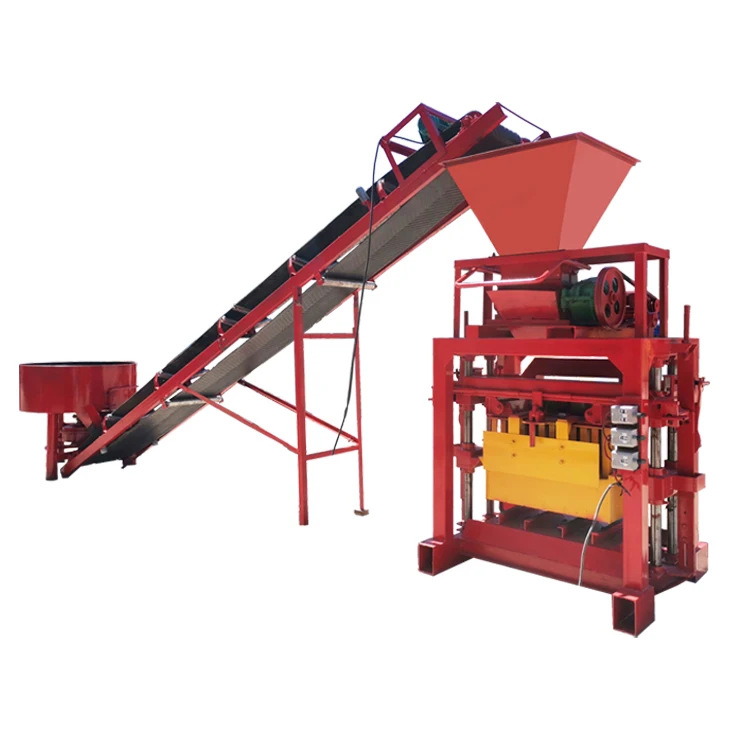
| Product Type | Automatic Cement Block Making Machine |
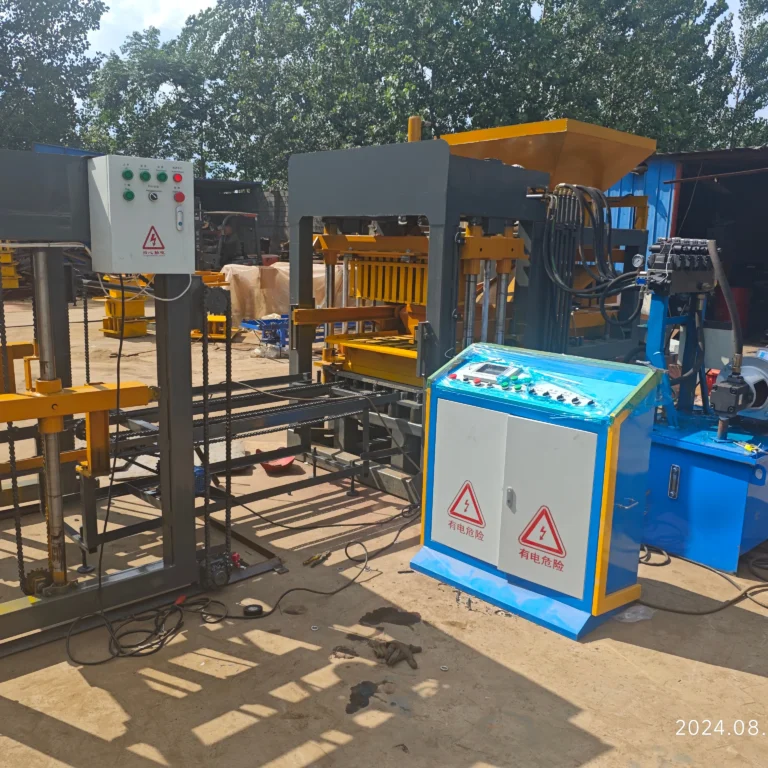
| Control System | PLC control cabinet |
| Hydraulic System | Independent integrated hydraulic station |
| Vibration Mode | Vertical station mode resonance, automatic FM-AM |
| Automation Level | Automatic |
| Mould Change | Simple mould replacement for format adjustment |
| Cycle Time (400×200×200 mm hollow block, 10 pcs/mould) | 15–20 s |
| Output (400×200×200 mm hollow block) | 1800–2400 pcs/hour; 14400–19200 pcs/8 hr shift |
| Cycle Time (400×150×200 mm hollow block, 12 pcs/mould) | 15–20 s |
| Output (400×150×200 mm hollow block) | 2160–2880 pcs/hour; 17280–23040 pcs/8 hr shift |
| Cycle Time (240×115×53 mm solid brick, 62 pcs/mould) | 15–20 s |
| Output (240×115×53 mm solid brick) | 8928–11160 pcs/hour; 71424–89280 pcs/8 hr shift |
| Cycle Time (200×100×60 mm paving block, 27 pcs/mould) | 20–25 s |
| Output (200×100×60 mm paving block) | 5184–6480 pcs/hour; 41472–51840 pcs/8 hr shift |
| Cycle Time (225×112.5×60 mm paving block, 24 pcs/mould) | 20–25 s |
| Output (225×112.5×60 mm paving block) | 4032–5040 pcs/hour; 32256–40320 pcs/8 hr shift |
| Warranty | 1 year for the whole machine (excluding spare parts) |
| Voltage & Frequency | (basis not stated in source — confirm with supplier for target market) |
| Overall Dimensions | (basis not stated in source — verify against manufacturer catalog) |
| Net Weight | (basis not stated in source — verify against manufacturer catalog) |
| Hydraulic Pressure | (basis not stated in source — verify against manufacturer catalog) |
| Vibration Force | (basis not stated in source — verify against manufacturer catalog) |
| Pallet Size | (basis not stated in source — verify against manufacturer catalog) |
| Mould Change Time | (basis not stated in source — verify against manufacturer catalog) |
| PLC Display Language | (basis not stated in source — confirm available languages) |
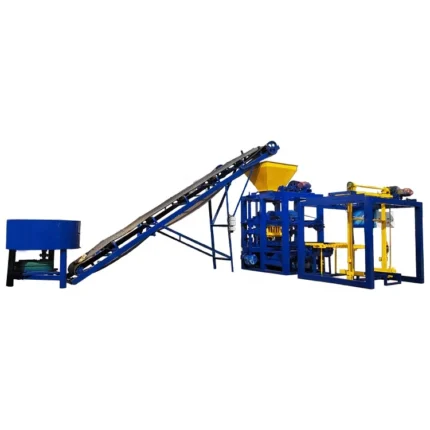
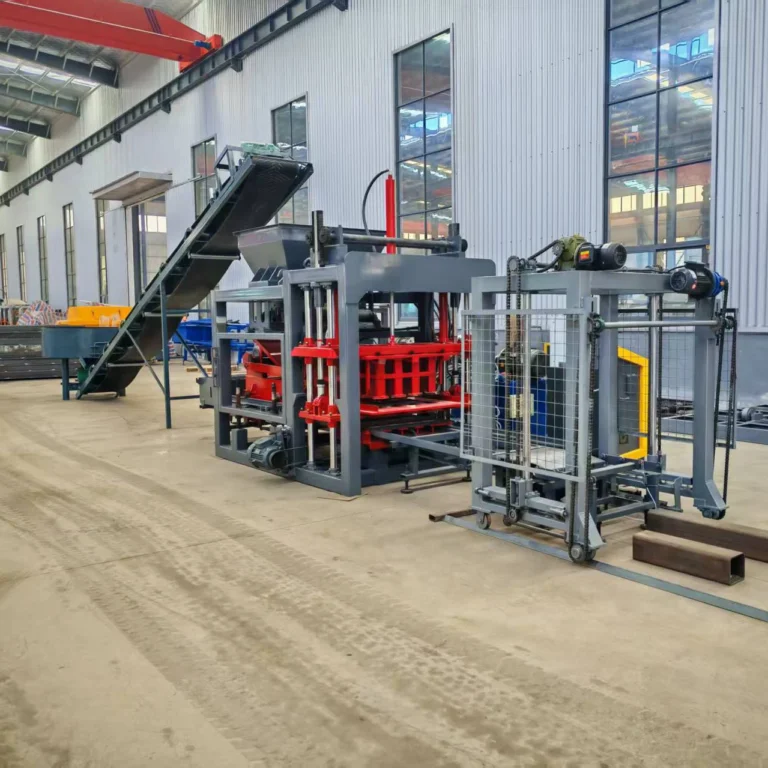
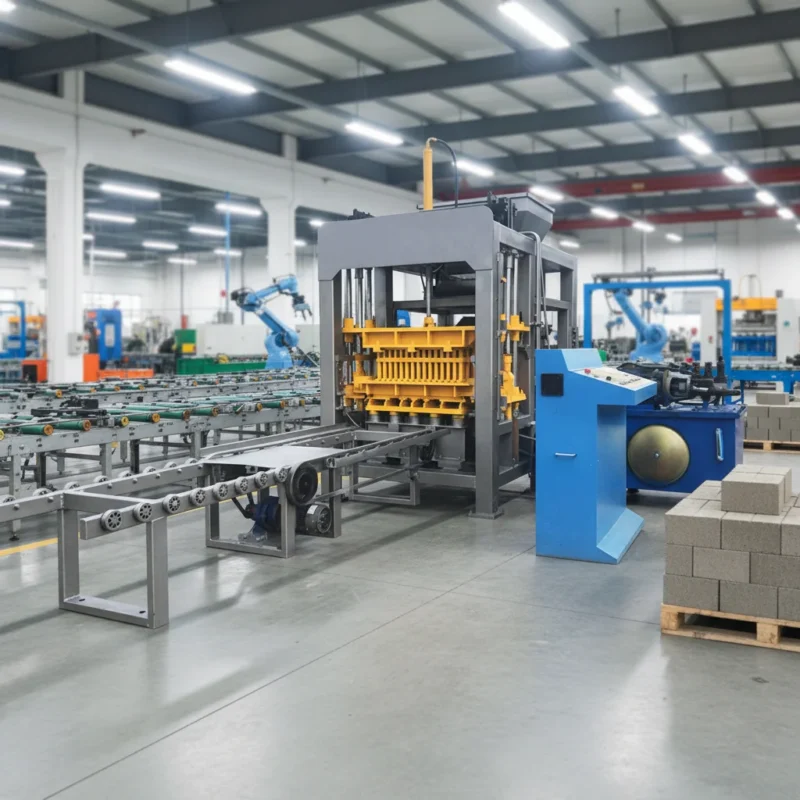
| Key Features | Pallet feed machine, storage hopper, conveyor, hydraulic unit, PLC control cabinet |
Application Suitability
| Application | Material or Output |
|---|---|
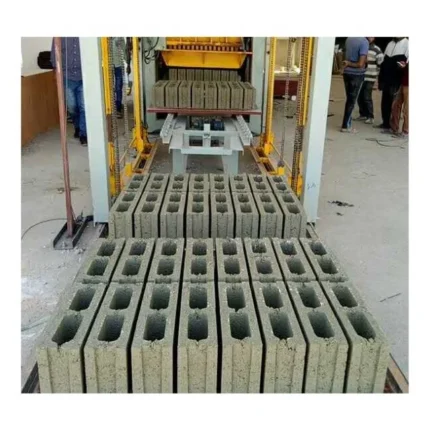
| Hollow block production | Cement, sand, crushed stone or local aggregate blends |
| Multicellular brick production | Lightweight and standard concrete mixes |
| Paving brick production | High-density concrete with fine aggregate |
| Standard solid brick production | Cement and graded aggregate for structural use |
Why PLC Control Changes the Block Consistency Conversation
A quoted cycle time means nothing when the operator shortens the vibration window to clear a pallet jam — the QT10-15’s PLC control cabinet governs every press parameter so the operator cannot drift outside the recipe.
In my years fitting out lines in Latin America, the most expensive problem was never the machine itself. It was the quiet variation that crept in shift by shift: a slightly shorter press, a slightly different feed, blocks that passed visual inspection but failed crush tests weeks later. An automatic cement block making machine PLC controlled removes that variable. The recipe is locked, the sequence is enforced, and every pallet that leaves the press has seen the same vibration profile and hydraulic pressure as the one before it [NEED_CITE: concrete block compressive strength testing standards].
What the PLC Actually Governs on the Press Floor
The programmable logic controller in the QT10-15 coordinates pallet feeding, material delivery from the storage hopper, vibration timing, and hydraulic pressing as a single continuous sequence. An operator monitors the automatic cement block making machine PLC controlled interface rather than triggering each step manually, which removes the timing inconsistencies that semi-automatic lines accept as normal.
Batch-to-Batch Consistency Without Operator Judgment
Once a recipe is stored — vibration duration, pressure hold time, feed volume — the PLC reproduces it identically on the ten-thousandth cycle. This matters when a plant runs hollow blocks in the morning and switches to pavers after lunch. The independent integrated hydraulic station sits apart from the main vibration zone, keeping pressure stable even during extended shifts [NEED_CITE: hydraulic system isolation in vibration-heavy equipment]. The vertical station mode resonance with automatic FM-AM further supports consistency by self-adjusting vibration frequency and amplitude, so different block formats compact properly without manual recalibration between runs.
Reading the Specs That Decide Your Line’s Real Output
Hydraulic pressure and vibration force together determine the density and strength of every block that leaves the mould. The QT10-15’s independent hydraulic station is specified separately from the host frame, which helps maintain pressure integrity over long production runs. Cycle time varies by format: 15–20 seconds for hollow blocks and solid bricks, 20–25 seconds for paving blocks where higher compaction is required. The mould cavity count directly multiplies output — 10 cavities for 400×200×200 mm hollow blocks, 62 for standard solid bricks — so capacity planning must start from the format the buyer actually sells. Pallet size, noted as requiring confirmation against the manufacturer catalog, must match both the press bed and the curing racks the buyer already operates. Mould change is designed as a simple replacement process, which matters for plants that serve multiple market segments from a single press line.
When the Wrong Configuration Follows You Home
I have watched a plant owner in Ecuador stand in front of a line that ran perfectly in the factory but produced weak blocks on local volcanic aggregate, because the vibration frequency had been set for a standard sand mix that did not exist in his region. Mismatched voltage and frequency can delay commissioning for weeks while transformers are sourced locally. A PLC display in the wrong language turns troubleshooting into a translation exercise every time an alarm triggers [NEED_CITE: voltage and frequency standards by export market]. These are not engineering failures — they are specification conversations that never happened before the machine shipped.
What Buying Here Actually Means
Block machinery is the single focus of Shandong Shiyue Intelligent Machinery, so the QT10-15 is specified as a matched system — press, mould, pallet, and handling — rather than assembled from separate suppliers. Machine configuration is set against the buyer’s actual mix design, local aggregate, and target block format instead of a catalog default. Mould design covers the formats the buyer’s market sells, with custom drawings available where standard moulds do not fit. The automation level is selectable, meaning a buyer can commission the QT10-15 as a semi-automatic line and add pallet stacking or cubing stations later without replacing the press. Installation support includes on-site commissioning and operator training so the PLC recipes are dialed in against local materials before the technical team leaves [NEED_CITE: CE machinery directive requirements for industrial equipment].
Documentation & Verification
- Line layout and capacity calculation stating the block format and cycle time assumed
- Machine specification sheet with confirmed voltage, frequency, and PLC display language
- Mould drawing and format list for every block type in the quotation
- Hydraulic and electrical schematic for the independent station and PLC cabinet
- Factory test record on the buyer’s target block format before dispatch
- Operation and maintenance manual with wear parts and mould replacement schedule
Installation, Commissioning & Support
- Foundation and floor space planning based on the QT10-15’s confirmed overall dimensions and pallet feed layout
- Dedicated electrical circuit sized to the confirmed voltage and frequency for the PLC cabinet and hydraulic station
- Machine dismantling for container shipment with reassembly sequencing at destination
- First-run commissioning with PLC recipe tuning against the buyer’s local aggregate and mix design
- Operator training covering PLC interface navigation, mould change procedure, and daily maintenance checkpoints
- Wear parts and mould supply list with reorder references for hydraulic seals and vibration components
What to Prepare Before You Send an Inquiry
A useful inquiry starts with the block formats your market actually buys, the daily volume you need per format, and the aggregate materials available locally. Confirm your site’s voltage and frequency, the PLC display language your operators will work with, and whether you need pallet feeding, stacking, and cubing included in the automatic scope or plan to add them later.
Frequently Asked Questions
Q: How does the PLC control ensure consistent block strength across batches?
A: The PLC governs vibration duration, hydraulic pressure hold time, and material feed volume for every cycle. Once a recipe is stored, it reproduces those parameters identically regardless of shift changes or operator rotation, which removes the manual timing drift that causes strength variation on semi-automatic lines.
Q: What automation level is included — does the line cover pallet feeding, stacking, and cubing?
A: The QT10-15 quotation scope should specify which stations are automated. The core press, pallet feed machine, and material delivery are PLC-governed. Stacking and cubing stations may be included or added separately depending on the buyer’s automation target and investment plan.
Q: Can the QT10-15 be upgraded from semi-automatic to fully automatic later?
A: The automation level is selectable at order and can be expanded afterward. A buyer can commission the press with semi-automatic pallet handling and add automatic stacking or cubing stations in a later phase without replacing the PLC cabinet or the press itself.
Q: What PLC display languages are available and how is voltage confirmed?
A: Available PLC display languages must be confirmed before production begins to avoid commissioning delays. Voltage and frequency are not stated as standard in the source data — the buyer must supply the target market’s electrical specifications so the motor and control cabinet are built to match.
Q: How does mould change work on an automated line?
A: The QT10-15 uses a simple mould replacement design that allows format switching without major press disassembly. Realistic changeover time should be confirmed with the supplier for the specific mould sizes in the buyer’s production plan, as it varies by format complexity and cavity count.