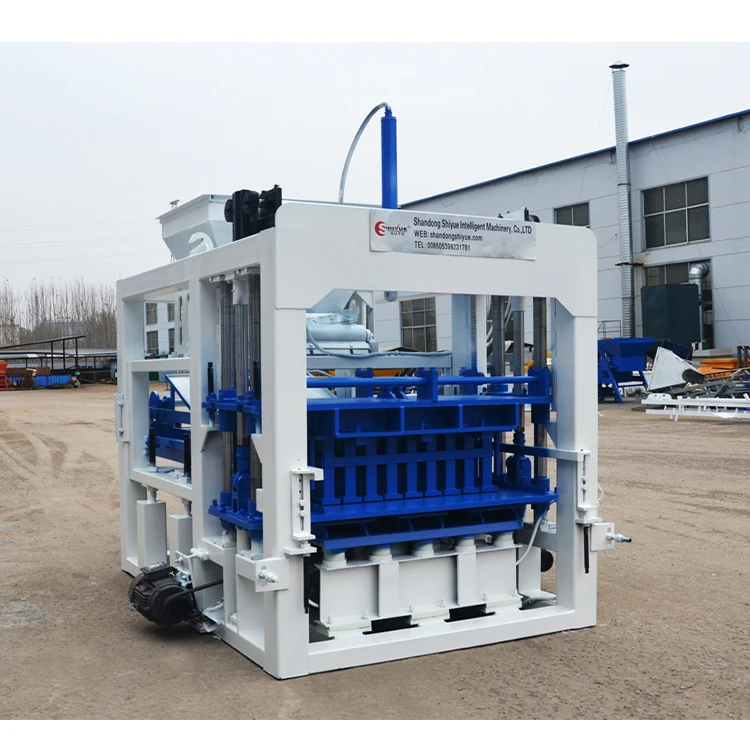

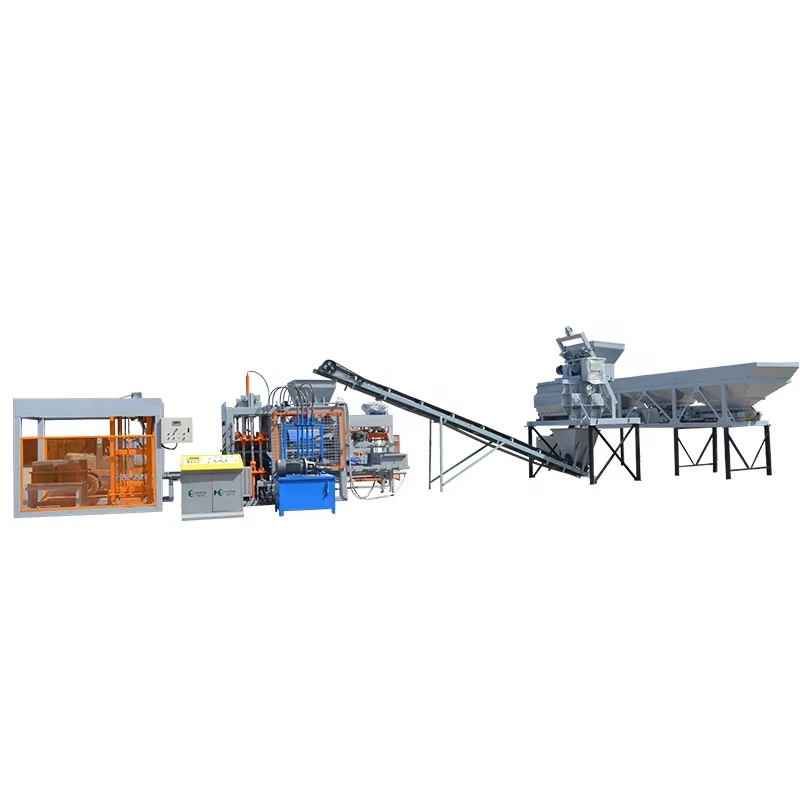


Description
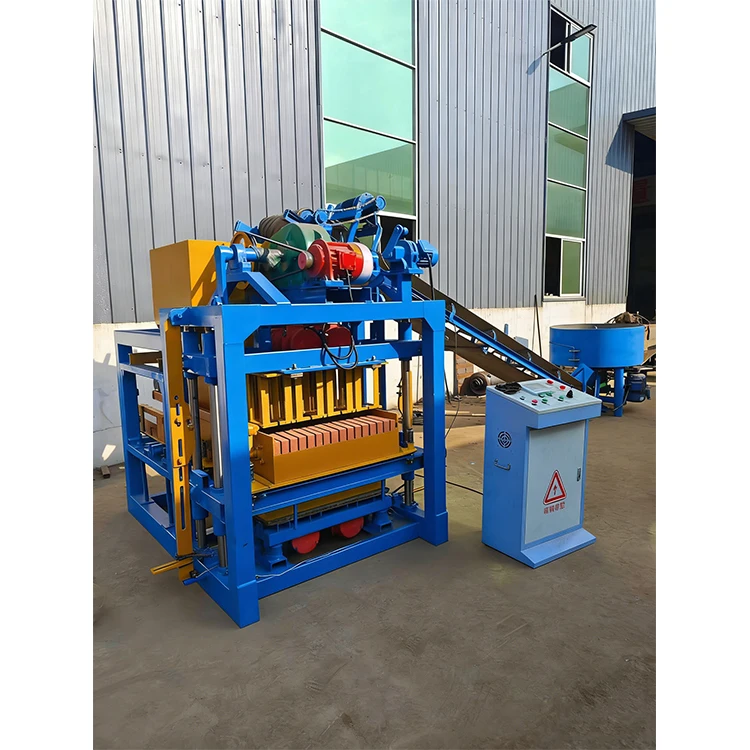
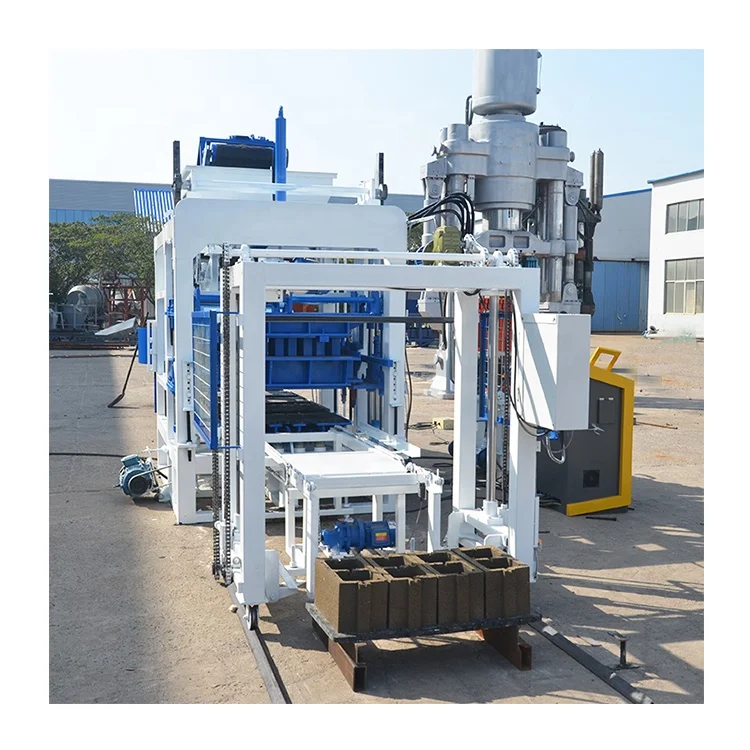
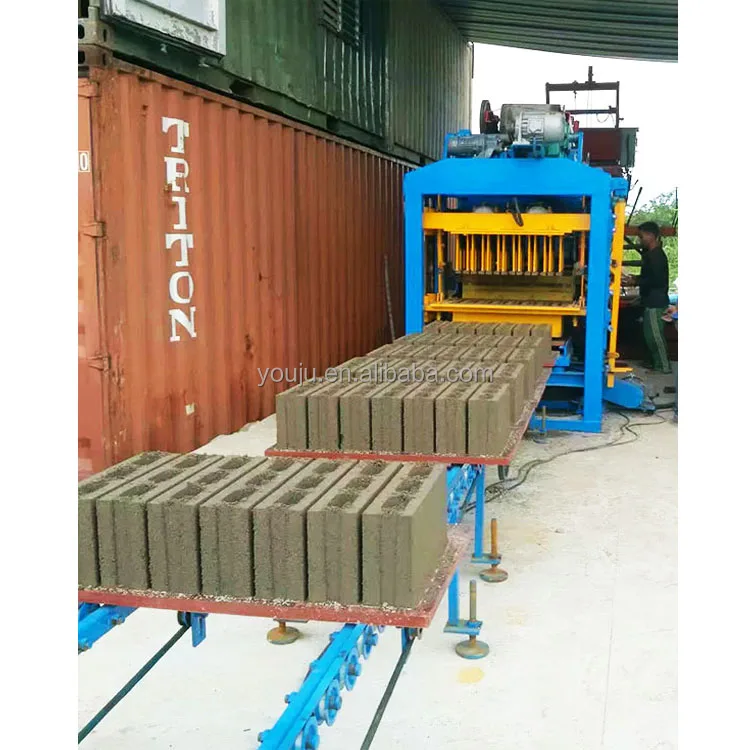
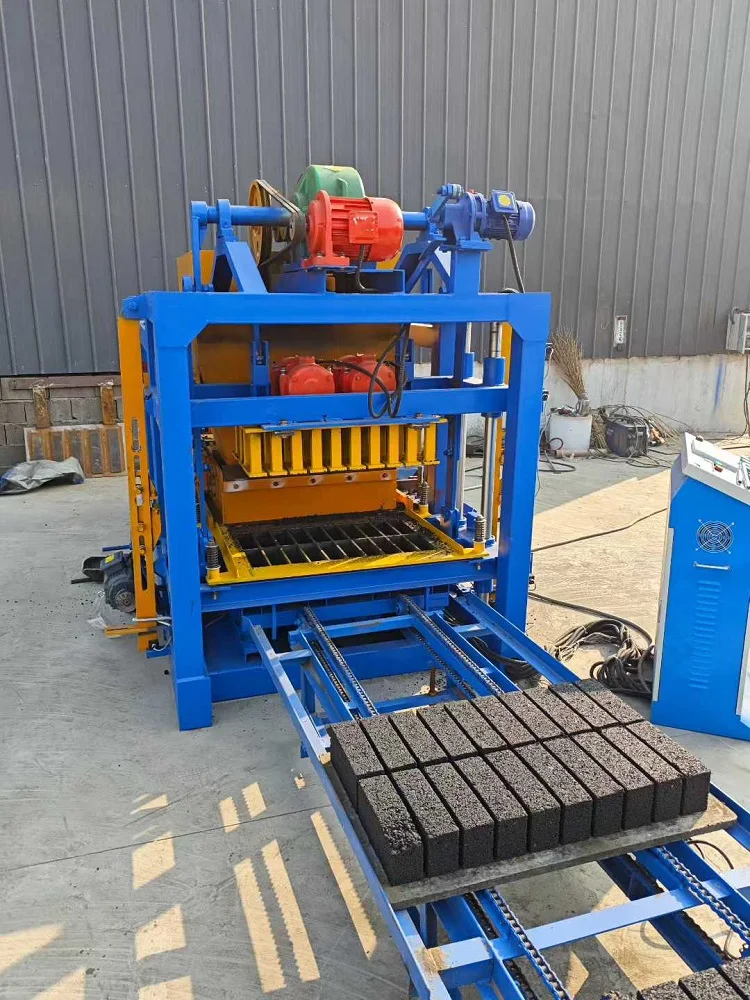
Matched System Intelligence — The QT5-15 places PLC intelligent control at the centre of a fully automatic block line where pallet feeding, material dosing, vibration and demoulding operate as one coordinated cycle rather than isolated manual stations.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT5-15 |
| Product Type | Automatic Concrete Block Making Machine |
| Overall Dimensions | 7400 × 1950 × 2800 mm |
| Total Mass | 5000 kg |
| Overall Power | 32 kW |
| Vibration Frequency | 0–60 Hz |
| Vibration Force | 80 kN |
| Vibration Form | Platform Vibration |
| Moulding Mode | Automatic loading, vibration moulding |
| Demolding Method | Hydraulic |
| Molding Cycle | 15–20 s (basis not stated in source) |
| Pallet Size | 1100 × 550 mm |
| Control System | PLC with touch screen interface |
| Automation Level | Fully automatic (pallet feeding, material feeding, vibrating, demoulding) |
| Hydraulic System | Independent integrated hydraulic station |
| Block Compressive Strength | ≥ 15 MPa |
| Factory Area Required | 1000 m² |
| Output Capacity (Hollow Block 400×200×200 mm) | 900–1200 pcs/h, 7200–9600 pcs/8h (based on 5 pcs/mould, 15–20 s cycle) |
| Output Capacity (Hollow Block 400×150×200 mm) | 1080–1440 pcs/h, 8640–11520 pcs/8h (based on 6 pcs/mould, 15–20 s cycle) |
| Output Capacity (Solid Brick 240×115×53 mm) | 5760–7680 pcs/h, 46080–61440 pcs/8h (based on 32 pcs/mould, 15–20 s cycle) |
| Output Capacity (Rectangular Paver 200×100×60 mm) | 3600–4500 pcs/h, 28800–36000 pcs/8h (based on 25 pcs/mould, 20–25 s cycle) |
| Output Capacity (Zigzag Paver 225×112.5×60 mm) | 2304–2880 pcs/h, 18432–23040 pcs/8h (based on 16 pcs/mould, 20–25 s cycle) |
| Raw Material Compatibility | Fly ash (up to 70%), slag, gangue, sand, crushed stone, cement, water |
| Mould Change | Quick replacement for multi-format production (time not stated in source) |
| Voltage & Frequency | To be confirmed before order |
| PLC Display Language | To be confirmed before order |
| Warranty | 1 year for the whole machine (excluding spare parts) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for building walls | Crushed stone, sand, cement, fly ash blends |
| Solid brick manufacturing for load-bearing masonry | Sand, gangue, slag with cement binder |
| Rectangular paving block for walkways and yards | Fine aggregate and cement mix designs |
| Interlocking zigzag paver for driveways | Graded crushed stone with cement |
| On-site block production for housing projects | Locally sourced aggregate and fly ash |
What "Fully Automatic" Actually Means for Your Shift
Automation only removes labour when every station in the chain keeps pace with the press.
I have watched plant owners invest in an automatic concrete block making machine PLC controlled at the press, then discover the quotation stopped at the mould exit. Pallets still get loaded by hand, wet blocks still get stacked on the floor by two workers, and the press sits idle waiting for the next pallet. The QT5-15 addresses this by specifying pallet feeding, material dosing, vibration and hydraulic demoulding as one continuous automatic sequence — but the downstream stacking and curing rack handling must also be defined before the line ships [NEED_CITE: common gaps in block machine quotations leaving manual bottlenecks]. Without that, your "fully automatic" line still depends on how fast someone can carry a pallet.
PLC Touch Screen as the Single Control Point
The QT5-15 uses a PLC with touch screen interface to manage the entire moulding sequence — from pallet indexing through material feed, vibration profile and hydraulic demoulding. Operators input process data and store recipes for each block format, so switching from hollow blocks to pavers means selecting a saved program rather than manually adjusting timers and valves. The system also provides fault diagnosis on screen, pointing the operator to the specific station that halted the cycle instead of requiring them to trace the problem mechanically.
Batch-to-Batch Consistency Without Operator Timing
On semi-automatic lines, block density varies because one operator holds the vibration a few seconds longer than another, or feeds material slightly unevenly across the mould. The automatic concrete block making machine PLC controlled cycle removes that variation by executing each step at the programmed duration and force every time. The 80 kN vibration force and adjustable 0–60 Hz frequency are applied identically across every cycle, producing blocks that meet the ≥ 15 MPa compressive strength target regardless of who is supervising the shift [NEED_CITE: effect of manual timing variation on block compressive strength consistency].
Reading the Numbers That Matter
The 32 kW overall power must cover vibration motors, hydraulic pump and material feed simultaneously, so buyers should confirm their site supply can sustain continuous draw at that level without voltage drop. The 1100 × 550 mm pallet size determines how many blocks exit per cycle and must match the curing rack dimensions and forklift capacity already on site — ordering a mismatched pallet means rebuilding the curing area. The independent integrated hydraulic station sits isolated from the press vibration and dust, which matters because hydraulic valve contamination is a leading cause of unplanned stops in block plants. The platform vibration form transmits force directly through the mould base, compacting the mix from below for uniform density across the full pallet area.
When the Wrong Configuration Costs More Than the Machine
A block machine configured for a mix design the buyer cannot source locally forces a material change that was never budgeted for, and the PLC recipes stored at the factory no longer match the available aggregate. Voltage and frequency left unconfirmed until the machine arrives can delay commissioning by weeks while transformers or motor replacements are sourced locally [NEED_CITE: commissioning delays from unconfirmed voltage and frequency specifications]. I once saw a line sit idle because the PLC display language was set to a script the local operators could not read, turning a simple fault reset into a phone call across time zones. These are not specification details — they are production blockers.
Why the QT5-15 Is Specified as a Line, Not a Standalone Press
The machine, mould, pallet and handling equipment are specified as one matched system so cycle times align across stations and the press is not left waiting on manual intervention. Automation level is selectable — a buyer can start with the fully automatic press cycle and add stacking or cubing stations later as production volume grows. Every configuration is set against the buyer’s actual mix design, local aggregate and target block format rather than a catalogue default, which means the PLC recipes shipped with the machine reflect real production conditions. Mould design covers the formats the buyer’s market actually sells, with custom drawings available. Installation includes operator training so the team running the line understands both the PLC interface and the mechanical sequence behind it.
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed for each output figure
- Machine specification sheet with confirmed voltage, frequency and PLC display language
- Hydraulic and electrical schematic plus PLC program documentation for on-site fault diagnosis
- Mould drawing and format list matching the block types specified in the contract
- Factory test record demonstrating cycle time and block output per confirmed format
- Wear parts and mould list identifying items to stock before first production run
Installation, Commissioning & Support
- 1000 m² factory area required with level concrete floor to support the 5000 kg total mass
- 32 kW dedicated power circuit matching confirmed voltage and frequency before machine arrival
- Machine arrives dismantled for container loading and requires on-site assembly and alignment
- Commissioning includes PLC parameter setup for local mix design and target block format
- Operator training covers touch screen navigation, recipe storage and fault diagnosis response
- Spare parts package includes hydraulic seals, vibration motor brushes and mould wear plates
Before You Request a Quote
To size the QT5-15 accurately, share the specific block formats your market sells along with the daily output you need for each. Confirm your local voltage, frequency and preferred PLC display language so the control system arrives ready for your operators. If you are upgrading from a semi-automatic line, describe which stations you currently run manually and which you want to automate first.
Frequently Asked Questions
Q: How is the PLC programmed for different block formats, and can the operator store multiple recipes?
A: The touch screen interface allows operators to input and save process parameters — vibration duration, frequency, material feed volume and hydraulic pressure — for each block format. When switching production from hollow blocks to pavers, the operator selects the stored recipe and the automatic concrete block making machine PLC controlled system adjusts the cycle accordingly, eliminating manual recalibration between formats.
Q: What automation level does the QT5-15 ship with, and which stations can be added later?
A: The QT5-15 ships with full automation across pallet feeding, material dosing, vibration and hydraulic demoulding. Downstream stations such as automatic stacking, cubing and enhanced batching can be added as upgrades. This means a plant owner can invest in the intelligent press first and extend automation to the curing area as production volume grows without replacing the core machine.
Q: How does the independent hydraulic station protect against dust and vibration in a block plant?
A: The hydraulic station is physically isolated from the press vibration and the dust generated during material feeding and moulding. This separation prevents particulate contamination of hydraulic valves and reduces seal wear caused by continuous vibration exposure, which directly lowers the frequency of unplanned hydraulic faults during long production runs.
Q: What language options are available for the PLC touch screen, and how is this confirmed?
A: PLC display language is confirmed in writing before production begins. The buyer specifies the preferred language during the quotation stage, and it is verified again before shipment. Confirming this early prevents the situation where operators cannot read fault codes or recipe names on arrival, which would otherwise delay commissioning.
Q: How does the automatic cycle handle pallet feeding and product exit?
A: Pallets are fed automatically from a magazine into the press, and after moulding the loaded pallet exits the machine for downstream handling. The cycle time for pallet indexing must match the moulding cycle so the press is never left waiting. Buyers should specify whether stacking and curing rack handling equipment will be included to close the loop beyond the press exit.