

Description
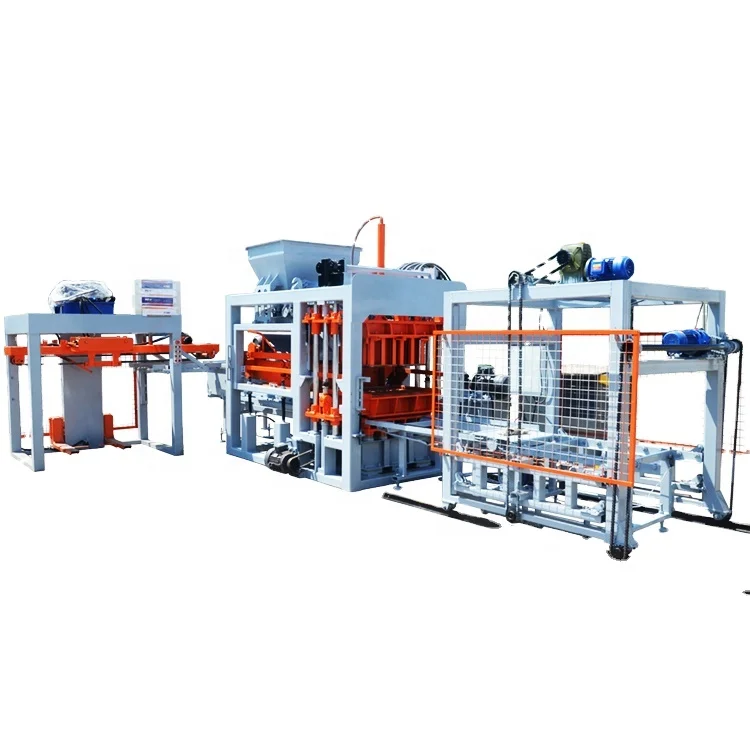
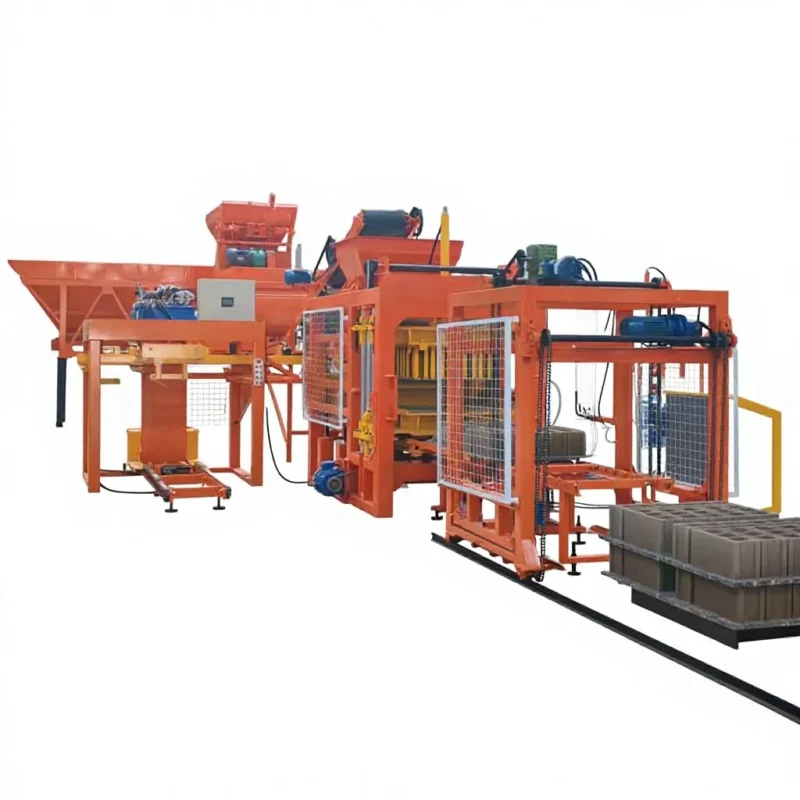
System-Matched Configuration — Every QT6-15 unit leaves the factory with its PLC language, hydraulic pressure, and vibration force set to the buyer’s actual block format and local aggregate, not a catalogue default.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT6-15 |
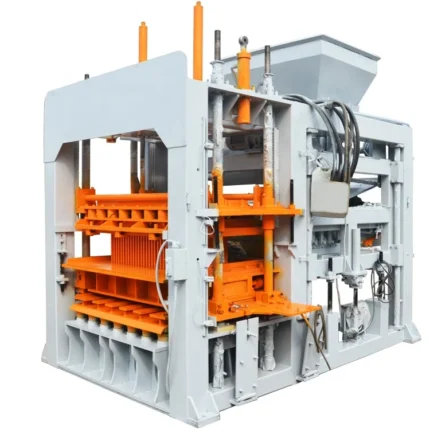
| Product Type | Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 8200×1700×2950 mm |
| Total Mass | 7 T |
| Vibration Frequency | 0-60 Hz |
| Vibration Form | Platform Vibration |
| Vibration Force | 45 kN |
| Moulding Mode | Automatic loading, vibration moulding |
| Demolding Method | Hydraulic |
| Pallet Size | 880×850 mm |
| Molding Cycle | 15-20 s |
| Overall Power | 37 kW |
| Control System | PLC with touch screen and fault diagnosis system |
| Hydraulic System | Independent integrated station, isolated from dust and vibration |
| Compressive Strength of Blocks | More than 15 MPa |
| Factory Area Requirement | 1200 m² |
| Output (Hollow block 400×200×200 mm) | 1080-1440 pcs/hour (basis stated in source) |
| Output (Hollow block 400×150×200 mm) | 1440-1920 pcs/hour (basis stated in source) |
| Output (Solid brick 240×115×53 mm) | 5760-7680 pcs/hour (basis stated in source) |
| Output (Rectangular brick 200×100×60 mm) | 2160-2880 pcs/hour, cycle 20-25 s (basis stated in source) |
| Output (Zigzag brick 225×112.5×60 mm) | 2160-2880 pcs/hour, cycle 20-25 s (basis stated in source) |
| Standards | CE (verify against specific unit) |
Application Suitability
| Application | Material or Output |
|---|---|
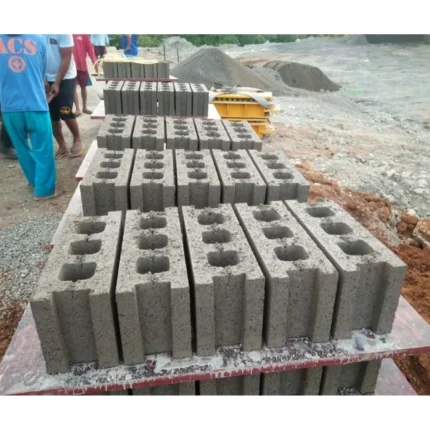
| Hollow block production | Crushed stone, sand, cement, fly ash blends |
| Solid brick production | Fine aggregate and cement mixes |
| Paving brick production | High-density aggregate with pigment layers |
| Interlocking brick production | Interlocking profile moulds with standard aggregates |
| Porous brick production | Lightweight aggregate and permeable mix designs |
Why Your PLC Language Must Be Confirmed Before the Machine Ships
A PLC controlled automatic block making machine is only as intelligent as the operator who can read its screen.
I once watched a QT6-15 sit idle on a Middle East site for two full days because the touch-screen HMI arrived in Chinese. The commissioning engineer could not navigate the fault diagnosis menu, and the local operator could not acknowledge alarms. We had to flash an English firmware image over a unreliable site Wi-Fi connection while the project deadline slipped [NEED_CITE: common PLC language mismatches in exported machinery]. When a plant owner invests in intelligent electronic control, the interface language is not a minor detail — it is the single point of contact between the automation layer and the people who run the line every shift.
What the Touch-Screen HMI Actually Removes from the Operator
The QT6-15 pairs a programmable controller with a graphical touch-screen interface, placing every cycle parameter — vibration duration, hydraulic pressure dwell, feed timing — on a single screen. Operators no longer adjust mechanical limit switches or estimate dwell times by ear. Each block format stores its own recipe, so switching from a 400×200×200 mm hollow block to a 200×100×60 mm paving brick becomes a menu selection rather than a half-shift recalibration. This is where a PLC controlled automatic block making machine earns its keep: the parameters that used to live in one veteran operator’s head are now locked into repeatable digital recipes.
How Built-In Fault Diagnosis Cuts Unplanned Stops
The fault diagnosis system monitors hydraulic pressure, vibration motor current, and sensor positions in real time, then displays an alarm code with a plain-language description on the HMI. Instead of calling a specialist to trace a stalled pallet feeder, the operator reads the alarm, checks the indicated proximity switch, and clears the fault in minutes. Remote diagnostics capability means our service team can review the same alarm log over a network connection, often resolving issues before a flight is booked [NEED_CITE: remote diagnostics adoption in concrete equipment]. Every minute the press is stopped, cured pallets are not stacking; the diagnosis system exists to keep those minutes short.
Reading the Specs That Actually Govern Block Strength
The 45 kN vibration force and independent hydraulic station work together: vibration settles the mix into the mould cavity, then hydraulic pressure compresses it to final density. If vibration frequency is too high for a coarse aggregate, the mix segregates; if hydraulic dwell is too short, the block leaves the mould before full compaction. The 0-60 Hz adjustable vibration range lets the operator dial in the frequency that matches local stone gradation. The 880×850 mm pallet size determines how many blocks fit per cycle, and that pallet must match the curing rack spacing and the forklift tine width already on site — a mismatch means double-handling every wet pallet. At 37 kW overall power, the electrical supply must provide a dedicated circuit with adequate breaker capacity to handle the vibration motor starting surge without tripping neighbouring equipment.
The Cost of Skipping the Automation Audit
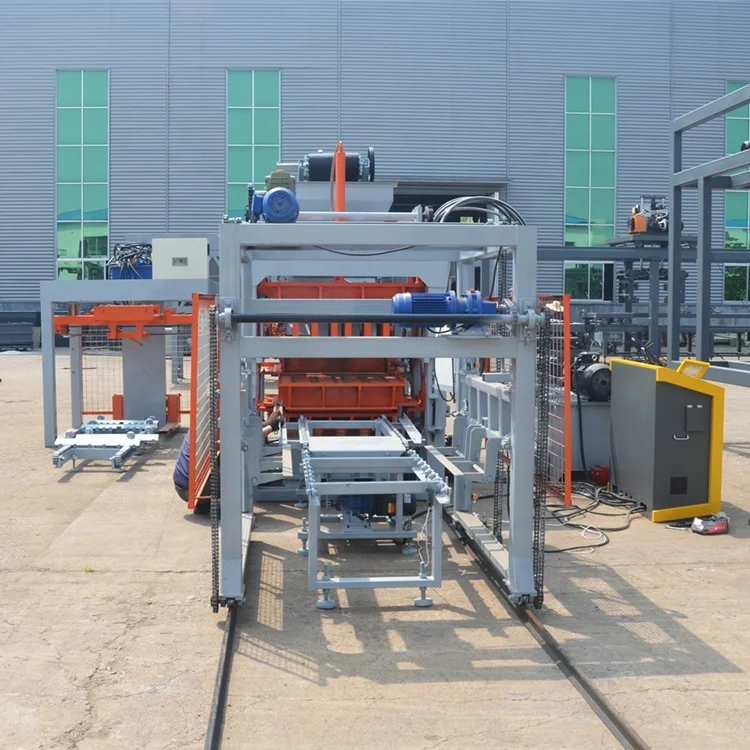
Plant owners who select automation level based on brochure photographs rather than labour availability end up with two problems. A fully automatic stacking and cubing system parked in a workshop with no trained maintenance staff becomes a liability the first time a gripper sensor fails. Conversely, a semi-automatic line that relies on manual pallet handling will bottleneck at the press output the moment daily volume exceeds what two operators can physically move [NEED_CITE: automation mismatch consequences in block plants]. The hidden cost is not the equipment price — it is the throughput gap between what the press can produce and what the surrounding handling can actually move to the curing area.
Why Sourcing the Automation Layer from the Press Builder Matters
Block machinery is our single focus, so the PLC program, hydraulic logic, and mechanical cycle are developed as one system rather than bolted on from separate vendors. We configure each QT6-15 against the buyer’s target block format, local aggregate sieve analysis, and available voltage — not against a generic catalogue setting. Mould design, pallet specification, and handling equipment are matched to the press cycle time so no station waits on another. The automation architecture is upgrade-ready: a buyer can commission the press with manual pallet handling today and add automatic stacking and cubing when volume justifies the investment. Factory test records verify every cycle parameter before the machine is crated, and our documentation package arrives with the machine, not weeks later by email.
Documentation & Verification
- Factory test record showing cycle times for your specific block format before dispatch
- PLC program backup with your confirmed display language loaded and verified
- Hydraulic and electrical schematic matching the as-built configuration
- Voltage, frequency, and control language confirmation sheet signed before production
- Operation and maintenance manual in your operator’s language
- Wear parts and mould list with part numbers for first-year reordering
Installation, Commissioning & Support
- Foundation plan sized to the 8200×1700 mm footprint and 7 T operating mass
- Dedicated 37 kW circuit with breaker rating confirmed against your local voltage and frequency
- PLC language and HMI labels verified with your operators on day one of commissioning
- Vibration frequency and hydraulic pressure tuned to your local aggregate sample on site
- Operator training covering recipe storage, mould change procedure, and fault alarm response
- Wear parts list with mould wear plate and hydraulic seal part numbers for local stocking
What We Need to Size Your Automation Correctly
Tell us the block formats your market actually buys, the daily volume you need to hit, and the labour headcount you plan to run per shift. Share your local aggregate type and the voltage and frequency at the site connection point. If you already have curing racks and forklifts, send the pallet dimensions they accept so we match the pallet feeding and stacking system to your existing handling infrastructure.
Frequently Asked Questions
Q: How is the PLC control language confirmed before the machine ships?
A: We confirm the display language during the order stage and document it on a signed voltage and control confirmation sheet. The PLC program is loaded and tested in the factory with that language active, and a program backup is included in the documentation package so your team can restore it if the HMI is ever replaced.
Q: Can I start with semi-automatic pallet handling and upgrade to full automatic stacking later?
A: Yes. The QT6-15 automation architecture allows the press to run with manual pallet handling initially. When throughput grows, automatic pallet feeding, stacking, and cubing modules can be added without replacing the PLC or the main press frame, because the controller already has the I/O channels reserved for those stations.
Q: How does the fault diagnosis system reduce unplanned downtime?
A: The system monitors hydraulic pressure, motor current, and sensor states continuously and displays alarm codes with plain-language descriptions on the touch screen. Operators can identify and clear common faults without waiting for a specialist, and the alarm log can be shared remotely for faster off-site support.
Q: What automation level is right for my current output target and labour availability?
A: The right level depends on your daily volume target, shift pattern, and available skilled maintenance staff. We map your production flow from raw material feeding through to stacking, then recommend an automation tier that removes bottlenecks without adding complexity your team cannot maintain.