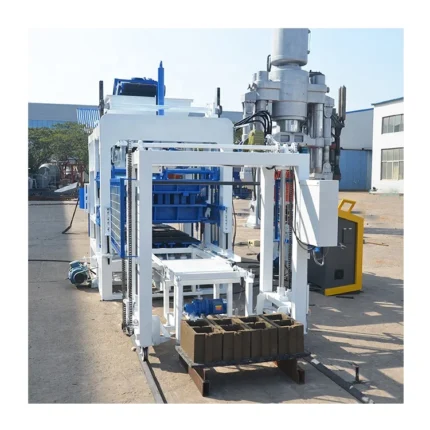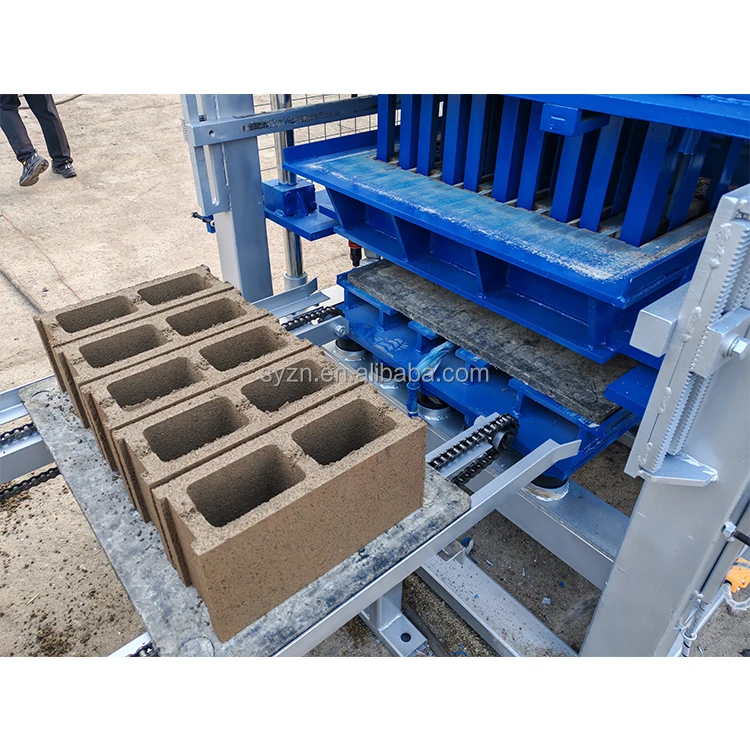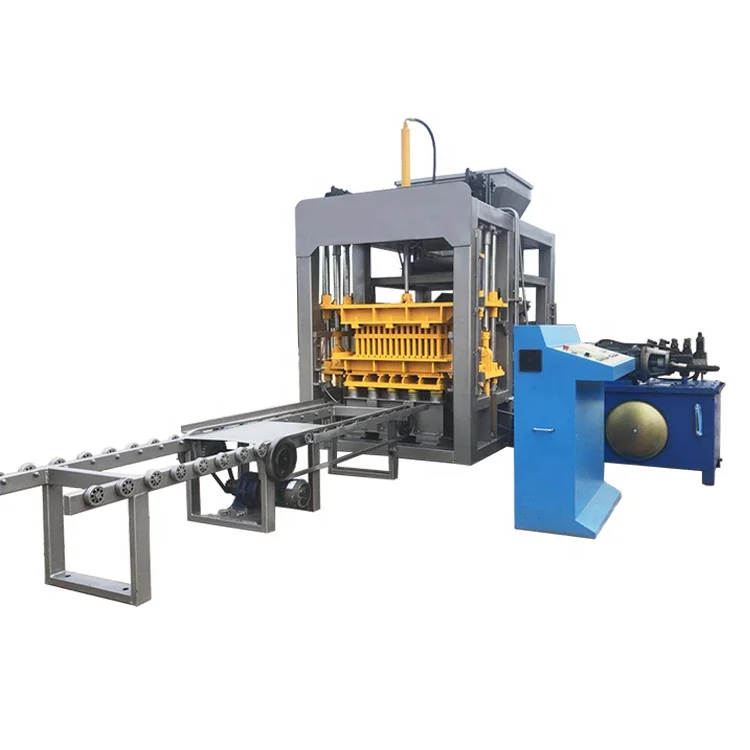

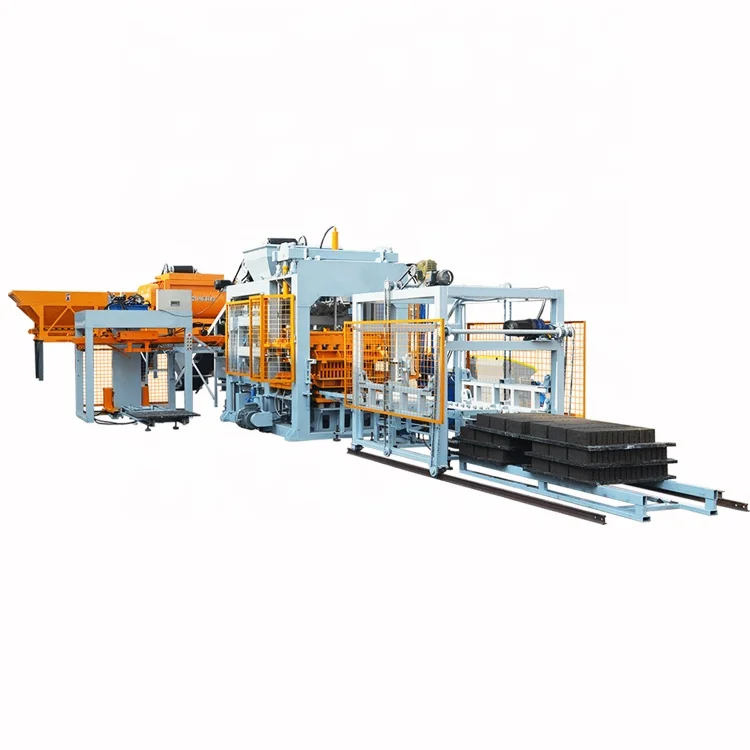

Description
Matched Control Architecture — PLC logic is written against your confirmed mix profile and target block format before assembly, not loaded from a generic template.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT8-15 |
| Product Type | Hydraulic Concrete Block Making Machine |
| Overall Dimensions | 8300 × 1860 × 3000 mm |
| Rated Pressure | 21 MPa |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency | 2800–4500 r/min |
| Vibration Force | 45 kN |
| Pallet Size | 950 × 900 mm |
| Molding Cycle | 15–20 s (basis not stated in source — confirm block format and material) |
| Overall Power | 55.5 kW |
| Total Mass | 8 T |
| Demolding Method | Hydraulic |
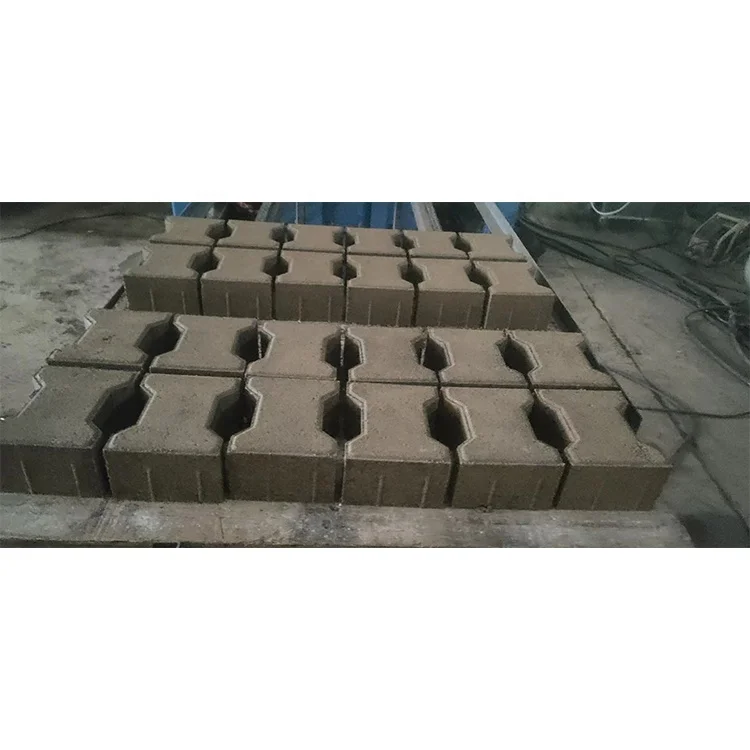
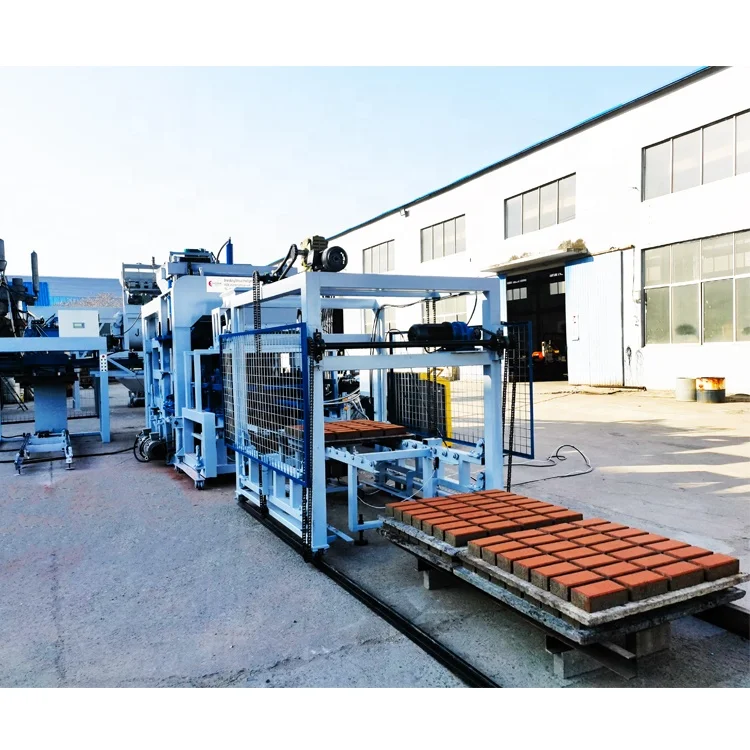
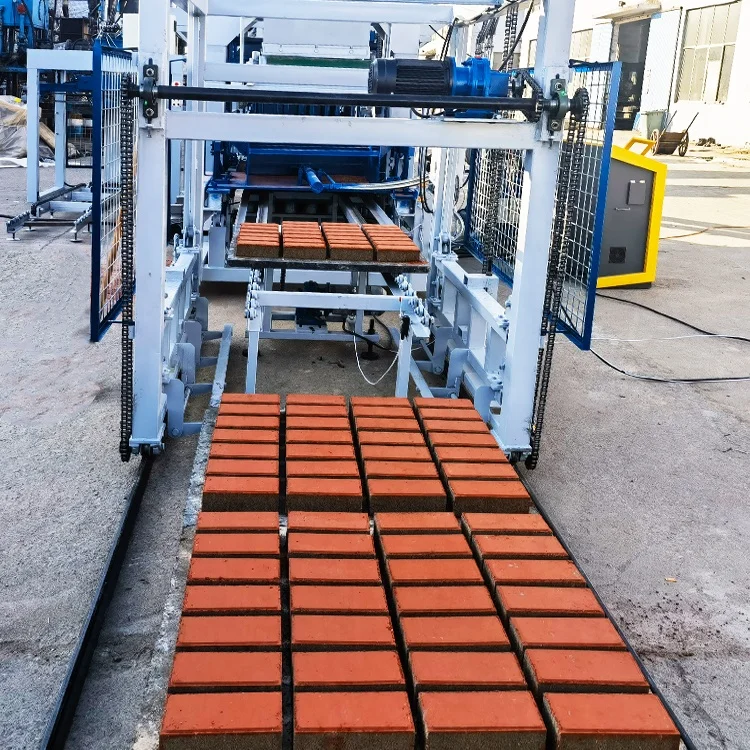
| Applied Products | Hollow blocks, solid blocks, pavers, interlocking blocks, curbstone, colored pavers |
| Voltage & Frequency | Configurable — confirm before production |
| Control System | PLC controlled — confirm brand and display language |
| Automation Level | Selectable from semi-automatic through fully automatic stacking |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for residential and commercial wall systems | Crushed stone, sand, cement, fly ash |
| Solid block manufacturing for load-bearing structures | Gravel, slag, cement blends |
| Paving block and colored paver runs for roads and walkways | Fine aggregate, cement, pigment additives |
| Interlocking brick production for retaining walls and landscapes | Local sand, crushed stone, cement |
| Kerbstone forming for curb and gutter projects | Coarse aggregate, cement, high-pressure hydraulic compaction |
What PLC Control Actually Removes from the Operator
An automatic hydraulic block making machine PLC controlled takes cycle timing, vibration duration, and hydraulic pressure sequencing out of human hands entirely.
When I started on the workshop floor here in Linyi, the most common failure mode was an operator shortening the vibration window because the line looked busy. Blocks left the press under-compacted, and strength test failures showed up days later at the curing yard. With the QT8-15, the PLC holds each stage to its programmed duration regardless of shift pressure, which is the difference between consistent density and random output [NEED_CITE: consistency requirements for concrete block compressive strength testing].
The real question buyers should ask is not whether the machine has a PLC, but whether the PLC program was written against their specific raw material behavior and target block geometry.
How the Automation Sequence Actually Runs
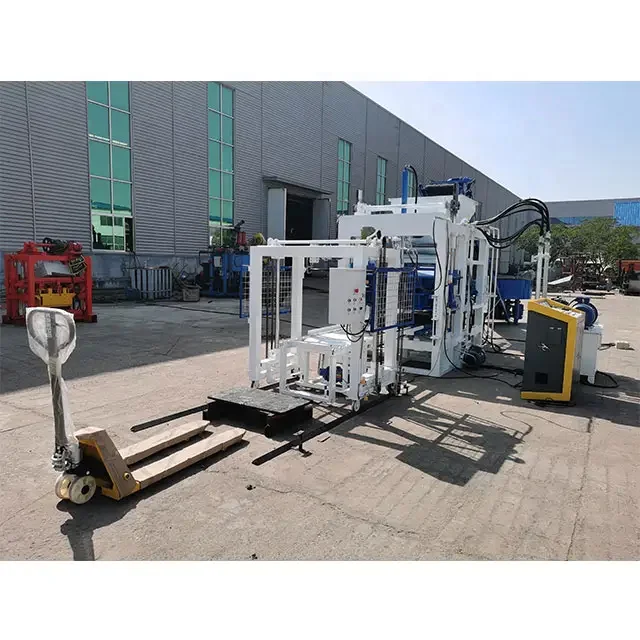
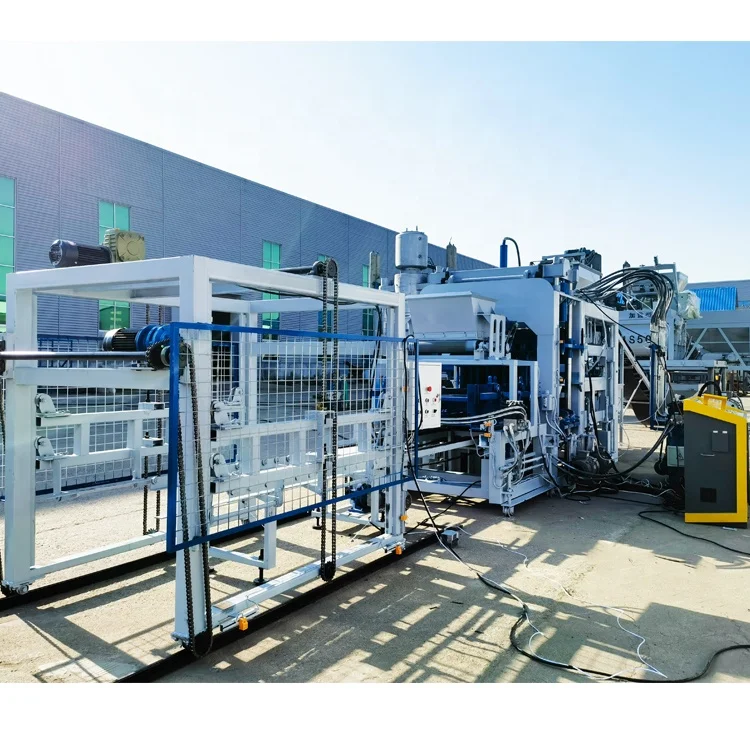
The automatic hydraulic block making machine PLC controlled sequence begins with raw material feeding into the mixer, then moves through pallet indexing, mold filling, vibration compaction, hydraulic demolding, and block ejection. Each station waits for a confirmed signal from the previous one before advancing, so the press never fires on a misaligned pallet or a partially filled mold cavity.
This interlocking logic is what separates a true automatic line from a collection of individually powered stations. If the pallet feeder jams, the press holds. If the mixer has not discharged, the mold stays open. The operator monitors rather than drives the sequence.
Where Consistency Comes from in Practice
Batch-to-batch consistency on a block line depends on three variables staying locked together: vibration frequency, hydraulic pressure, and cycle dwell time [NEED_CITE: relationship between vibration parameters and concrete block density]. The QT8-15 platform vibration system operates across a 2800–4500 r/min range with 45 kN vibration force, and the PLC stores the confirmed set points for each block format.
When a plant switches from hollow blocks to pavers, the operator selects the stored recipe rather than manually adjusting dials. This means the transition does not depend on which operator is on shift or how well they remember the last paver run. The automation upgrade path from semi-automatic operation is a matter of enabling additional stations — automatic pallet feeding, stacking, and cubing — on the same control platform.
Reading the Specs Against Your Actual Line
What the Numbers on the Sheet Actually Mean
The 21 MPa rated pressure and 45 kN vibration force work as a pair. Hydraulic pressure provides the static compaction force that squeezes air voids out of the mix, while platform vibration rearranges aggregate particles into a denser packing arrangement. If either parameter is set without reference to the other, blocks either crack on demolding or come out soft at the core. The 950 × 900 mm pallet size determines how many blocks fit per cycle and must match your curing rack spacing and forklift tine width — a mismatch here means manual restacking after the press does its job.
The 55.5 kW overall power rating covers the main press motor, hydraulic pump, and vibration system running simultaneously. Plants need to confirm their supply can sustain this draw plus the mixer, conveyor, and stacking equipment running on the same bus, otherwise voltage drop during peak demand will trip the PLC mid-cycle.
What Happens When Automation Is Specified Blindly
The Cost of Skipping the Configuration Conversation
Ordering a block press by catalog specs alone means the PLC arrives loaded with default parameters calibrated for a standard sand-cement mix that may not match your local aggregate [NEED_CITE: impact of aggregate gradation on concrete block compaction]. If your crushed stone runs high in fines or your sand carries moisture that varies by season, the default vibration duration will over-compact or under-compact depending on the day.
Voltage and frequency mismatches are the second silent problem. A machine wired for 380V/50Hz running on a 440V/60Hz supply will spin motors faster than the PLC timing expects, throwing off the entire cycle sequence. These are not warranty issues — they are configuration issues that should be resolved before the machine ships.
Why This Is Where the Conversation Starts
Block machinery is the single focus of this operation, which means the QT8-15 press, mold, pallet, and handling equipment are specified as one matched system rather than assembled from separate suppliers. The PLC program is written against the buyer’s confirmed mix design and local aggregate, not loaded from a generic library.
Mold design covers the formats the buyer’s market actually sells, including custom drawings when standard cavity layouts do not fit. The automation level is selectable, so a buyer can start with semi-automatic pallet handling and add stacking and cubing stations later on the same control platform. Installation includes on-site commissioning with operator training so the team knows how to read PLC diagnostics before the first production shift.
Documentation & Verification
- Line layout showing station spacing matched to the 8300 × 1860 mm press footprint
- Capacity calculation stating the block format assumed for the 15–20 s cycle time
- PLC program printout with parameters locked to your confirmed mix and format list
- Hydraulic and electrical schematic showing valve bank and motor circuit assignments
- Factory test record on your specified pallet size and block format before dispatch
- Voltage, frequency, and control display language confirmation signed before production
Installation, Commissioning & Support
- Foundation plan sized for the 8 T machine mass and 21 MPa hydraulic reaction loads
- Dedicated 55.5 kW circuit with voltage and frequency confirmed before wiring begins
- Press arrives partially dismantled for container loading, reassembled on prepared slab
- First-run parameter tuning against your actual raw material feed and mix ratio
- Operator training on PLC recipe selection, fault codes, and manual override procedures
- Wear parts list covering hydraulic seals, vibration springs, and mold liner replacements
What to Include in Your First Inquiry
Before quoting the QT8-15, I need to know the block formats you plan to run, your local aggregate type and gradation, and the voltage and frequency at your site. If you have existing curing racks or forklifts, send the pallet dimensions they accept so the 950 × 900 mm pallet size can be confirmed or adjusted. State your target daily output per format so the capacity calculation is honest from the start.
Frequently Asked Questions
Q: How is the 15–20 s molding cycle verified per block format, and what daily output does that translate to?
A: Cycle time varies by block geometry, mix stiffness, and target density. A hollow block with thin walls compacts faster than a thick kerbstone. Before quoting, we calculate daily output based on your specific format, including mold fill time, vibration dwell, and demolding — not a single catalog number applied across all products.
Q: What PLC brand and display language options are available, and is remote diagnostics supported?
A: The PLC brand and display language are confirmed during the specification stage to match your operator team and local electrical standards. Remote diagnostics capability depends on the selected control platform and your site connectivity. We confirm these details before production begins, not after arrival.
Q: How do I confirm the 950 × 900 mm pallet size matches my curing racks and forklift before ordering?
A: Send us the dimensions of your existing curing rack slots and forklift tine spacing. If the standard pallet does not fit, we adjust the mold cavity layout and pallet size together so the automated handling system aligns with your downstream equipment without manual restacking.
Q: What automation level does the QT8-15 ship with, and what is the upgrade path from semi-automatic?
A: The base configuration covers PLC-controlled press cycling with manual or semi-automatic pallet handling. Additional stations — automatic pallet feeding, stacking, and cubing — can be added on the same PLC platform later, so the upgrade does not require replacing the control system or rewiring the press.
Q: Which voltage and frequency configurations are supported for my target market?
A: The 55.5 kW power system is configurable to match your local supply. Voltage, frequency, and phase must be confirmed before production so motors, the hydraulic pump, and PLC power supply are wound and rated correctly. We document the confirmed specification in the electrical schematic before the machine ships.