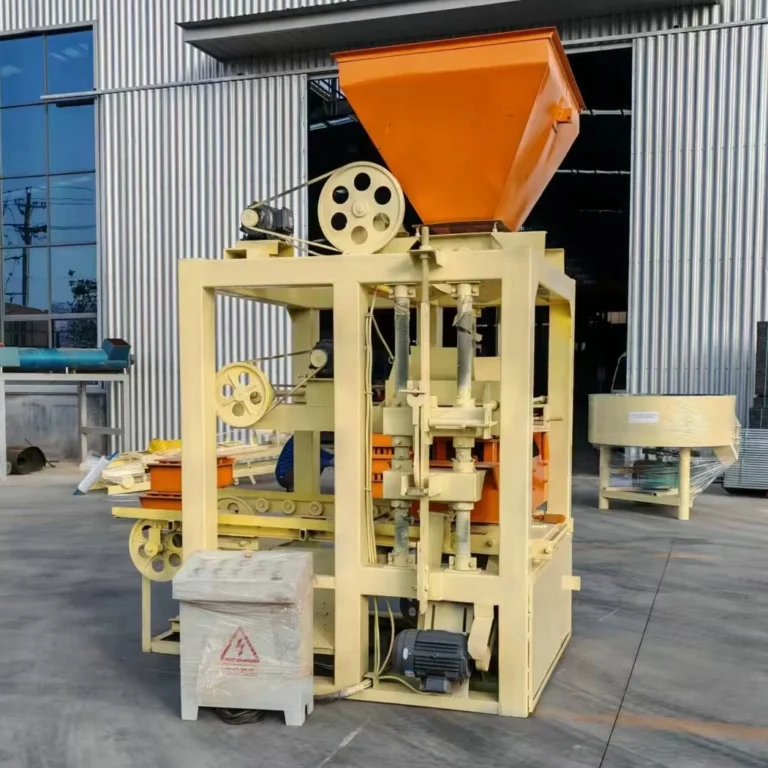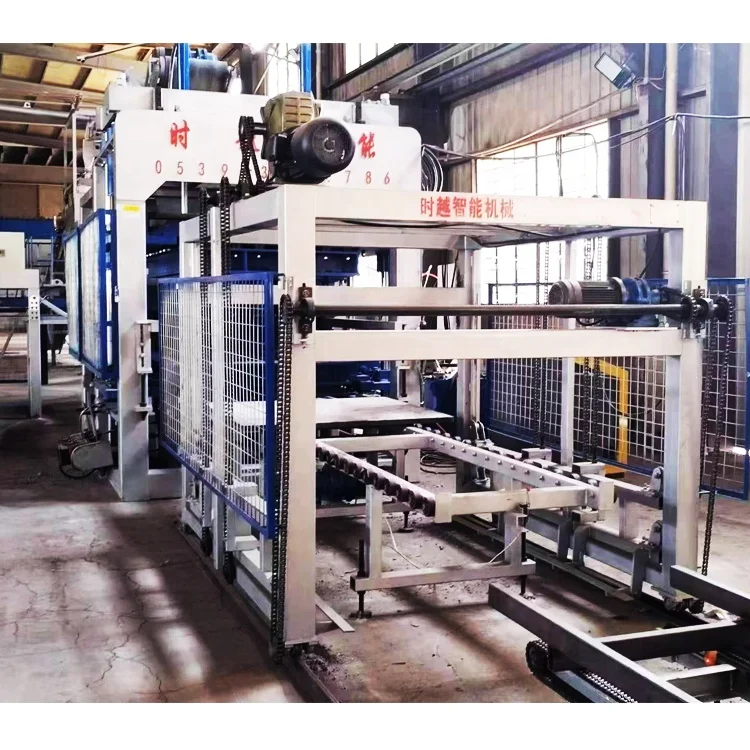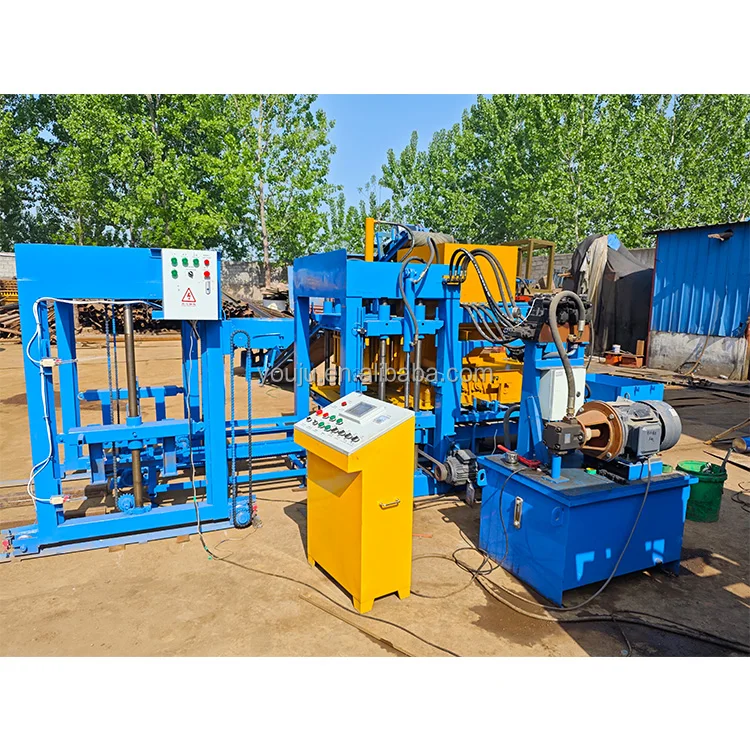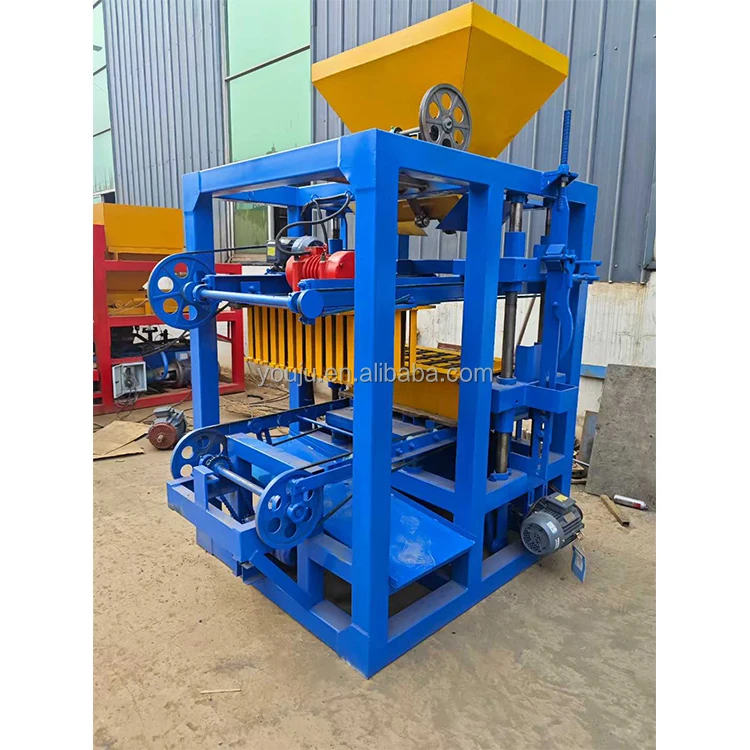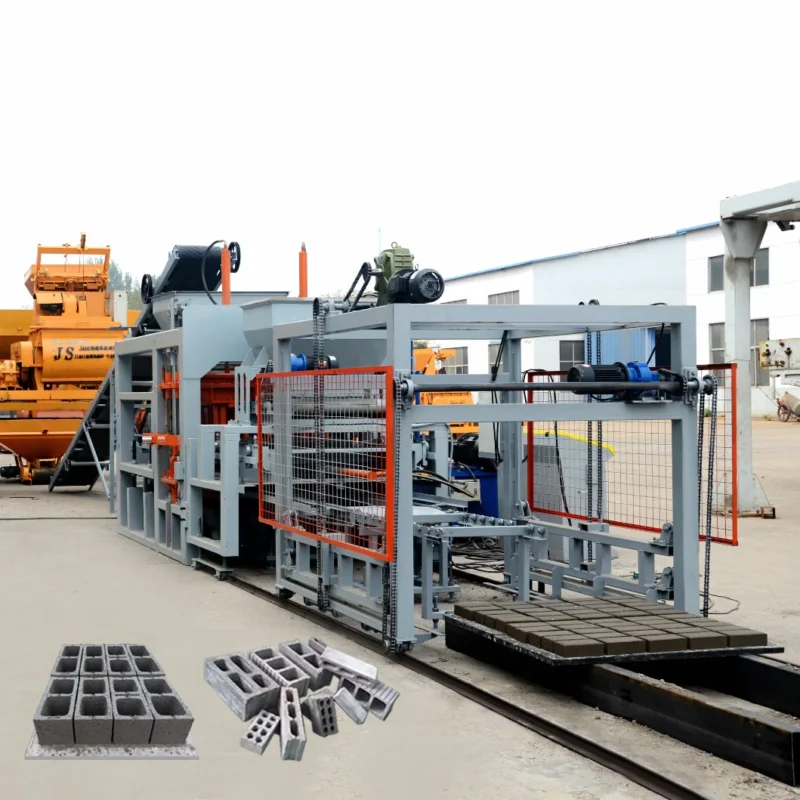


Description
Matched to your mix design — the QT8-15 control system is calibrated to the buyer’s actual aggregate and target block format before dispatch, not shipped with a catalogue default program.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT8-15 |
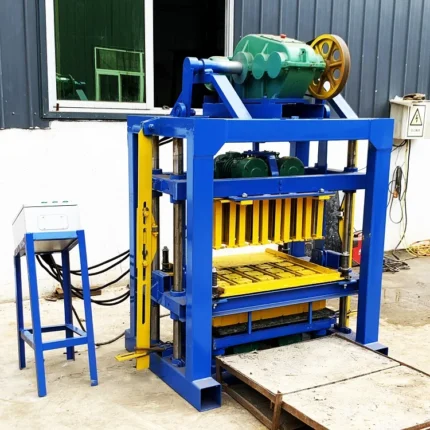
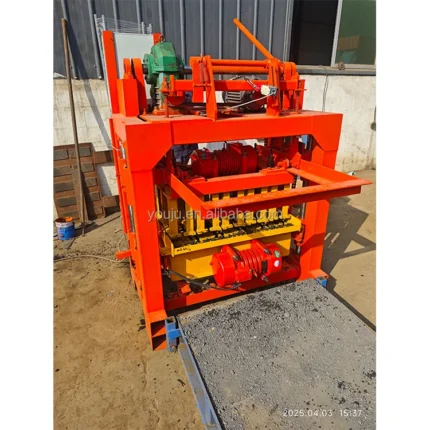
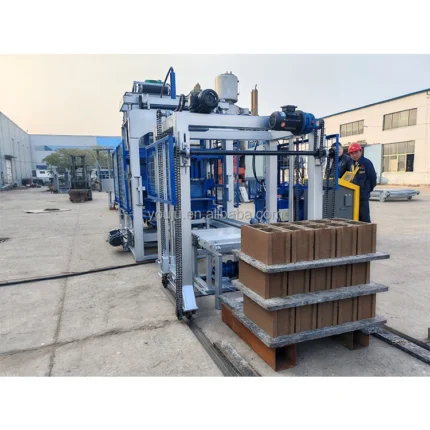
| Product Type | Fully Automatic Hydraulic Block Making Machine |
| Overall Dimensions (L×W×H) | 8300×1860×3000 mm |
| Total Mass | 9 T |
| Overall Power | 55.5 kW |
| Rated Pressure | 21 MPa |
| Vibration Form | Platform vibration |
| Vibration Frequency | 2800~4500 r/min |
| Vibration Force | 45 kN |
| Pallet Size | 950×900 mm |
| Molding Cycle | 15-25 S (basis not stated in source — confirm block format / material / thickness) |
| Demolding Method | Hydraulic |
| Factory Area | 500 m² |
| Control System | Computer controlled, fully automatic (source value — verify against manufacturer catalog) |
| Automation Level | Fully automatic |
| Standards | CE, ISO 9001 |
Application Suitability
| Application | Material or Output |
|---|---|
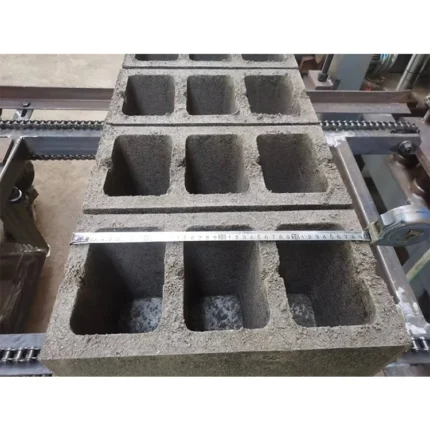
| Hollow block production | Crushed stone, sand, cement, fly ash |
| Solid block production | Gravel, sand, cement, slag |
| Paving block and colored paver production | Fine aggregate, cement, pigment |
| Interlocking block production | Crushed stone, sand, cement |
| Curbstone production | Coarse aggregate, cement |
Why Voltage Confirmation Must Happen Before the Machine Ships
The automatic QT8-15 block making machine PLC controlled system is only as reliable as the electrical specification it was built against.
I learned this the hard way in the Pearl River Delta. A QT8-15 unit arrived at a site running three-phase 440V, but the control cabinet had been wired for 380V. The panel went black on first power-up. The installation crew sat idle for three weeks waiting for a step-down transformer while the contractor’s schedule unraveled. That single oversight cost more in lost time than the transformer itself [NEED_CITE: voltage and frequency standards by export market]. Every automatic QT8-15 block making machine PLC controlled configuration should have its voltage, frequency, and panel language locked in writing before the control cabinet goes onto the bench.
How the PLC Removes Operator Guesswork
The computer-controlled system on the QT8-15 manages the complete molding cycle — from raw material feed timing through vibration duration to hydraulic demolding. Operators no longer decide when to stop the vibration or when to lift the upper mold. The PLC holds the recipe, and each cycle follows it identically. This is what separates batch-to-batch consistency from hoping the morning shift and afternoon shift produce blocks of the same density.
What Automation Actually Takes Off the Operator’s Plate
In a fully automatic configuration, pallet feeding, block stacking, and curing rack handling run without manual intervention. The operator’s role shifts from physical labor to monitoring the HMI and responding to alarms. For a plant owner moving from semi-automatic operation, this means the labor headcount on the press line drops and the remaining staff focus on quality checks rather than pallet lifting. The automatic QT8-15 block making machine PLC controlled architecture also supports a staged upgrade — a buyer can commission the press with manual pallet handling first and add automatic stacking later when volume justifies it [NEED_CITE: CE machinery directive requirements for industrial equipment].
Reading the Specs That Actually Matter on the Press Floor
The 21 MPa rated pressure and 45 kN vibration force work together to compact the mix into a dense, dimensionally stable block. Pressure alone would leave voids; vibration alone would not consolidate the bottom layer. The platform vibration mode directs force vertically downward through the mold box, which is where compaction matters most for hollow blocks with thin webs. The long-period over-length guide bearing keeps the upper mold aligned with the mold box throughout the press stroke, preventing scuffing that widens tolerances over thousands of cycles. The 950×900 mm pallet size must match the curing racks and forklifts already at the buyer’s site — a mismatch here means either rebuilding the curing area or running a non-standard pallet that no local supplier stocks.
The Cost of Skipping the Line-Level Conversation
When a buyer orders the press alone without specifying how pallets will feed in and how wet blocks will stack out, the machine arrives and sits half-finished. Operators end up pulling pallets by hand and stacking blocks on the floor, which introduces handling damage before curing even begins. A control panel delivered in the wrong language forces the operator to memorize alarm codes instead of reading them, and the first fault becomes a crisis [NEED_CITE: common causes of commissioning delays in exported block machinery]. These are not equipment failures — they are specification failures that surface only after the container is opened.
Why Buyers Source This Press Through Our Line
Block machinery is our single focus, so the QT8-15 press, its molds, pallets, and handling equipment are specified as one matched system rather than assembled from unrelated suppliers. The automation level is selectable — a buyer can start with semi-automatic pallet handling and add stacking and cubing modules as production volume grows. Each mold is designed for the block formats the buyer’s market actually sells, including custom drawings when local standards require non-standard dimensions. The control system is configured against the buyer’s confirmed voltage and preferred operating language before the cabinet is closed. Installation includes on-site commissioning and operator training so the crew running the automatic QT8-15 block making machine PLC controlled line on day one knows every alarm and recipe.
Documentation & Verification
- Line layout showing capacity calculation per block format for the QT8-15
- PLC specification sheet listing every automated station included in the line
- Voltage, frequency, and control language confirmation signed before production
- Factory test record verifying pressure and vibration matched to your mix
- Mold drawing and format list covering every block type in your quotation
Installation, Commissioning & Support
- Foundation plan sized for the QT8-15’s 9 T mass and 55.5 kW power draw
- Dedicated circuit specification for the 21 MPa hydraulic pump motor
- Pallet conveyor alignment checked against your 950×900 mm pallet stock
- PLC recipe loaded and verified with your local aggregate on first run
- Operator training covering mold change procedure and alarm response
- Wear parts list with hydraulic seal and vibration motor part numbers
What to Include with Your Inquiry
Send your target block formats, daily output requirement, and the local aggregate you will run — crushed stone, fly ash, or slag each behave differently under vibration. Confirm your site voltage, frequency, and the language your operators read. If you already have curing racks and forklifts, share the pallet dimensions they accept so the line is configured around your existing infrastructure.
Frequently Asked Questions
Q: What automation levels are available and how does the upgrade path work?
A: The QT8-15 ships in configurations from semi-automatic with manual pallet handling to fully automatic with stacking and cubing. A buyer can commission the press semi-automatic and add pallet feeding, stacking, or cubing modules later without replacing the core machine. The PLC architecture accepts additional I/O stations as they are installed.
Q: How is the PLC configured and which display languages are supported?
A: The control system is programmed with the buyer’s confirmed recipes before dispatch. Display language is specified during the order confirmation stage so the HMI reads in the operator’s language on day one. Voltage and frequency are wired to match the site supply, avoiding transformer delays at commissioning.
Q: Which stations are included in the automatic line and how do cycle times match?
A: The full line can include raw material feeding, mixing, pallet feeding, the press itself, stacking, and curing rack handling. Cycle times across stations are balanced so the press is not left waiting for a pallet or for the stacker to clear. The capacity calculation in the line layout states which block format each timing assumes.
Q: How are vibration force and hydraulic pressure matched to my mix design?
A: The 45 kN vibration force and 21 MPa hydraulic pressure are set during factory testing using the buyer’s stated aggregate and mix proportions. The multiaxis synchronizer vibration mode directs compaction downward through the mold. If the local aggregate differs from the test sample, parameters are adjusted on-site during commissioning.